Buhler Extruder Parts: Screw Elements for BCTM and BCTA Twin-Screw Extruders
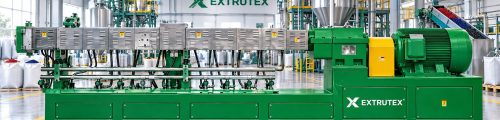
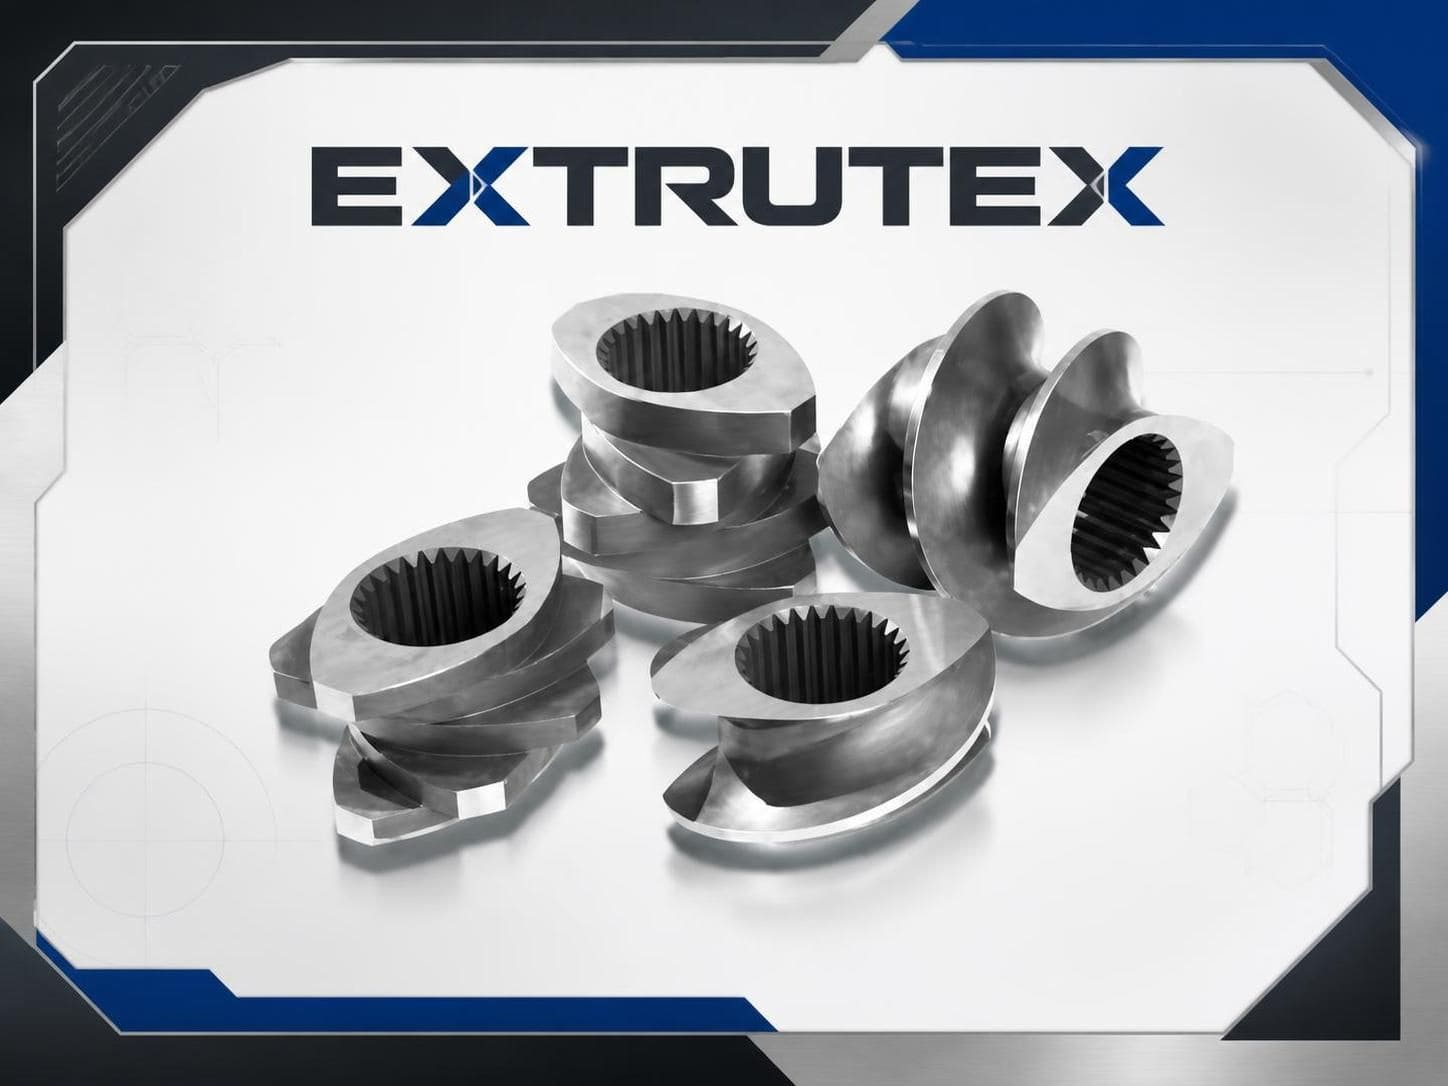
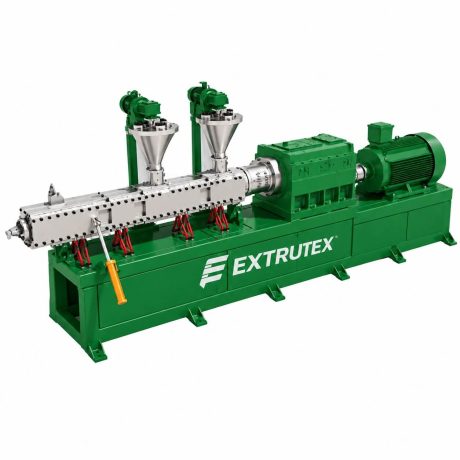
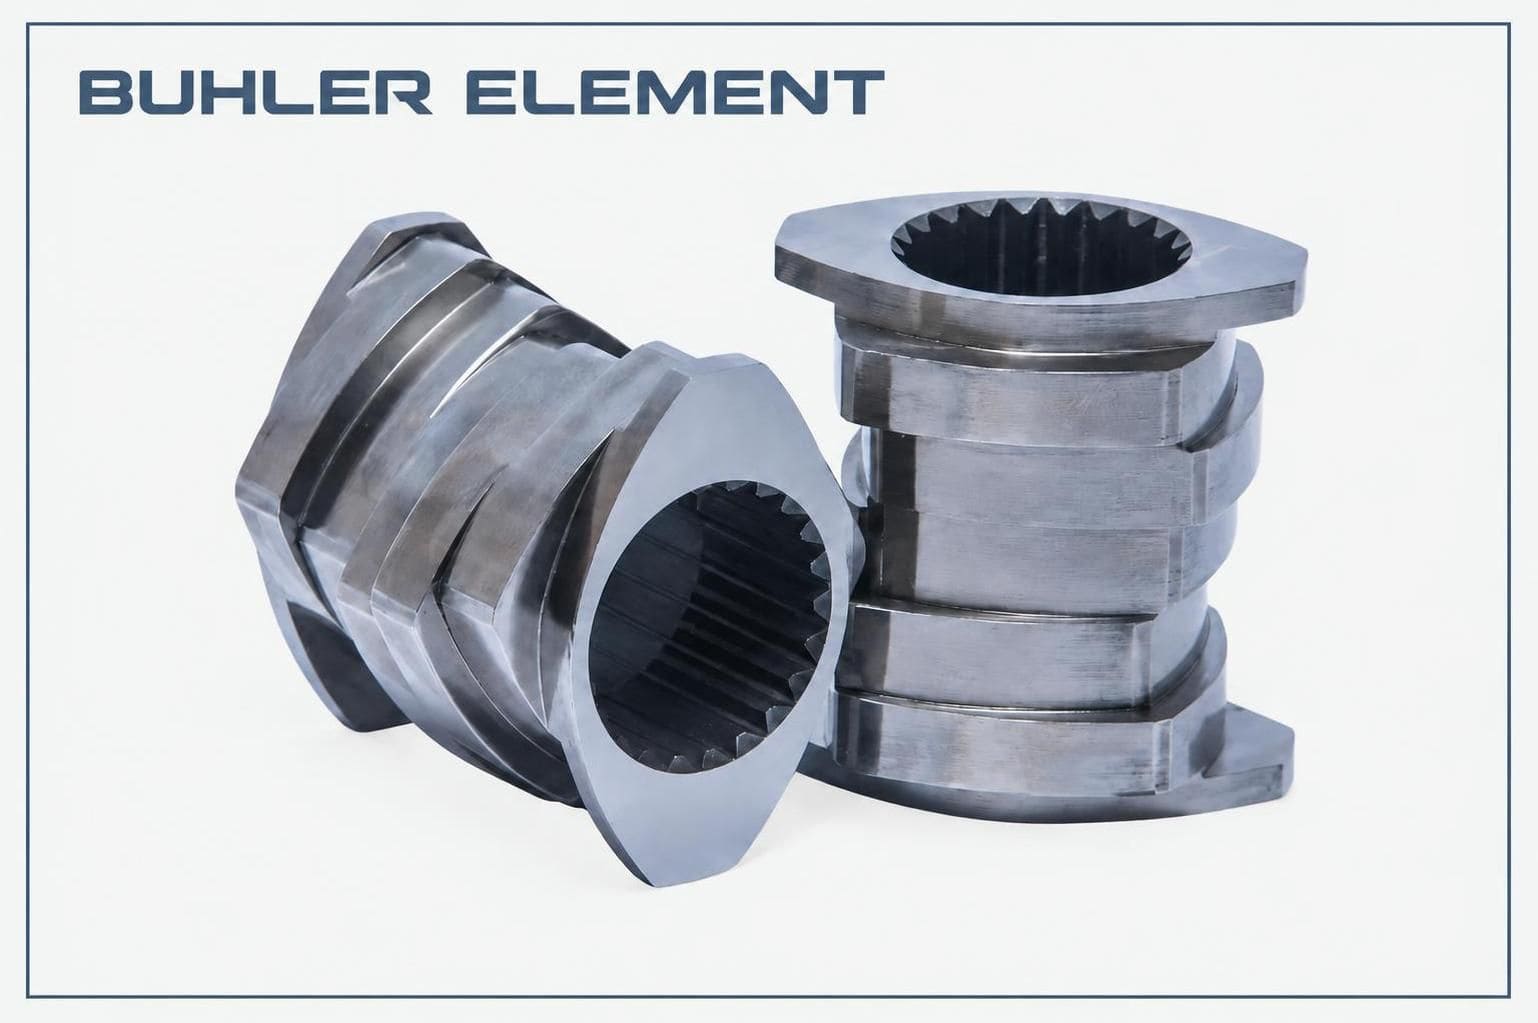
EXTRUTEX manufactures replacement screw elements, kneading blocks, screw shafts, barrel sections and wear liners for Buhler BCTM and BCTA twin-screw extruders used in pasta, snack food and breakfast-cereal production. We manufacture individual replacement components and complete screw assemblies, working from available OEM drawings or accurately measured samples.
Extruder components operate under continuous mechanical loading, temperature variation, pressure and product abrasion. Over time, wear can change the original screw geometry, reduce conveying efficiency and affect the cooking or forming characteristics of the finished product. Replacing worn components with accurately manufactured parts helps restore the intended machine configuration without automatically replacing the complete screw assembly.
Our replacement parts are manufactured to the required machine dimensions and component geometry. Where the original drawings are available, they provide the starting point for production. Where drawings are unavailable, our engineering team can assess a physical sample, measure its critical dimensions and reconstruct the required profile, subject to the condition of the sample and availability of sufficient reference information.
Replacement parts for individual positions or complete screw sets.
EXTRUTEX can manufacture individual conveying elements, kneading blocks, shafts, barrel sections and liners. We can also produce matched replacement sets when several screw positions or the shaft itself require replacement.
Technical Specifications
| Technical Data |
Specification |
| Compatible platforms |
Buhler BCTM and BCTA twin-screw extruders |
| Applications |
Pasta, snack food and breakfast-cereal production |
| Components |
Screw elements, kneading blocks, screw shafts, barrel sections and wear liners |
| Interchangeability |
Manufactured to the required OEM dimensions and geometry; compatibility confirmed by model and position |
| Base materials |
300-series stainless steel, nitrided materials or through-hardened materials, according to application |
| Abrasive product duty |
Corrosion-resistant wear-grade material, with 58–62 HRC specified for suitable grades and applications |
| Dimensional verification |
CMM inspection report per batch |
| Minimum order |
1 piece |
| Material documentation |
EN 10204 3.1 certificate on request |
| Lead time |
Typically 30–45 days for imported-machine spare parts, plus transit time |
The stated 30–45 day lead time applies after material availability and drawing confirmation. Special surface finishes, non-standard material grades or additional processing requirements may extend the manufacturing schedule. Final delivery time also depends on the destination and selected transport method.
Buhler BCTM and BCTA Replacement Components
A twin-screw extruder is a complete processing system. The screw elements, shafts and barrel sections must work together to provide the required conveying, mixing, cooking and pressure-building performance. A replacement component therefore needs more than a similar outside diameter. Its dimensions, profile and position within the screw configuration must correspond to the original machine arrangement.
1. Conveying Screw Elements
Conveying elements transport the food material through the extruder and contribute to filling, residence time and pressure development. Their geometry influences how consistently the material moves through the processing zones.
EXTRUTEX manufactures replacement conveying elements for the relevant BCTM and BCTA configurations. Depending on the original design, the replacement may require a specific flight profile, pitch, outside diameter, element length and shaft connection.
- Single-flight and double-flight conveying elements, where specified by the original configuration.
- Replacement screw segments for individual worn positions.
- Elements manufactured to the required outside diameter and pitch.
- Components produced from OEM drawings or verified physical samples.
- Individual pieces or matched groups for a complete screw assembly.
2. Kneading Blocks
Kneading blocks are important in the cooking and mixing sections of snack and breakfast-cereal extruders. They influence mechanical energy input, material distribution, mixing intensity and the development of the required product structure.
Their geometry and stagger arrangement must match the original processing design. Changing the block configuration without considering the complete screw layout can affect product quality, temperature development and machine loading.
- Single-piece kneading blocks.
- Assembled kneading-block configurations.
- Replacement blocks for worn cooking and mixing zones.
- Custom-manufactured blocks based on drawings or measured samples.
3. Screw Shafts and Shaft Assemblies
The screw shaft transfers torque from the drive system to the screw elements. Its spline or keyway, shaft diameter, length and connection details determine how the assembled components fit and operate.
A worn or damaged shaft can affect the positioning and alignment of the screw elements. In some cases, replacing individual elements is not sufficient because the shaft connection itself has become worn or damaged. EXTRUTEX can manufacture replacement shafts and shaft assemblies according to the required mechanical specifications.
- Replacement screw shafts.
- Splined or keyed shaft configurations, as required.
- Individual shafts and assembled shaft sets.
- Dimensional machining based on approved drawings or samples.
4. Barrel Sections and Wear Liners
The barrel provides the processing chamber around the screw assembly. Its internal bore, centre distance, section length and connection arrangement must correspond to the original extruder design.
EXTRUTEX manufactures replacement barrel sections and wear liners for compatible BCTM and BCTA configurations. Depending on the original construction, the barrel may use a treated bore, replaceable liner or another specified wear-resistant surface.
- Figure-eight barrel sections for twin-screw configurations.
- Replacement wear liners.
- Polished or plated barrel bores, where specified.
- Nitrided, alpha-101, HIP PM or laser-clad liner options, subject to application and material verification.
- Replacement components manufactured to confirmed bore and connection dimensions.
Where Buhler Screw Elements Actually Wear
Wear does not necessarily develop evenly along the screw. The positions exposed to the greatest pressure, shear, temperature and abrasive contact are often the first to show measurable dimensional changes. The dominant wear location depends on the product, recipe, operating conditions and screw configuration.
Wear Patterns in Pasta Production
On pasta lines, the pressure-building section and the final conveying elements ahead of the die can experience significant wear. These components help build and maintain the pressure needed to push stiff, relatively low-moisture dough through the die.
The screw must convey the dough consistently while maintaining the pressure required for stable forming. As the conveying geometry wears, the machine may no longer produce the same pressure and flow conditions as before. Operators may notice changes in output stability, die performance or the shape of the finished pasta.
The actual wear distribution depends on the dough formulation, moisture level, operating temperature, production rate and die resistance. Inspection should therefore consider the complete processing configuration rather than assuming that one screw position always wears first.
Wear Patterns in Snack and Breakfast-Cereal Production
On snack and cereal lines, kneading blocks in the cooking and mixing zones can experience substantial wear. These sections operate under mechanical shear at elevated temperature while processing flour, bran and other ingredients.
Mineral and vitamin premixes may also introduce additional abrasive particles, depending on their composition and concentration. As the kneading-block geometry changes, the mechanical energy input and mixing behaviour can change as well.
The result may be a gradual change in cooking performance, product texture or process consistency. In some cases, operators may need to increase specific mechanical energy to approach the previous product condition. This should be assessed alongside feed rate, moisture, temperature and other operating variables.
Important maintenance point:
A worn screw element does not always cause an immediate mechanical failure. Product changes, reduced process stability and altered energy requirements can be early indicators. Dimensional inspection during planned maintenance helps identify wear before it develops into a more serious production problem.
What Does Dimensionally Interchangeable Mean?
A replacement element must match the relevant mechanical and geometric characteristics of the original component. Similar appearance alone is not enough to establish compatibility.
For EXTRUTEX, dimensional interchangeability means checking the critical dimensions and geometry required for the replacement element to fit the intended shaft position and operate within the existing screw arrangement.
| Inspection Point |
What Must Be Confirmed |
| Spline or keyway |
Connection profile, dimensions and fit on the screw shaft. |
| Outside diameter |
Element diameter and required clearance within the barrel. |
| Pitch |
Flight lead and conveying geometry. |
| Element length |
Axial dimension and position within the screw assembly. |
| Stagger angle |
Angular arrangement of kneading or mixing elements. |
| Centre distance |
Relationship between the two screw axes and the barrel bore. |
| Profile |
Flight shape and other geometry needed to reproduce the original function. |
Where the dimensions are confirmed, replacement elements can be manufactured for use alongside original Buhler components on the same shaft. Mixing original and replacement parts should still be based on verified dimensions and the correct assembly sequence. A replacement part should not be installed solely because its outside diameter appears correct.
Manufacturing Without Original Drawings
Not every spare-parts enquiry arrives with a complete engineering drawing. In some cases, the original part number is unavailable, the machine has been operating for many years, or the OEM drawing cannot be obtained. A physical sample can provide the starting point for reverse engineering.
EXTRUTEX can assess worn components and reconstruct their geometry when sufficient reference information remains. The process begins with identifying the machine platform, component position and original dimensions that can still be measured.
Our Measurement and Reconstruction Process
- Identify the machine: Review the machine nameplate and confirm whether the equipment is a BCTM or BCTA platform.
- Identify the component position: Establish where the worn element is installed within the screw assembly.
- Inspect the sample: Measure the outside diameter, length, shaft connection, pitch and other accessible features.
- Assess wear: Determine whether the original geometry remains measurable or has been substantially altered.
- Reconstruct the profile: Use available drawings, unworn areas or other reliable reference components to establish the intended geometry.
- Confirm before production: Review the proposed dimensions and manufacturing requirements before machining begins.
When severe wear has removed the original profile, the damaged component alone may not provide enough information for an accurate reconstruction. In that situation, EXTRUTEX may request a section drawing, an additional sample or photographs of the same component position from another machine.
We do not guess critical dimensions.
If the available sample cannot establish the original geometry with sufficient confidence, additional reference information is required before production. This helps avoid manufacturing a replacement that fits physically but does not reproduce the intended screw configuration.
Material Selection for Pasta, Snack and Cereal Extruders
Material selection depends on the product being processed and the operating conditions at each screw position. A general pasta application may require different wear and corrosion properties from a snack formulation containing mineral premixes or other abrasive ingredients.
The material must also be suitable for its intended position. Product-contact components have different requirements from non-contact mechanical parts, and the material designation alone does not establish food-contact compliance.
| Application or Component |
Material Direction |
| General product-contact duty |
300-series stainless steel, with nitriding or through-hardening considered only where appropriate for the selected grade and application. |
| Abrasive product-contact duty |
Suitable corrosion-resistant wear-grade material. A hardness range of 58–62 HRC may be specified for compatible grades and verified heat-treatment conditions. |
| Non-product-contact positions |
Nitrided steel or tool steel, according to the mechanical and wear requirements. |
| Barrel bore |
Polished or plated bore, depending on the original construction and process requirements. |
| Wear liners |
Nitrided, alpha-101, HIP PM or laser-clad options, subject to the required specification and suitability for the application. |
300-Series Stainless Steel
300-series stainless steels are used in many food-processing environments because of their corrosion-resistance characteristics. The specific grade must be selected according to the product, cleaning conditions, operating temperature and mechanical loading.
For screw elements and other product-contact components, the required finish and cleanability should be considered alongside the material. A material certificate and a stated stainless-steel grade do not, by themselves, establish compliance with every food-contact requirement.
Through-Hardened Wear-Resistant Materials
Abrasive formulations can require a harder wear surface or a material with improved resistance to mechanical abrasion. Where the application calls for a corrosion-resistant grade with a hardness target of 58–62 HRC, the material and heat-treatment route must be checked together.
Not every stainless-steel grade can achieve this hardness range while retaining the required corrosion resistance and mechanical properties. Final selection should therefore be based on the exact material designation and operating conditions.
Barrel Bore and Liner Treatments
Barrel bore condition affects the working clearance between the screw elements and the barrel. Surface wear can change the processing behaviour and reduce the effectiveness of the original screw geometry.
Depending on the original barrel design, EXTRUTEX can assess polished or plated bores and liner solutions using nitrided materials, alpha-101, HIP PM or laser cladding. The final option must be confirmed against the required dimensions, wear conditions and product-contact requirements.
Dimensional Inspection and Quality Documentation
Replacement components need to be checked against the agreed drawing or dimensional reference. EXTRUTEX uses dimensional inspection to verify the critical features of manufactured parts and to help maintain consistency across a production batch.
Available Inspection and Documentation
- CMM dimensional report: Coordinate measurement results for agreed critical dimensions.
- Material certificate: EN 10204 3.1 documentation on request.
- Hardness records: Hardness results for applicable materials and heat treatments.
- Case-depth records: Available where a specified surface-hardening process is used.
- Pre-shipment photographs: Photographs of components before packing.
The inspection scope is agreed according to the component, drawing and purchase requirements. If a specific measurement report, material certificate or additional inspection is required, it should be confirmed before production.
Individual Screw Elements or Complete Screw Sets?
The correct replacement scope depends on the condition of the existing screw assembly. Replacing every element is not automatically necessary when only a small number of positions are worn.
Individual Replacement Components
When the shaft and the majority of the screw elements remain within the required dimensions, EXTRUTEX can manufacture individual replacement components for the affected positions. This approach can reduce the number of parts that need to be replaced during maintenance.
Matched Replacement Sets
A matched set may be more appropriate when multiple processing zones show wear, several elements are outside tolerance or the complete screw arrangement needs to be renewed. A matched set is manufactured according to the agreed assembly configuration and dimensional requirements.
When the Shaft Also Needs Replacement
If the shaft connection is worn or damaged, replacing the screw elements alone may not restore the required fit. The shaft should be inspected together with the elements, particularly at the spline or keyway and other critical connection areas.
| Existing Condition |
Possible Replacement Scope |
| Only a few elements show measurable wear |
Individual replacement elements. |
| Several positions across one processing zone are worn |
Replacement group or matched zone set. |
| Multiple zones show wear or inconsistent dimensions |
Complete matched screw set, subject to inspection. |
| Shaft connection is worn or damaged |
Replacement elements together with shaft repair or replacement assessment. |
| Barrel bore or liner is worn |
Barrel section or liner replacement assessment. |
How to Request a Buhler Spare Parts Quotation
A quotation can often be prepared from basic machine and component information. An original drawing is useful but is not always essential. The more accurately the machine model and component position are identified, the easier it is to confirm the correct replacement specification.
Information to Send EXTRUTEX
- Machine nameplate photograph: A clear image showing the machine model and available identification details.
- Component position: The screw position or processing zone where the worn element is installed.
- Component photograph: A photograph of the worn part with a ruler or scale in the frame.
- OEM part number: If the original number is visible, include it with the enquiry.
- Application: Confirm whether the machine processes pasta, snacks or breakfast cereal, and provide relevant product information.
- Quantity: State whether you require one component, several positions or a complete screw set.
For barrel sections and wear liners, additional information may be required, including the bore dimensions, centre distance, section length, connection arrangement and relevant mounting details.
Minimum order: 1 piece.
EXTRUTEX accepts enquiries for individual screw elements as well as complete screw assemblies. Send the machine nameplate, component position and available photographs so that the required dimensions and compatibility can be assessed before machining.
Manufacturing Lead Time and Delivery
The typical manufacturing lead time for imported-machine spare parts is 30–45 days after material availability and drawing confirmation. This is a production estimate rather than a guaranteed delivery date.
The schedule may change according to the selected material, manufacturing complexity, heat treatment, surface finishing and inspection requirements. Special stainless-steel grades or non-standard surface finishes may require additional preparation and processing time.
Transit time is additional to manufacturing lead time and depends on the destination, shipment method and transport arrangements.
Why Choose EXTRUTEX for Buhler Replacement Parts?
- Individual components or complete sets: Replace only the positions that require attention or request a matched screw assembly.
- Drawing-based manufacturing: Production can be based on available OEM drawings and confirmed engineering dimensions.
- Sample-based reconstruction: Worn components can be measured and assessed when original drawings are unavailable, provided sufficient reference geometry remains.
- Material options: Material selection can be matched to the product, wear conditions and component position.
- Dimensional inspection: CMM inspection reports are available per batch.
- Documentation: EN 10204 3.1 certificates and additional inspection records can be requested.
- Low minimum quantity: Orders can start from one replacement component.
EXTRUTEX is an independent manufacturer of replacement extruder components. Buhler, BCTM and BCTA are referenced only to identify the compatible machine platforms. EXTRUTEX is not affiliated with, authorised by or endorsed by Buhler.
Frequently Asked Questions
1. Do you supply Buhler extruder parts as well as complete screw sets?
Yes. EXTRUTEX manufactures individual screw elements, kneading blocks, screw shafts, barrel sections and wear liners, as well as complete matched screw sets. Many enquiries involve replacing only the worn positions on an existing shaft. Where several zones are worn, we can assess a larger replacement scope.
2. Are BCTM and BCTA parts interchangeable with each other?
Not necessarily. BCTM and BCTA are different machine platforms, and their screw dimensions, shaft connections and barrel bores may differ. The machine nameplate and component position should be checked before confirming compatibility.
3. What wears first on a Buhler pasta or snack line?
On pasta lines, the pressure-building section and final conveying elements ahead of the die can experience significant wear. On snack and breakfast-cereal lines, kneading blocks in the cooking zone can wear more quickly. Actual wear depends on the formulation, operating conditions and screw configuration.
4. Can you manufacture Buhler parts when no original drawing is available?
Yes, provided sufficient reference information is available. EXTRUTEX can measure a physical sample and reconstruct its geometry. If wear has removed the original profile, an additional sample, drawing or reference component may be needed to establish the correct dimensions.
5. What documentation comes with a Buhler replacement element?
A dimensional inspection report is available with each shipment. On request, EXTRUTEX can also provide EN 10204 3.1 material certificates, hardness results, case-depth records where applicable and CMM measurement documentation for the batch.
6. Can I order only one screw element?
Yes. The minimum order quantity is one piece. Individual replacement elements can be manufactured when the required dimensions and component position have been confirmed.
7. Can replacement elements be installed alongside original Buhler elements?
They can be manufactured for mixed assemblies when the relevant dimensions, shaft connection and screw geometry have been verified. Compatibility should be confirmed for the exact machine model and element position before installation.
8. What information is needed for a quotation?
Start with a machine nameplate photograph, the worn component position and a photograph of the part with a ruler or scale. An OEM part number or original drawing is also helpful where available.
9. What materials are available for food extruder screw elements?
Material options include 300-series stainless steel and other suitable wear-resistant materials, depending on the product and component position. The exact grade, heat treatment and surface finish must be selected according to the operating and product-contact requirements.
10. Can you manufacture barrel sections and wear liners as well?
Yes. EXTRUTEX can manufacture replacement barrel sections and wear liners based on the required bore geometry, centre distance, section length, connection details and material specification.
11. How long does manufacturing take?
The typical lead time for imported-machine spare parts is 30–45 days after material availability and drawing confirmation. Special materials and surface finishes may require additional time. Transit time is additional.
12. Can you provide a complete matched screw assembly?
Yes. EXTRUTEX can manufacture a matched set according to the confirmed screw configuration. The scope can include conveying elements, kneading blocks and the associated shaft components, depending on the machine specification.
13. How do I know whether individual elements or a complete set should be replaced?
The decision depends on the measured condition of the existing screw assembly. If only a few positions are worn and the shaft and remaining elements are within the required dimensions, individual replacement may be appropriate. If wear is widespread or the shaft connection is damaged, a larger replacement scope may be more suitable.
14. Are the replacement parts original Buhler components?
No. EXTRUTEX manufactures independent replacement components for compatible Buhler extruder platforms. The parts are produced according to confirmed dimensions and engineering requirements; they are not represented as original Buhler-manufactured parts.
Request Buhler BCTM or BCTA Replacement Parts
For screw elements, kneading blocks, screw shafts, barrel sections or wear liners, send EXTRUTEX your machine nameplate photograph, the component position and available part measurements. Our engineering team can review the information, identify the required reference dimensions and confirm the manufacturing scope before production.
Whether you need one worn conveying element or a complete matched screw assembly, EXTRUTEX can assess the replacement requirements for your Buhler BCTM or BCTA twin-screw extruder.



-
(0 customer reviews)