Andritz Extruder Parts: Screw Elements, Barrels and Shafts for Feed and Aquafeed Lines
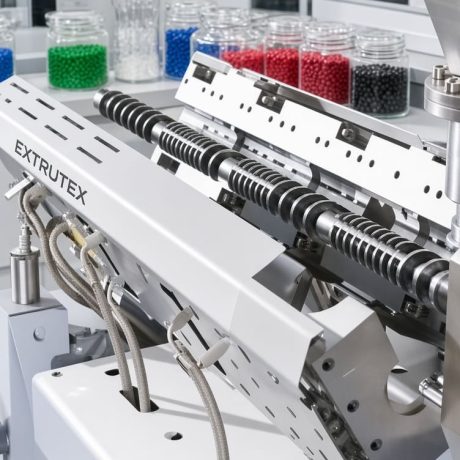
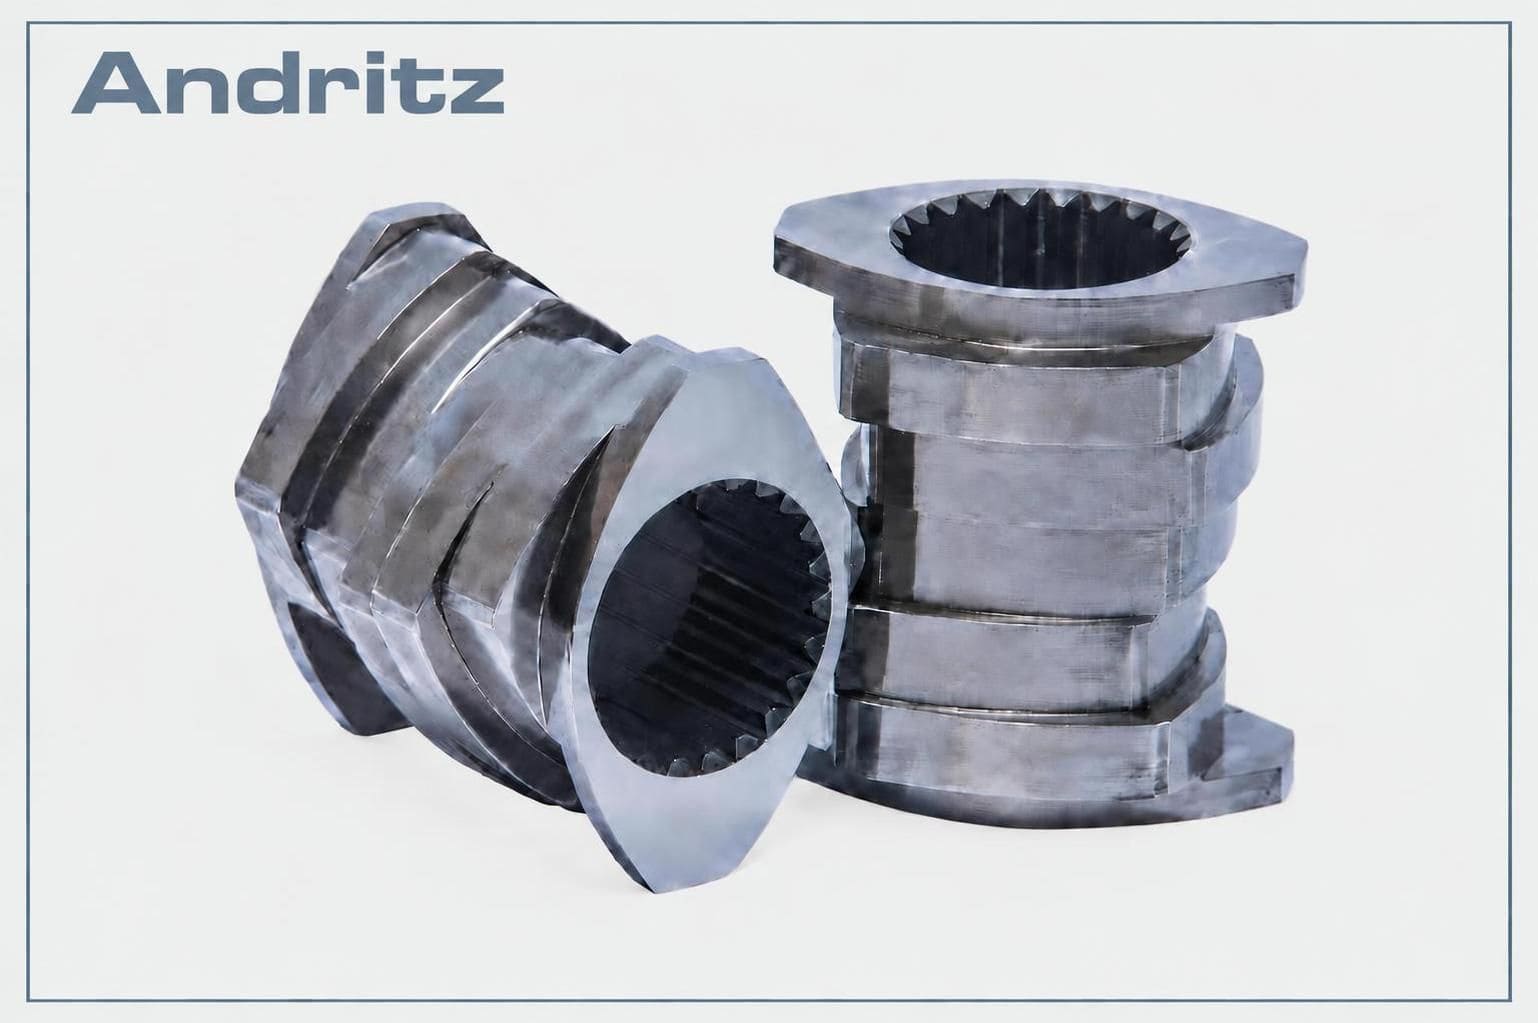
EXTRUTEX manufactures replacement screw elements, kneading blocks, screw shafts, barrel sections and wear liners for Andritz feed, aquafeed and food extrusion equipment. These components are engineered around the machine configuration, original dimensions and operating requirements.
Feed and aquafeed extrusion can expose screw and barrel components to abrasion, corrosion and sustained mechanical loading. Mineral premixes, bone meal, salt and other recipe ingredients can affect the service life of both screw elements and barrel surfaces. Selecting the correct material is important, but so is maintaining the correct operating clearance between the screw flights and barrel bore.
Replacement parts for Andritz extrusion equipment
We confirm the machine platform and component geometry from the machine nameplate, original drawings or measured samples. Because Andritz equipment includes different platform names, sizes and generations, we do not publish an unverified universal model list.
Technical Specifications
| Platforms covered |
Andritz feed, aquafeed and food extruders, subject to machine identification and dimensional confirmation |
| Available components |
Screw elements, kneading blocks, screw shafts, shaft assemblies, barrel sections and wear liners |
| Interchangeability |
Manufactured to match verified OEM dimensions and geometry |
| Base material options |
300-series stainless steel for suitable product-contact applications; selected corrosion-resistant wear grades for abrasive duty |
| Hardness |
58–62 HRC for suitable corrosion-resistant grades and verified heat treatments, where specified |
| Verification |
CMM dimensional inspection report per batch |
| Minimum order |
1 piece |
| Documentation |
EN 10204 3.1 material certificate on request |
| Lead time |
Approximately 30–45 days after material availability and geometry confirmation, plus transit |
Final material grade, hardness, surface treatment and inspection requirements are confirmed according to the component position, recipe, operating conditions and applicable product-contact requirements.
Why Feed and Aquafeed Extrusion Is Demanding on Wear Parts
Feed extrusion is not simply food extrusion with different ingredients. The recipe and operating conditions can create a demanding environment for the screw and barrel assembly. Abrasive particles, corrosive ingredients and sustained mechanical loading may act together, increasing wear and making material selection particularly important.
1. Abrasive Wear
Limestone, mineral premixes, bone meal and other hard ingredients can abrade screw flight crests, kneading surfaces and barrel bores. The degree of wear depends on particle hardness, particle size, concentration, moisture and processing conditions.
2. Corrosion
Salt in marine aquafeed formulations and acidic recipe inclusions may attack unsuitable materials or surface treatments. Corrosion can produce pits and local surface damage that may become starting points for further abrasive wear.
3. Mechanical Loading
Feed and aquafeed processes may require sustained torque and specific mechanical energy to achieve the required cooking, density and pellet durability. Actual loading depends on the formulation, moisture content, throughput and process configuration.
4. Combined Wear
Abrasion and corrosion can reinforce each other. A damaged or pitted surface may become more vulnerable to material removal, while increasing clearance can change the mechanical and thermal conditions inside the extruder.
Material selection must follow the recipe. A poultry feed formulation and a marine aquafeed formulation running on similar equipment may require different wear-resistant and corrosion-resistant material solutions.
How to Identify Screw and Barrel Wear Before Failure
On feed and aquafeed extrusion lines, changes in finished product quality can appear before an obvious mechanical failure. These changes are useful warning signs, although they are not proof of component wear on their own. Formulation, moisture, conditioning, temperature, screw speed and other process variables can produce similar effects.
Common operating and product indicators
-
Falling pellet durability index: Pellet durability may decline even when the main process settings have not changed.
-
Changing bulk density: Bulk density may drift as the extrusion process changes. For aquafeed, changes in pellet density can also affect the finished product's sinking or floating behaviour.
-
Increasing specific mechanical energy: Operators may need to increase energy input to maintain a similar cooking or product result.
-
Reduced throughput: Production capacity may eventually fall, although this can happen after clearance has already increased significantly.
Measure clearance at planned shutdowns
The most reliable way to monitor screw and barrel wear is to measure the screw flight crest and the corresponding barrel bore. Record the results at planned maintenance intervals and compare them over time.
Where applicable, measure bore diameter and roundness at multiple positions along the barrel. Inspect screw flight dimensions, surface condition and the relationship between the screw and barrel. A single measurement may not reveal the full wear pattern.
Maintenance recommendation: Measure screw elements and barrel liners during the same shutdown. Replacing screw elements without checking the barrel bore can leave a new screw set operating in an oversized or out-of-round barrel.
Andritz Extruder Parts Manufactured by EXTRUTEX
EXTRUTEX supplies replacement components for feed, aquafeed and food extrusion equipment. Parts can be manufactured individually or as matched sets, depending on the maintenance requirement and the condition of the existing screw and barrel assembly.
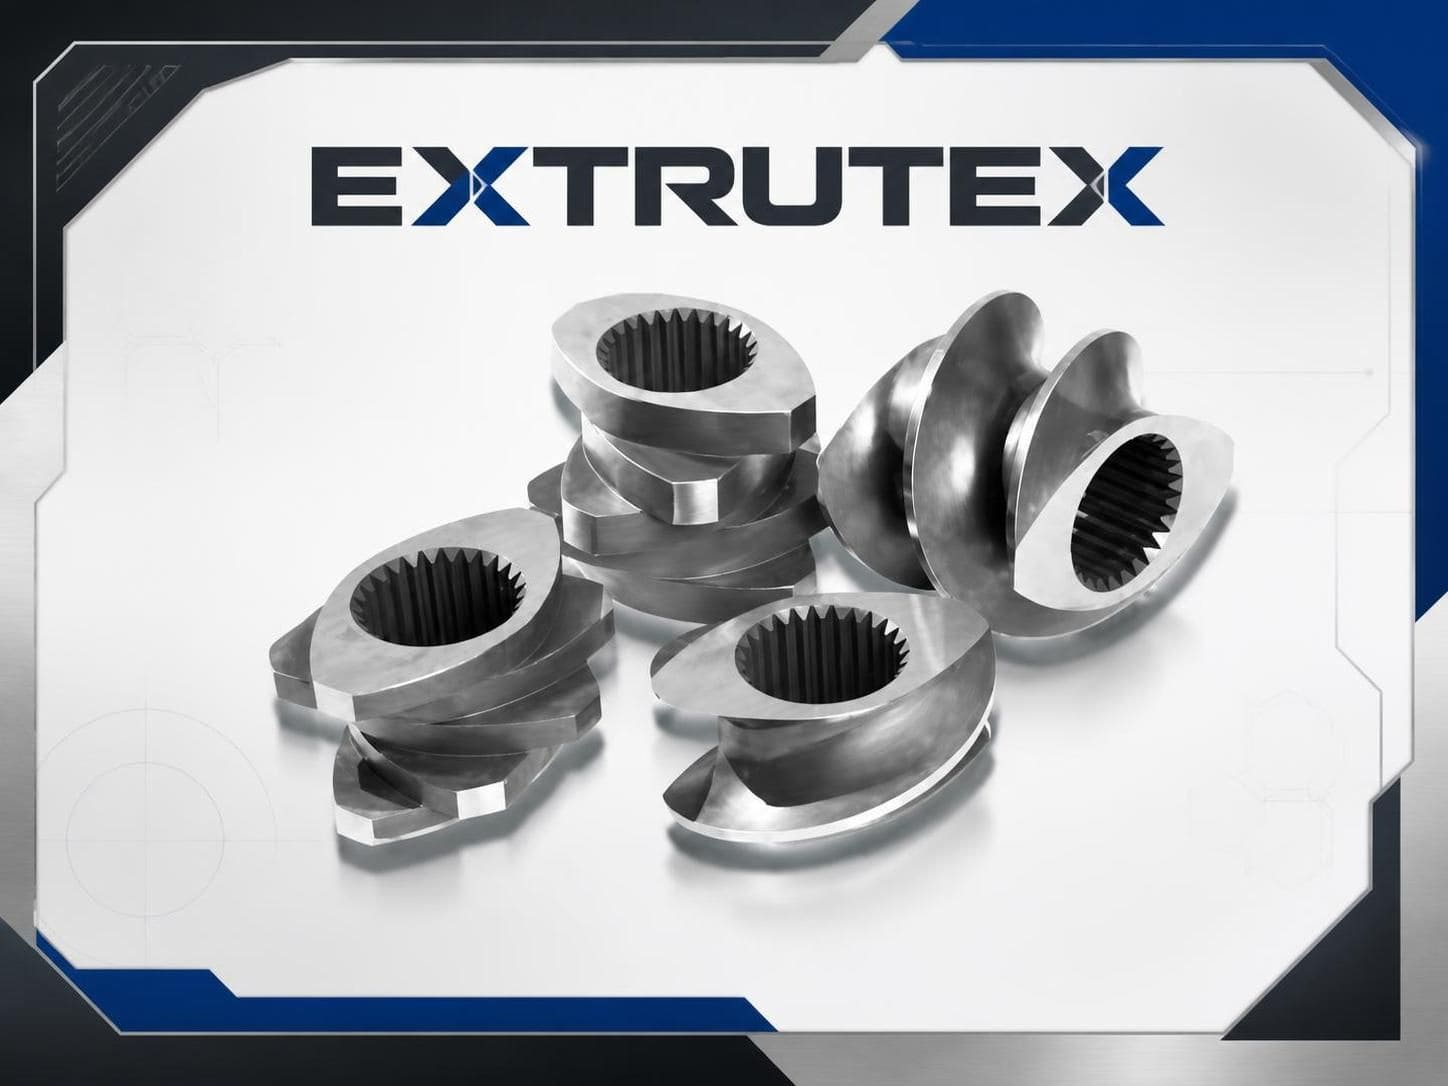
Screw Elements and Segments
Conveying elements and other screw segments manufactured to match the required outside diameter, pitch, profile, length and shaft connection. Component geometry is confirmed against the original part or approved technical information.
Kneading Blocks
Single-piece and assembled kneading blocks for mixing, working and processing sections. Stagger angle, block width, outside diameter and assembly orientation must be checked against the original configuration.
Screw Shafts and Assemblies
Replacement screw shafts and shaft assemblies manufactured according to verified dimensions, spline or keyway details, torque requirements and machine configuration.
Barrel Sections and Wear Liners
Replacement barrel sections, internal wear liners and liner replacement components. Material and surface treatment are selected according to the barrel position, process conditions and wear requirements.
Barrel Liners: Why They Must Be Checked Alongside Screw Elements
On abrasive feed and aquafeed applications, barrel liners can reach their wear limit before the screw elements. This is particularly important where the barrel experiences sustained contact with abrasive ingredients and operates under demanding pressure and temperature conditions.
A barrel liner is a replaceable wear component in configurations designed with a liner. Its purpose is to provide a suitable internal working surface and help protect the main barrel structure. The liner material and construction must be appropriate for the process and the mechanical design of the barrel.
What happens when a new screw set is installed in a worn barrel?
If the barrel bore is already oversized or out of round, installing new screw elements alone may not restore the intended operating clearance. The new components may operate with excessive clearance, reducing the expected benefit of replacement and potentially accelerating further wear.
Before ordering replacement parts, inspect both sides of the screw-and-barrel working pair:
- Measure the screw flight crest diameter.
- Measure the barrel bore at relevant positions.
- Check barrel roundness and local wear patterns.
- Inspect liner thickness and surface condition, where applicable.
- Compare measurements with the original drawings or verified service limits.
If both the screw elements and liner are worn, a matched replacement plan can help restore the intended geometry more effectively than replacing individual components without checking the complete assembly.
Material Selection for Feed and Aquafeed Applications
The correct material depends on the recipe, component position, temperature, moisture, cleaning procedure and expected wear mechanism. A material suitable for one feed formulation may not be the best choice for another.
| Application or Position |
Material and Surface Options |
| General product-contact duty |
Suitable 300-series stainless steel grades, with material condition selected for the application |
| Abrasive product-contact duty |
Selected corrosion-resistant wear grades, with hardness potentially in the 58–62 HRC range where the grade and heat treatment permit |
| Non-product-contact positions |
Nitrided steel or suitable tool steel, subject to component design and operating conditions |
| Barrel bore |
Polished or plated bore, depending on the original construction and engineering requirements |
| Barrel liner |
Nitrided steel, alpha-101, HIP PM materials or nickel-based tungsten-carbide laser-clad options, subject to suitability and verification |
Corrosion-resistant wear grades
For abrasive recipes containing bone meal, mineral premixes or other hard ingredients, a suitable corrosion-resistant wear grade may provide a better combination of hardness and corrosion resistance than a general-purpose stainless steel.
The 58–62 HRC range is an application-dependent option, not a universal specification for every stainless steel. The actual grade, heat treatment, corrosion performance and achievable hardness must be confirmed before production.
300-series stainless steel
Suitable 300-series stainless steel grades can be considered for general product-contact applications where corrosion resistance, cleanability and process compatibility are important. They should not automatically be treated as equivalent to hardened wear-resistant grades.
Barrel bore and liner treatments
Depending on the original barrel design, available solutions may include polished or plated bores, nitrided liners, alpha-101 materials, HIP powder metallurgy materials and laser-clad surfaces. Each solution has different characteristics and must be evaluated for the operating environment.
Food-contact documentation: Food-contact suitability must be confirmed for the actual material, manufacturing process and surface treatment. A material name or hardness value alone does not establish food-contact compliance. Coatings and liners also require application-specific qualification.
What Does Interchangeability Mean?
For replacement screw elements to work correctly, they must reproduce the relevant mechanical and geometric features of the original components. A part that looks similar is not necessarily interchangeable.
EXTRUTEX checks the dimensional details required for the intended installation and operating position. Depending on the component, these may include:
- Spline and keyway: The shaft connection must match the original shaft geometry.
- Outside diameter: Screw element diameter must correspond to the required screw and barrel configuration.
- Pitch and flight geometry: Conveying geometry must match the required process position.
- Centre distance: The twin-screw configuration must maintain the correct relationship between the two screw axes.
- Kneading block stagger angles: Block orientation and assembly geometry must be verified.
- Component length: Element length and overall screw assembly dimensions must be checked.
Mixing replacement components with original parts
Replacement elements may be installed alongside original components on the same shaft when the relevant dimensions, geometry, material requirements and assembly sequence have been verified. This should not be assumed from the machine brand or visual similarity alone.
For a reliable replacement, EXTRUTEX checks the supplied drawing, original component or measured sample before confirming the manufacturing specification.
Dimensional Inspection and Quality Documentation
Replacement components for industrial twin-screw extruders must meet the dimensional requirements of the original assembly. EXTRUTEX uses dimensional inspection to verify critical features before parts are released.
- CMM dimensional inspection: Critical dimensions and geometric features are checked against the approved manufacturing information.
- Batch inspection report: A CMM report is available per batch.
- Material documentation: EN 10204 3.1 material certificates can be supplied on request.
- Hardness verification: Hardness records can be provided where a specified heat treatment or wear grade requires them.
- Surface inspection: Components can be checked for visible machining and surface defects.
- Photographic records: Inspection photographs can be supplied to support incoming maintenance checks.
Inspection requirements should be agreed before production, particularly for components with special material, heat-treatment, coating or food-contact requirements.
Manufacturing from Drawings or Worn Samples
Original drawings are useful, but they are not always available for older machines or components that have been modified during previous maintenance. EXTRUTEX can assess replacement requirements using drawings, original parts, worn samples and available machine measurements.
When drawings are available
We review the component dimensions, tolerances, material specifications, shaft connection and assembly position. Any unclear or conflicting details are confirmed before machining begins.
When only a worn sample is available
A worn component can provide useful reference information, but its original geometry may have changed through service. Where possible, provide an unworn section, a drawing, a reference component or measurements from a matching position on another screw assembly.
If the sample is severely worn, we may need additional information before reconstructing its original geometry. Manufacturing should not proceed on the assumption that the worn dimensions represent the original design.
How to Request Andritz Replacement Parts
To identify the correct replacement components, please provide as much of the following information as possible:
-
Machine nameplate photograph
Send a clear photograph showing the machine manufacturer, model, type and serial information. This is the first information we request for Andritz enquiries.
-
Component position
Identify the position of the worn screw element or kneading block. A photograph of the complete screw assembly is useful.
-
Worn component photograph
Photograph the component with a ruler or measuring scale in the frame. Include the OEM part number if it is available and legible.
-
Barrel measurements
If barrel wear is suspected, provide the measured bore diameter and roundness results, together with the measurement positions where available.
-
Process information
Tell us whether the equipment processes poultry feed, livestock feed, marine aquafeed, pet food or another formulation. Include relevant abrasive or corrosive recipe ingredients where possible.
Important: A machine nameplate photograph is particularly useful for Andritz enquiries because platform names and generations vary. We confirm the machine configuration before determining whether a replacement component can be manufactured.
Lead Time and Order Planning
The typical lead time for imported-machine replacement components is approximately 30–45 days after the required material is available and the component geometry has been confirmed. Transit time is additional.
Special stainless steel grades, non-stock liner materials, unusual surface treatments and complex machining requirements may extend the production schedule.
For planned maintenance, we recommend identifying worn screw elements and barrel liners before the scheduled shutdown. This allows time for measurement, material selection, manufacturing and inspection rather than relying on emergency replacement after a machine failure.
| Order Stage |
What Is Confirmed |
| Machine identification |
Nameplate, platform, generation and configuration |
| Technical review |
Drawings, measurements, component position and wear condition |
| Material confirmation |
Steel grade, heat treatment and surface requirements |
| Manufacturing |
Machining and component production to the approved specification |
| Inspection |
Dimensional checks and agreed documentation |
| Dispatch |
Packaging and shipment after inspection and order release |
Why Choose EXTRUTEX for Andritz Extruder Parts?
- Replacement component manufacturing: Screw elements, kneading blocks, shafts, barrel sections and wear liners.
- Drawing and sample-based production: Components assessed against original technical information or measured samples.
- Material selection: Options for abrasive, corrosive and general product-contact applications.
- Dimensional inspection: CMM inspection reports available per batch.
- Small order quantities: Minimum order quantity of one piece.
- Technical assessment: Machine identification and component verification before manufacturing.
- Maintenance-focused supply: Individual parts or matched screw and barrel replacement components.
EXTRUTEX combines Austrian design, laboratory and R&D capabilities with manufacturing in China. Our focus is on practical replacement components for plastics, food and feed extrusion equipment.
EXTRUTEX is an independent replacement-parts manufacturer. Andritz is a third-party equipment manufacturer. References to Andritz identify equipment compatibility and do not imply affiliation, authorisation or endorsement.
Frequently Asked Questions
Which Andritz extruder platforms can EXTRUTEX supply parts for?
We assess replacement requirements for Andritz feed, aquafeed and food extrusion equipment. Platform names, machine configurations and generations vary, so we confirm the exact equipment from the machine nameplate rather than publish an unverified model list. Send us a photograph of the nameplate with your enquiry.
Why can Andritz aquafeed parts experience demanding wear conditions?
Aquafeed formulations can combine abrasive ingredients such as mineral premixes and bone meal with corrosive ingredients such as salt in marine diets. The process may also require sustained mechanical energy to achieve the specified product density and durability. The actual wear rate depends on formulation, operating conditions and material selection.
How do I know when an Andritz screw element needs replacing?
Possible warning signs include declining pellet durability, changing bulk density, altered aquafeed sinking behaviour, increasing specific mechanical energy and reduced throughput. These symptoms can also have process-related causes. Measure the screw flight crest and barrel bore during planned shutdowns to assess actual wear.
Do you supply barrel wear liners as well as screw elements?
Yes. EXTRUTEX supplies barrel sections, wear liners and liner replacement components alongside screw elements, kneading blocks and shafts. On abrasive feed duty, liners may reach their wear limit before the screw elements, so both should be inspected.
Can replacement screw elements be installed alongside original Andritz parts?
This may be possible when the shaft connection, outside diameter, pitch, stagger angles, component length and other relevant dimensions have been verified. Compatibility should be confirmed for the exact machine and assembly position before mixing replacement and original components.
Can EXTRUTEX manufacture parts without original drawings?
Yes, we can assess worn samples and measured components. However, a worn part may no longer represent its original geometry. Additional measurements, an unworn reference section or information from a matching assembly may be required before the manufacturing specification can be approved.
Which material is best for abrasive aquafeed applications?
The correct material depends on the ingredients, corrosion exposure, temperature and component position. Selected corrosion-resistant wear grades may be suitable for abrasive recipes. A hardness of 58–62 HRC is an option only where the specific material and heat treatment support it. It is not a universal specification for all stainless steel.
Can you supply food-contact materials and documentation?
Material options and documentation can be discussed according to the application. Food-contact suitability must be confirmed for the actual material, treatment and finished component. EN 10204 3.1 material certificates are available on request.
What is the minimum order quantity?
The minimum order quantity is one piece. We can assess individual screw elements, kneading blocks, shafts, barrel sections and wear liners, as well as larger matched replacement sets.
What lead time should I plan for?
Allow approximately 30–45 days after material availability and geometry confirmation, plus transit. Special grades and non-stock liner materials may require additional time. For this reason, we recommend planning replacement orders around scheduled maintenance shutdowns.
Request a Quotation for Andritz Extruder Parts
Send EXTRUTEX your Andritz machine nameplate photograph, component position, worn-part photographs and available drawings or measurements. Our team can review the machine configuration, assess the required replacement geometry and recommend suitable material options.
Whether you need individual screw elements, kneading blocks, screw shafts, barrel sections or complete wear-liner replacement, provide the available technical information so the requirements can be checked before manufacturing.
EXTRUTEX - Replacement Screw Elements, Barrels, Shafts and Wear Parts for Industrial Extrusion Equipment.



-
(0 customer reviews)