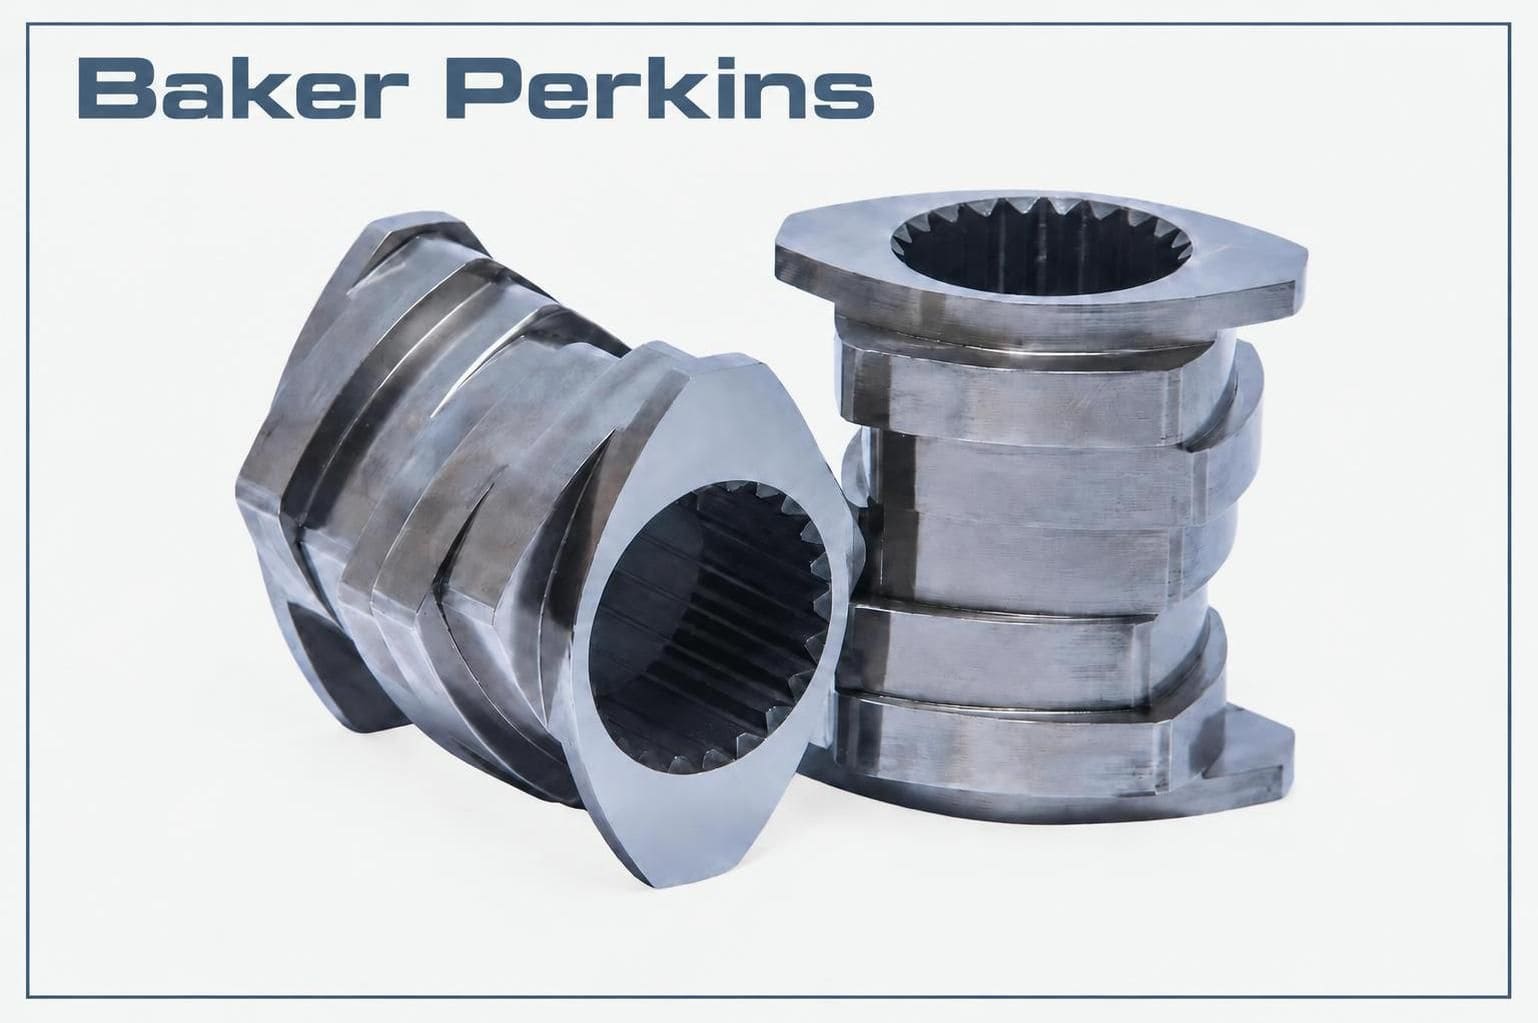
Baker Perkins Compatible Screw Elements for MPF and SBX Extruders
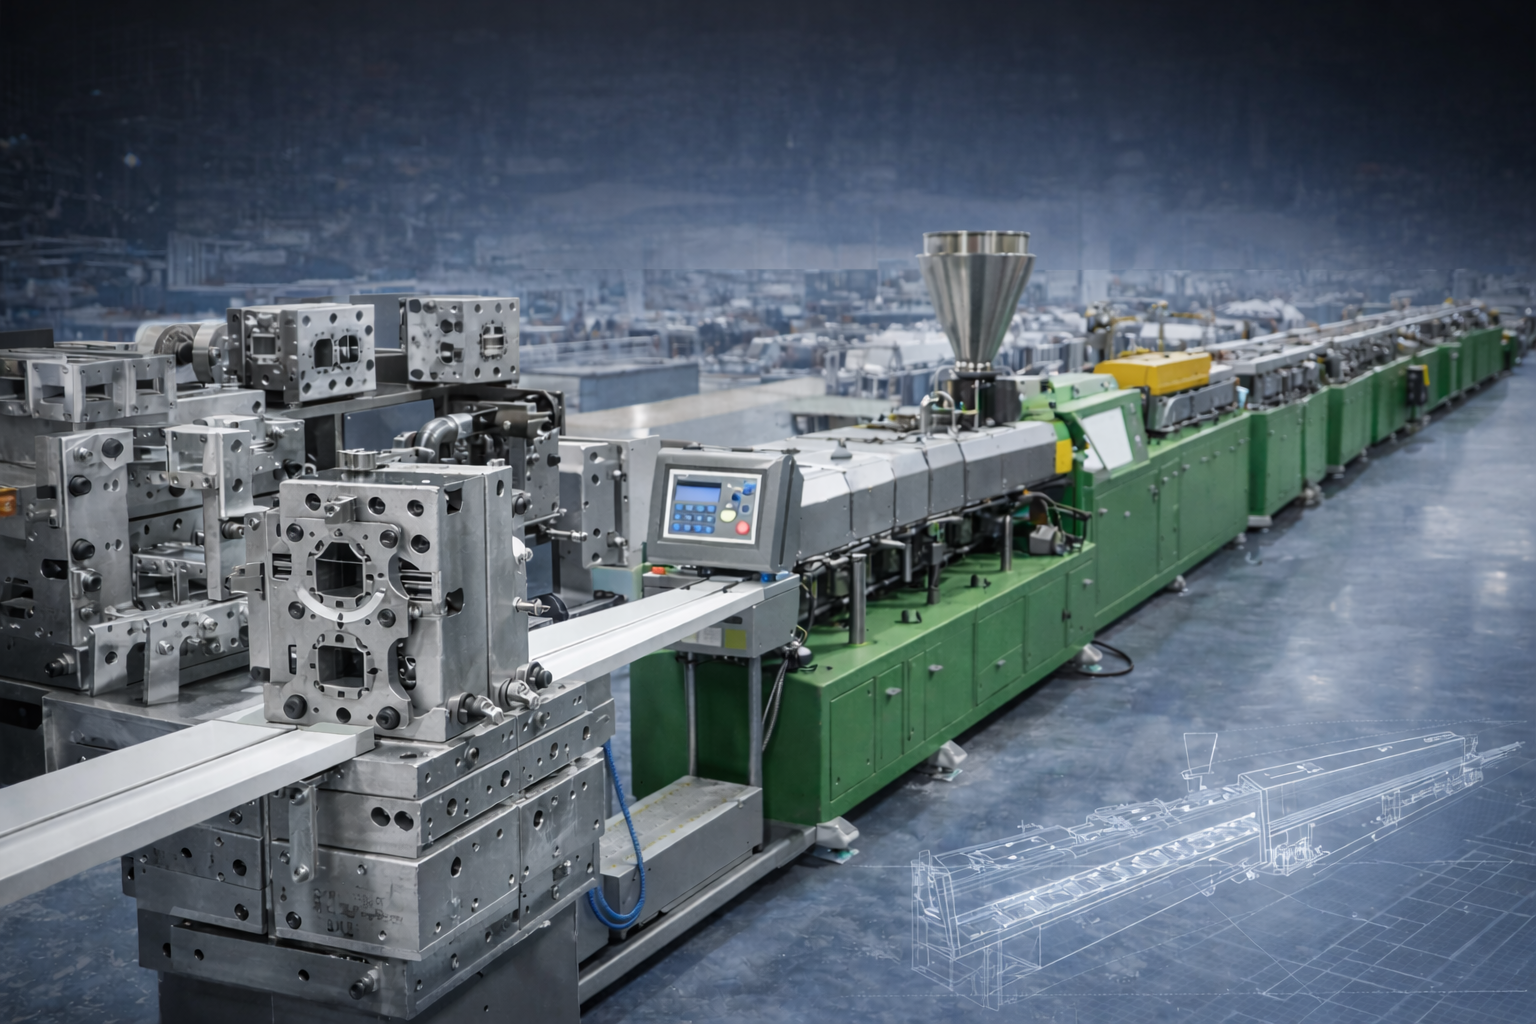
EXTRUTEX manufactures replacement screw elements, kneading blocks, screw shafts, barrel sections and wear liners for Baker Perkins MPF and SBX twin-screw extruders. These components are intended for food-processing applications including breakfast cereals, snacks and confectionery production.
We manufacture individual replacement parts and complete screw assemblies according to available OEM drawings or dimensions taken from an existing component. When original drawings are unavailable, our engineering team can assess a physical sample, measure its critical features and reconstruct the required geometry, provided sufficient reference information remains.
Food extrusion places particular demands on screw elements and barrel components. Material selection, surface condition, component clearances and cleanability all influence the suitability of a replacement part. The correct replacement must reproduce the required machine dimensions while meeting the material and finish requirements of the specific production process.
Replacement parts for Baker Perkins MPF and SBX platforms.
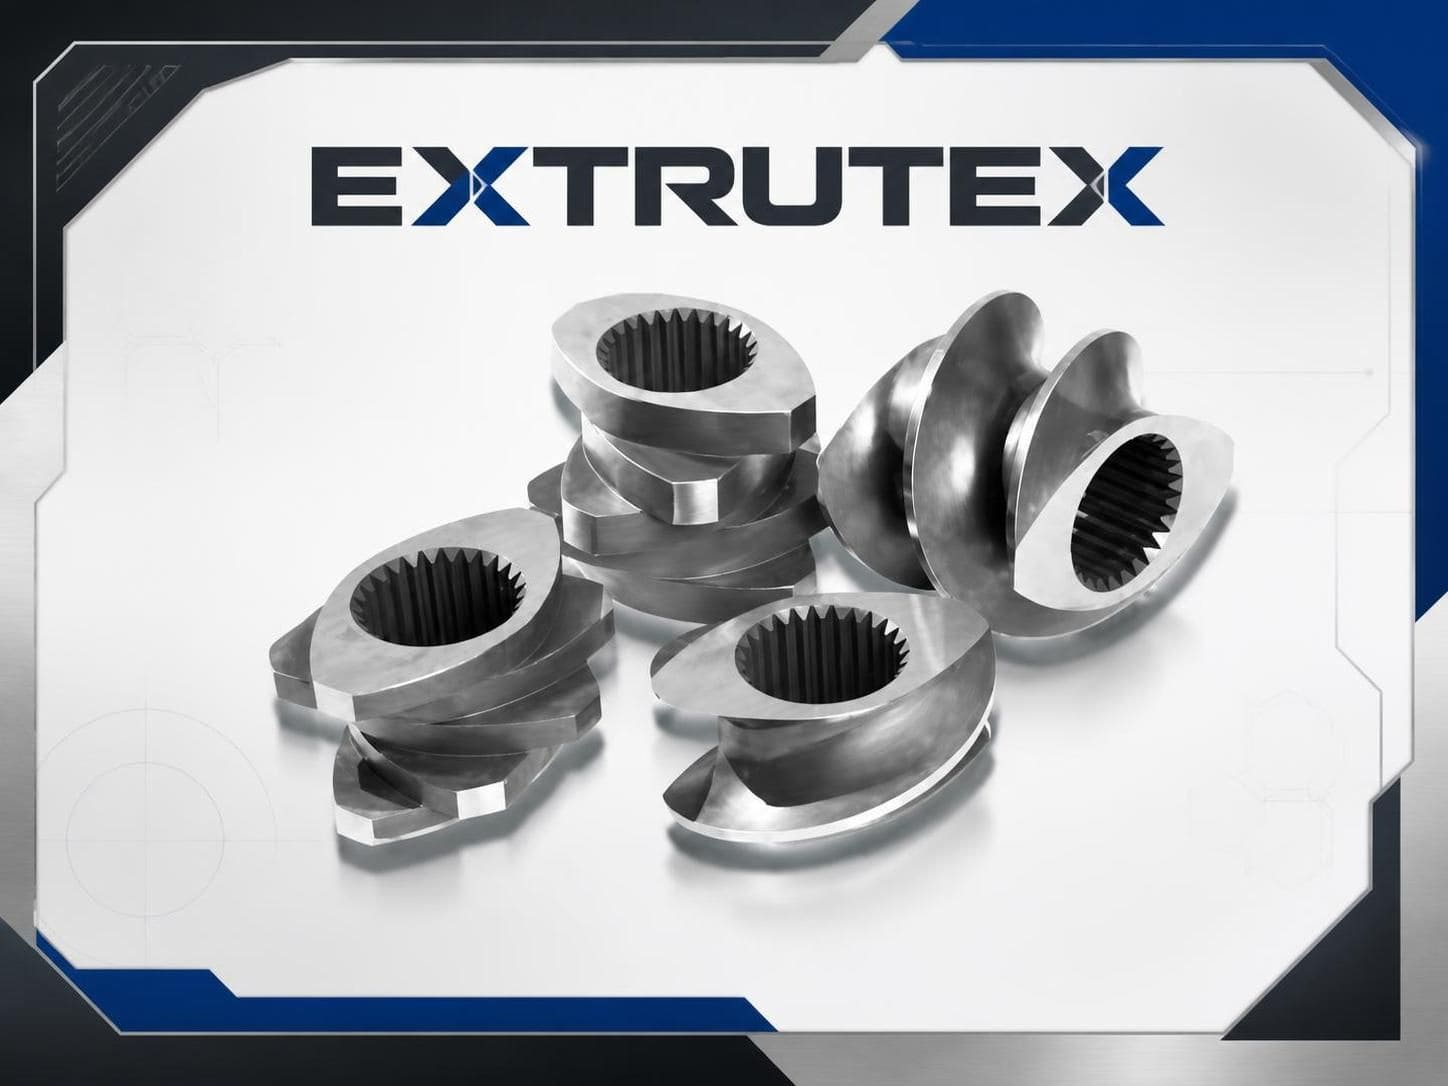
EXTRUTEX can manufacture conveying elements, kneading blocks, shafts, barrel sections and wear liners individually or as matched assemblies. Replacement scope can be limited to the worn positions rather than automatically requiring a complete screw set.
Technical Specifications
| Technical Data |
Specification |
| Compatible platforms |
Baker Perkins MPF and SBX twin-screw extruders |
| Applications |
Breakfast cereals, snacks and confectionery production |
| Components |
Screw elements, kneading blocks, screw shafts, barrel sections and wear liners |
| Interchangeability |
Manufactured to confirmed OEM dimensions and geometry |
| Base materials |
300-series stainless steel, nitrided or through-hardened materials, according to application |
| Abrasive product duty |
Corrosion-resistant wear-grade material; 58–62 HRC for suitable grades and specified applications |
| Dimensional verification |
CMM inspection report per batch |
| Minimum order |
1 piece |
| Documentation |
EN 10204 3.1 material certificate on request |
| Imported-machine spares |
Typically 30–45 days after material availability and drawing confirmation, plus transit |
| Chinese standard-machine spares |
Ex stock, immediate dispatch where stock is available |
The 30–45-day lead time applies to imported-machine spare parts once material is available and the manufacturing drawings or dimensions are confirmed. Special stainless-steel grades, specified surface finishes and materials not held in stock may require additional preparation time. Transit time is additional.
Baker Perkins MPF and SBX Replacement Components
The screw assembly is central to the operation of a twin-screw food extruder. Each element contributes to conveying, mixing, cooking, pressure development or product forming. A replacement component must therefore match its intended position and function within the complete screw configuration.
1. Conveying Screw Elements
Conveying elements move the product through the extruder and help control material transport, filling behaviour and residence time. Their geometry influences the movement of the food material through the different processing zones.
EXTRUTEX manufactures replacement conveying elements for Baker Perkins MPF and SBX platforms according to the confirmed dimensions and configuration of the original parts.
- Single-flight and double-flight conveying elements, where specified by the original design.
- Replacement screw segments for individual worn positions.
- Elements manufactured to the required outside diameter and pitch.
- Components made from approved drawings or verified physical samples.
- Individual elements or matched groups for planned maintenance.
2. Kneading Blocks
Kneading blocks are used in mixing and cooking zones to influence mechanical energy input, material distribution and product development. Their geometry and angular arrangement determine how the material is worked as it passes through the processing section.
A replacement kneading block must reproduce the original dimensions and stagger arrangement. An incorrect angle or block length can change the processing behaviour and affect the balance between conveying and mixing.
- Single-piece kneading blocks.
- Assembled kneading-block configurations.
- Replacement blocks for worn cooking and mixing zones.
- Custom-manufactured blocks based on drawings or measured samples.
3. Screw Shafts and Shaft Assemblies
Screw shafts transmit torque from the drive system to the screw elements. Their connection geometry, length, diameter and mechanical properties must match the machine configuration.
Spline or keyway wear can affect the fit between the shaft and the installed elements. If the shaft connection is damaged, replacing the screw elements alone may not restore the required assembly condition.
EXTRUTEX manufactures replacement screw shafts and shaft assemblies according to the confirmed engineering requirements. The shaft specification is assessed separately from product-contact screw-element material requirements.
- Replacement screw shafts.
- Splined or keyed shaft configurations, as required.
- Individual shafts and shaft assemblies.
- Precision-machined connections and component interfaces.
4. Barrel Sections and Wear Liners
The barrel forms the processing chamber around the screw assembly. Its internal bore geometry, centre distance, section length and connection arrangement must correspond to the original machine specification.
EXTRUTEX manufactures replacement barrel sections and wear liners for compatible MPF and SBX configurations. The correct construction depends on the original barrel design and the operating conditions of the production line.
- Replacement twin-screw barrel sections.
- Figure-eight bore configurations.
- Wear liners and liner replacement components.
- Polished or plated barrel bores, where specified.
- Nitrided, alpha-101, HIP PM or laser-clad liner options, subject to application and material verification.
Why Food Extrusion Wears Screw Elements Differently
Food extrusion is not simply polymer compounding with a different recipe. The processing objective is different, and the materials, surface finish and clearances must be selected accordingly.
Depending on the product and process, food extrusion may involve moisture levels around 15–30%. The extruder is expected to cook, texturise, mix and convey the product to a specified processing condition. It is not simply trying to disperse ingredients to a target fineness.
Product-contact components must also be suitable for the intended food-processing environment, including cleaning procedures and the required surface condition. Material selection and geometry therefore need to consider both operating performance and cleanability.
1. Abrasive Wear
Flour, bran and mineral-containing ingredients can contribute to abrasive wear. The effect depends on particle characteristics, concentration, moisture and operating conditions.
As the screw flight crest and barrel bore wear, the working clearance can increase. This may change conveying behaviour and reduce the ability of the original screw configuration to maintain consistent processing conditions.
2. Corrosion and Surface Pitting
Salt and acidic inclusions can create corrosive conditions in certain recipes. Surface pitting may develop before substantial dimensional wear becomes visible.
The correct stainless-steel grade and surface condition depend on the actual ingredients, operating temperature and cleaning chemicals. General stainless-steel identification alone is not enough to establish suitability for every food-processing environment.
3. Washdown and Cleaning Conditions
Cleaning and washdown can affect component surfaces, especially where the geometry contains narrow gaps, crevices or areas that are difficult to access. A replacement part should preserve the required surface finish and avoid introducing unnecessary locations where product residue can accumulate.
The required finish should be defined according to the machine design, hygiene requirements and cleaning procedure. A polished surface may be appropriate in one application, while another position may require a different specified treatment.
Clearance growth can affect product quality before a part fails mechanically.
A change in screw-to-barrel clearance can influence conveying behaviour, processing consistency and energy input. Product changes should be assessed together with screw wear, barrel condition, feed rate, moisture and operating temperature.
What Interchangeable Actually Means
A dimensionally interchangeable screw element must match the mechanical connection and relevant geometry of the original component. Similar appearance or a matching outside diameter is not sufficient to establish interchangeability.
EXTRUTEX works from OEM drawings where they are available and measured samples where they are not. Critical dimensions are checked against the agreed reference before production.
| Inspection Point |
Compatibility Requirement |
| Spline and keyway |
Correct connection profile, dimensions and shaft fit. |
| Outside diameter |
Matches the required element diameter and barrel clearance. |
| Pitch |
Reproduces the required conveying geometry. |
| Element length |
Matches the axial dimension and assembly position. |
| Stagger angle |
Matches the required angular arrangement of kneading or mixing elements. |
| Centre distance |
Corresponds to the two screw axes and barrel bore configuration. |
| Flight profile |
Reproduces the relevant original geometry. |
When these dimensions and the assembly arrangement are verified, replacement elements can be manufactured for use alongside original components on the same shaft. Mixed assemblies should always be checked against the intended screw sequence and machine configuration.
Materials for Baker Perkins Food-Contact Components
Material selection follows the processing duty rather than the machine brand alone. A confectionery line and a cereal line using abrasive mineral premixes may require different material properties, even when the same extruder platform is involved.
The material must be selected according to the component position, product ingredients, temperature, wear mechanism, cleaning conditions and applicable food-contact requirements.
| Material Selection |
Application and Considerations |
| Product contact, general food duty |
300-series stainless steel, with any hardening or surface treatment selected according to the specific grade and application. |
| Product contact, abrasive recipe |
Suitable corrosion-resistant wear-grade material. A 58–62 HRC target may be specified for compatible grades and verified heat-treatment conditions. |
| Non-contact positions |
Nitrided steel or tool steel according to the mechanical and wear requirements. |
| Barrel bore |
Polished or plated bore, depending on the original construction and required finish. |
| Wear liners |
Nitrided, alpha-101, HIP PM or laser-clad options, subject to dimensional and application requirements. |
300-Series Stainless Steel
300-series stainless steels are widely used in food-processing equipment because of their corrosion-resistance characteristics. The precise grade must be selected according to the ingredients, cleaning chemicals, temperature and mechanical loading.
For product-contact components, the required finish and cleanability are also important. The material designation alone does not establish compliance with every food-contact regulation or application requirement.
Hardened and Wear-Resistant Materials
Abrasive recipes can require improved resistance to mechanical wear. In some applications, a corrosion-resistant wear-grade material with a specified hardness range may be appropriate.
The 58–62 HRC range must be matched to a material capable of achieving the required hardness while retaining the necessary corrosion and mechanical properties. Not every stainless-steel grade can meet this combination of requirements.
Non-Contact Mechanical Components
Shafts and other non-product-contact mechanical components have different material requirements from product-contact screw elements. Their selection is based on torque transmission, mechanical loading, fatigue resistance, connection design and the required heat treatment.
Barrel Bore and Liner Options
The barrel bore must maintain the specified geometry and working clearance around the screw assembly. Depending on the original construction, replacement options may include polished or plated bores and different liner materials or surface treatments.
Nitrided, alpha-101, HIP PM and laser-clad options should be evaluated against the required wear performance, dimensions and product-contact suitability. A coating or liner should not be assumed suitable for food contact without confirming its specific material and compliance documentation.
Dimensional Inspection and Documentation
EXTRUTEX checks replacement components against the agreed engineering reference. Dimensional inspection helps verify the features that determine assembly fit and the geometry of the finished component.
Available Quality Records
- CMM dimensional report: Coordinate measurement results for agreed critical dimensions.
- EN 10204 3.1 material certificate: Available on request.
- Hardness records: For applicable materials and heat-treatment processes.
- Case-depth records: Where a specified surface-hardening process is used.
- Pre-shipment photographs: Photographs of the finished components before packing.
The inspection scope is agreed according to the component drawing and order requirements. If specific material certificates, dimensional reports, hardness tests or additional inspection records are required, these should be confirmed before production.
Individual Replacement Elements or Complete Screw Sets?
The correct replacement scope depends on the condition of the existing screw assembly. A complete set is not automatically necessary when only a few positions are worn.
Individual Screw Elements
When the shaft and the remaining elements are within the required dimensions, EXTRUTEX can manufacture individual replacement components for the affected positions. This can be suitable for planned maintenance where wear is concentrated in a limited section of the screw.
Matched Screw Element Sets
A matched set may be more appropriate when multiple processing zones show wear, several elements are outside tolerance or the screw configuration is being renewed as part of a major overhaul.
The replacement set is manufactured according to the confirmed machine configuration, assembly sequence and required dimensions.
Shaft and Barrel Inspection
If the shaft connection is worn or the barrel bore has developed excessive wear, replacing the screw elements alone may not restore the original operating clearance. The shaft, barrel and screw elements should be considered together when determining the replacement scope.
| Existing Condition |
Possible Replacement Scope |
| Only a few conveying elements are worn |
Individual conveying element replacement. |
| Kneading blocks in one processing zone are worn |
Replacement kneading blocks or a matched zone set. |
| Multiple screw positions are outside tolerance |
Matched screw element set. |
| Shaft connection is worn or damaged |
Shaft replacement assessment together with screw elements. |
| Barrel bore or liner is worn |
Barrel section or wear liner replacement assessment. |
Manufacturing Without Original Drawings
Some Baker Perkins spare-parts enquiries arrive with an existing worn component but no original drawing. In other cases, the part number is missing or the machine documentation is incomplete.
A physical sample can provide a basis for reverse engineering. EXTRUTEX measures the available component features and assesses whether the original geometry can be reconstructed accurately.
Our Measurement Process
- Machine identification: Review the nameplate and identify the MPF or SBX platform and available size information.
- Position identification: Establish the location of the worn component in the screw assembly.
- Sample measurement: Measure the outside diameter, element length, shaft connection, pitch and other relevant dimensions.
- Wear assessment: Determine which areas remain suitable as dimensional references.
- Geometry reconstruction: Use drawings, unworn sections or additional reference components to establish the original profile.
- Production confirmation: Confirm the required dimensions, material and finish before machining.
If the sample is too worn to establish the original geometry, we may request a section drawing, another sample or photographs of the same position from a sister machine. This avoids relying on assumptions when reconstructing critical dimensions.
Sample-based manufacturing requires sufficient reference information.
A worn part can be measured, but severe wear may have changed the original profile. Additional reference information is necessary when the original dimensions cannot be established reliably from the sample alone.
How to Request a Baker Perkins Spare Parts Quotation
Most enquiries can begin with three basic items. An original drawing is useful but not essential for the initial assessment.
Information to Send EXTRUTEX
- Machine nameplate photograph: A clear photograph showing the MPF or SBX platform and available machine identification details.
- Element position: Identify the worn position on the shaft or provide a photograph of the complete screw assembly.
- Worn component photograph: Photograph the part with a ruler or measuring scale in the frame.
- OEM part number: Include the original number if it is visible or available.
- Application details: Explain whether the line processes cereals, snacks, confectionery or another food product.
- Quantity: Specify individual elements, several positions or a complete screw set.
For barrel sections and wear liners, additional information may be required, including bore diameter, centre distance, section length, mounting arrangement and connection dimensions.
Minimum order quantity: 1 piece.
EXTRUTEX accepts orders for individual components and complete matched assemblies. Send the available machine and component information so that the required dimensions and compatibility can be assessed before production.
Lead Time and Delivery
For imported-machine spare parts, the typical manufacturing lead time is 30–45 days after material availability and drawing confirmation. Transit time is additional.
The actual schedule depends on the material grade, component complexity, machining requirements, heat treatment, surface finish and inspection scope. Stainless-steel grades or specified finishes that are not held in stock may require additional preparation time.
For Chinese standard-machine spare parts, ex-stock availability and immediate dispatch may be possible. Availability must be confirmed for the exact component and quantity before an order is placed.
Why Choose EXTRUTEX for Baker Perkins Replacement Parts?
- MPF and SBX platform coverage: Replacement components for the specified Baker Perkins twin-screw extruder platforms.
- Individual components: Replace selected worn positions instead of automatically ordering a complete screw assembly.
- Complete matched sets: Manufacturing for planned overhauls and larger replacement requirements.
- Drawing-based production: Components manufactured according to confirmed engineering drawings and dimensions.
- Reverse engineering: Sample-based measurement and reconstruction when original drawings are unavailable, subject to sufficient reference information.
- Material options: Selection according to the processing duty and product-contact requirements.
- Dimensional inspection: CMM inspection reports available per batch.
- Low minimum order: Orders accepted from one piece.
EXTRUTEX is an independent manufacturer of replacement extruder components. Baker Perkins, MPF and SBX are referenced only to identify the compatible machine platforms. EXTRUTEX is not affiliated with, authorised by or endorsed by Baker Perkins.
Frequently Asked Questions
1. Do you manufacture screw elements for Baker Perkins MPF and SBX extruders?
Yes. EXTRUTEX manufactures replacement conveying elements, kneading blocks, screw shafts, barrel sections and wear liners for the Baker Perkins MPF and SBX platforms. Parts can be made from available drawings or dimensions taken from a suitable physical sample.
2. Can your Baker Perkins replacement elements be mixed with original parts on the same shaft?
They can be manufactured for mixed assemblies when the required dimensions and geometry have been verified. This includes the spline or keyway, outside diameter, pitch, element length and stagger angles. The assembly sequence and compatibility of each position should also be checked.
3. What material do you use for food-contact screw elements?
Material selection depends on the application. General food-processing duty may use suitable 300-series stainless steel. Abrasive recipes may require a corrosion-resistant wear-grade material with a specified hardness. The exact grade, heat treatment and surface finish must be confirmed for the intended product-contact application.
4. How long does a Baker Perkins screw element set take?
The typical manufacturing lead time for imported-machine spare parts is 30–45 days after material availability and drawing confirmation, plus transit time. Special stainless-steel grades and specified surface finishes may take longer if the material is not held in stock. Chinese standard-machine parts may be available ex stock for immediate dispatch, subject to stock confirmation.
5. What information do you need to quote a Baker Perkins element?
A photograph of the machine nameplate, the element position on the shaft and a photograph of the worn part with a ruler in frame are a useful starting point. An OEM part number or original drawing is also helpful where available.
6. Can you manufacture parts if the original Baker Perkins drawing is unavailable?
Yes. EXTRUTEX can measure a physical sample and reconstruct the required geometry when sufficient reference information remains. If the component is severely worn, an additional sample, drawing or reference from the same position on another machine may be required.
7. Do you supply individual kneading blocks?
Yes. Individual kneading blocks can be manufactured for confirmed MPF and SBX positions. The original dimensions and stagger arrangement must be established before production.
8. Can you supply complete screw shafts as well as elements?
Yes. EXTRUTEX manufactures replacement screw shafts and shaft assemblies according to the required dimensions, connection geometry and mechanical specification.
9. Can you manufacture barrel sections and wear liners?
Yes. Replacement barrel sections and wear liners can be manufactured according to the required bore geometry, centre distance, section length, connection details and material specification.
10. What inspection documents are available?
A dimensional inspection report is available for each shipment. On request, EXTRUTEX can provide EN 10204 3.1 material certificates, hardness results, case-depth records where applicable and CMM measurement documentation for the batch.
11. Can I order only one replacement screw element?
Yes. The minimum order quantity is one piece. Individual components can be manufactured when the required dimensions and machine compatibility have been confirmed.
12. Are MPF and SBX screw elements interchangeable with each other?
Not automatically. The exact machine configuration, shaft connection, element dimensions and processing arrangement must be checked. Send the machine nameplate and component position so that compatibility can be assessed before production.
13. Can you manufacture screw elements for abrasive food recipes?
Yes. Material selection can be assessed for abrasive formulations containing ingredients such as mineral premixes or bone meal. The appropriate corrosion resistance, hardness, surface condition and product-contact suitability must be confirmed for the specific application.
14. Why can product quality change even when the screw elements are not broken?
Screw and barrel wear can gradually increase working clearances and change conveying and processing behaviour. This may affect product consistency, cooking performance and energy requirements before any component fails mechanically.
15. Are EXTRUTEX components original Baker Perkins parts?
No. EXTRUTEX manufactures independent replacement components for compatible Baker Perkins machine platforms. The parts are not represented as original Baker Perkins-manufactured components.
Request Baker Perkins MPF or SBX Replacement Parts
For replacement screw elements, kneading blocks, screw shafts, barrel sections or wear liners, send EXTRUTEX your machine nameplate photograph, component position and available measurements. Our engineering team can review the information, assess the required dimensions and confirm the manufacturing scope before production.
Whether you need one replacement element or a complete matched screw assembly, EXTRUTEX can assess the spare-parts requirements for your Baker Perkins MPF or SBX twin-screw extruder.


-
(0 customer reviews)