No products in the cart.
All rights of this website are reserved for EXTRUTEX Austria and its partner companies, © 2026
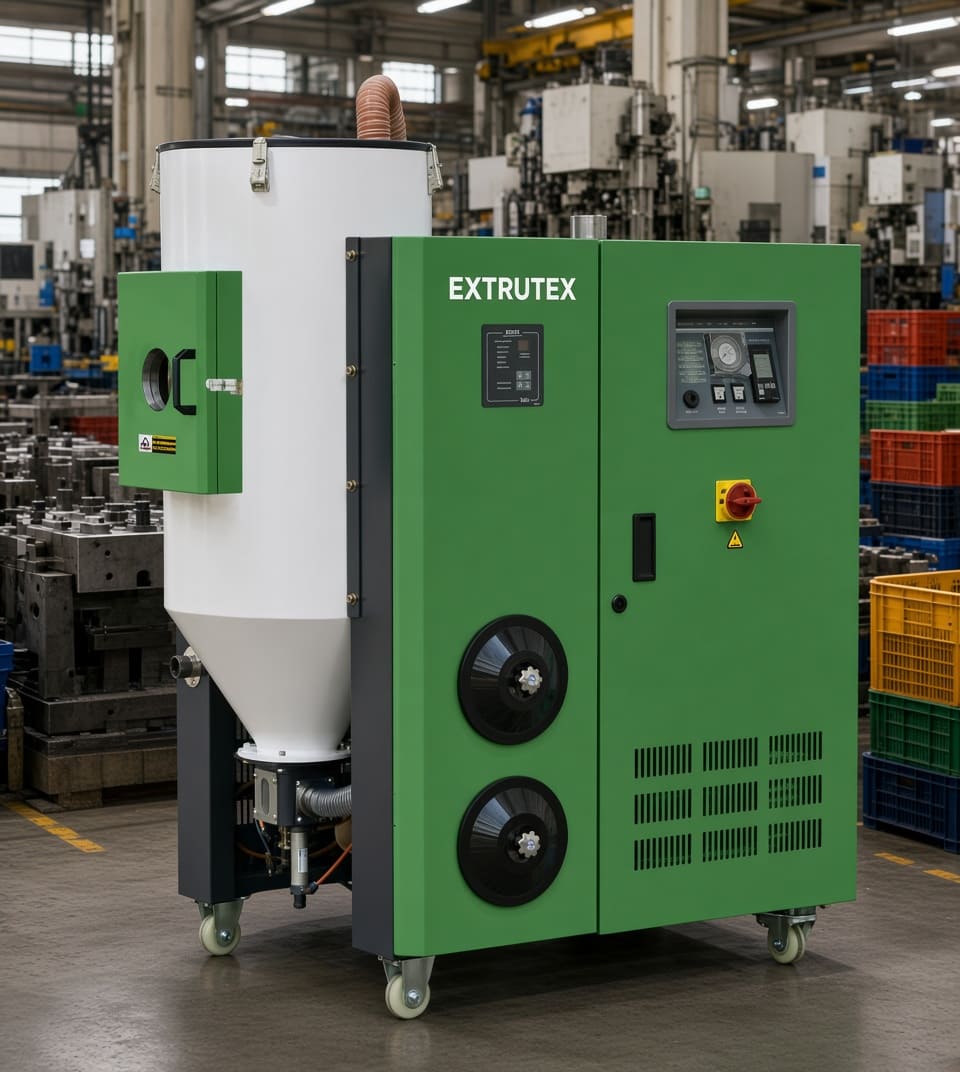
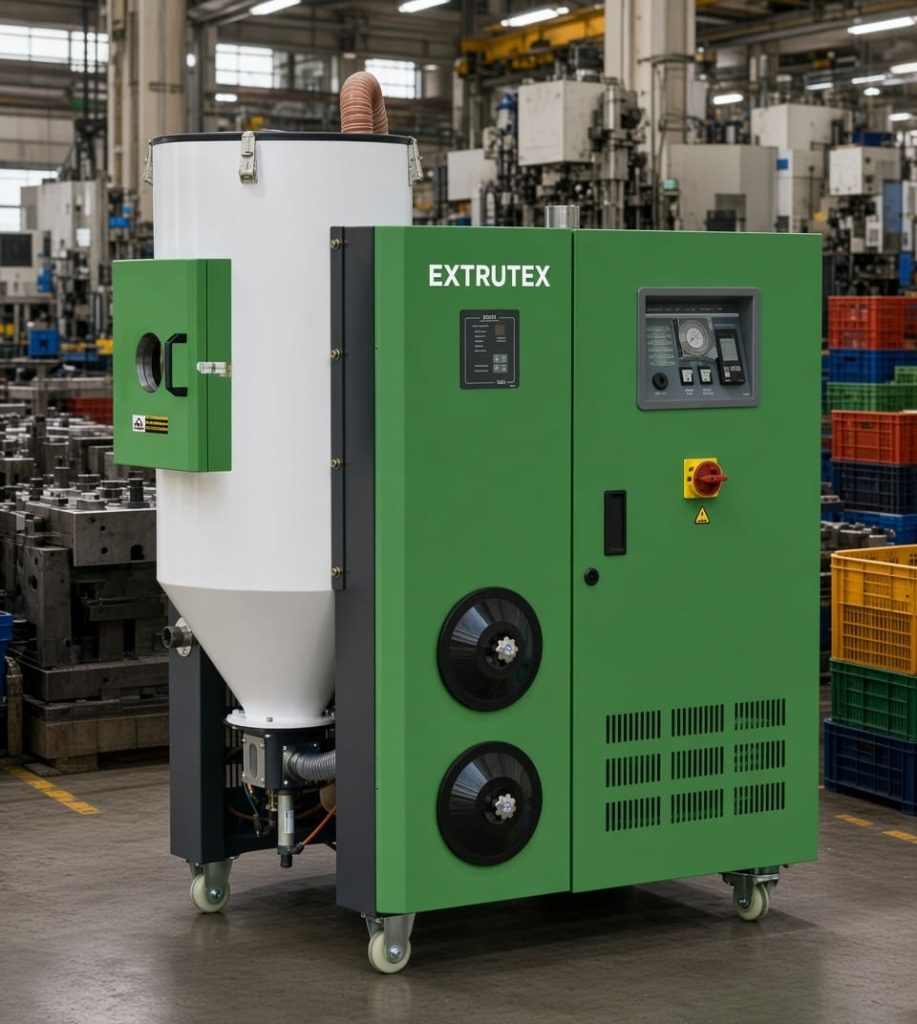
Combination of Drying, Dehumidifying and Conveying

Multiple Payment Methods

Discount for advance payments over 50%

Free Shipping Coordination Services
Payment methods:

Integrated three-in-one solutions engineered by EXTRUTEX for superior material preparation in plastics processing. Designed in Austria, precision-manufactured in Nanjing and Shanghai.
In the modern plastics processing industry, the quality of the final product begins long before the material enters the extruder or injection molding machine. Moisture content, temperature uniformity, and the integrity of the material transfer process are critical variables that determine whether a production run succeeds or fails. Contaminated or improperly dried resin can lead to surface defects, reduced mechanical properties, increased scrap rates, and costly downtime. Recognizing these challenges, EXTRUTEX has developed a sophisticated line of combination drying, dehumidifying and conveying systems that consolidate three essential functions into a single, highly efficient unit.
EXTRUTEX is a specialized manufacturer whose engineering philosophy originates in Austria—renowned for precision mechanical design, rigorous quality standards, and a deep understanding of European industrial requirements. Production takes place in advanced manufacturing facilities located in Nanjing and Shanghai, China. This dual-structure approach allows EXTRUTEX to combine Austrian design excellence with the cost efficiency, scale, and rapid production capabilities of modern Chinese industrial manufacturing. The result is equipment that meets international performance expectations while remaining competitively priced for global markets.
The EXTRUTEX combination systems are specifically engineered for processors who require reliable, closed-loop material handling. Whether the application involves hygroscopic engineering resins such as PET, PA, PC, or PBT, or standard materials that still benefit from controlled drying and contamination-free conveying, these units deliver consistent results. By integrating drying, dehumidifying, and multi-hopper conveying into one machine, EXTRUTEX eliminates the need for separate standalone dryers, dehumidifiers, and vacuum loaders, thereby reducing floor space, simplifying installation, and lowering overall energy consumption.
This comprehensive product overview explores the technical principles, performance characteristics, construction details, main components, and full technical specifications of the EXTRUTEX combination systems. It is intended for production managers, process engineers, purchasing specialists, and technical decision-makers who require detailed, factual information before specifying equipment for their facilities.
The core strength of the EXTRUTEX combination system lies in its carefully engineered performance features. Each characteristic has been developed to address real-world operational problems encountered in plastics processing plants. Below is a detailed examination of the six primary performance advantages that define the series.
The equipment combines drying, dehumidifying, and conveying into a single integrated unit. This architecture allows the system to dry the material to the required residual moisture level, maintain a stable low dew-point process air stream, and then convey the conditioned material to one, two, or three separate hoppers according to the customer’s production layout. The multi-hopper capability is especially valuable for multi-cavity or multi-material production cells where different machines or different zones of a single machine require simultaneous feeding of the same dried resin.
The dehumidification system is designed as a completely closed loop. Process air of low dew point never comes into contact with ambient plant air. This design prevents the re-introduction of moisture that would otherwise raise the dew point and compromise drying efficiency. Closed-loop operation also reduces the load on the regenerative heating elements, contributing to lower energy consumption and more stable long-term performance.
Just as the dehumidification air circuit is sealed, the material charging path is also fully enclosed. Once the resin has been dried, it remains isolated from ambient humidity during transfer. This prevents the dried material from re-absorbing moisture while traveling through the conveying lines—an especially critical consideration when the production environment has high relative humidity or when long conveying distances are required.
A dedicated material stop valve is installed on the charging device. This valve ensures that no residual material remains in the conveying pipeline after each transfer cycle. Residual material left in lines can absorb moisture, degrade thermally, or cause blockages. The stop-valve design guarantees clean, smooth, and consistent material delivery cycle after cycle.
The drying barrel features a double-layer heat-insulation construction. This barrier significantly reduces heat loss to the surrounding environment, improving thermal efficiency and lowering the energy required to maintain the set drying temperature. The insulation also contributes to a safer working environment by reducing the external surface temperature of the unit.
An advanced heat-dissipation system cools the process air to a lower temperature and correspondingly lower dew point. Efficient cooling of the return air improves the moisture-adsorption capacity of the desiccant, allowing the system to achieve and maintain lower dew points even under demanding production conditions.
Many conventional drying systems rely on open or semi-open circuits. In such designs, a portion of the process air is continuously exhausted and replaced by ambient air. While this approach can work in controlled environments, it becomes problematic when ambient humidity fluctuates or when the plant is located in a tropical or subtropical climate. The closed-loop philosophy adopted by EXTRUTEX removes ambient air as a variable. Once the system reaches steady state, the only moisture entering the circuit is the moisture released by the plastic pellets themselves. This results in more predictable drying performance, tighter process control, and reduced sensitivity to seasonal or daily weather changes.
Energy consumption is a major operating cost for any drying system. The double-layer insulated barrel reduces standby heat loss, while the high-efficiency cooler improves the thermodynamic efficiency of the dehumidification cycle. In addition, the ability to convey material to multiple hoppers from a single drying source eliminates the need for multiple independent dryers, each with its own heater, blower, and control system. The cumulative energy savings over a full production year can be substantial, particularly for facilities running continuous or multi-shift operations.
The physical arrangement of the EXTRUTEX combination system is the result of careful engineering aimed at compactness, accessibility, and process integrity. The unit is typically organized around a central drying and dehumidifying module, with the material conveying components arranged to minimize the length of the transfer lines while maintaining clear access for maintenance.
Material enters the system through the vacuum bunker or barrel hopper. From there it is drawn into the material suction box under vacuum created by the air pump. After passing through the material suction filter, the resin is directed into the drying barrel. Inside the barrel, heated process air of low dew point flows through the material bed, extracting moisture. The moisture-laden air then travels to the regeneration section, where the desiccant is periodically regenerated by the regeneration heating box and regeneration blower fan. Cooled, dried air is returned to the drying circuit via the cooler and drying filter. Simultaneously, dried material can be conveyed from the drying barrel to one or more remote hoppers through the closed charging system equipped with the material stop valve.
Understanding the role of each major component helps operators and maintenance teams keep the system performing at its design capacity. The following list corresponds to the construction layout diagram and provides a clear description of every numbered part.
Each of these components is selected and dimensioned according to the specific model size. Larger capacity models naturally employ higher-powered blowers, larger-diameter pipes, and more robust heating elements, while the fundamental process architecture remains consistent across the entire range.
The EXTRUTEX combination series is offered in a wide range of sizes to match different production volumes and material throughputs. The table below presents the complete technical data for all standard models. Capacities are given in liters for the drying barrel, with corresponding dry blower airflow, heating powers, pipe diameters, electrical requirements, and overall dimensions.
| Model | Capacity | Dry Blower (m³/h) |
Power of Dry Heater |
Power of Dry Blower |
Power of Reg. Blower |
Power of Air Pump |
Power of Reg. Heater |
Pipe Diameter |
Input Voltage |
Dimensions L×W×H (mm) |
|---|---|---|---|---|---|---|---|---|---|---|
| SLH-40L/60 | 40 L | 60 | 3 kW | 0.55 kW | 0.37 kW | 0.75 kW | 3 kW | 38 mm | 380 V / 50 Hz | 700 × 1200 × 1215 |
| SLH-80L/60 | 80 L | 60 | 4.5 kW | 0.75 kW | 0.37 kW | 1.1 kW | 4.5 kW | 38 mm | 380 V / 50 Hz | 700 × 1200 × 1215 |
| SLH-120L/100 | 120 L | 100 | 6 kW | 0.75 kW | 0.37 kW | 1.1 kW | 6 kW | 38 mm | 380 V / 50 Hz | 700 × 1200 × 1215 |
| SLH-160L/100 | 160 L | 100 | 7.5 kW | 0.75 kW | 0.55 kW | 1.1 kW | 6 kW | 38 mm | 380 V / 50 Hz | 800 × 1350 × 1300 |
| SLH-230L/120 | 230 L | 120 | 9 kW | 0.75 kW | 0.55 kW | 1.1 kW | 6 kW | 38 mm | 380 V / 50 Hz | 800 × 1350 × 1300 |
| SLH-300L/150 | 300 L | 150 | 12 kW | 1.1 kW | 0.75 kW | 1.5 kW | 7.5 kW | 51 mm | 380 V / 50 Hz | 900 × 1500 × 1450 |
| SLH-380L/200 | 380 L | 200 | 15 kW | 1.1 kW | 0.75 kW | 1.5 kW | 7.5 kW | 51 mm | 380 V / 50 Hz | 900 × 1500 × 1450 |
| SLH-460L/300 | 460 L | 200 | 15 kW | 1.1 kW | 0.75 kW | 1.5 kW | 9 kW | 51 mm | 380 V / 50 Hz | 1100 × 1650 × 1550 |
| SLH-600L/400 | 600 L | 400 | 18 kW | 1.5 kW | 1.1 kW | 1.5 kW | 9 kW | 51 mm | 380 V / 50 Hz | 1100 × 1650 × 1550 |
| SLH-800L/500 | 800 L | 500 | 21 kW | 1.5 kW | 1.1 kW | 2.2 kW | 9 kW | 51 mm | 380 V / 50 Hz | 1750 × 1900 × 1900 |
| SLH-1000L/700 | 1000 L | 700 | 24 kW | 2.2 kW | 1.5 kW | 2.2 kW | 12 kW | 51 mm | 380 V / 50 Hz | 1750 × 1900 × 1900 |
| SLH-1200L/700 | 1200 L | 700 | 30 kW | 2.2 kW | 1.5 kW | 2.2 kW | 12 kW | 51 mm | 380 V / 50 Hz | 1800 × 2200 × 2100 |
Notes on the specification table:
EXTRUTEX combination drying, dehumidifying and conveying systems are primarily designed for the plastics processing industry. Typical applications include:
Floor-space reduction – By combining three functions into one machine, plants free up valuable production area that would otherwise be occupied by separate dryers, loaders, and dehumidifiers.
Simplified installation and commissioning – Fewer interconnecting pipes, fewer electrical connections, and a single control interface reduce installation time and the potential for wiring or piping errors.
Improved process consistency – Closed-loop drying and closed conveying paths remove ambient humidity as a process variable, leading to more repeatable residual moisture levels and fewer quality fluctuations.
Lower energy consumption – Insulated barrels, efficient coolers, and the elimination of redundant heating and blower systems contribute to measurable reductions in electricity usage.
Reduced material degradation risk – Residue-free conveying lines and the absence of stagnant material pockets minimize thermal history and the risk of yellowing or property loss in sensitive resins.
Flexible multi-hopper feeding – The ability to supply up to three hoppers from one unit supports complex production cells without requiring multiple independent drying systems.
Model selection should begin with an accurate assessment of the required material throughput (kg/h) and the bulk density of the resin. The drying barrel volume is then chosen so that the residence time at the target temperature is sufficient to reach the desired residual moisture. Airflow (dry blower capacity) must be adequate to fluidize or penetrate the material bed effectively. Finally, the conveying distance and the number of destination hoppers influence the sizing of the air pump and the diameter of the conveying lines. EXTRUTEX technical support can assist with detailed calculations based on specific material data sheets and plant layouts.
Austria Design · Manufacturing in Nanjing & Shanghai
EXTRUTEX combines the engineering discipline and quality expectations of Austrian industrial design with the manufacturing scale and cost efficiency of modern Chinese production facilities located in Nanjing and Shanghai. This structure enables the company to deliver equipment that meets international performance standards while remaining accessible to a broad range of processors worldwide.
Customers who specify EXTRUTEX combination systems benefit from a design philosophy that prioritizes closed-loop integrity, energy efficiency, and practical operability. The equipment is built to operate reliably under continuous production conditions, with components selected for durability and ease of maintenance. Documentation, spare-parts support, and technical assistance are structured to serve both domestic Chinese users and international export customers.
In an industry where small variations in residual moisture can translate into significant differences in product quality and scrap rates, the consistent performance delivered by a well-engineered closed-loop drying and conveying system represents a tangible competitive advantage. EXTRUTEX has engineered its combination series specifically to provide that advantage.
Contact EXTRUTEX to discuss your specific drying, dehumidifying, and conveying requirements. Our technical team can help you select the optimal model, configure multi-hopper layouts, and calculate expected energy and quality improvements for your application.
EXTRUTEX – Austria Design · Precision Manufacturing in Nanjing & Shanghai
This technical overview is based on standard product specifications. Exact performance depends on material type, inlet moisture, ambient conditions, and operating parameters. Always consult the latest official documentation and perform trials with your specific resin before final process qualification.
There are no reviews yet.
By submitting your email, you agree to our company’s terms and conditions.
We are not looking to sell; we are here to provide you with the best support and service.
Contact available 24/7
Please do not contact us for advertising or sales inquiries
All rights of this website are reserved for EXTRUTEX Austria and its partner companies, © 2026
-
(0 customer reviews)