No products in the cart.
All rights of this website are reserved for EXTRUTEX Austria and its partner companies, © 2026

Multiple Payment Methods

Discount for advance payments over 50%

Free Shipping Coordination Services
Payment methods:

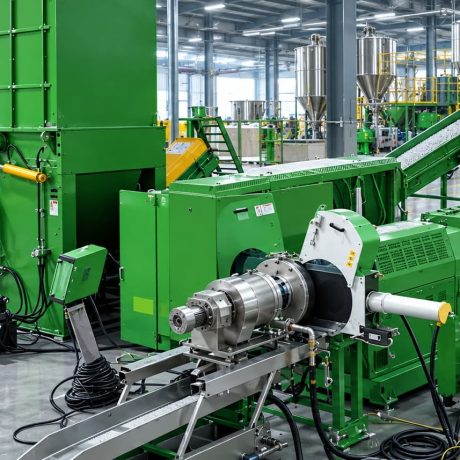
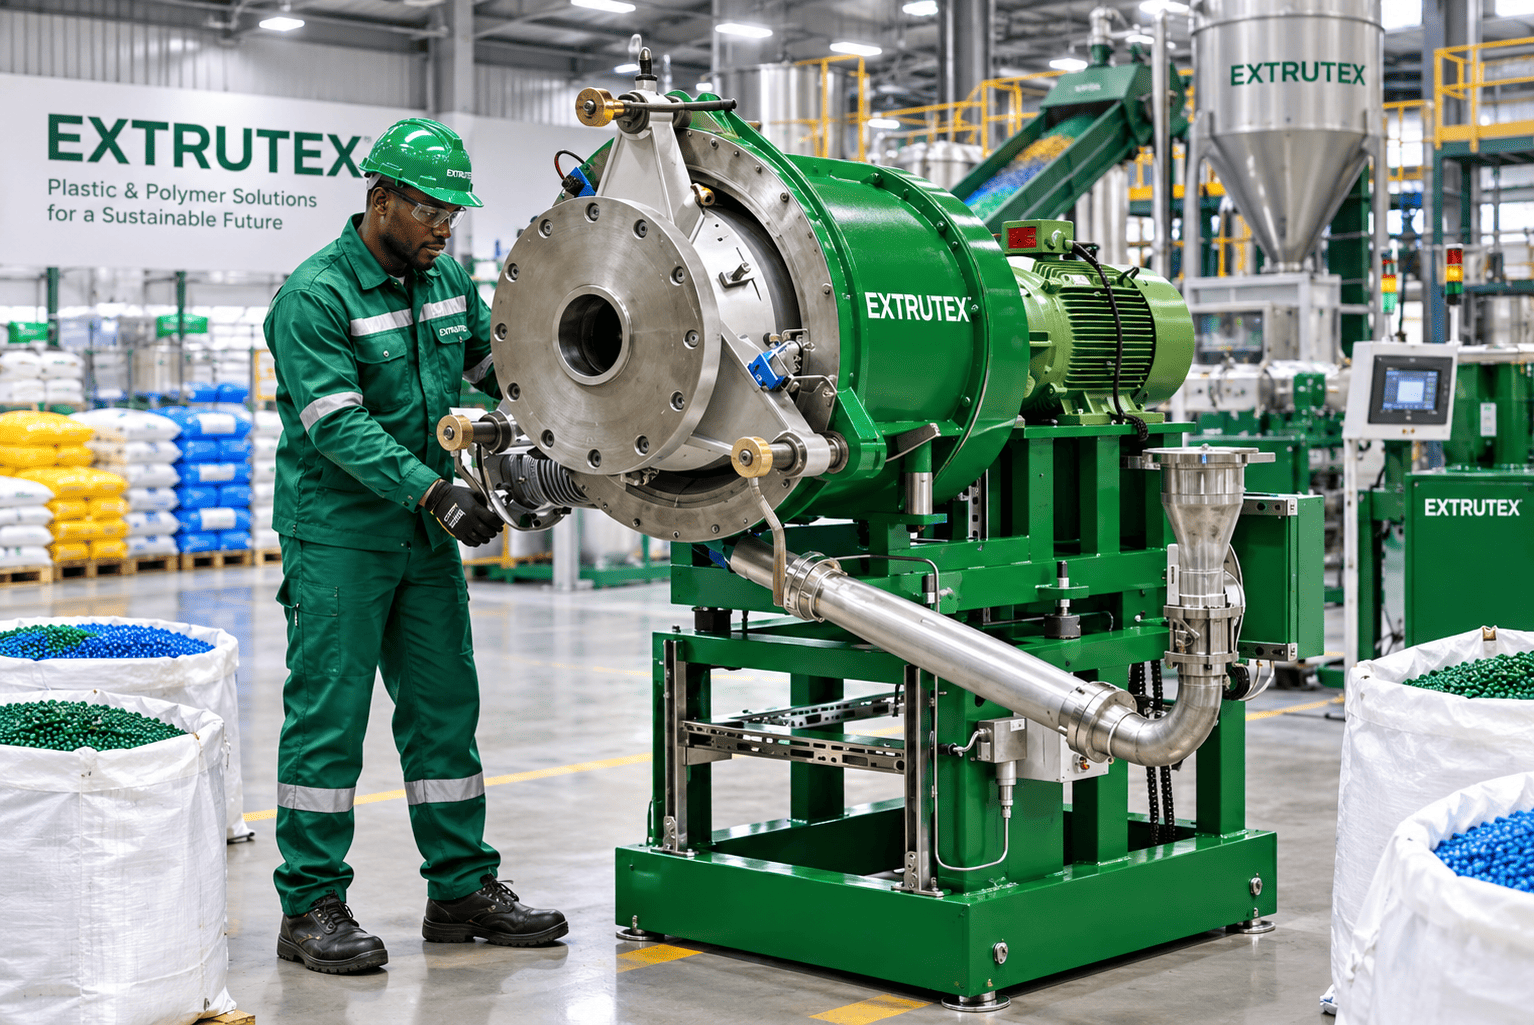
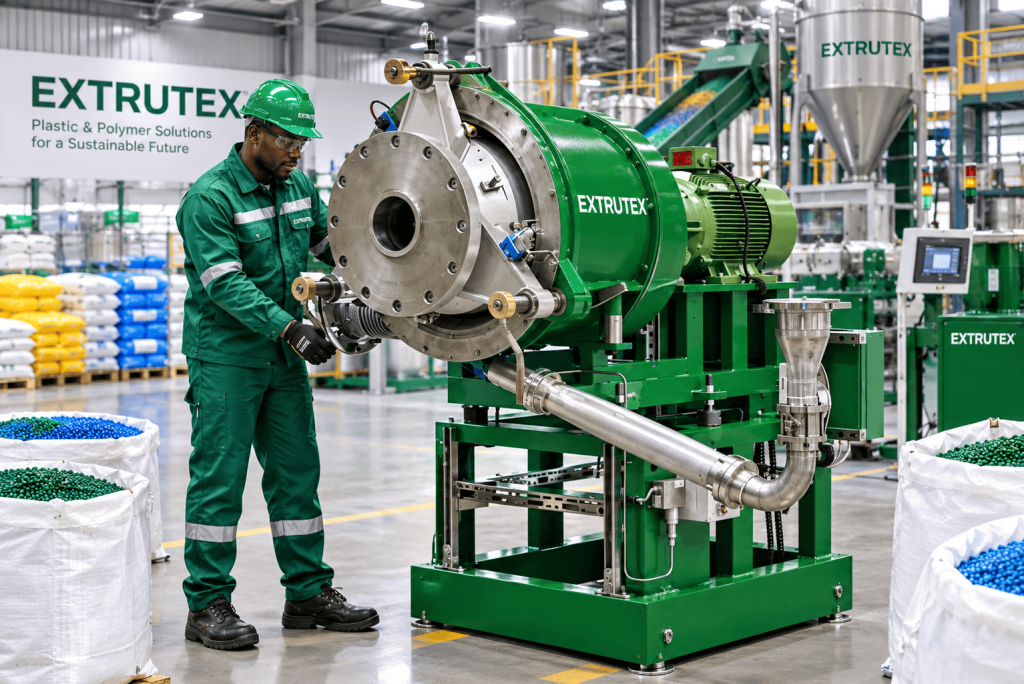
The EXTRUTEX EWRG Water Ring Pelletizer is a compact and efficient strand-cutting pelletizing solution designed for the continuous production of thermoplastic pellets. Developed around a water-ring cooling and conveying principle, the system is suitable for a broad range of polymer materials and can be configured for standard, filled, reinforced and technically demanding thermoplastic compounds.
EXTRUTEX engineering combines Austrian design standards with industrial manufacturing in Nanjing and Shanghai, China. The result is a pelletizing system designed for stable operation, practical maintenance and consistent pellet quality without unnecessary mechanical complexity.
Depending on the selected model and polymer formulation, the EWRG series can handle throughput requirements of up to approximately 12 t/h within the standard models presented below. The technology is particularly suitable for polyethylene, styrene-based polymers, hard thermoplastic polyurethane and many other pelletizable thermoplastics.
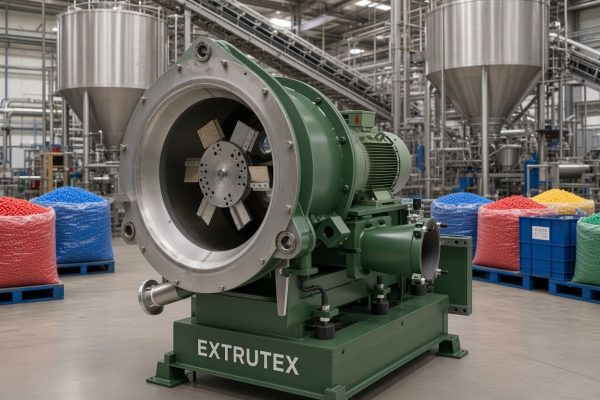
The water ring pelletizing process is designed to separate the cooling and conveying function from the heated die plate. This allows the polymer to be cut directly at the die face while the hot pellets are immediately captured and transported by a controlled water flow.
Polymer melt exits through the heated die openings and is divided into individual pellets by rotating knives positioned at the die face. The freshly cut pellets are thrown into the surrounding circulating water. The water rapidly removes heat from the pellets and simultaneously carries them away from the cutting chamber toward the downstream separation and drying equipment.
A key characteristic of the EWRG design is that the circulating cooling water does not directly contact the heated die plate. This separation helps maintain controlled die conditions and avoids many of the operating problems associated with direct water contact at the die surface.
In conventional strand pelletizing, polymer strands must first be cooled and then transported to a separate cutting operation. Water ring pelletizing takes a more compact approach. Cutting takes place immediately after the polymer exits the die, while water is introduced around the cutting zone to receive, cool and transport the individual pellets.
The die plate remains thermally controlled while the knives operate continuously against the emerging polymer. Because the cooling medium is kept away from the die plate, the thermal conditions around the extrusion openings can be maintained more consistently. This is particularly useful when processing materials that require stable melt temperatures and controlled die conditions.
The geometry of the die holes and the knife arrangement can be adapted to the characteristics of the polymer and the required pellet dimensions. This provides the process engineer with considerable flexibility when configuring the pelletizing system for different materials, formulations and production capacities.
The EWRG concept is therefore well suited to compound production where pellet uniformity, stable operation and reliable continuous production are more important than simply achieving the highest possible cutting speed.
The pelletizing chamber and water circuit are designed to allow a straightforward start-up sequence. This helps operators bring the line into stable production without unnecessarily complicated preparation procedures.
The water circulation is separated from the heated die plate. This supports controlled thermal conditions at the die and helps maintain consistent polymer flow through the nozzle openings.
The die configuration is designed to reduce the risk of freezing or solidification at individual holes when the polymer load per opening is relatively low.
Direct cutting at the die face, together with controlled knife rotation and water transport, provides a practical route to producing pellets with uniform dimensions and a consistent overall appearance.
The die design can be engineered to maintain an efficient melt flow path without creating unnecessary pressure accumulation immediately before the die plate.
Nozzle geometry can be selected according to polymer type, formulation, throughput and desired pellet characteristics. This gives the system considerable flexibility across different thermoplastic applications.
The separation of the cooling circuit from the die plate helps avoid undesirable cavitation effects at the die surface and contributes to stable pelletizing conditions.
Cutting, cooling and pellet transport are integrated into a compact process section. This reduces the required installation footprint compared with more extended strand-cooling arrangements.
Efficient heating and drive requirements, practical component design, controlled wear and straightforward access to service parts help reduce the total operating cost over the equipment lifetime.
The EWRG series can be engineered for a wide variety of thermoplastics, including filled and reinforced compounds where dependable cutting and heat removal are essential.
The die plate is one of the most important components influencing pellet quality. Its thermal performance, hole arrangement, melt-channel geometry and surface condition directly affect the stability of the extrusion process. EXTRUTEX EWRG systems are designed around a controlled die environment so that the polymer remains sufficiently fluid until it reaches the cutting zone.
The rotating knife assembly works directly at the die face. As the polymer exits each opening, the knife separates the melt into individual pellets. Knife speed and die configuration can be selected according to the material and production conditions. This provides process engineers with a practical means of balancing pellet size, throughput and cutting stability.
Because the cooling water does not flow directly across the heated die plate, the system avoids unnecessary thermal disturbance at the melt discharge area. This is particularly beneficial for polymers where small temperature variations can influence melt viscosity or die-hole stability.
Water performs two functions in the EWRG system: it removes heat from the freshly cut pellets and transports them away from the pelletizing chamber. The circulating water forms a controlled ring around the cutting area, receiving the hot pellets immediately after cutting.
The required water circulation rate increases with system capacity and thermal load. EXTRUTEX therefore offers different water-flow configurations across the EWRG model range, allowing the cooling system to be matched to the required production rate.
After cooling and transport, the pellet-water mixture can be directed toward the downstream separation and drying section. The overall arrangement can be integrated into a complete pelletizing line according to the material and production requirements.
The EWRG range covers several machine sizes to accommodate different extrusion capacities. The largest standard model in this specification range is designed for a maximum pelletizable polymer throughput of approximately 12 tonnes per hour.
Actual production capacity depends on several process variables, including polymer formulation, melt temperature, die-hole configuration, pellet size, additive or filler content, knife speed and thermal load. For this reason, EXTRUTEX recommends selecting the pelletizer according to the complete process rather than using throughput alone as the sizing criterion.
Filled and reinforced polymers can require different cutting and cooling conditions from unfilled materials. EXTRUTEX engineering can therefore evaluate the material formulation and extrusion conditions when determining the appropriate EWRG configuration.
The following technical values represent the principal machine parameters for the standard EWRG models. Final machine configuration may vary according to polymer, die arrangement, heating medium, pellet dimensions and required production capacity.
| Technical Parameter | EWRG 280 | EWRG 300 | EWRG 320 | EWRG 400 |
|---|---|---|---|---|
| Maximum Heating Medium Pressure [bar] | 32 | 32 | 32 | 40 |
| Minimum Installed Drive Motor Power [kW] | 7.5 | 9.2 | 17 | 30 |
| Water Circulation Capacity [m³/h] | 90 | 90 | 120 | 200 |
| Maximum Pelletizing Throughput [t/h] | 3 | 4.5 | 7 | 12 |
| Heating Medium | Thermal Oil / Steam | Thermal Oil / Steam | Thermal Oil / Steam | Thermal Oil / Steam |
| Pelletizing Technology | Water Ring | Water Ring | Water Ring | Water Ring |
Note: Throughput values are indicative maximum capacities for suitable pelletizable thermoplastics. Actual output depends on polymer grade, formulation, filler or reinforcement content, melt temperature, die configuration, pellet dimensions and operating conditions.
The EXTRUTEX EWRG water ring pelletizer can be engineered for a broad spectrum of thermoplastic materials. Typical applications include the pelletizing of polyethylene, styrene polymers, thermoplastic polyurethane and other pelletizable engineering and commodity thermoplastics.
The technology is also suitable for many filled and reinforced formulations. Depending on the material, additives such as mineral fillers, glass fiber or other reinforcement systems can influence melt viscosity, die pressure and knife wear. These factors should be considered during machine configuration.
For technically demanding compounds, EXTRUTEX can adapt the die and cutting configuration to the processing characteristics of the specific formulation.
A pelletizing system should not be evaluated only by its maximum hourly output. Energy consumption, knife and die wear, accessibility, spare-part requirements, start-up time and operator workload all have a direct influence on the long-term economics of a production line.
The EXTRUTEX EWRG architecture focuses on keeping these factors under control. Its compact construction reduces unnecessary equipment volume, while the integrated cutting and cooling principle minimizes the number of process stages between the die and the finished pellet.
Low mechanical complexity also makes routine inspection and maintenance more straightforward. Wear components can be serviced without turning the pelletizing section into a lengthy maintenance operation.
Consistent pellet quality depends on keeping the die plate, knife assembly and water circuit in proper operating condition. Regular inspection of knife geometry, die-hole condition and water circulation is recommended, particularly when processing abrasive filled or reinforced compounds.
EXTRUTEX designs the EWRG system with service accessibility in mind. Routine maintenance activities can be incorporated into the production schedule, helping reduce unnecessary downtime and maintain stable pelletizing performance over the operating life of the machine.
The equipment can also be configured with appropriate material-resistant components for demanding processing environments. Components exposed to process conditions can be selected according to the polymer formulation and operating environment.
EXTRUTEX develops its pelletizing technology around an engineering approach that combines Austrian design standards with competitive industrial manufacturing capability.
The EWRG water ring pelletizers are manufactured in Nanjing and Shanghai, China, under EXTRUTEX technical specifications and quality requirements. This manufacturing structure allows EXTRUTEX to provide industrial pelletizing equipment with a strong balance between engineering performance, manufacturing efficiency and overall investment cost.
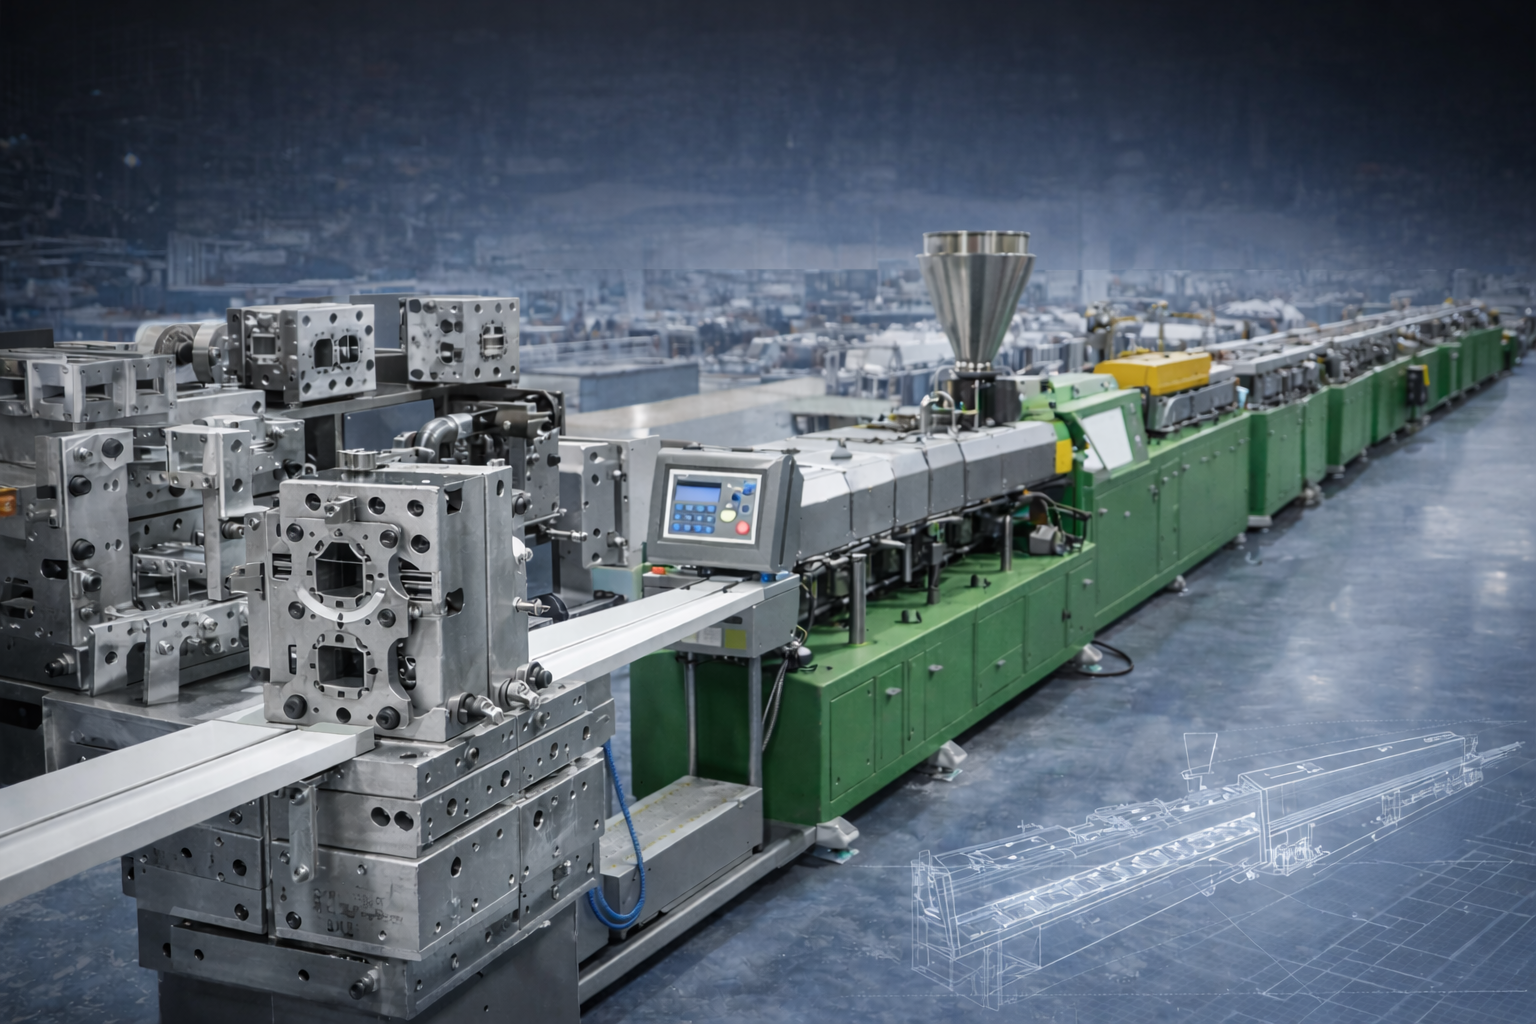
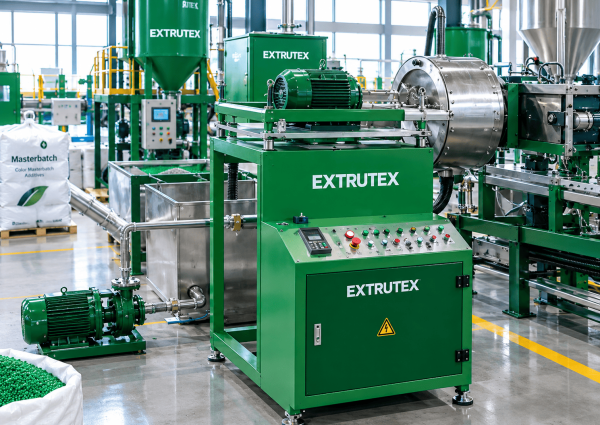
From individual pelletizers to complete extrusion and compounding lines, EXTRUTEX can coordinate the pelletizing section with the upstream extruder, melt filtration, die system, cooling circuit and downstream pellet handling equipment.
The EWRG is not limited to operation as an isolated machine. It can form the pelletizing section of a complete EXTRUTEX compounding or polymer processing line. Depending on the application, the upstream process may include a single-screw extruder, co-rotating twin-screw extruder, melt filtration system and heated die.
Downstream equipment can include the water circulation system, pellet separation, drying equipment, fines removal and pellet collection or conveying. The complete arrangement can be engineered around the polymer formulation and required production capacity.
The EXTRUTEX EWRG Water Ring Pelletizer provides a compact approach to continuous thermoplastic pellet production, combining direct melt cutting with rapid water cooling and hydraulic pellet transport.
With capacities from approximately 3 to 12 t/h across the standard EWRG 280, EWRG 300, EWRG 320 and EWRG 400 models, the range covers a broad spectrum of industrial compounding and polymer processing applications.
The combination of controlled die heating, direct knife cutting, separated water circulation, flexible nozzle configuration and compact machine architecture makes the EWRG a practical solution for producers looking for stable pellet quality, efficient operation and manageable maintenance requirements.
EXTRUTEX — Austrian Design Engineering, Manufactured in Nanjing and Shanghai, China.
There are no reviews yet.
By submitting your email, you agree to our company’s terms and conditions.
We are not looking to sell; we are here to provide you with the best support and service.
Contact available 24/7
Please do not contact us for advertising or sales inquiries
All rights of this website are reserved for EXTRUTEX Austria and its partner companies, © 2026
-
(0 customer reviews)