No products in the cart.
All rights of this website are reserved for EXTRUTEX Austria and its partner companies, © 2026

Multiple Payment Methods

Discount for advance payments over 50%

Free Shipping Coordination Services
Payment methods:

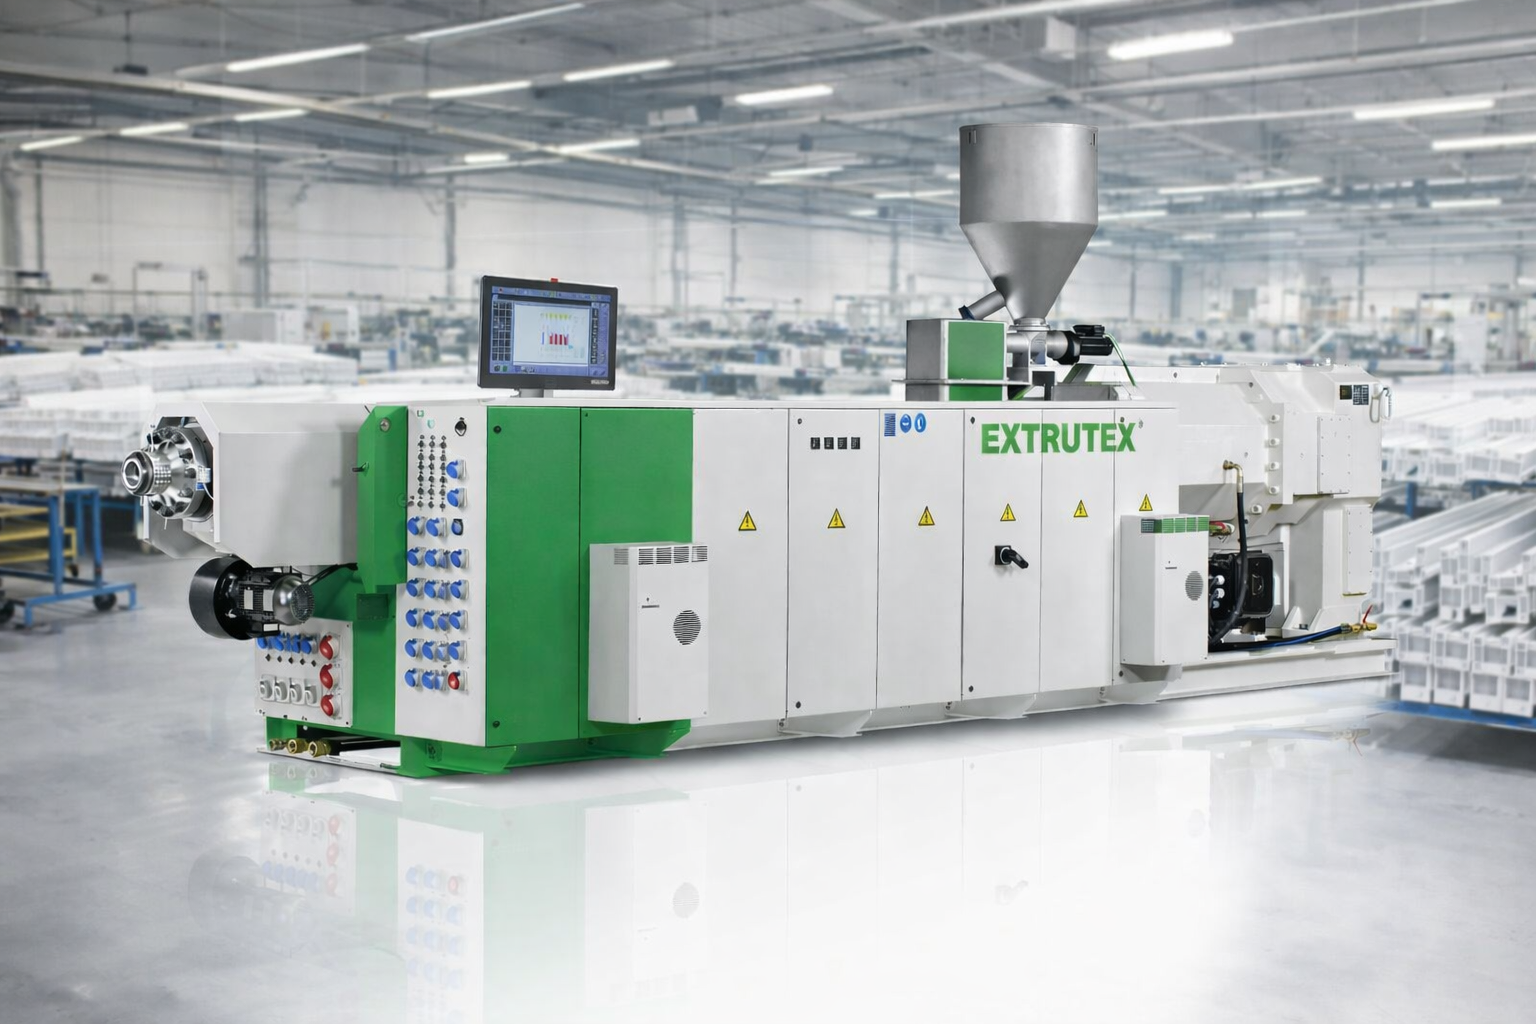
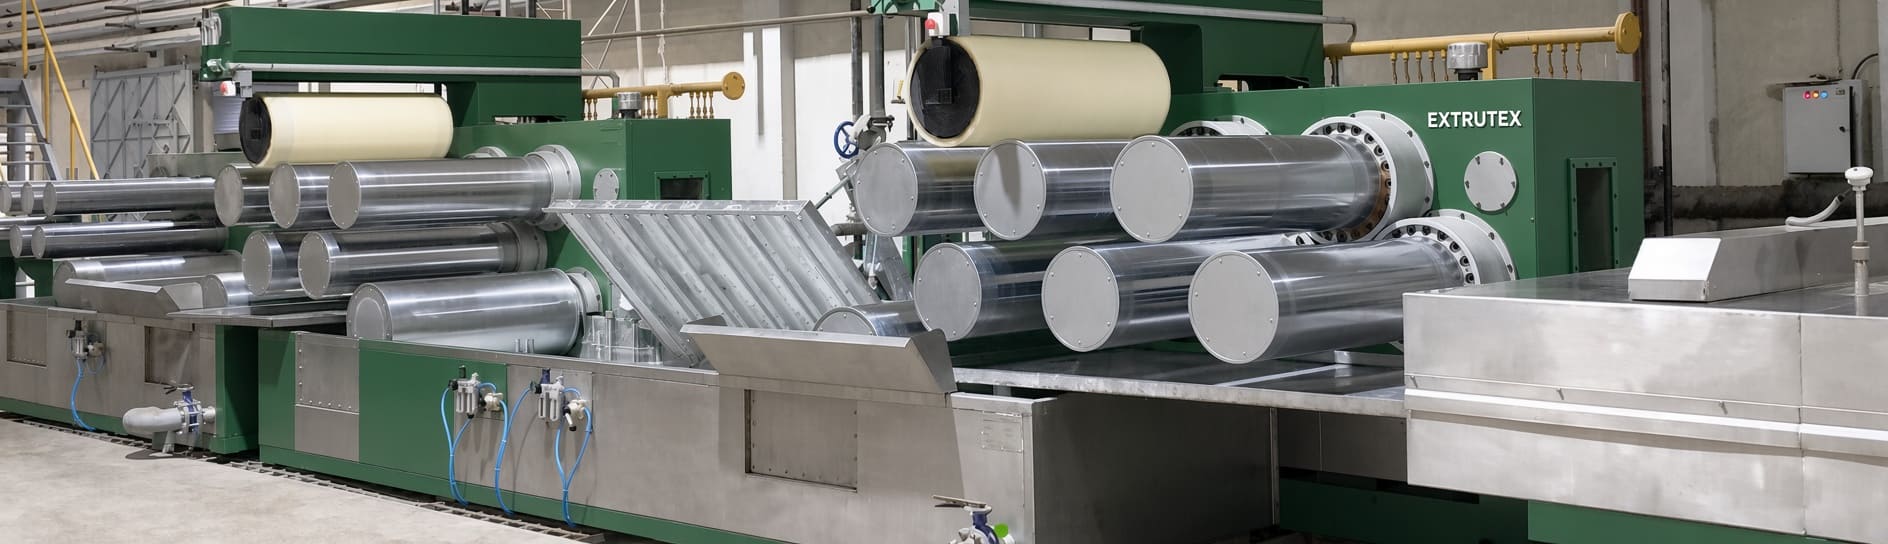
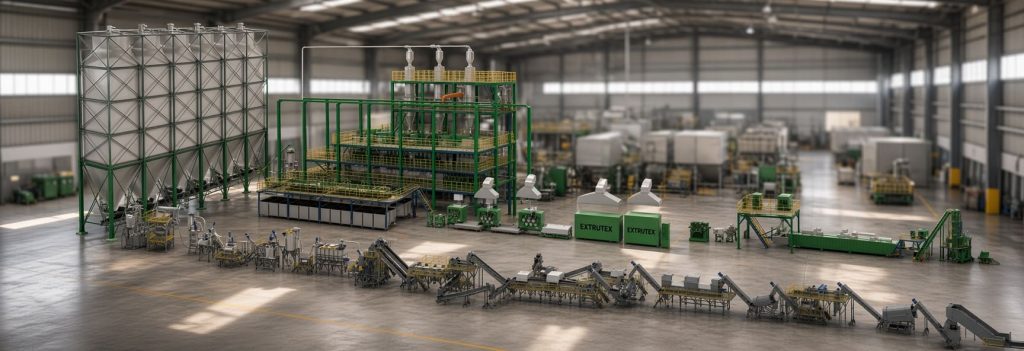
The EXTRUTEX Waste PET Bottles to Polyester Staple Fiber Production Line is a complete industrial solution for converting post-consumer PET bottles and other suitable recycled PET feedstocks into high-quality polyester staple fiber. The system combines PET material preparation, drying, melting, extrusion, spinning, drawing, crimping, cutting and baling into an integrated production process.
Polyester staple fiber made from recycled PET provides an effective route for converting used plastic bottles into valuable textile and industrial raw materials. Instead of treating waste PET bottles as a disposal problem, the material can be recovered, cleaned, processed and transformed into fibers for applications such as sofas, carpets, garments, non-woven products and other textile or industrial materials.
EXTRUTEX develops complete bottle-to-fiber solutions according to the characteristics of the available PET feedstock and the required fiber specification. The production line can be configured for different types of polyester staple fiber, including cotton-type fiber, non-woven fiber, hollow fiber, hollow conjugate fiber and dope-dyed fiber.
```Producing polyester staple fiber from waste PET bottles requires much more than a fiber spinning machine. The quality of the final fiber depends on the quality of the recycled PET feedstock, the drying conditions, melt quality, extrusion stability, spinning parameters, drawing ratio, crimping performance and final cutting.
EXTRUTEX therefore approaches the project as a complete production system. The line can receive suitable recycled PET flakes, pellets, lumps or compatible polyester fiber waste and prepare the material for controlled melting and extrusion.
The production process is engineered around the final fiber application. Different customers may require different deniers, cross-sections, lengths, crimp levels, hollow structures or dyeing characteristics. The drawing and downstream fiber-processing sections can therefore be configured according to the required product.
The extrusion section can be designed to process several forms of recycled PET feedstock, subject to appropriate quality and preparation. Typical materials include:
The quality of the input material has a direct influence on fiber quality. PET flakes should therefore be properly washed, sorted and prepared before entering the fiber production line. For bottle-to-fiber projects, EXTRUTEX can coordinate the required PET washing and preparation process according to the characteristics of the local waste stream.
Each section performs an important function in converting recycled PET into stable, commercially useful polyester staple fiber. The following stages describe the process in greater detail.
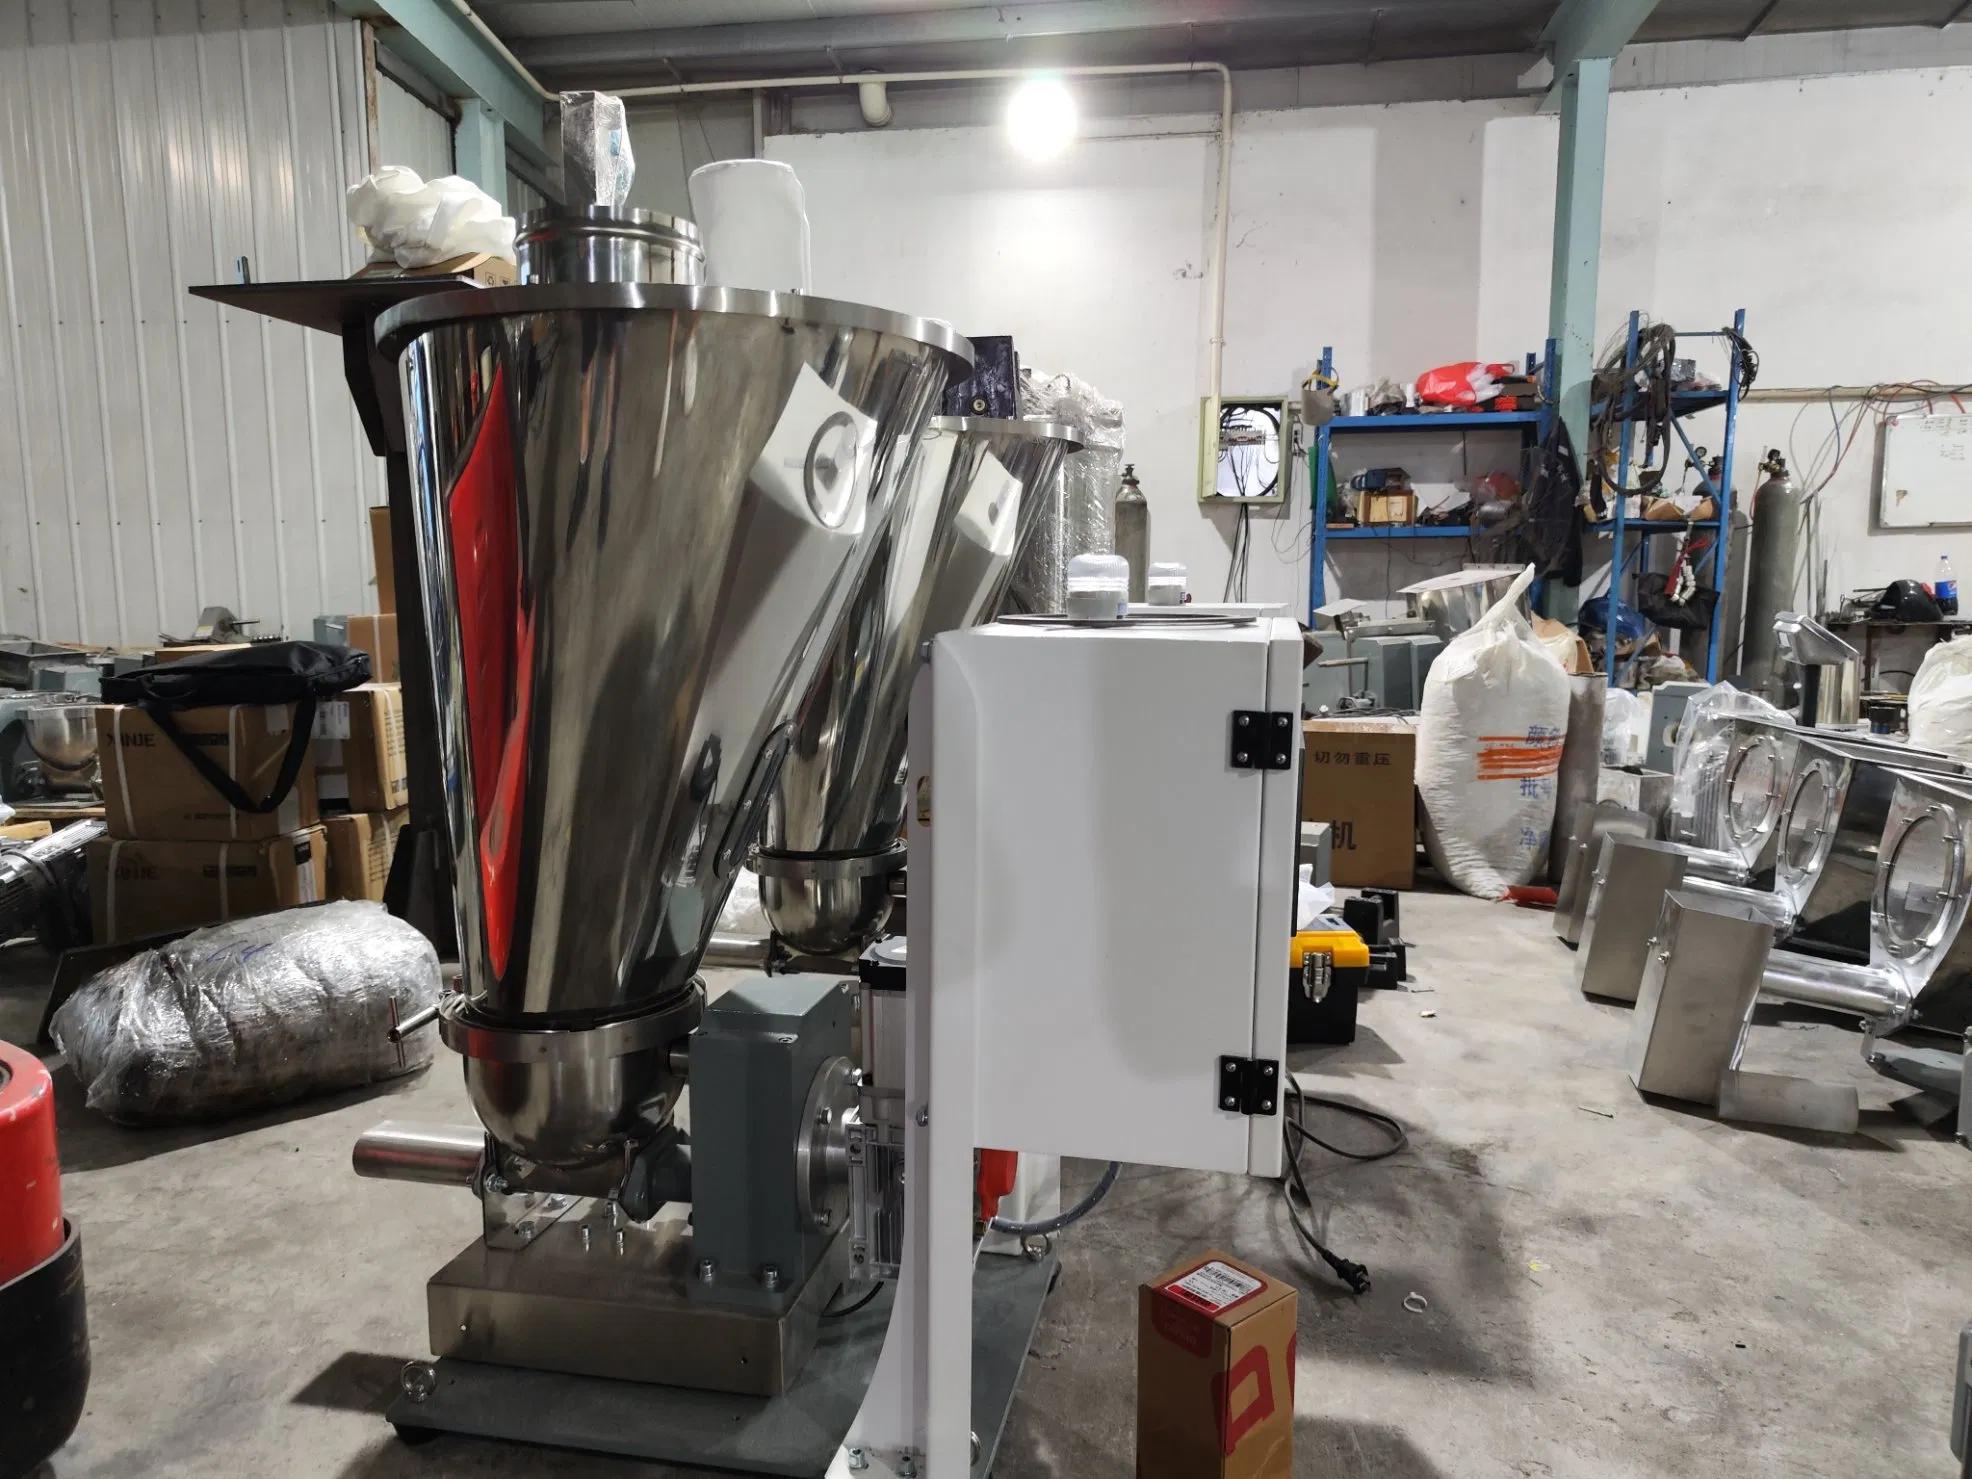
The production process begins with controlled feeding of recycled PET material into the fiber production system. The feeding equipment is designed to provide a stable and continuous supply of flakes, pellets, lumps or other approved PET feedstock.
Consistent feeding is essential because fluctuations in material supply can influence extrusion pressure, melt throughput and spinning stability. The feeding system therefore forms the connection between material storage and the main fiber-production process.
After feeding, the recycled PET material is transferred to a silo or controlled storage system. The silo provides a buffer between material preparation and the extrusion process.
Stable material storage helps maintain continuous production and allows the extrusion system to receive PET at a controlled rate. It also simplifies factory logistics and provides operators with better control over material supply.
Drying is one of the most critical stages in recycled PET processing. PET is sensitive to moisture, and excessive moisture during melting can cause hydrolytic degradation, reducing molecular weight and negatively affecting melt properties.
The drying system therefore removes moisture from the recycled PET before it enters the melting and extrusion section. Controlled drying conditions help protect material quality and contribute to stable spinning performance.
Proper drying is particularly important when processing recycled PET flakes because the material can retain moisture after washing and storage. The drying system is selected according to the material throughput, moisture level and required production conditions.
The dried PET enters the heating and melting section, where controlled thermal energy converts the solid material into a homogeneous polymer melt.
Temperature control is carefully managed throughout the melting process. The objective is to achieve uniform plasticization without unnecessarily exposing the recycled PET to excessive thermal stress.
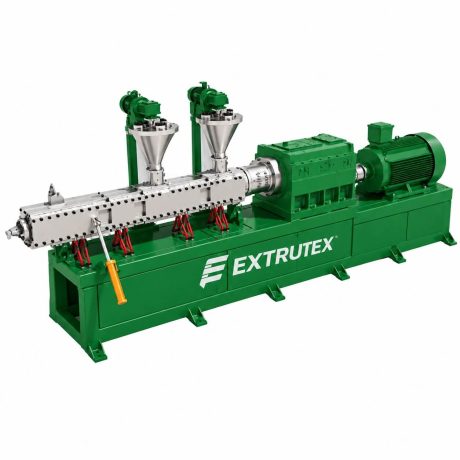
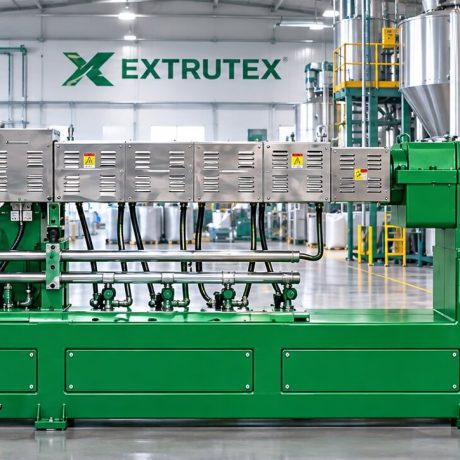
The molten PET is transported through the extrusion system. The extruder provides controlled conveying, melting and pressure generation before the polymer reaches the spinning section.
A stable extrusion process is essential for consistent fiber production. Variations in melt pressure or temperature can influence fiber diameter, denier and spinning stability. EXTRUTEX designs the extrusion section according to the required production capacity and fiber specification.
The metering pump provides precise and stable polymer flow to the spinning system. Accurate melt metering is particularly important in polyester fiber production because even small variations in polymer flow can influence the consistency of the resulting filaments.
Stable metering contributes to uniform fiber production and supports precise control of the target denier.
During spinning, the molten PET is forced through the spinneret to form multiple fine polymer filaments. The spinneret design and operating conditions are selected according to the desired fiber specification.
Different spinneret configurations can be used to achieve different fiber structures and applications. Depending on the production design, the system can produce standard solid fibers, hollow fibers and other specialized fiber structures.
Newly formed filaments are cooled and solidified in the quenching section. Controlled airflow removes heat from the polymer and stabilizes the freshly spun filaments.
Uniform cooling is important for maintaining stable filament properties across the spinning position. Proper quenching contributes to consistent fiber diameter and downstream drawing behavior.
After quenching, the filaments are collected by the take-up system. Controlled take-up speed maintains stable filament tension and prepares the material for the drawing process.
Accurate control of this stage contributes to stable fiber production and helps maintain consistency throughout the subsequent processing steps.
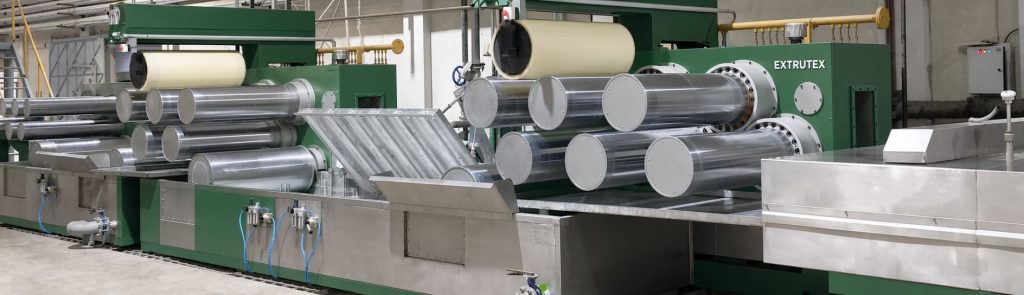
Drawing is a fundamental stage in polyester staple fiber production. The filaments are stretched under controlled conditions to orient the polymer molecules and improve the mechanical properties of the fiber.
The drawing process can be adjusted according to the target fiber denier, strength, elongation and application. Multiple drawing stages provide controlled stretching and allow the production line to achieve the required fiber characteristics.
The fiber tow is organized through the feeding and creel sections. These systems guide and manage the fiber bundles before they enter the sequential drawing and finishing stages.
Proper tow management is important for maintaining even tension and preventing tangling or irregular fiber movement.
The tow-guiding system controls the movement and alignment of the fiber bundle as it passes through the production line. Stable guiding helps maintain consistent tow tension and ensures smooth movement between processing stations.
The first drawing stand begins the controlled orientation process. The fiber tow is stretched at a defined ratio to achieve the desired molecular orientation and preliminary mechanical properties.
The exact drawing conditions depend on the PET feedstock and final fiber specification.
The immersion bath provides controlled treatment of the fiber tow during the drawing process. Temperature and process conditions can be adjusted to support stable fiber stretching and improve processing behavior.
The second drawing stage continues the orientation process. Controlled stretching improves the balance between strength, elongation and dimensional stability.
Multi-stage drawing allows the fiber producer to optimize the final properties more precisely than a single drawing operation.
The draw chest provides controlled handling and conditioning of the fiber tow between drawing stages. It contributes to stable fiber movement and supports the required process sequence.
The third drawing stage completes the main stretching sequence. The final drawing conditions are selected according to the target denier, mechanical properties and end-use requirements.
Proper coordination between all drawing stages is essential for producing uniform polyester staple fiber.
Oiling applies a controlled finish to the fiber surface. The finish improves fiber processing characteristics, reduces unwanted friction and supports smoother handling during crimping, cutting and subsequent textile processing.
The finish formulation and application rate can be selected according to the intended fiber application.
After finishing, the fiber tow is collected and arranged for the crimping process. Controlled stacking helps maintain a stable tow structure and prepares the material for mechanical crimp formation.
Crimping gives the polyester staple fiber its characteristic three-dimensional waviness. This structure improves bulk, resilience, softness and processing behavior.
Crimp parameters can be adjusted according to the intended application. Different requirements may exist for sofa filling, carpet fiber, non-woven materials and garment-related applications.
The relaxation stage allows the fiber to stabilize after drawing and crimping. Controlled thermal and mechanical conditions help reduce internal stress and improve dimensional stability.
The continuous fiber tow is cut into predetermined staple lengths. Fiber length is selected according to the target market and downstream application.
Consistent cutting is important for subsequent carding, spinning, non-woven processing, filling and other textile operations.
The final polyester staple fiber is compressed and packed into bales for storage, transportation and sale. Automatic or semi-automatic baling systems can be integrated according to production requirements.
Proper bale density and packaging improve transportation efficiency and simplify handling at the customer's textile or industrial processing facility.
| Fiber Type | Typical Specification Range | Potential Applications |
|---|---|---|
| Spinning / Cotton-Type Fiber | 1.2D–3D | Textile and spinning applications |
| Non-Woven Fiber | 1.5D–25D | Non-woven fabrics and industrial materials |
| Hollow Fiber | 1.5D–25D | Filling, insulation and textile applications |
| Hollow Conjugate Fiber | 3D–20D | High-bulk filling and specialized textile products |
| Dope-Dyed Fiber | Project dependent | Colored fiber applications and textile products |
EXTRUTEX polyester staple fiber production lines are available in production capacities from approximately 15 to 100 tons per day per line. The final capacity depends on fiber denier, fiber type, production speed, PET feedstock quality and the selected line configuration.
| Parameter | Specification |
|---|---|
| System | Waste PET Bottles to Polyester Staple Fiber Production Line |
| Manufacturer | EXTRUTEX |
| Production Capacity | 15–100 tons/day per line |
| Feedstock | Recycled PET flakes, pellets, lumps and suitable polyester fiber waste |
| Fiber Types | Cotton-type, non-woven, hollow, hollow conjugate and dope-dyed fiber |
| Spinning Fiber | Approximately 1.2D–3D |
| Non-Woven Fiber | Approximately 1.5D–25D |
| Hollow / Conjugate Fiber | Approximately 3D–20D |
| Process | Drying → Melting → Extrusion → Spinning → Drawing → Oiling → Crimping → Cutting → Baling |
| Research & Laboratory | EXTRUTEX Austria |
| Manufacturing | China |
Hollow and hollow-conjugate polyester staple fibers can provide useful bulk, resilience and softness for furniture filling applications. Recycled PET fiber can therefore be used as a secondary raw material for sofa cushions, furniture padding and similar products.
Polyester staple fiber is widely used in carpet and floor-covering applications. The fiber specification can be adjusted according to the required strength, bulk, appearance and processing characteristics.
Suitable cotton-type and fine-denier recycled polyester staple fibers can be used in selected textile applications. Fiber denier, length, finish and mechanical properties can be configured according to the intended spinning process and final textile product.
Larger-denier polyester staple fibers are suitable for various non-woven applications. Depending on the fiber properties and downstream process, recycled polyester can be used in industrial fabrics, padding, filtration-related materials and other technical textile products.
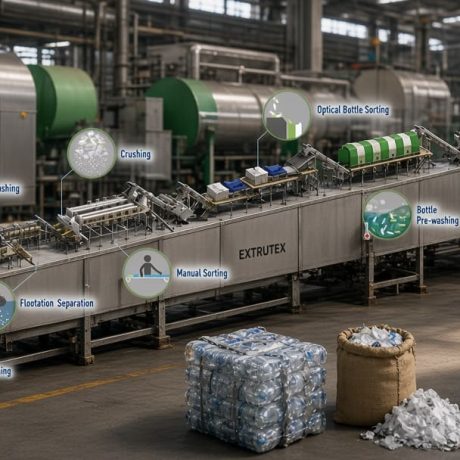
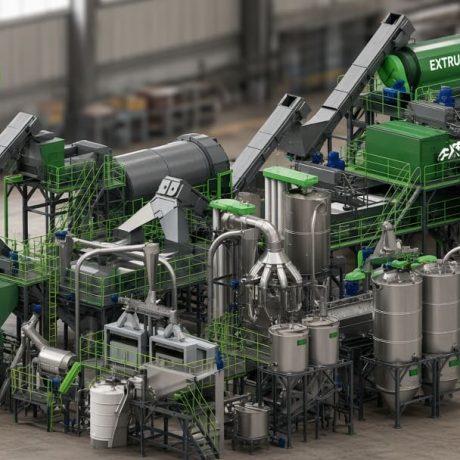
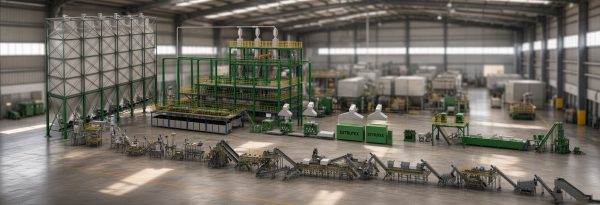
For customers starting with post-consumer PET bottles, EXTRUTEX can develop the project as an integrated bottle-to-fiber solution. The complete project can include PET bottle sorting, crushing, washing, flake separation, drying and preparation before the material enters the polyester staple fiber production line.
This integrated approach provides better control over the quality of the PET feedstock entering the fiber process. The washing and sorting configuration can be designed according to local bottle collection conditions, contamination levels and required fiber quality.
The drawing and finishing section can then be customized for the intended fiber type. Different products require different drawing ratios, deniers, fiber lengths, crimp levels and finish characteristics, so the production line should be designed around the final application rather than using a one-size-fits-all configuration.
EXTRUTEX can integrate centralized industrial automation and DCS-based control technology into the polyester staple fiber production line. The control architecture coordinates material feeding, drying, extrusion, spinning and downstream fiber-processing equipment.
Automated monitoring helps operators control important process parameters such as temperature, pressure, throughput, drawing conditions and production speed. This contributes to more consistent production and simplifies operation of large-scale fiber plants.
EXTRUTEX develops complete polymer recycling and fiber-production technology with research and laboratory activities in Austria and industrial manufacturing in China. This structure combines process-development capabilities with competitive manufacturing for large-scale international projects.
The engineering process begins with understanding the customer's PET feedstock, required production capacity and final fiber application. The line can then be configured around the target product rather than simply selecting standard equipment.
For projects using waste PET bottles, the quality of the bottle-washing and flake-preparation process is particularly important. The cleaner and more consistent the PET feedstock, the more stable the subsequent drying, extrusion and spinning process can be.
The EXTRUTEX Waste PET Bottles to Polyester Staple Fiber Production Line provides a complete route for converting discarded PET bottles into commercially valuable polyester fiber. By integrating material preparation, drying, melting, extrusion, spinning, drawing, finishing, crimping, cutting and baling, the system transforms recycled PET into a usable textile and industrial raw material.
With production capacities from 15 to 100 tons per day and multiple fiber configurations, the technology can be adapted for different markets and applications. Whether the target is fine spinning fiber, non-woven fiber, hollow fiber, hollow conjugate fiber or dope-dyed fiber, the process can be engineered around the required product specifications.
EXTRUTEX can develop a complete waste PET bottle recycling and polyester staple fiber production project according to your raw material, production capacity and target fiber application.
Provide your PET feedstock information, required tons-per-day capacity, target denier and intended fiber application to our engineering team for process evaluation and complete line configuration.
```
There are no reviews yet.
By submitting your email, you agree to our company’s terms and conditions.
We are not looking to sell; we are here to provide you with the best support and service.
Contact available 24/7
Please do not contact us for advertising or sales inquiries
All rights of this website are reserved for EXTRUTEX Austria and its partner companies, © 2026
-
(0 customer reviews)