No products in the cart.
All rights of this website are reserved for EXTRUTEX Austria and its partner companies, © 2026

Multiple Payment Methods

Discount for advance payments over 50%

Free Shipping Coordination Services
Payment methods:

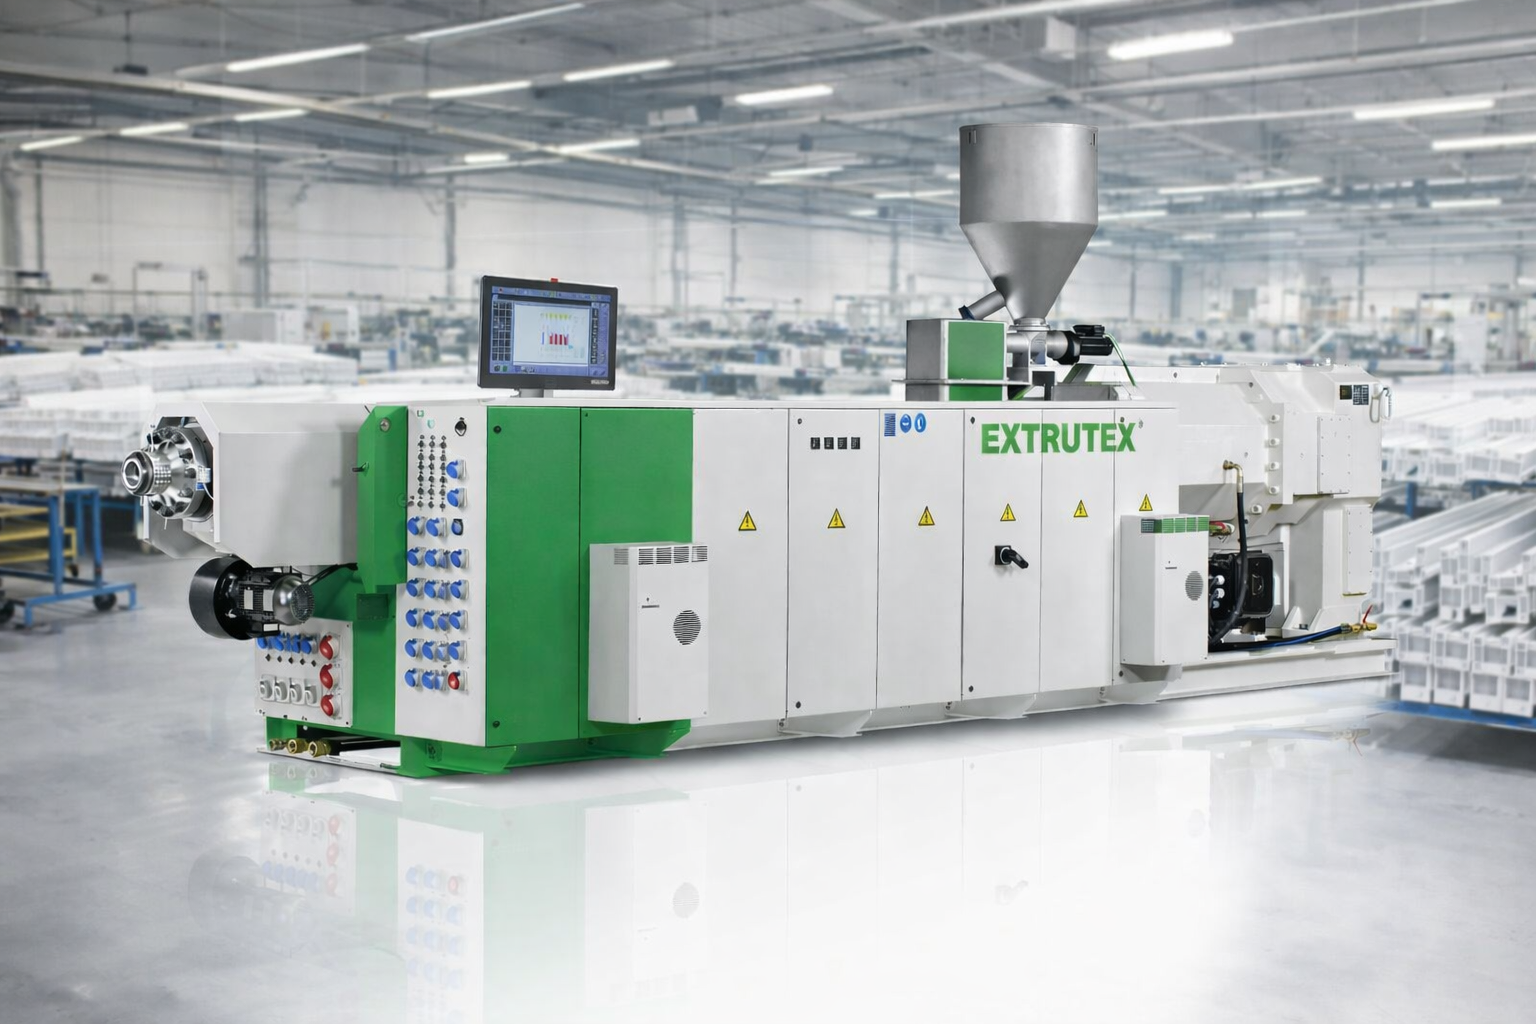
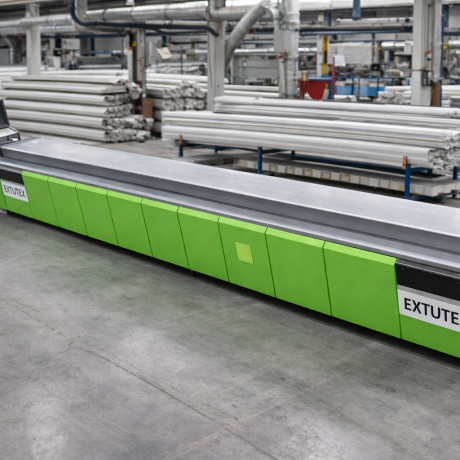
The EXTRUTEX PVC Edge Band Extrusion Line is designed for the continuous production of decorative plastic edge bands used in modern furniture manufacturing. EXTRUTEX manufactures customized edge band extrusion equipment for PVC, ABS, PP, and acrylic-based materials, helping producers manufacture edge bands in different colors, widths, thicknesses, surface finishes, and profile designs.
Plastic edge banding is widely used to cover and protect the exposed edges of furniture panels, including particleboard, MDF, laminated boards, and other engineered wood products. It provides a finished appearance while helping protect panel edges from everyday wear and moisture exposure, depending on the material and the final application.
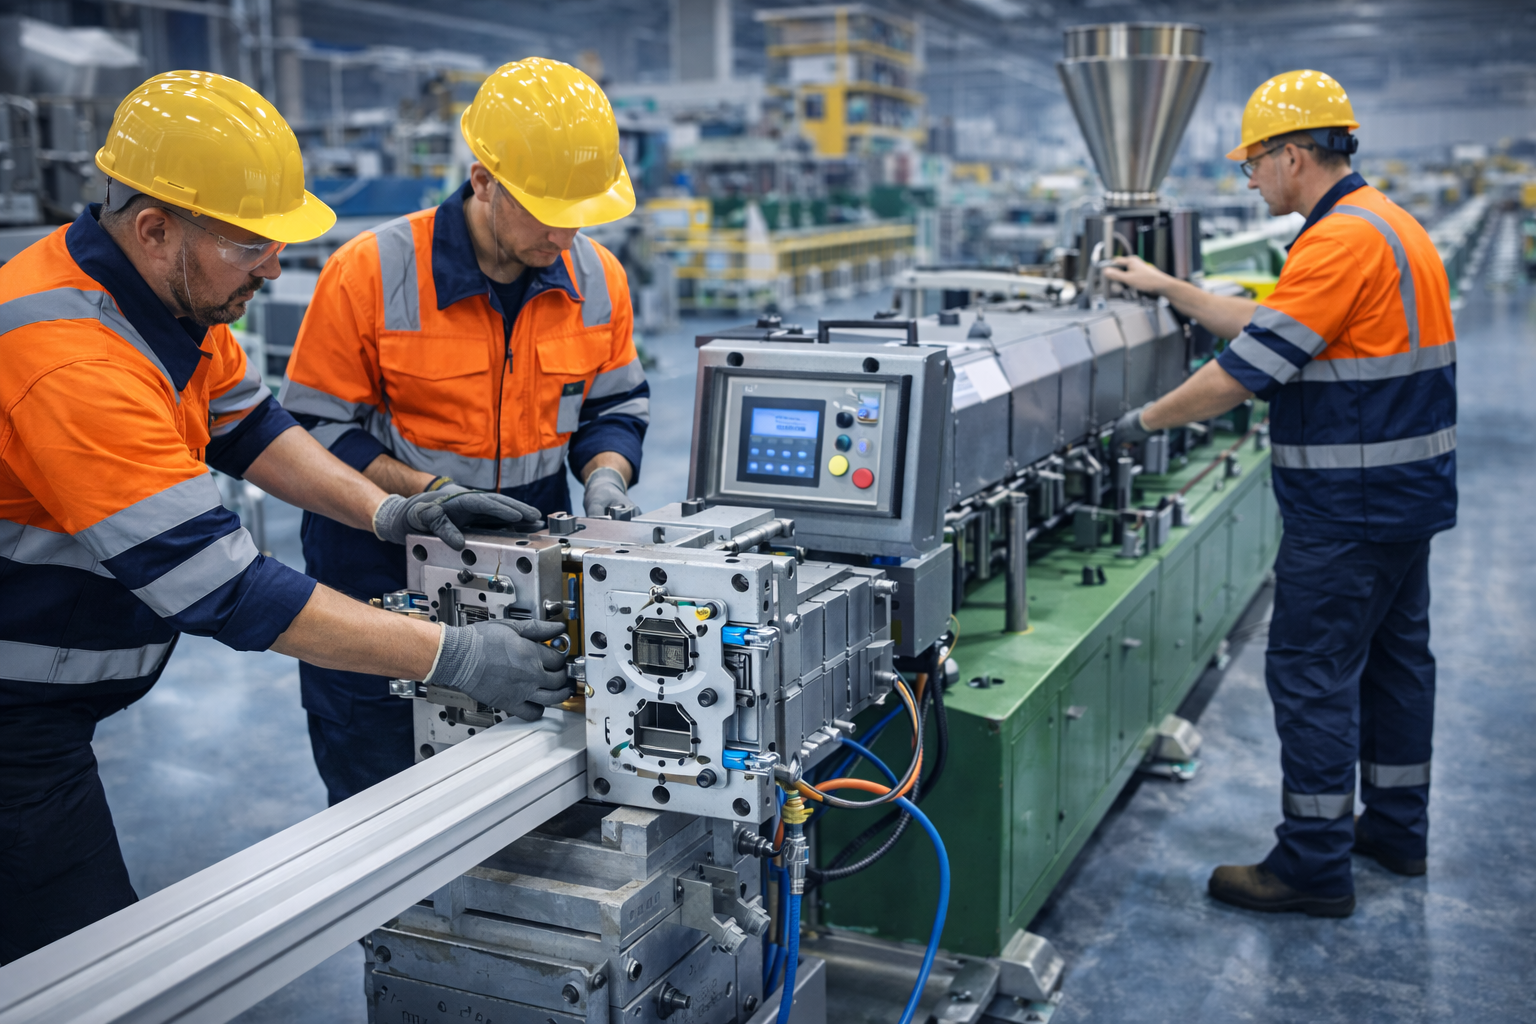
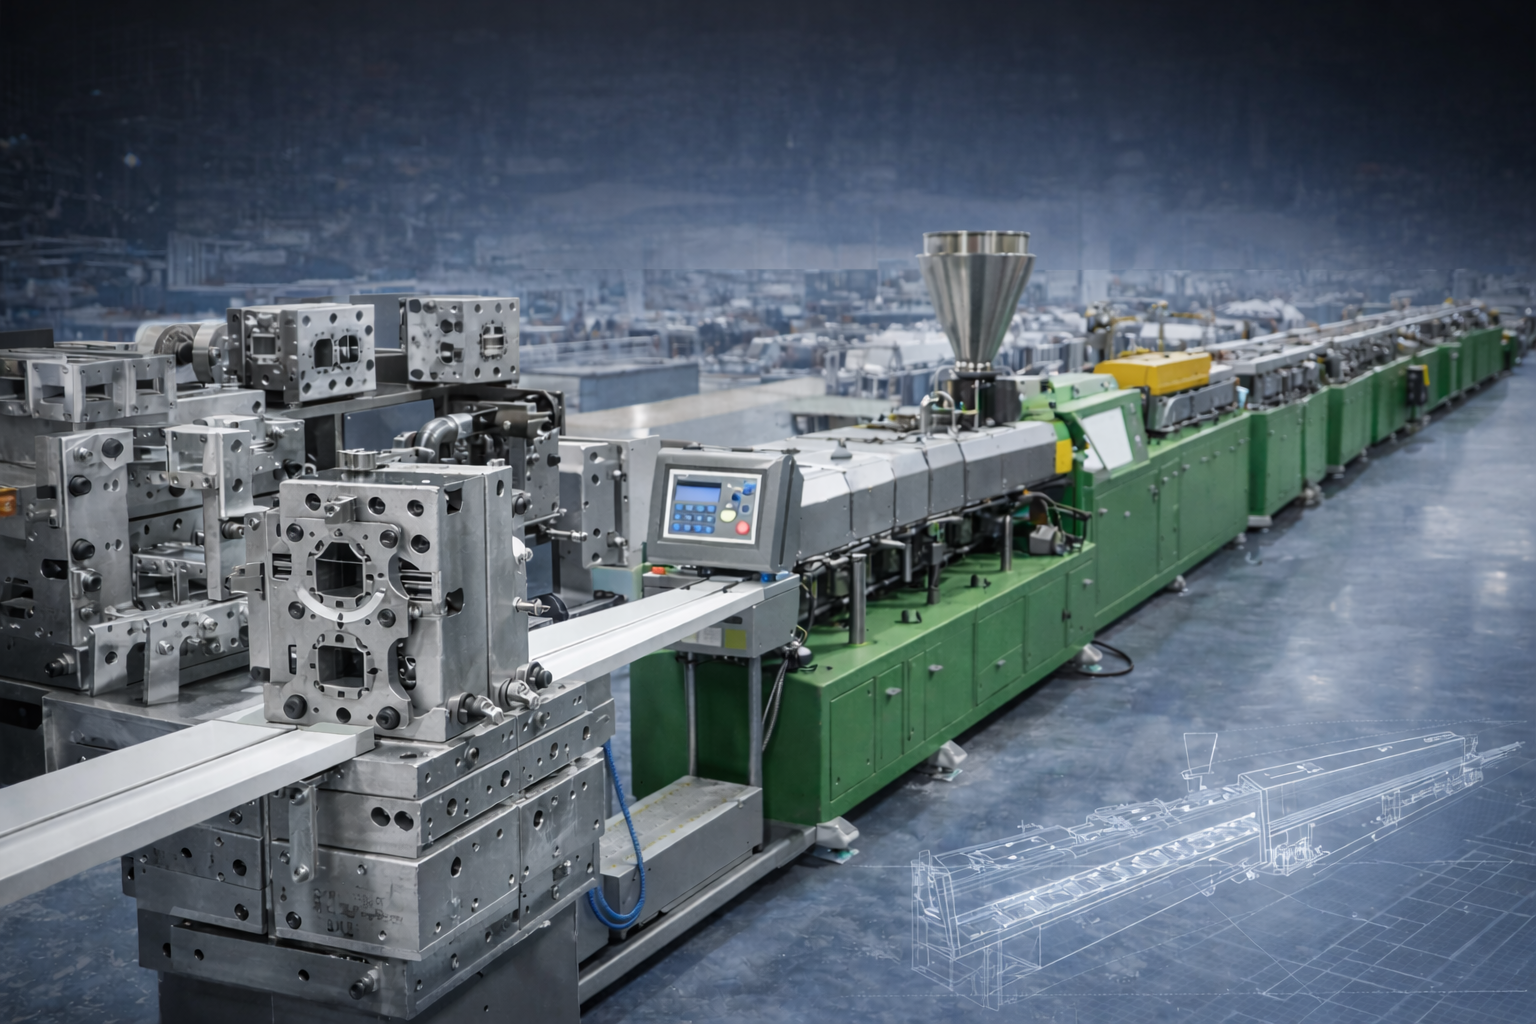
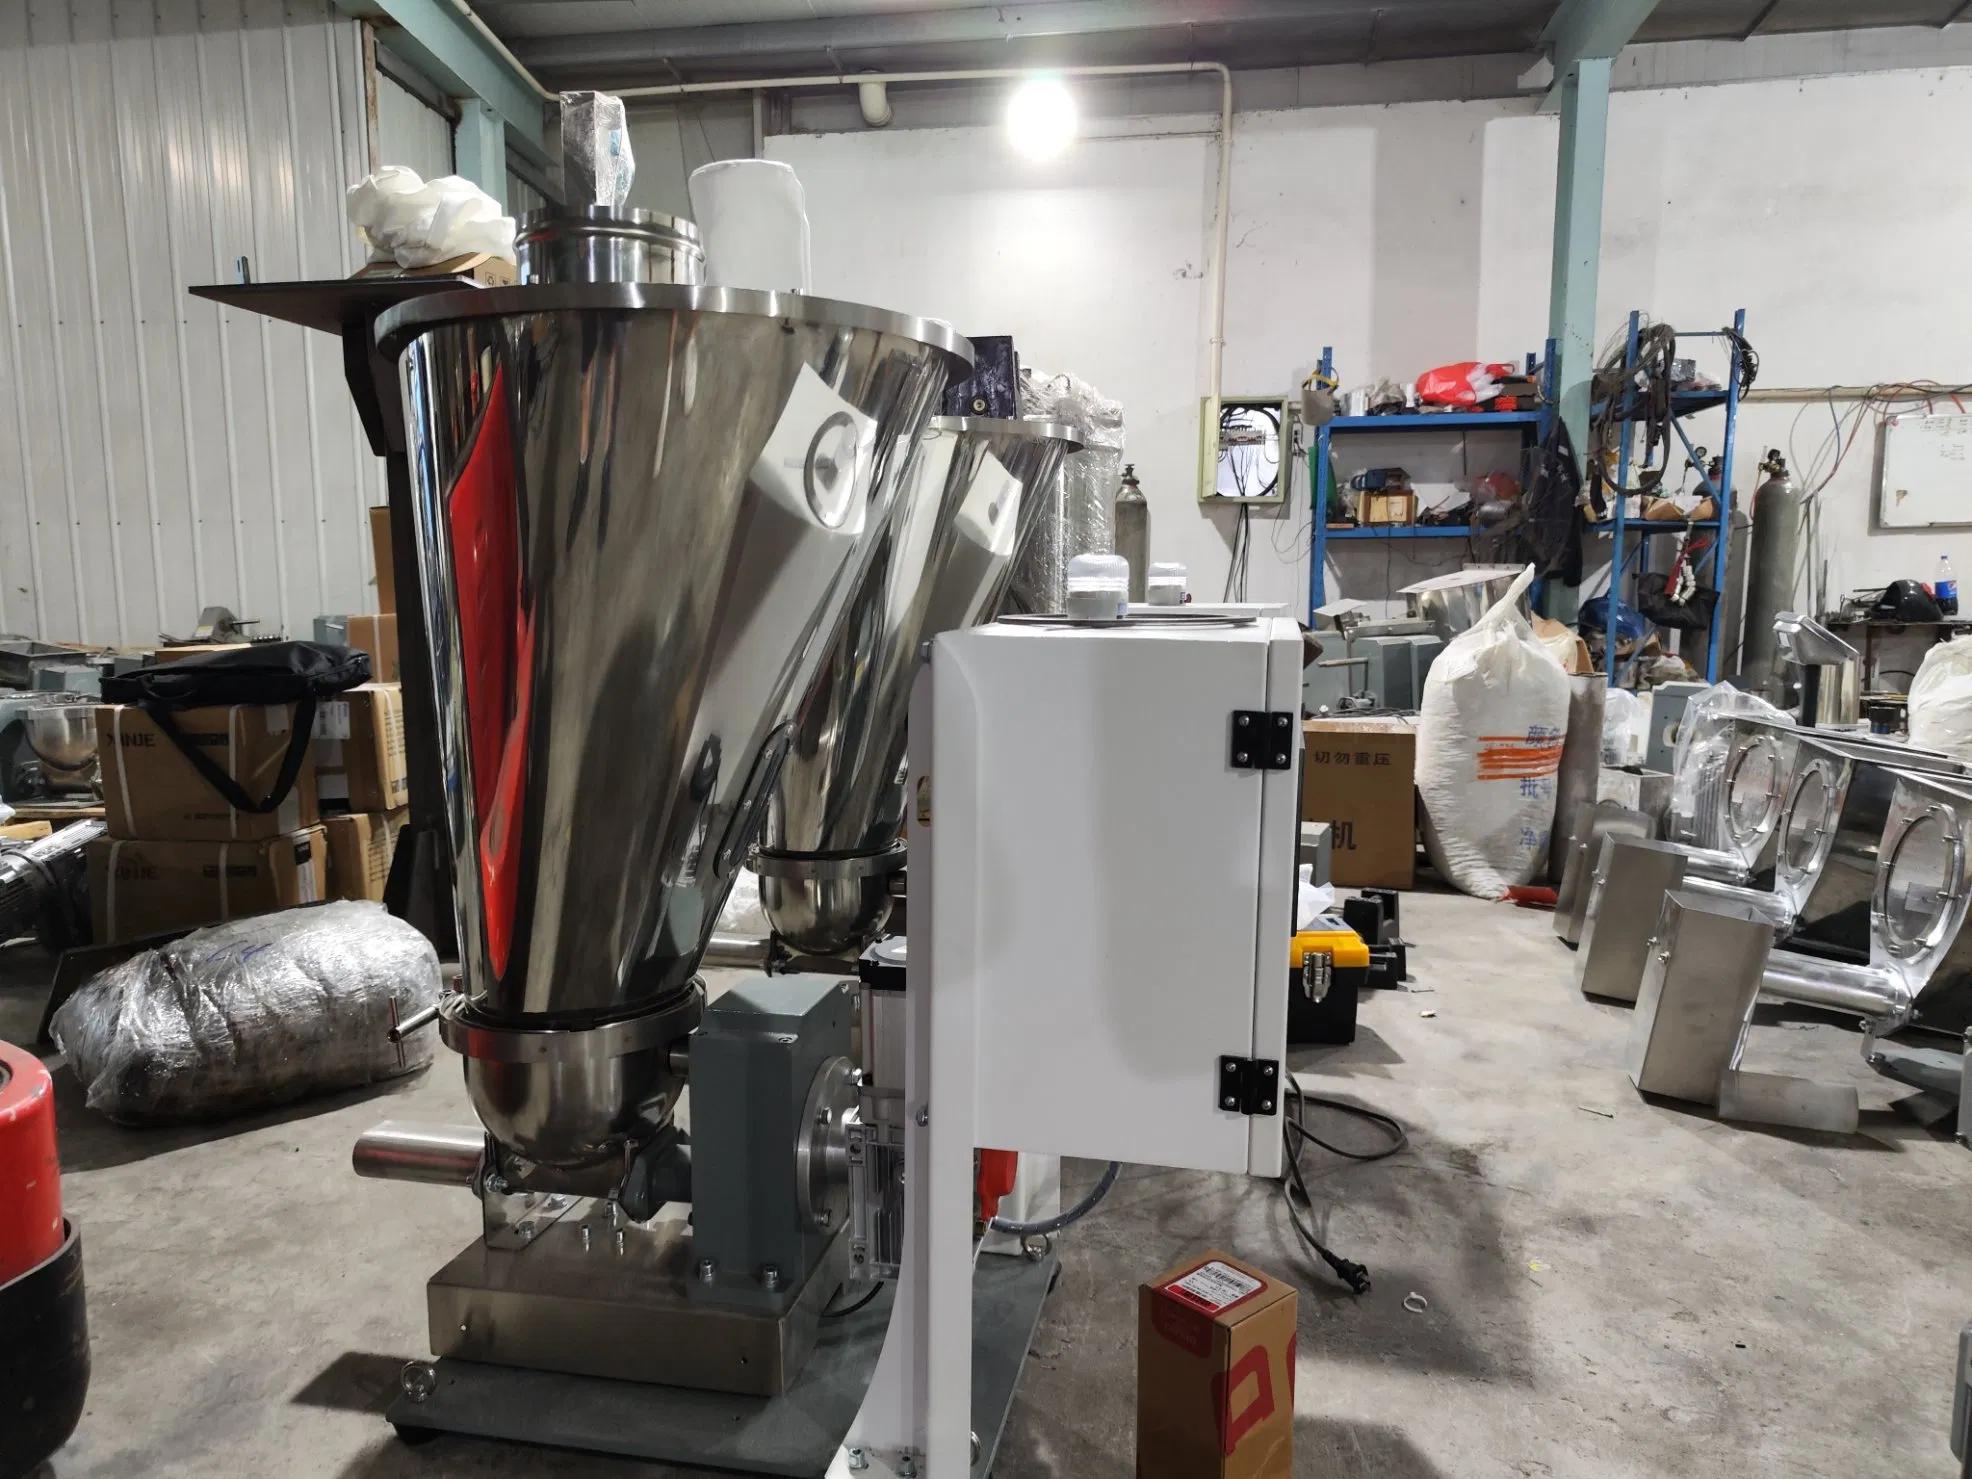
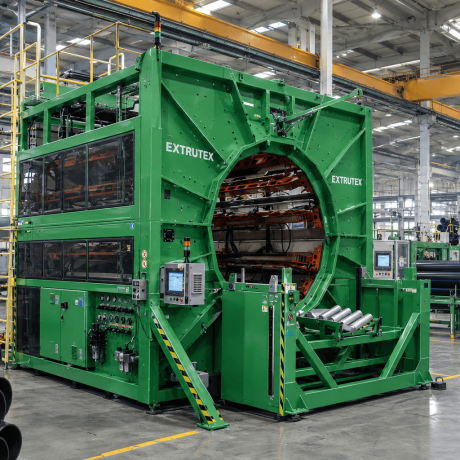
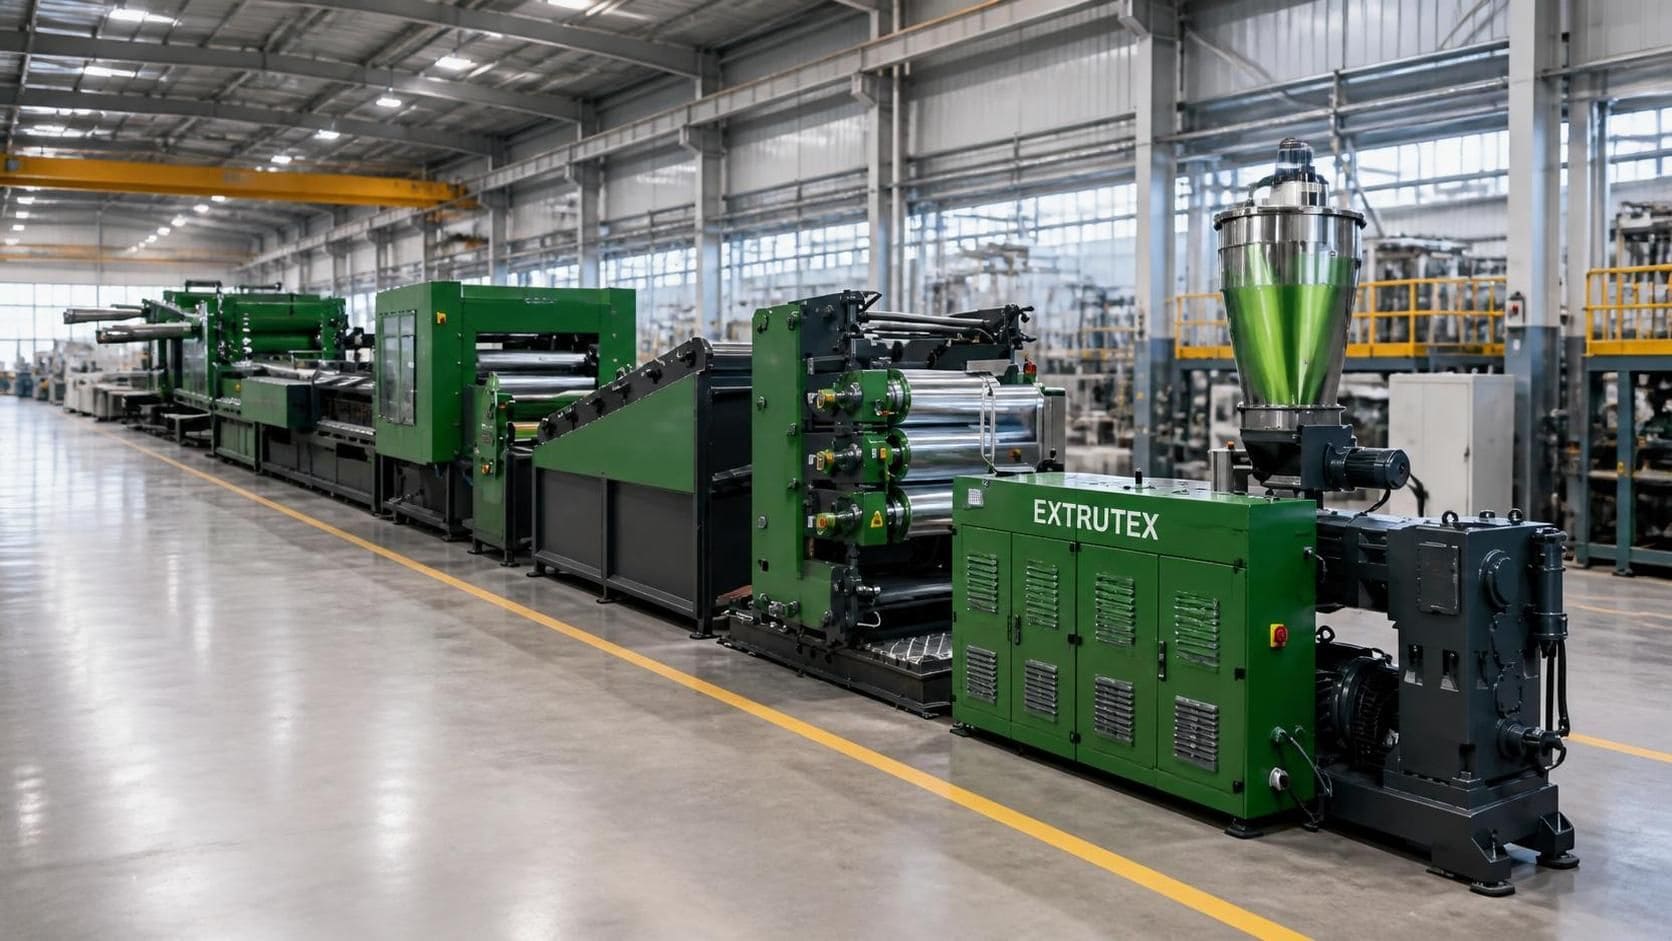
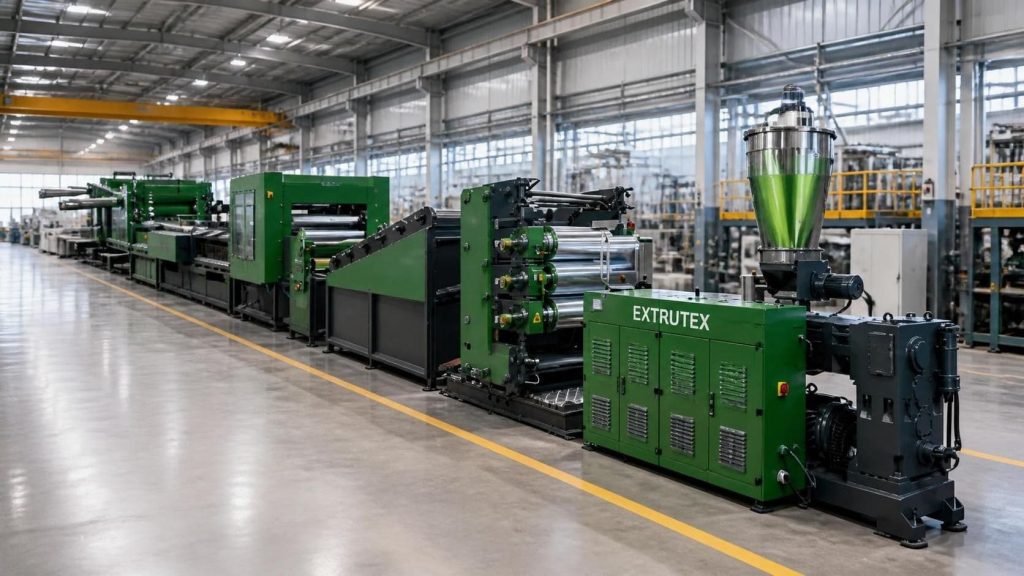
EXTRUTEX develops edge band extrusion lines according to each customer's product requirements, target output, selected polymer, and factory conditions. The complete line can include an extruder, extrusion tooling, cooling and vacuum calibration equipment where required, haul-off, cutting equipment, and a double winding unit. Additional equipment, such as gravimetric or volumetric dosing, co-extrusion, and primer application systems, can be considered according to the required product.
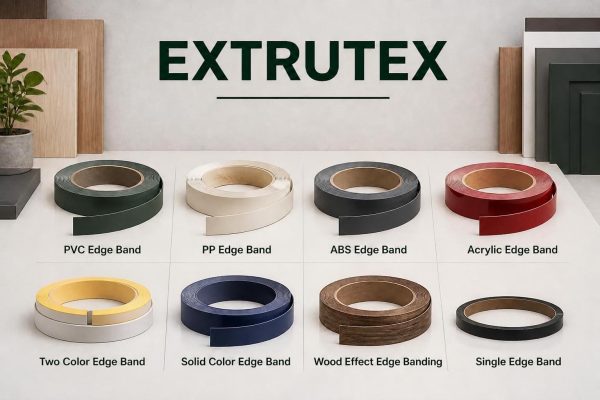
Whether you plan to manufacture standard solid-color PVC edge bands, decorative wood-effect products, two-color edge bands, flexible PP bands, ABS edge bands, or acrylic decorative strips, EXTRUTEX can help configure an extrusion solution around your intended production range.
Plastic edge bands are essential finishing materials for furniture and interior products. They cover exposed board edges, improve visual consistency, and help provide a neat transition between the panel surface and its edge.
The appropriate edge band material depends on the finished product, bonding method, required flexibility, surface appearance, chemical exposure, and expected service conditions. EXTRUTEX configures the extrusion line to suit the selected material and product specification.
Edge band production requires coordination between the extrusion process and the downstream equipment. The extruder must deliver a stable melt, while cooling, calibration, pulling, cutting, and winding must preserve the required product dimensions and appearance.
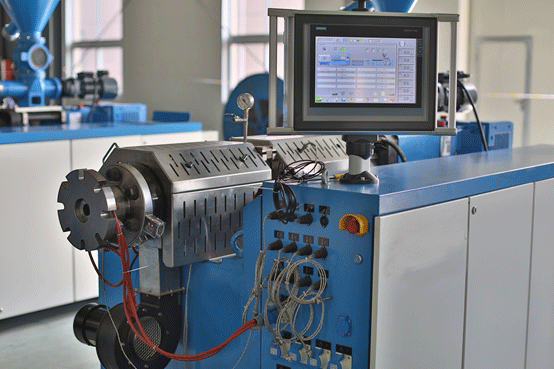
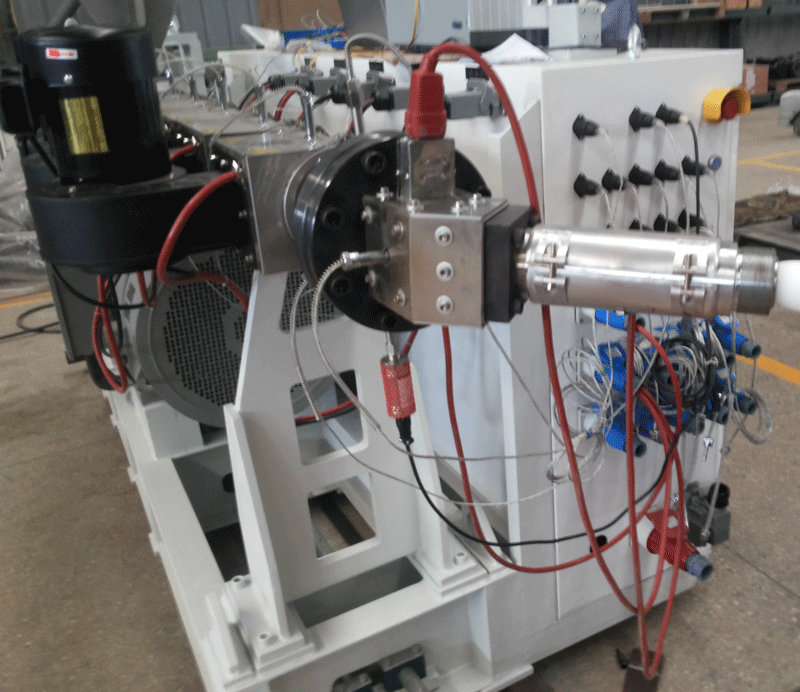
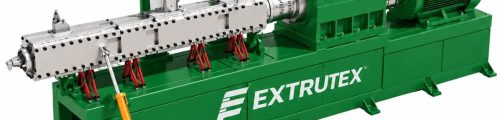
The extruder melts and homogenizes the polymer compound before delivering it to the die. Screw diameter, geometry, compression characteristics, mixing sections, and barrel design are selected according to the material, required output, and product dimensions.
EXTRUTEX can configure extrusion systems for different production capacities and edge band specifications. The screw and barrel design should be matched to the chosen formulation rather than assuming that one setup is optimal for every polymer family.
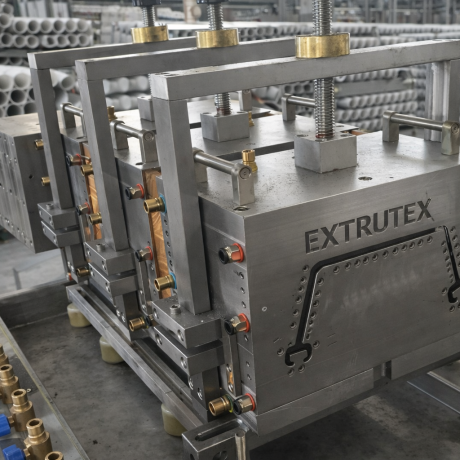
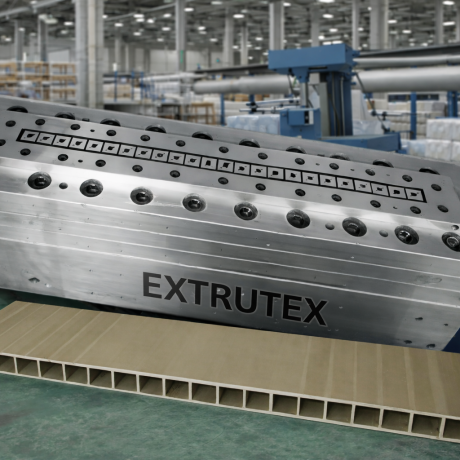
The die determines the initial shape and dimensions of the extruded edge band. Calibration and cooling equipment help stabilize the product as it leaves the die. Tooling can be designed for different widths, thicknesses, and product constructions, subject to the required tolerances and line configuration.
For direct extrusion of individual edge bands, the tooling can be designed with one or multiple extrusion openings, often referred to as single-eye or multi-eye configurations. The final tooling design depends on the cross-section, material flow, dimensional accuracy, and desired production output.
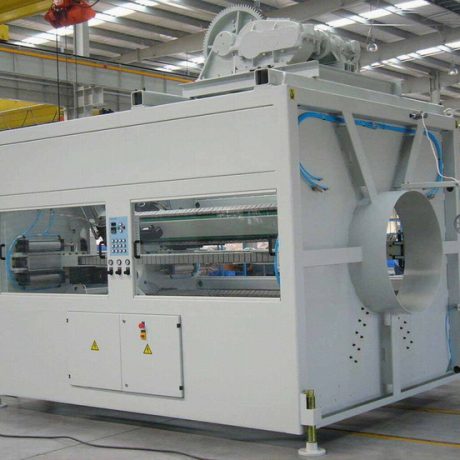
Cooling equipment reduces the temperature of the extruded material and helps it retain its intended dimensions. Vacuum calibration may be used where appropriate for the product geometry and process. Cooling length, water flow, vacuum conditions, and calibration surfaces must be matched to the material and profile.
The haul-off draws the edge band through the downstream section at a controlled speed. Stable pulling is important for maintaining thickness, width, and surface consistency. The haul-off must be synchronized with the extruder output to avoid excessive stretching or product deformation.
The cutting unit separates the continuous extruded product into the required lengths when cut-to-length collection is specified. Cutting parameters and equipment design depend on material flexibility, product dimensions, cutting accuracy, and the intended packaging method.
The double winder provides a practical solution for collecting suitable continuous edge bands onto rolls. Depending on the selected configuration, two winding positions can help operators prepare a new roll while managing the finished roll at the other position. Winding tension and roll dimensions should be controlled to avoid stretching, creasing, or damaging the product surface.
Standard line scope: The described complete production line includes the extruder, cooling and vacuum equipment, haul-off, cutting unit, and double winder. The extrusion die, dosing equipment, co-extruder, primer machine, printing equipment, and other optional units should be specified in the final quotation according to the selected product.
PVC is a widely used material for furniture edge banding because its formulation can be adjusted to provide different levels of rigidity, flexibility, color, surface finish, and processing characteristics. PVC edge bands are available for a wide range of furniture designs and production volumes.
The EXTRUTEX PVC edge band extrusion line is configured according to the selected PVC compound, product dimensions, and required output. Depending on the formulation, PVC edge bands can be manufactured in solid colors, decorative finishes, or other customized appearances.
Important process considerations include compound preparation, additive distribution, melt temperature, die flow, cooling, and dimensional stability. Suitable stabilizers, pigments, processing aids, and other additives must be selected for the intended application.
PVC products can be recyclable where appropriate collection and recycling facilities accept the material. Fire behavior is formulation-dependent, so flame-retardant or fire-performance claims should only be made when supported by the specific compound and applicable test results.
Polypropylene (PP) is an alternative material for selected edge band applications. It can offer useful chemical resistance and flexibility, depending on the polymer grade and formulation. These properties can make PP attractive for certain furniture components, kitchen applications, and products requiring curved or rounded edge designs.
Compared with other edge band materials, PP may require different processing temperatures, shrinkage control, surface treatment, and bonding considerations. Adhesion to the furniture panel is particularly important: the edge band and the selected adhesive or bonding process must be compatible.
EXTRUTEX can configure a PP edge band production line according to the intended width, thickness, color, output, and downstream handling requirements. Screw design, die configuration, cooling conditions, and haul-off settings should be selected for the specific PP grade.
Acrylonitrile butadiene styrene (ABS) is widely used in furniture edge banding where a combination of impact performance, surface quality, and dimensional stability is desired. ABS edge bands can be manufactured in solid colors and decorative designs for cabinets, wardrobes, desks, shelving, and other furniture products.
ABS does not contain chlorine in its polymer structure, unlike PVC. However, environmental performance depends on the full formulation, manufacturing process, product lifetime, and end-of-life management. ABS should not automatically be described as more environmentally friendly without considering these factors.
ABS also has different thermal and processing characteristics from PVC and PP. EXTRUTEX therefore selects the extrusion configuration according to the intended ABS grade, required output, and finished edge band specification.
Acrylic-based edge band products, often associated with PMMA or multilayer decorative constructions, are selected for applications where appearance, surface clarity, decorative depth, or resistance to everyday wear is important. Depending on the design, acrylic edge bands can create a distinctive visual effect for contemporary furniture and interior panels.
The exact structure of an acrylic edge band can vary. Some products use acrylic as a principal material, while others combine decorative or functional layers. The extrusion line and tooling must be designed around the actual construction and the thermal properties of the selected materials.
EXTRUTEX can assess acrylic edge band production requirements based on product drawings, material specifications, target output, and desired surface quality. If multiple layers are required, the feasibility of co-extrusion or other production methods should be confirmed during technical evaluation.
Solid-color edge bands are commonly used in furniture production to match, contrast with, or complement the surface of a board. Consistent color is essential when manufacturers need to maintain visual uniformity across large production batches.
EXTRUTEX can incorporate a suitable pigment dosing system into the production line where required. Correct dosing, mixing, temperature control, and raw material consistency help reduce color variation. The final result also depends on pigment selection, polymer formulation, and the product's surface finish.
Two-color edge bands combine two colors or visual zones within one product. They can be used for decorative effects, contrast detailing, or specific furniture design requirements.
For suitable product designs, EXTRUTEX can assess a co-extrusion configuration that combines two material streams through compatible tooling. Stable output requires attention to the rheology of both materials, melt temperature, flow balance, and bonding between the layers or color zones.
Wood-effect edge bands are used to coordinate furniture panel edges with woodgrain surfaces, including oak, walnut, and other decorative patterns. These products help create a consistent appearance across panel faces and edges.
A complete decorative process may combine extrusion with printing or other surface-finishing operations. A primer application system can help prepare a compatible surface for a subsequent printing process, but the primer must be matched to the substrate, ink, and printing technology. Color accuracy also depends on ink formulation, print settings, surface preparation, and quality control.
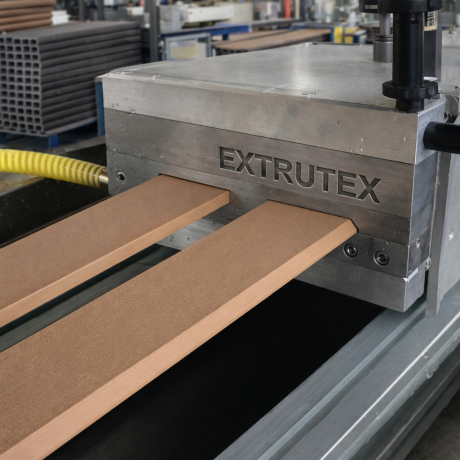
Some manufacturers prefer to extrude individual edge bands directly rather than producing a wider sheet that is later slit into narrower strips. Direct extrusion can be useful when a product requires a specific cross-section, rounded edges, or a defined profile shape.
EXTRUTEX can evaluate single-opening and multi-opening tooling options according to the product design and target output. The feasibility and productivity of each arrangement depend on the band dimensions, material behavior, cooling requirements, and tooling layout.
Decorative printing is an important part of many edge band production processes. Woodgrain, stone-effect, and customized graphic patterns allow manufacturers to coordinate edge bands with furniture surfaces and create a distinctive product appearance.
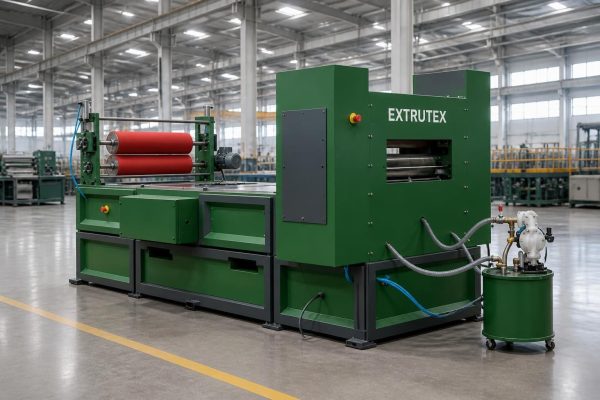
The EXTRUTEX edge band primer machine can be considered as part of a suitable printing preparation system. Primer is applied to prepare the material surface for the selected printing process. The correct primer depends on the polymer, surface condition, ink chemistry, and printing method.
Primer application alone does not guarantee printing adhesion or color accuracy. Customers should validate the primer, ink, substrate, and curing or drying conditions together before full-scale production. Printing equipment, ink systems, and drying units should be included in the quotation if a complete printing line is required.
The screw and barrel are among the most important components of an edge band extruder. Their design affects feeding, melting, mixing, pressure generation, temperature distribution, and output stability.
EXTRUTEX specifies screw and barrel configurations according to the polymer family, compound formulation, required production rate, and final product dimensions. Material selection and surface treatment should be confirmed in the technical documentation to match the intended service conditions.
For applications requiring nitrided steel, EXTRUTEX can discuss the relevant steel grade and treatment specifications with the customer. The reference to DIN 8550 nitrided steel and a screw hardness target of 65–70 HRC should be confirmed against the actual component material, heat-treatment process, and final inspection documentation before being treated as a guaranteed specification.
EXTRUTEX configures extrusion lines for different polymer types, product widths, thicknesses, colors, and output targets. The final machine arrangement is selected according to the customer's product requirements and production objectives.
Appropriate motor sizing, inverter control, heating management, and coordinated downstream operation can help reduce unnecessary energy use. Actual consumption depends on the polymer, production rate, installed equipment, and factory operating conditions.
A practical control arrangement allows operators to monitor and adjust important production parameters. Clear operating procedures and suitable training help support repeatable production and efficient changeovers.
Depending on the product, the line can be configured with single extrusion, co-extrusion, dosing, cooling and vacuum calibration, haul-off, cutting, winding, and optional primer or printing preparation equipment.
EXTRUTEX considers material behavior, die design, cooling requirements, product tolerances, and collection method when preparing a proposed line. This helps align the equipment with the actual manufacturing process rather than relying only on nominal machine capacity.
Before selecting equipment, manufacturers should define the intended product range and production targets. The following information helps EXTRUTEX recommend a suitable configuration:
A product sample, technical drawing, or material data sheet can help clarify the tooling and process requirements. Production capacity and final equipment specifications should be confirmed after reviewing the intended product range.
EXTRUTEX can supply lines for these material families, but one configuration should not be assumed to process all of them optimally. Compatibility depends on the specific grades, screw and barrel design, temperature range, tooling, and changeover requirements. Confirm all intended materials before ordering.
Yes, a suitable co-extrusion configuration can be considered for compatible two-color product designs. The number of extruders and the die arrangement depend on the required construction.
The basic extrusion line includes the extruder, cooling and vacuum equipment, haul-off, cutting unit, and double winder. A primer machine and printing equipment are additional systems and should be specified separately if required.
EXTRUTEX can assess an extrusion and finishing configuration for wood-effect edge bands. The required printing or decorative process depends on the substrate and desired appearance.
Direct single-band extrusion can be considered using suitable tooling. Single-opening or multi-opening arrangements depend on the product geometry, output target, and cooling requirements.
EXTRUTEX manufactures plastic edge band extrusion lines for furniture component producers seeking solutions for PVC, PP, ABS, and acrylic-based edge band products. From solid-color bands to decorative wood-effect and two-color products, the equipment configuration can be developed around your material, dimensions, production target, and finishing requirements.
Contact EXTRUTEX with your product drawings, material details, desired capacity, and preferred downstream process. Our team can evaluate a suitable line configuration, including extrusion, cooling and vacuum equipment, haul-off, cutting, double winding, and optional dosing, co-extrusion, or primer systems.
EXTRUTEX — Edge Band Extrusion Solutions for Modern Furniture Manufacturing.
There are no reviews yet.
By submitting your email, you agree to our company’s terms and conditions.
We are not looking to sell; we are here to provide you with the best support and service.
Contact available 24/7
Please do not contact us for advertising or sales inquiries
All rights of this website are reserved for EXTRUTEX Austria and its partner companies, © 2026
-
(0 customer reviews)