Food Extruder Parts and Food-Grade Twin-Screw Extruder Components
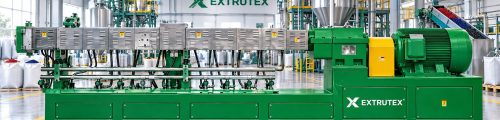
EXTRUTEX manufactures replacement screw elements, kneading blocks, screw shafts, barrel sections and wear components for food and feed twin-screw extruders. We have manufactured replacement parts for machines from Bühler, Baker Perkins, Clextral, Wenger and ANDRITZ, and can assess spare-part requirements for most other food and feed extrusion machine brands against original drawings, technical specifications or physical samples.
Food extrusion requires a different approach from conventional plastics compounding. Moisture content, cooking intensity, product texture, temperature, residence time and cleaning requirements all influence the design of the screw assembly. A replacement component must not only fit the machine; it must also be appropriate for the product, process conditions and hygiene requirements.
EXTRUTEX manufactures parts to customer drawings or dimensions established from original components. Depending on the machine and application, we can work with stainless steels, specified corrosion-resistant materials, wear-resistant alloys and suitable surface treatments. Screw diameters from 7 to 486 mm can be assessed, subject to the required machine geometry and manufacturing specification.
Independent replacement-parts manufacturer: EXTRUTEX is not affiliated with, authorised by or an approved supplier to the OEMs named on this page. Manufacturer and machine names are used only to identify equipment for which replacement components may be assessed and manufactured.
Food and Feed Extruder Brands We Can Support
EXTRUTEX has manufactured replacement components for food and feed extrusion equipment from several established international machine manufacturers. We can also assess parts for other brands, including older machines, regional manufacturers and equipment where original spare parts are difficult to obtain.
Part numbering, screw geometry and shaft connections vary between manufacturers and machine generations. For this reason, we confirm the dimensions and component arrangement before machining. The following directory includes established food and feed extrusion manufacturers and additional machine brands that can be considered for model-specific enquiries.
International food and feed extrusion manufacturers
BühlerBCTM, BCTA, PolyTwin, EcoTwin, CompacTwin and Nutrex platforms
Baker PerkinsMPF and SBX food extrusion platforms
ClextralBC and EVOLUM twin-screw extruders
WengerTX, Magnum and other food and feed extrusion systems
ANDRITZFood, pet food and aquafeed extrusion equipment
CoperionFood, feed and specialist twin-screw extrusion platforms
GEAFood and pet food extrusion systems; model verification required
Extru-TechPet food, aquatic feed and food extrusion equipment
American Extrusion InternationalFood and feed extrusion machinery
The Bonnot CompanySpecialist food and industrial extrusion equipment
Diamond AmericaFood, feed and specialist extrusion machinery
CPMCentury Extrusion and related processing platforms
Amandus KahlFeed processing and extrusion-related machinery
FAMSUNFeed, aquafeed and pet food extrusion systems
IDAHAquafeed, pet food and food processing extrusion equipment
BrabenderLaboratory and pilot-scale extrusion equipment
Schaaf TechnologieSpecialist food and industrial extrusion equipment
Reading Bakery SystemsSnack and food processing machinery; configuration dependent
PavanPasta and food processing extrusion systems
Extrusion-LinkFood and feed extrusion equipment and complete lines
Labtech EngineeringLaboratory and pilot-scale extrusion systems
TechnovelSpecialist twin-screw extrusion equipment
LeistritzLaboratory and specialist twin-screw platforms
STEERTwin-screw extrusion equipment; application verification
Additional Chinese and Asian food and feed extruder manufacturers
FAMSUN / MuyangFeed, pet food and aquafeed production machinery
Jinan DarinPet food and snack extrusion equipment
Shandong LightFood and feed processing extrusion machinery
Shandong SainaFood and feed extrusion machinery
Shandong ArrowFood and pet food processing equipment
Jinan SaibainuoFood and snack extrusion machinery
Jinan SunwardFood and feed extrusion equipment
Jinan MeitengFood and pet food extrusion machinery
Yeong MingFood processing and extrusion equipment
Chia TungFood processing and extrusion machinery
Five Continents MachineryFood and feed processing equipment
ExtrugroupExtrusion machinery; confirm exact food application
This is a non-exhaustive manufacturer directory. Some companies listed manufacture single-screw extruders, complete food-processing lines or specialist laboratory machines rather than the same type of co-rotating twin-screw extruder. EXTRUTEX evaluates the exact machine and component before confirming manufacturing feasibility.
Food Extruder Spare Parts We Manufacture
1. Food-grade screw elements
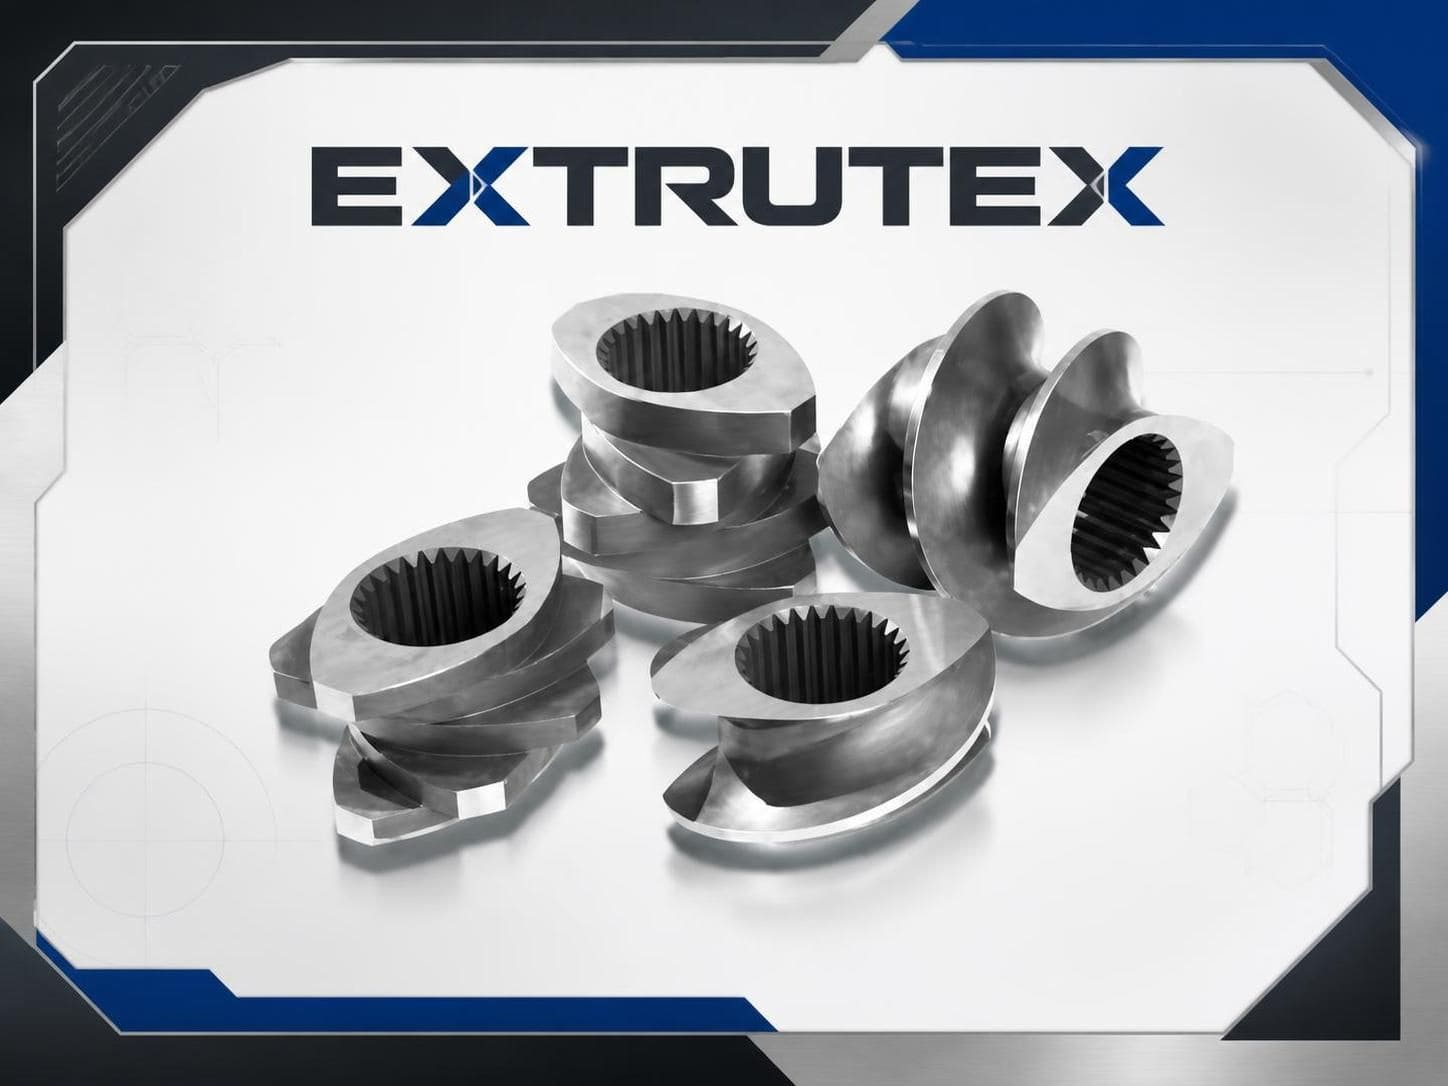
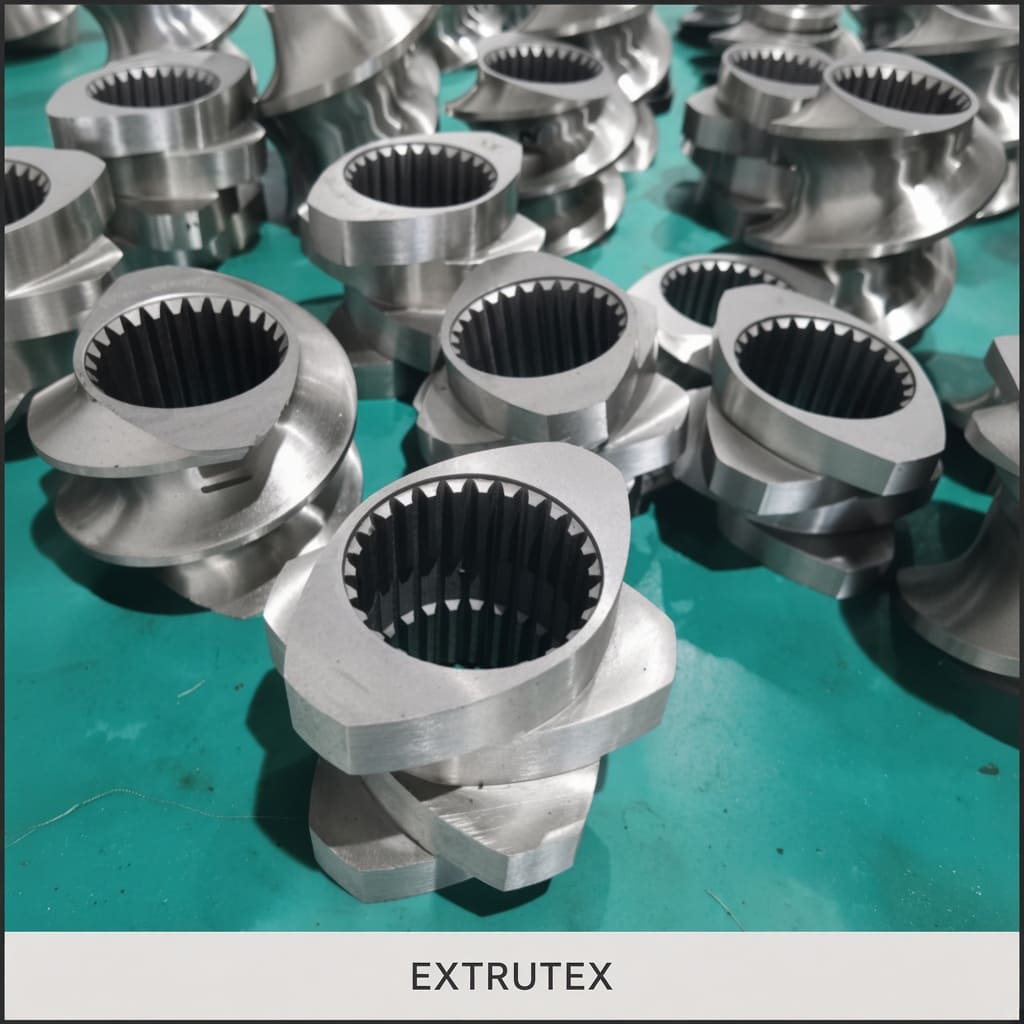
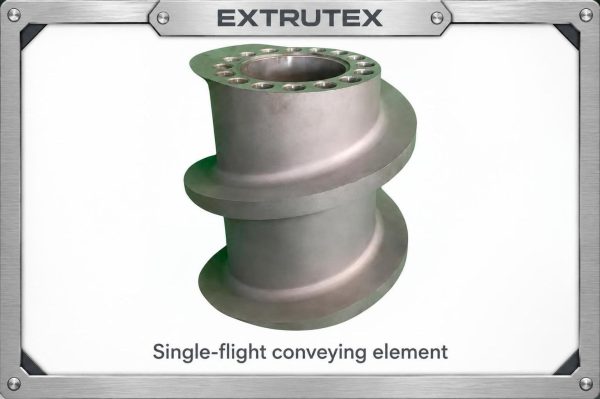
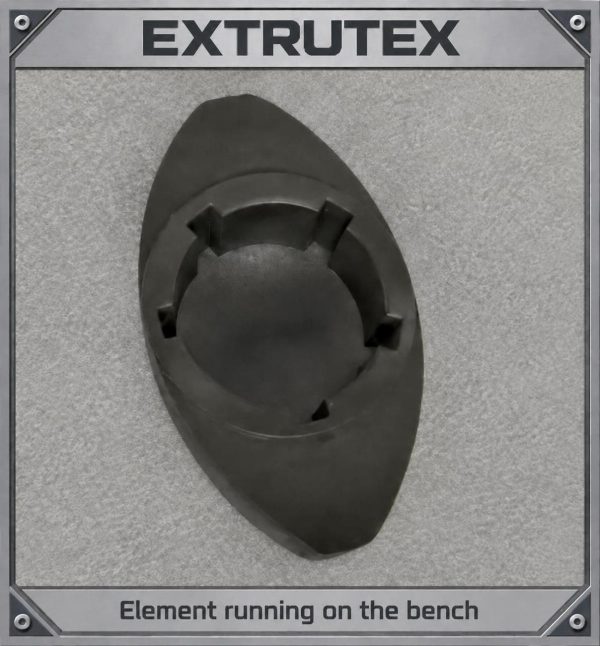
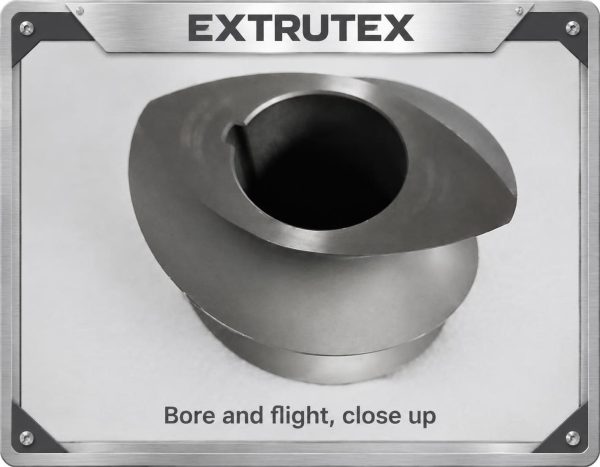
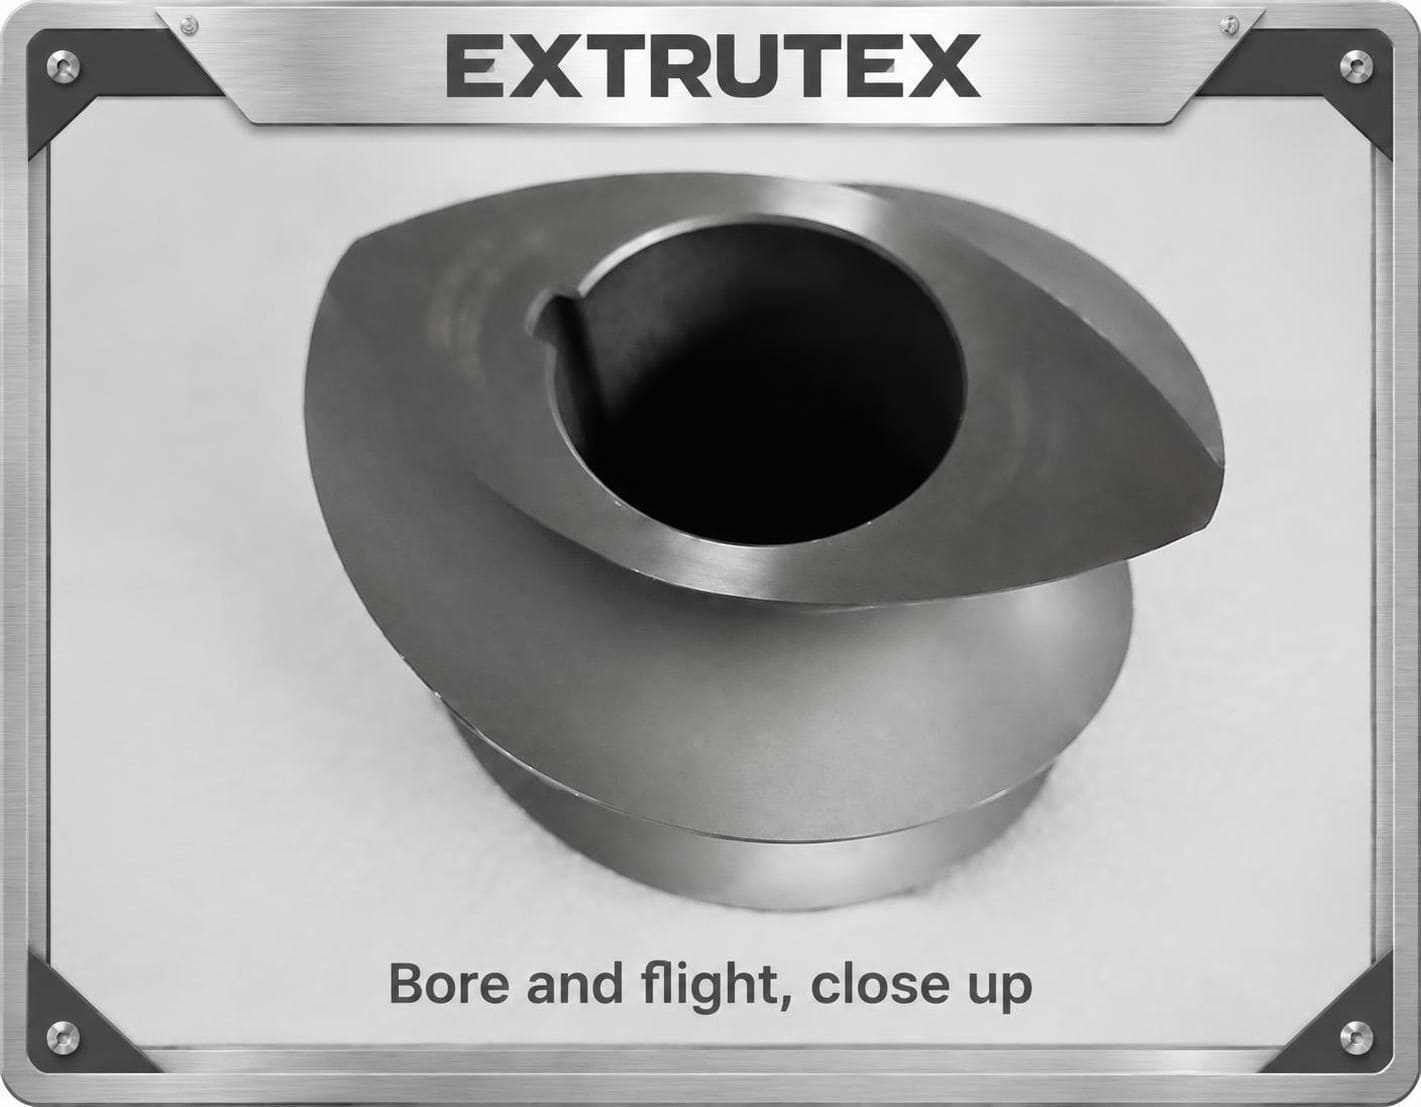
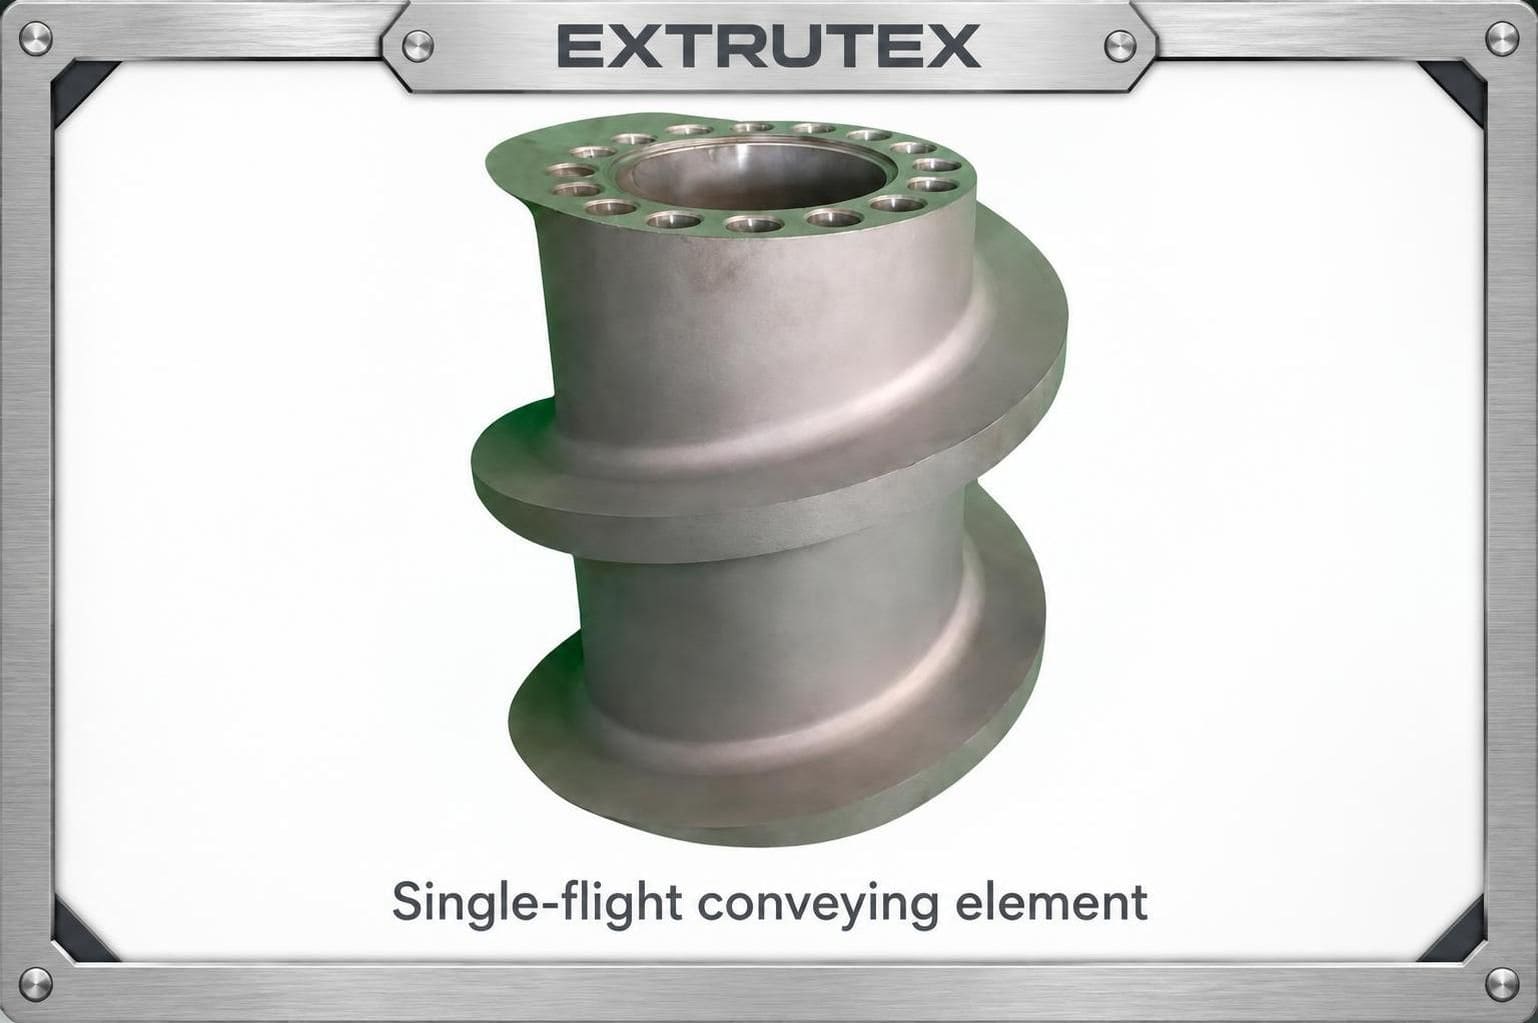
We manufacture single-flight and double-flight conveying elements and other modular screw components for food and feed extrusion equipment. Each element is produced to the specified outside diameter, internal connection, pitch, flight profile and axial length.
- Single-flight conveying elements.
- Double-flight conveying elements.
- Long-pitch and short-pitch conveying elements.
- Mixing and distributive mixing elements.
- Reverse conveying elements where specified.
- Special-purpose screw elements for food and feed processing.
Product-contact surfaces require suitable material selection and finishing. The required surface finish, corrosion resistance and cleanability should be defined according to the machine design and the food-processing application.
2. Kneading blocks
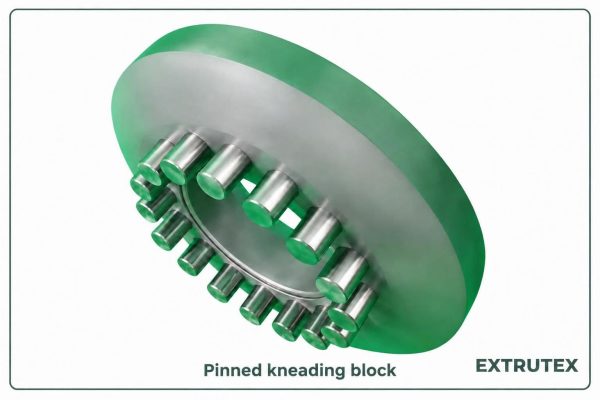
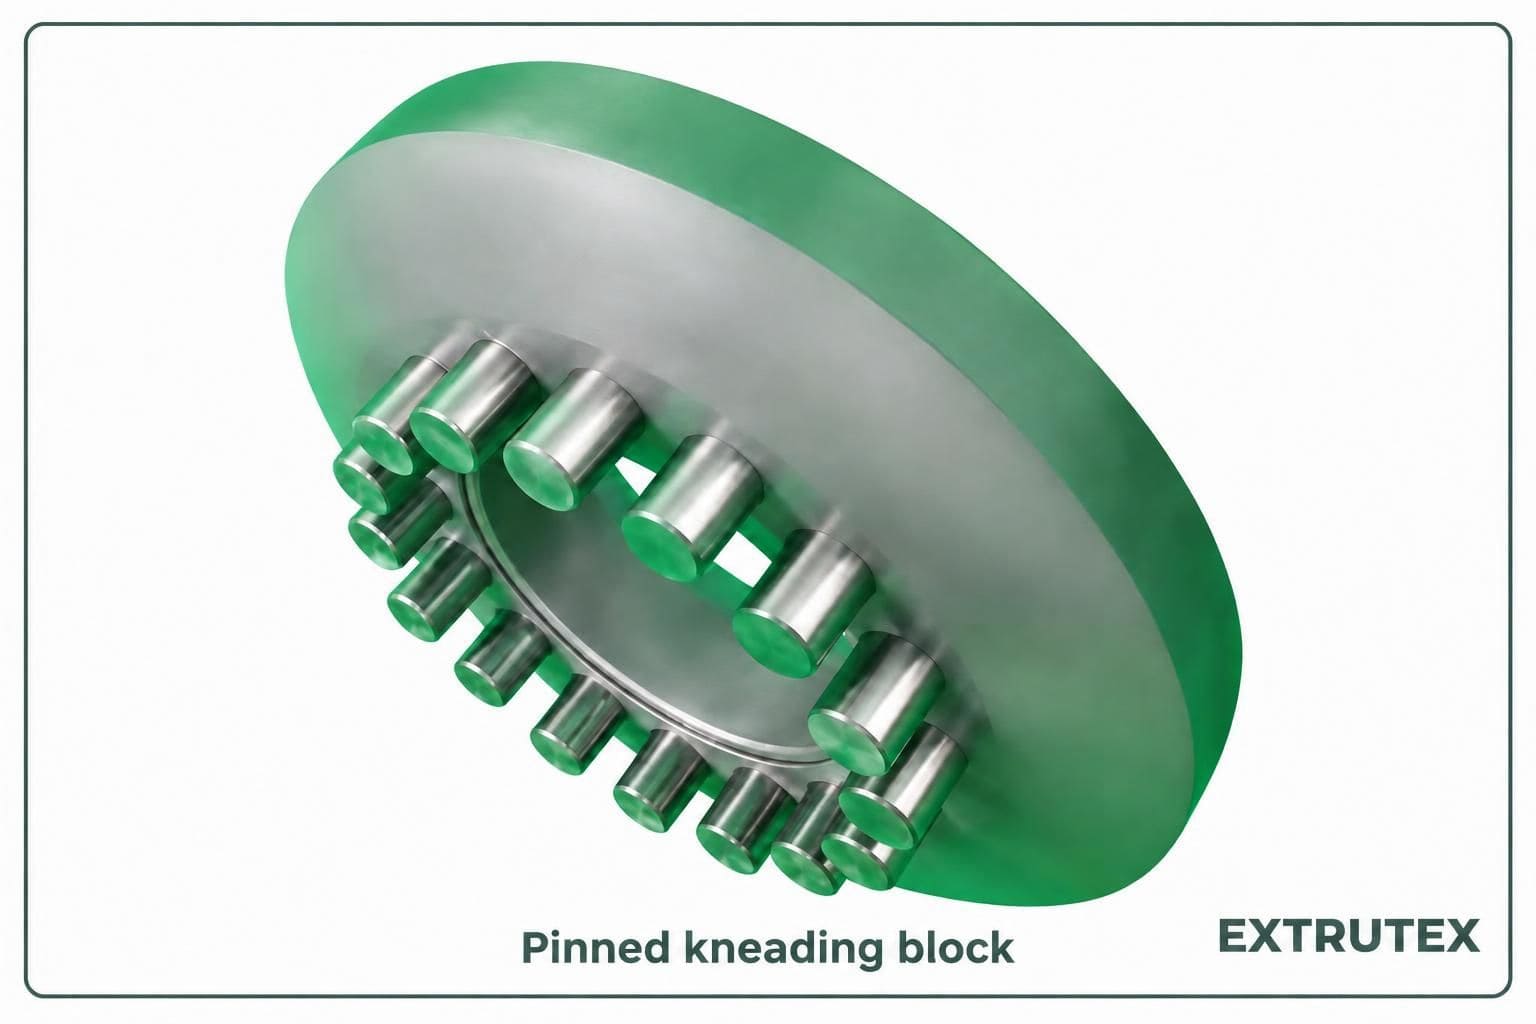
Kneading blocks are assembled from discs with defined thicknesses and stagger angles. In food extrusion, their role is to support the required cooking, hydration, mixing and texturisation process. The correct arrangement depends on the recipe and the target product properties.
- 30-degree stagger kneading blocks.
- 45-degree stagger kneading blocks.
- 60-degree stagger kneading blocks.
- 90-degree stagger kneading blocks.
- Pinned and specialised mixing blocks where required.
- Custom disc thicknesses and element arrangements.
The stagger angle alone does not determine the cooking result. Disc thickness, element sequence, screw speed, moisture, temperature and throughput all influence the process. Replacement blocks should follow the original screw configuration or an approved process design.
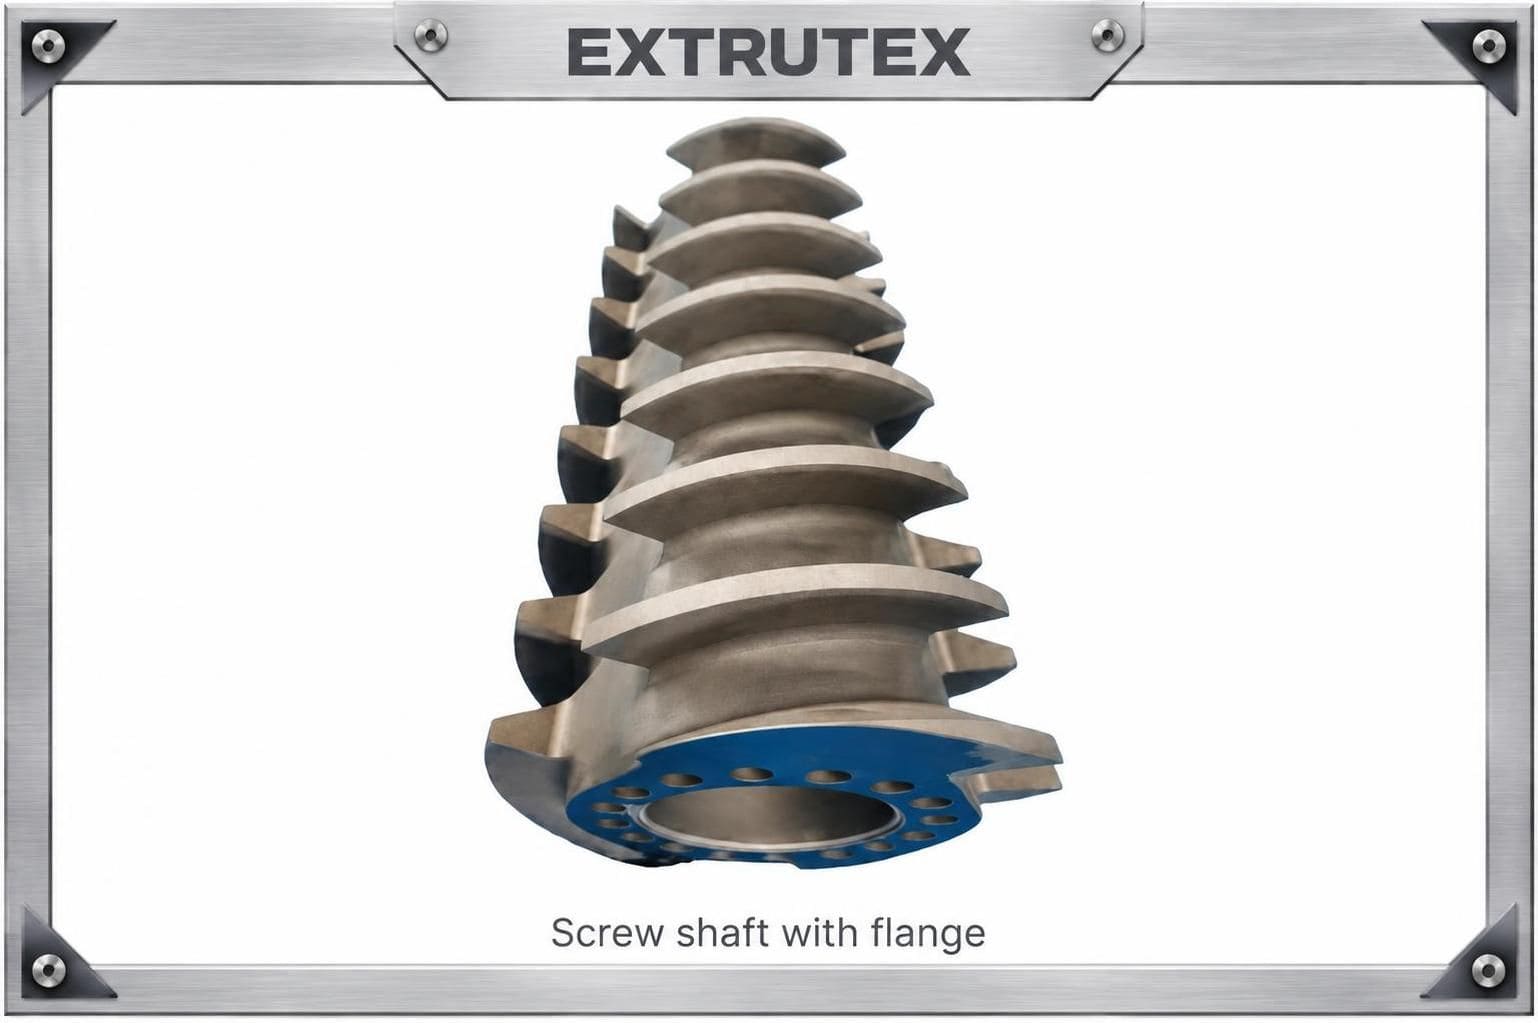
3. Screw shafts
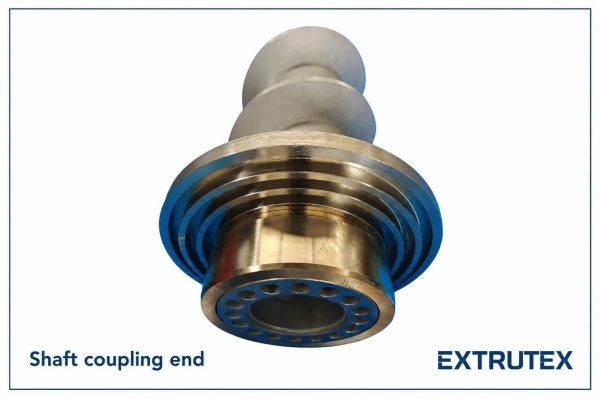
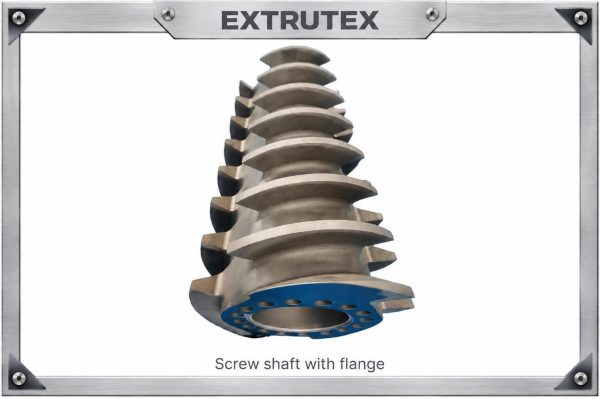
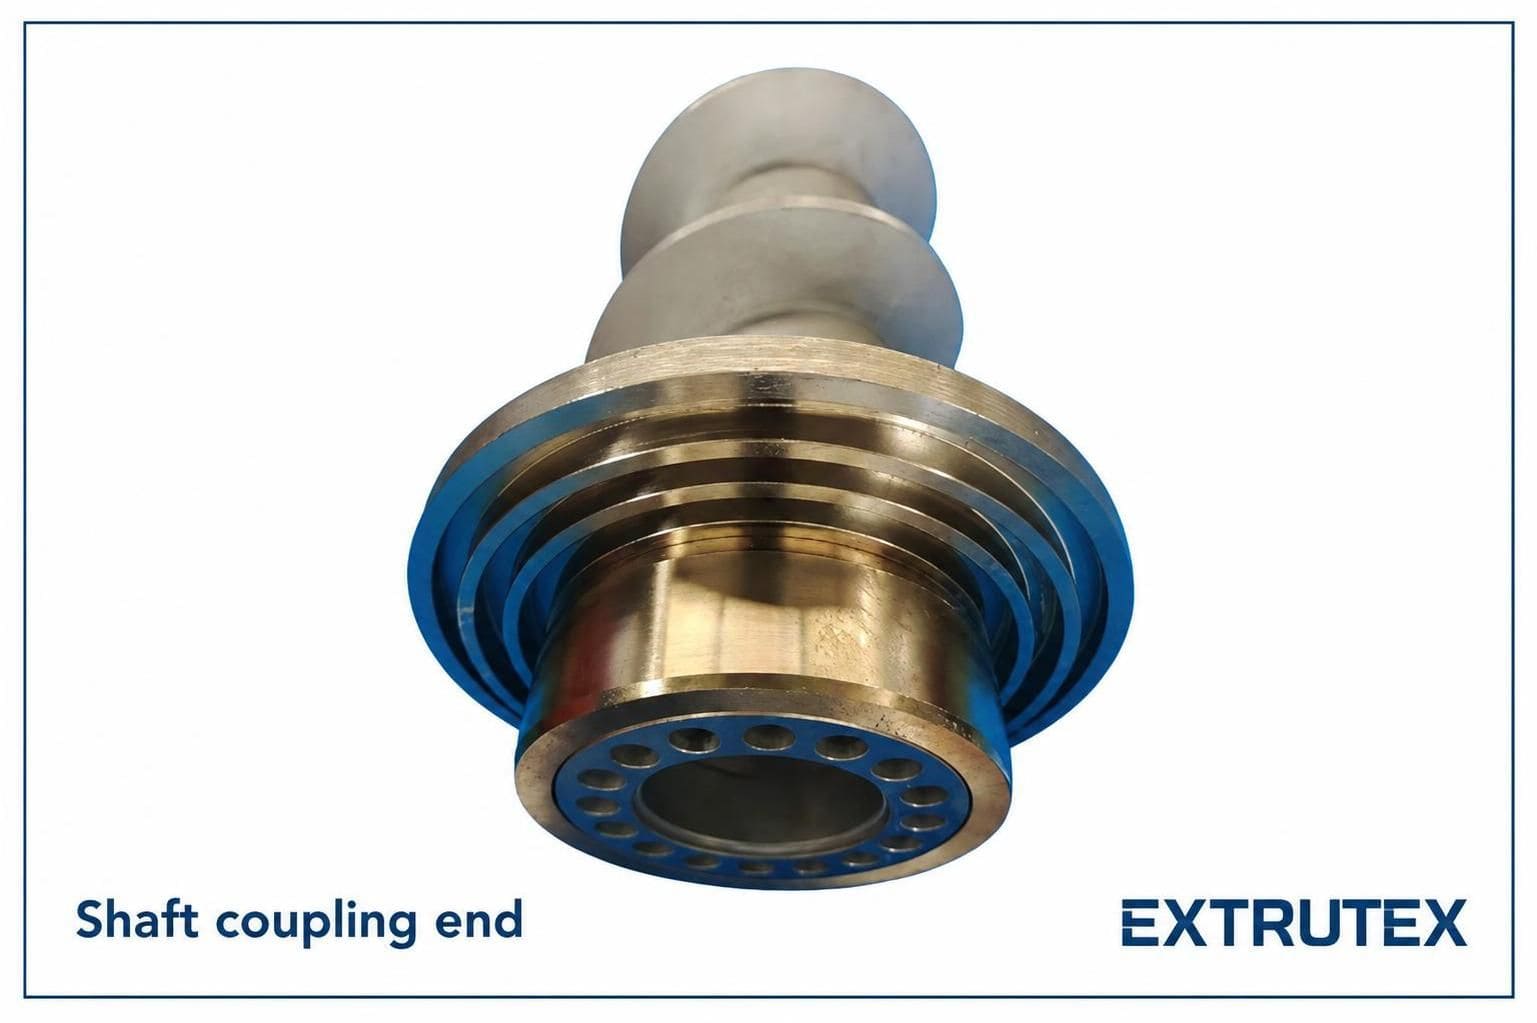
EXTRUTEX manufactures replacement screw shafts for modular twin-screw assemblies. Shaft dimensions and coupling geometry must match the existing gearbox and screw-element arrangement.
- Splined screw shafts.
- Keyed screw shafts.
- Custom drive and coupling ends.
- Single and paired shaft assemblies.
- Replacement shafts manufactured to OEM drawings or approved samples.
Depending on the design and location, shaft materials may include 40CrNiMo, H13 or WR15E. These are engineering material options, not automatic food-contact material approvals. Where a shaft or component can contact the product, the material and surface condition must be separately confirmed as suitable for the intended application.
4. Barrels and barrel liners
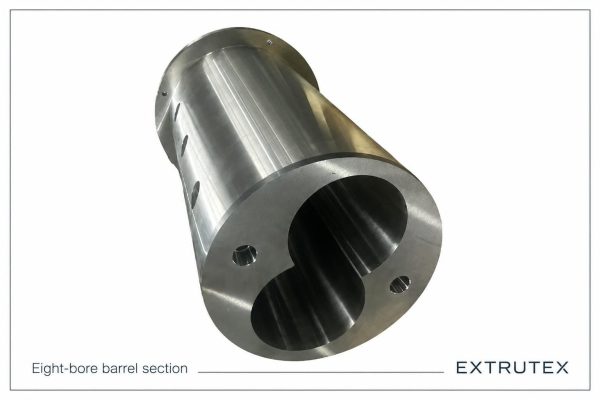
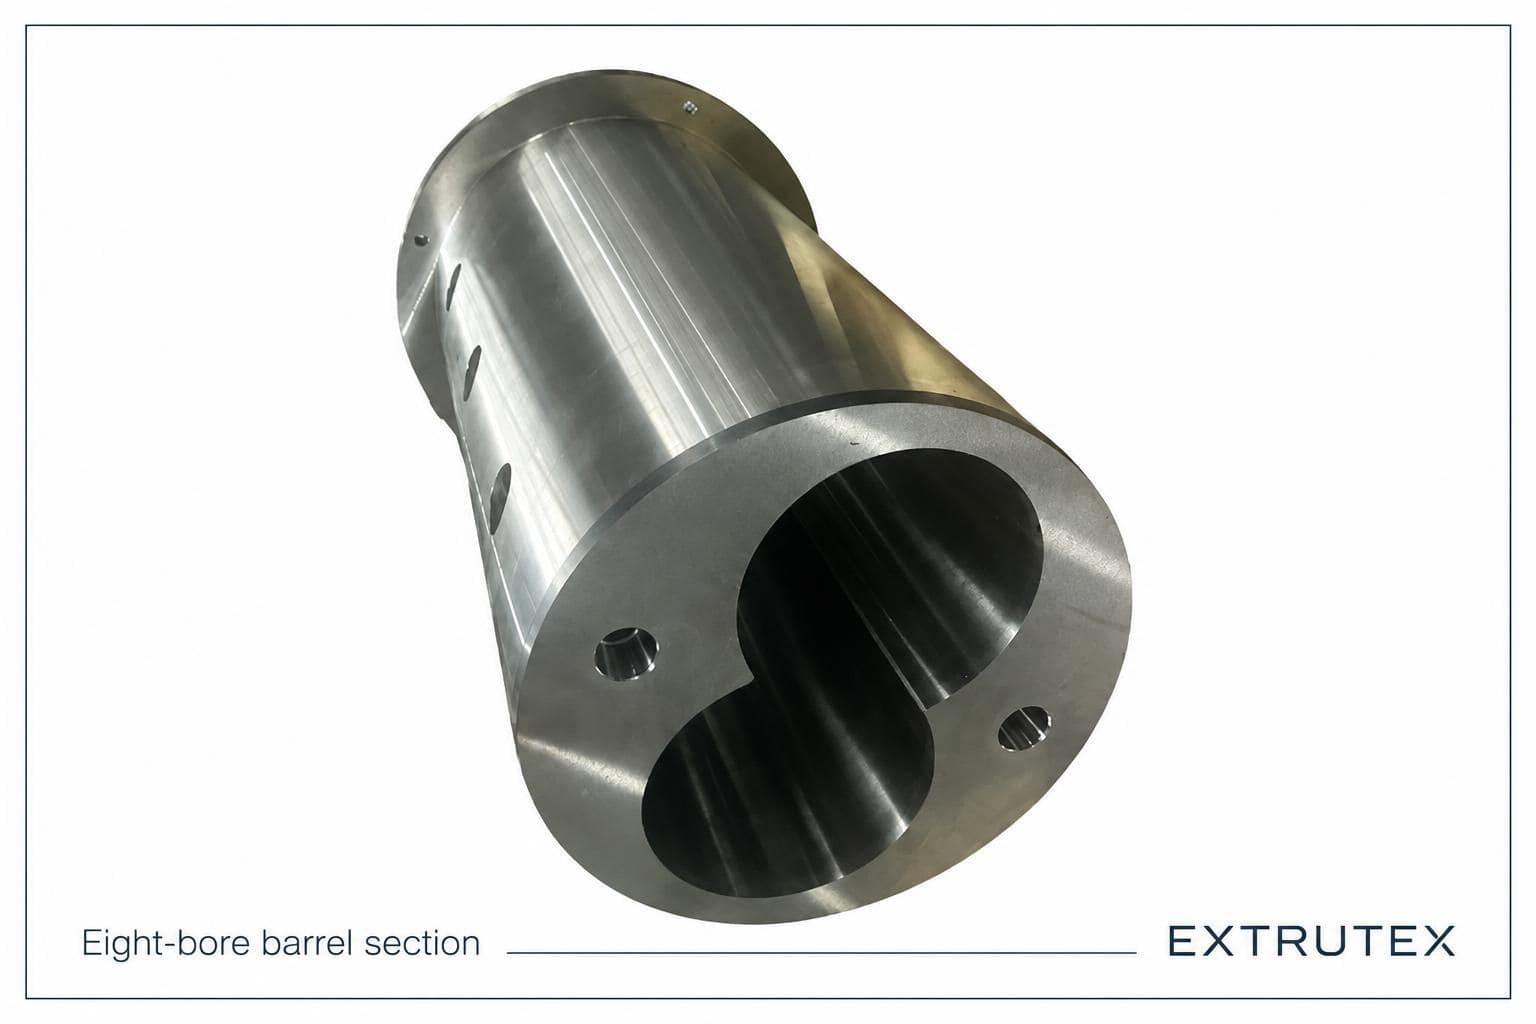
We manufacture and assess replacement barrel sections and liners for food and feed twin-screw extruders. The barrel bore must maintain the correct geometry and working clearance with the screw assembly.
- Figure-8 barrel sections.
- Feed and conveying barrel sections.
- Venting and degassing sections.
- Closed barrel sections.
- Replaceable barrel liners.
- Wear-resistant and corrosion-resistant bore solutions.
- Custom barrel sections manufactured to drawings or samples.
Polished or plated bores, nitrided surfaces, powder-metallurgy liners and other wear-resistant constructions can be assessed according to the product-contact position and application. Any material, plating or coating that contacts food must be suitable for the intended food-contact conditions and supported by the required documentation.
Why Food Extruder Parts Are Different from Plastics Compounding Parts
Food and feed extrusion may use a similar modular screw arrangement to polymer compounding, but the operating conditions and hygiene requirements can be very different. A replacement part must be designed around the actual process rather than selected only because its dimensions appear similar.
Controlled cooking and shear
In plastics compounding, screw elements are often selected to disperse fillers, break down agglomerates and distribute additives. Food extrusion has different objectives. The screw assembly manages hydration, mixing, cooking, starch transformation, protein texturisation and product expansion.
Excessive mechanical energy can damage texture, cause unwanted product degradation or create local overheating. The kneading arrangement must therefore match the required process conditions. Copying a screw stack from a plastics compounding line is not a reliable way to design a food extrusion screw assembly.
Moisture and corrosion resistance
Food and feed extrusion processes can operate with a broad range of moisture levels. The required water content depends on the product, recipe, preconditioning and extrusion technology. Moisture exposure, cleaning chemicals and temperature cycles can create corrosion risks for unsuitable materials.
Some mineral-rich feed formulations, bone meal, mineral premixes and abrasive aquafeed ingredients can also increase wear. Material selection must consider both corrosion and abrasion rather than treating them as the same problem.
Cleanability and hygienic design
Food-contact components must be designed and finished so that they can be cleaned effectively. Gaps, damaged surfaces, crevices and poorly matched component interfaces can retain product residues. This creates cleaning difficulties and potential contamination risks.
Element-to-element fit, surface finish, accessible cleaning areas and the design of the complete screw assembly are important. A surface that looks smooth is not automatically hygienic; the actual finish, geometry and cleaning procedure all matter.
Food-contact material requirements
Materials used in product-contact areas must be suitable for the intended food or feed application. The appropriate grade depends on the food type, moisture, temperature, cleaning chemicals and applicable regulatory requirements.
Wear-resistant coatings and surface treatments must not be assumed suitable for food contact simply because they provide good abrasion resistance. Their suitability, process conditions and supporting documentation must be confirmed before use in a product-contact area.
Materials for Food and Feed Extruder Parts
Material selection depends on the component's location, the product being processed, the cleaning regime and the expected wear mechanism. Product-contact components and non-product-contact mechanical components should be specified separately.
| Component duty | Material or construction options | Important consideration |
|---|
| General product-contact components | Suitable 300-series stainless steel grades | Confirm exact grade, corrosion resistance, surface finish and food-contact suitability. |
| Product-contact components under abrasive duty | Suitable corrosion-resistant, wear-resistant material grades | Hardness, corrosion performance and food-contact suitability must all be evaluated. |
| Specialised hardened components | Selected corrosion-resistant hardenable alloys | Some grades can achieve high hardness, but grade and heat-treatment condition must be confirmed. |
| Non-product-contact shafts | 40CrNiMo, H13, WR15E and other engineering steels | Selected according to torque, strength, fatigue and connection requirements. |
| Barrel bore and liners | Stainless or other suitable base materials, replaceable liners and specified surface treatments | Any product-contact surface must meet the relevant material and hygiene requirements. |
For abrasive recipes, a high-hardness corrosion-resistant material may be considered. A hardness target such as 58–62 HRC is not suitable for every stainless steel grade. It must be linked to a specific hardenable alloy and heat-treatment specification. The final material should be selected only after the application and product-contact requirements have been reviewed.
Food Extruder Applications
EXTRUTEX can assess replacement components for a broad range of food and feed extrusion applications.
- Breakfast cereals: conveying elements, kneading blocks and barrel components for cereal processing.
- Expanded snacks: screw components for controlled cooking, expansion and product shaping.
- Pet food: screw elements, shafts and barrel parts for dry pet food production.
- Aquafeed: replacement parts for fish feed and other aquatic feed processing.
- Textured vegetable protein: components for plant-protein extrusion and texturisation.
- Food ingredients: screw and barrel parts for starch, protein and ingredient processing.
- Confectionery: selected extrusion equipment and specialist food-processing applications.
- Pasta and cereal products: model-specific screw components and wear parts.
- Feed premixes: components for mineral-rich and abrasive feed formulations.
- Specialty food products: custom components for specific recipes and extrusion conditions.
Replacement Parts for Bühler Food Extruders
Bühler manufactures twin-screw extrusion platforms for breakfast cereals, food ingredients, pet food and aquafeed. Its product range includes PolyTwin, EcoTwin, CompacTwin and Nutrex platforms, in addition to other equipment generations.
EXTRUTEX can assess replacement screw elements, kneading blocks, screw shafts and barrel sections for specified Bühler machines. The exact model, screw diameter, shaft connection and component position are required to confirm compatibility.
Replacement Parts for Baker Perkins Extruders
Baker Perkins is an established name in food extrusion, including cereal, snack and confectionery processing. EXTRUTEX can assess replacement components for MPF and SBX machine platforms.
- Conveying screw elements.
- Kneading and mixing blocks.
- Replacement screw shafts.
- Barrel sections and liners.
- Single components and matched screw assemblies.
For Baker Perkins replacement parts, provide the machine model, element position and original part number if available. If the original drawing is no longer available, a physical sample may be used for dimensional assessment.
Replacement Parts for Clextral Food Extruders
Clextral is known for co-rotating twin-screw extrusion systems used in food, feed, cereal and plant-protein applications. EXTRUTEX can assess replacement screw elements, kneading blocks, shafts and barrel sections for specified BC and EVOLUM machines.
Because screw configurations can vary by machine generation and process, the complete element arrangement should be considered when manufacturing replacement parts.
Replacement Parts for Wenger Food and Feed Extruders
Wenger manufactures extrusion equipment for pet food, aquatic feed, snacks and other food-processing applications. EXTRUTEX can assess replacement screw elements, kneading blocks and wear components for confirmed TX, Magnum and other machine configurations.
Send the machine model and screw arrangement so that the required geometry, material and manufacturing tolerances can be reviewed.
Replacement Parts for ANDRITZ Food and Feed Extruders
ANDRITZ supplies equipment for feed, aquafeed and food processing. EXTRUTEX can review replacement-part requirements for specified ANDRITZ extruder models, including screw elements, barrel components, shafts and liners.
For older machines or discontinued configurations, a drawing or physical sample can help establish the original dimensions.
Replacement Parts for Other Food Extruder Brands
EXTRUTEX can also assess spare-part requirements for other food and feed extrusion manufacturers. These include Coperion, GEA, Extru-Tech, American Extrusion International, The Bonnot Company, Diamond America, CPM, Amandus Kahl, FAMSUN, IDAH, Brabender, Schaaf Technologie, Pavan and other regional machine builders.
Some manufacturers produce single-screw food extruders, specialist processing equipment or laboratory machines rather than modular co-rotating twin-screw extruders. We therefore confirm the machine architecture and actual component requirements before accepting an order.
How We Manufacture Replacement Food Extruder Parts
EXTRUTEX can work from OEM drawings, approved technical specifications, part numbers or physical samples. The manufacturing process begins with technical identification and dimensional confirmation.
- Machine identification: We record the manufacturer, model, machine generation and screw diameter.
- Component identification: We establish the position of the element, shaft or barrel section within the machine.
- Dimensional inspection: Critical dimensions, connection geometry and relevant tolerances are checked.
- Material confirmation: The product-contact and non-product-contact material requirements are reviewed separately.
- Machining: The component is manufactured according to the confirmed drawing or approved dimensional specification.
- Finishing: Surface finish, treatment and cleaning requirements are applied according to the component's intended duty.
- Inspection: Critical dimensions are checked against the agreed specification before shipment.
Dimensional Inspection and Quality Control
Correct fit is essential for replacement screw elements and barrel components. EXTRUTEX can provide dimensional inspection according to the agreed drawing and quality requirements.
- Outside diameter and element length inspection.
- Flight pitch and relevant screw-profile measurements.
- Internal spline, keyway or shaft connection inspection.
- Kneading disc thickness and stagger-angle verification.
- Barrel bore and centre-distance inspection where specified.
- Surface finish checks according to the agreed requirement.
- Material and heat-treatment documentation as specified in the order.
- CMM dimensional report for the agreed critical features.
Inspection reports can be supplied with the production batch. Material certificates and other documents should be specified at the quotation stage so that traceability and documentation requirements can be confirmed.
Reverse Engineering When the OEM Drawing Is Missing
Many food and feed extruders have been in service for years. Original drawings may be unavailable, part numbers may have changed, and some OEM spare parts may have long delivery times. EXTRUTEX can assess worn original components and reproduce replacement parts when enough information is available.
For screw elements, we normally inspect:
- Outside diameter and overall length.
- Internal spline or shaft connection.
- Flight lead, pitch and profile geometry.
- Element orientation and position on the shaft.
- Disc thickness and stagger angle for kneading blocks.
- Wear patterns and remaining measurable surfaces.
For barrel sections, we may require the bore diameter, centre distance, section length, connection dimensions and bolt pattern. If the original component is severely worn, an unworn neighbouring element or the shaft and barrel drawings may be needed to establish the correct original dimensions.
What Information to Send for a Quotation
To help us identify the correct replacement component, please provide as much of the following information as possible.
| Information required | Details |
|---|
| Machine manufacturer | Bühler, Baker Perkins, Clextral, Wenger, ANDRITZ or another brand. |
| Machine model | Exact model, series and machine generation if known. |
| Screw diameter | Nominal screw diameter or measured flight-tip diameter. |
| Element position | Position on the left or right shaft and the element sequence. |
| Part number | OEM part number or drawing reference, if available. |
| Photographs | Clear photographs of the worn part with a ruler or scale in frame. |
| Product or recipe | Pet food, aquafeed, cereal, snack, plant protein or other product. |
| Moisture and process conditions | Approximate moisture, temperature and relevant operating conditions. |
| Barrel information | Bore diameter, centre distance, section length and bolt pattern. |
| Material requirement | Product-contact material, wear resistance and documentation requirements. |
Lead Time and Supply Options
Delivery time depends on the machine brand, material availability, component complexity and whether the original drawings are available.
| Machine and supply type | Indicative delivery arrangement |
|---|
| Common Chinese food and feed machines | Selected standard components may be available from stock for immediate dispatch. |
| Imported OEM machine spares | Typically 30–45 days after material availability and drawing or sample confirmation. |
| Special stainless steel grades | Depends on stock availability, machining requirements and surface finish. |
| Custom screw sets and barrel sections | Confirmed individually after technical review. |
For planned maintenance shutdowns, we recommend sending the drawings and part information early. Special material grades, surface finishes and inspection documentation can affect the manufacturing schedule. Transit time is additional to the manufacturing lead time.
Frequently Asked Questions
Can EXTRUTEX supply parts for Bühler, Baker Perkins, Clextral, Wenger and ANDRITZ food extruders?
Yes. EXTRUTEX has manufactured replacement components for machines from these manufacturers. Send the exact machine model, screw diameter and element position, or provide a photograph or drawing of the original component. We will review compatibility before manufacturing.
Can you manufacture parts for other food extruder brands?
Yes. We can assess replacement-part requirements for most food and feed extruder brands, including older and discontinued machine platforms. Manufacturing feasibility depends on the machine design, component dimensions, available material and the information supplied.
Are your food extruder parts made from food-contact materials?
Product-contact components can be manufactured using specified food-contact-suitable materials. The exact material grade, surface finish and documentation must be agreed according to the product and applicable requirements. Tell us which components contact the food or feed so that the correct material can be evaluated.
Can I use plastics compounding screw elements in a food extruder?
Not without checking the design and materials. Even when the screw geometry looks similar, the product-contact material, surface finish, cleanability and process requirements may be different. A component suitable for plastics compounding is not automatically suitable for food processing.
Why does my food product come out overcooked or burnt?
Possible causes include excessive mechanical energy input, unsuitable screw-element arrangement, high barrel temperature, incorrect moisture, excessive residence time, restricted flow or an inappropriate process setting. The screw assembly is only one part of the system. Check the recipe, preconditioning, screw speed, temperature profile and throughput before changing the kneading arrangement.
Can you manufacture replacement kneading blocks with different stagger angles?
Yes. EXTRUTEX can manufacture specified 30°, 45°, 60° and 90° stagger kneading blocks, subject to the machine design and drawing. Disc thickness, arrangement and element position must also be confirmed.
Do you supply complete food extruder barrels or only screw elements?
Both. We can manufacture screw elements, kneading blocks, shafts, complete barrel sections and replacement liners. Barrel refurbishment and re-machining can also be assessed according to the original construction and required tolerances.
Can you reproduce parts if the OEM drawing is missing?
Yes, in many cases. Send the original worn part, photographs with a scale, and any available shaft or barrel information. We can measure the component and assess whether its original geometry can be reconstructed reliably.
What screw diameters can you manufacture?
EXTRUTEX can assess screw components from 7 to 486 mm in diameter. The actual available dimensions depend on the component design, machine requirements and manufacturing specification.
What materials do you use for abrasive food and feed recipes?
Material selection depends on the product-contact requirements and the type of abrasion. Mineral-rich recipes, bone meal and some aquafeed formulations may require additional wear resistance. We evaluate corrosion resistance, hardness, material suitability and the required documentation before recommending a grade.
Can you use a wear-resistant coating on food-contact components?
Only when the coating is suitable for the intended food-contact application and the required supporting documentation is available. A coating should never be selected solely because it provides high wear resistance.
What lead time should I plan for?
Selected standard components for Chinese food and feed extruders may be available from stock. Imported-machine spares generally require around 30–45 days after material availability and drawing or sample confirmation, plus transit time. Special stainless grades and surface finishes may require additional time.
Can you supply one replacement element or only complete sets?
Both options are available. Customers can order one replacement element, a group of kneading blocks, a complete screw set, shafts or barrel sections.
Can you provide a CMM inspection report?
Yes. Dimensional inspection and a CMM report can be provided according to the agreed inspection requirements. Please specify the critical dimensions and documentation requirements before production.
Contact EXTRUTEX for Food Extruder Spare Parts
Looking for replacement screw elements, kneading blocks, shafts or barrels for a food or feed extruder?
Send us the machine manufacturer, model, screw diameter, component position and available drawings or photographs. EXTRUTEX can assess replacement parts for Bühler, Baker Perkins, Clextral, Wenger, ANDRITZ and most other food and feed extrusion machine brands.
We manufacture to confirmed dimensions and agreed material specifications, with dimensional inspection available for the production batch.



-
(0 customer reviews)