EXTRUTEX Screws and Barrels: Precision Replacement Components for Every Plastic Extruder Brand Worldwide
In the demanding world of polymer processing, the screw and barrel assembly forms the absolute core of every extruder. These components determine melt quality, throughput, energy consumption, dimensional stability of the final product, and ultimately the economic viability of an entire production line. When screws wear, barrels lose their original bore geometry, or flight clearances increase beyond design limits, output drops, melt temperature rises, gels and black spots appear, and unplanned downtime becomes inevitable. EXTRUTEX specializes exclusively in the design, manufacture, and supply of new high-performance screws and barrels engineered as direct replacements or upgraded solutions for virtually any plastic extruder in commercial use anywhere in the world.
Drawing on Austrian design expertise, German metallurgical standards, and advanced manufacturing facilities in Germany and China, EXTRUTEX delivers components that restore or even exceed original equipment manufacturer (OEM) performance while offering competitive lead times and pricing. Whether the machine is a decades-old single-screw pipe extruder or a modern co-rotating twin-screw compounding line, EXTRUTEX engineers can reverse-engineer, optimize, and produce exact-fit or performance-enhanced screws and barrels.
Core promise: EXTRUTEX manufactures new screws and barrels for any plastic extruder brand. From the largest European and American OEMs to specialized Asian and emerging-market machines, compatibility is not a limitation—it is the foundation of the service.
1. The Critical Role of Screws and Barrels in Plastic Extrusion
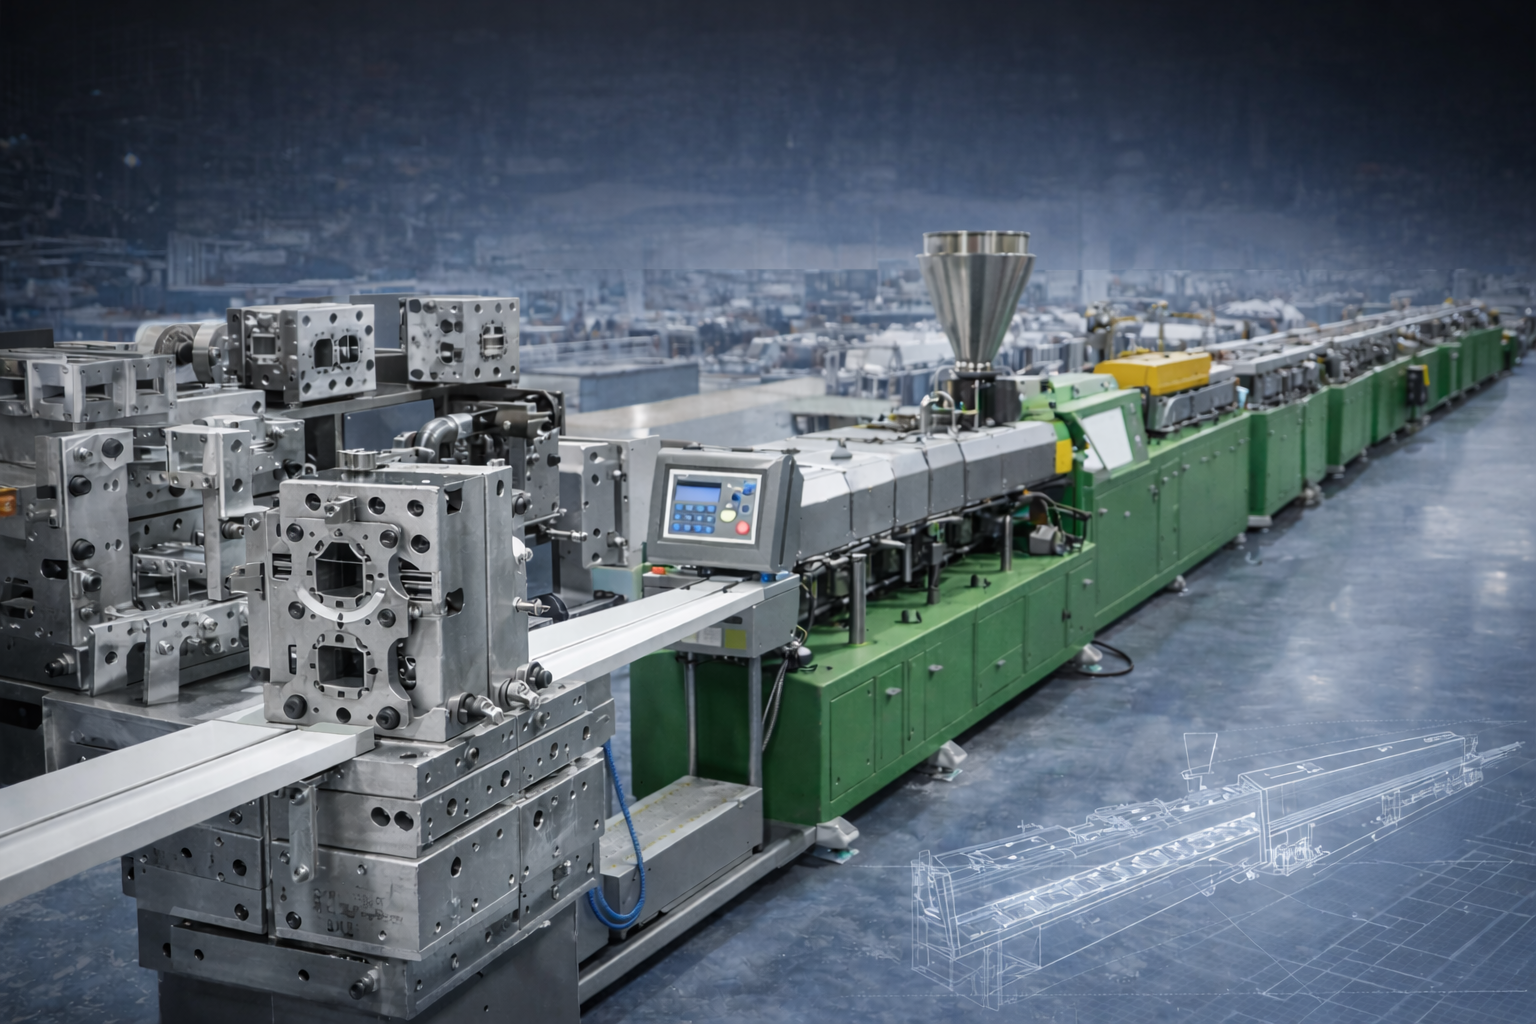
Plastic extrusion converts solid polymer pellets, powder, or recycled flakes into continuous profiles, pipes, films, sheets, cables, and compounded pellets. The process relies on the rotating screw (or intermeshing pair of screws) inside a precisely temperature-controlled barrel. Material is conveyed, compressed, melted by a combination of conductive heat and viscous shear, homogenized, degassed if necessary, and finally pressurized for passage through a die.
Single-screw extruders remain the workhorses for pipe, profile, sheet, and many film applications because of their simplicity, robustness, and relatively low cost. Twin-screw extruders—especially co-rotating intermeshing designs—dominate compounding, masterbatch production, reactive extrusion, and recycling of contaminated or highly filled materials because of their superior mixing, venting, and self-wiping characteristics. Conical counter-rotating twin screws are preferred for rigid PVC pipe and profile extrusion where high torque at low shear is essential to avoid degradation.
Regardless of configuration, the geometric relationship between screw flights and barrel wall, the surface hardness and corrosion resistance of both components, and the precision of the feed zone (smooth or grooved) govern process stability. Typical wear mechanisms include abrasive wear from mineral fillers (CaCO3, talc, glass fiber, TiO2), corrosive attack from HCl liberated by PVC or from halogenated flame retardants, and adhesive wear or scoring under high pressure. Once radial clearance exceeds approximately 0.3–0.5 mm on a medium-sized machine, pumping efficiency collapses and the line becomes uneconomic to run.
2. EXTRUTEX Product Portfolio
Single-Screw Systems
EXTRUTEX supplies complete screw-and-barrel sets with diameters ranging from 20 mm laboratory sizes up to 300 mm high-output industrial machines. L/D ratios are customized—commonly 25:1 to 40:1 for polyolefins and up to 48:1 or higher for specialized venting or barrier designs. Available geometries include conventional three-zone screws, barrier screws (Maillefer or similar), Maddock mixing sections, pineapple or Saxton mixers, and multi-flight designs optimized for specific resins such as PE, PP, PET, PS, ABS, PMMA, and engineering polymers.
Twin-Screw Systems
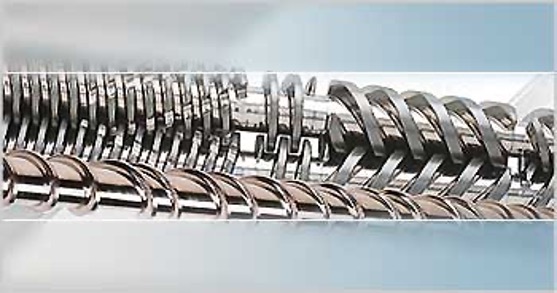
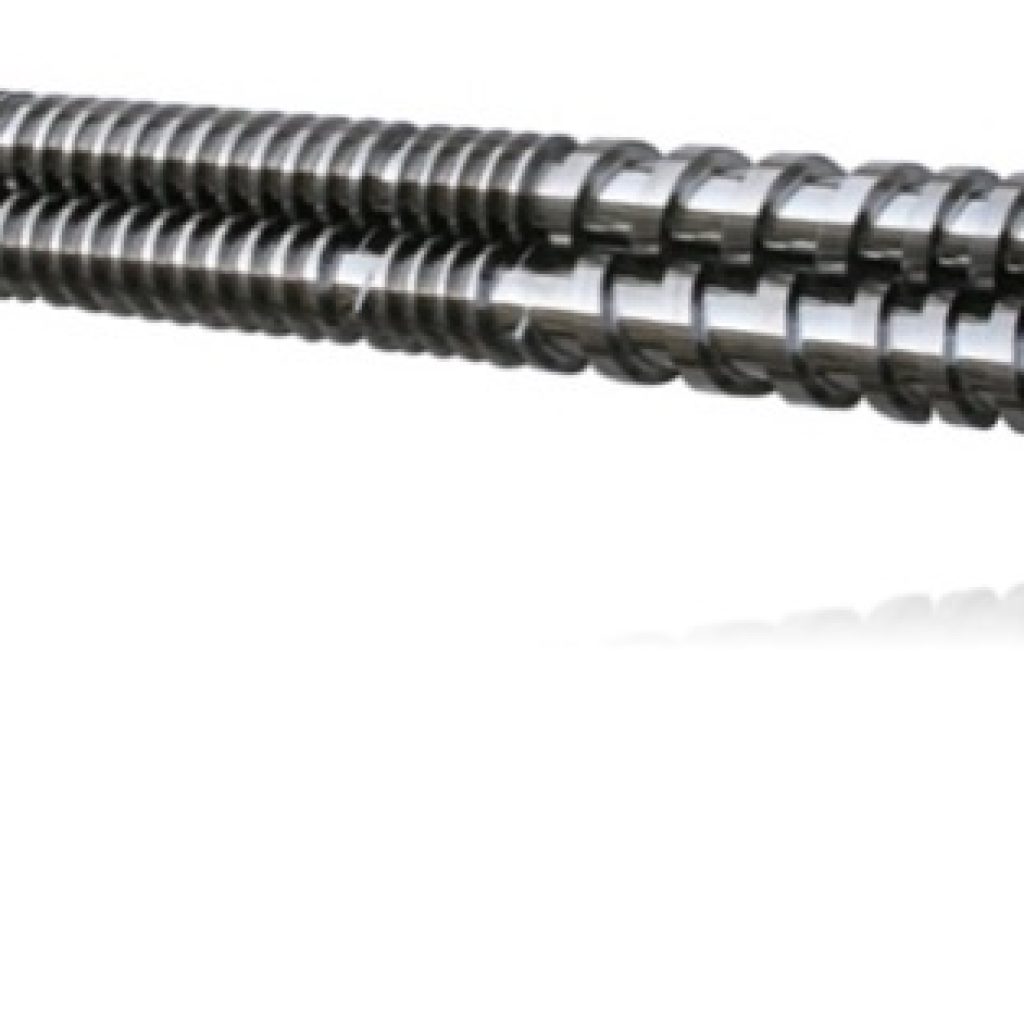
For conical twin-screw extruders (primarily PVC), EXTRUTEX produces matched pairs with optimized compression and mixing zones. For parallel co-rotating and counter-rotating machines, the company manufactures segmented modular elements—conveying, kneading, mixing, and reverse-flight blocks—compatible with the major OEM platforms. Complete barrel sections with optional liners are also available.
Materials and Surface Engineering
Base materials include nitriding steels 38CrMoAlA (DIN 1.8509) and Böhler V820 (1.8550), tool steels, powder-metallurgy grades for extreme abrasion, and corrosion-resistant stainless alloys for fluoropolymers or aggressive formulations. Heat treatment typically involves gas or ion nitriding to surface hardness ≥ HV 900 with case depths of 0.5–0.8 mm. Flight tips may receive plasma-sprayed molybdenum coatings or hard-facing alloys; barrels can be supplied as monobloc nitrided units or with bi-metallic liners (nickel-based or tungsten-carbide) for maximum service life.
EXTRUTEX
3. Compatibility with Global Plastic Extruder Brands
EXTRUTEX maintains extensive dimensional databases and reverse-engineering capability covering virtually every significant plastic extruder manufacturer. The following non-exhaustive list illustrates the breadth of coverage. Customers routinely order replacement screws and barrels for machines from these brands and many smaller or regional makers as well.
KraussMaffei (Germany)
Coperion (Germany)
Leistritz (Germany)
Battenfeld-Cincinnati (Austria/Germany)
Reifenhäuser Group (Germany)
Davis-Standard (USA)
Milacron (USA)
Shibaura Machine (Japan, formerly Toshiba)
Japan Steel Works – JSW (Japan)
Bausano & Figli (Italy)
AMUT (Italy)
Luigi Bandera (Italy)
SML Maschinengesellschaft (Austria)
ENTEK (USA)
NFM Welding Engineers (USA)
CPM Extrusion Group (USA)
BUSS AG (Switzerland)
Kabra Extrusiontechnik (India)
STEER Engineering (India)
Windsor Machines (India)
Everplast Machinery (Taiwan)
Hans Weber Maschinenfabrik (Germany)
Hosokawa Alpine (Germany)
Windmöller & Hölscher – W&H (Germany)
Brückner Group (Germany)
Macchi (Italy)
Colines (Italy)
JWELL (China)
Nanjing Haisi (China)
USEON (China)
Jiangsu Xinda (China)
Clextral (France)
Alpha Marathon (Canada)
Rajoo Engineers (India)
Gneuss (Germany)
And many regional OEMs worldwide
For twin-screw platforms the segmented elements are dimensionally interchangeable with Coperion ZSK, Leistritz ZSE, JSW TEX, Shibaura (Toshiba), STEER Omega, and equivalent systems. Conical twin-screw pairs are routinely supplied for classic Battenfeld, KraussMaffei, Cincinnati, and parallel Chinese or Indian machines. Single-screw replacements cover the full range of Davis-Standard, Milacron, Reifenhäuser, Bandera, AMUT, SML, and countless others.
4. Engineering and Manufacturing Process
Every project begins with either an OEM drawing, a set of precise measurements taken from the existing worn components, or a 3-D scan. EXTRUTEX process engineers then select the optimal base material, heat-treatment route, and surface-protection strategy according to the polymer family, filler content, and required service life. Computer-aided design and finite-element analysis may be applied for high-output or high-torque applications to verify stress distribution and thermal expansion.
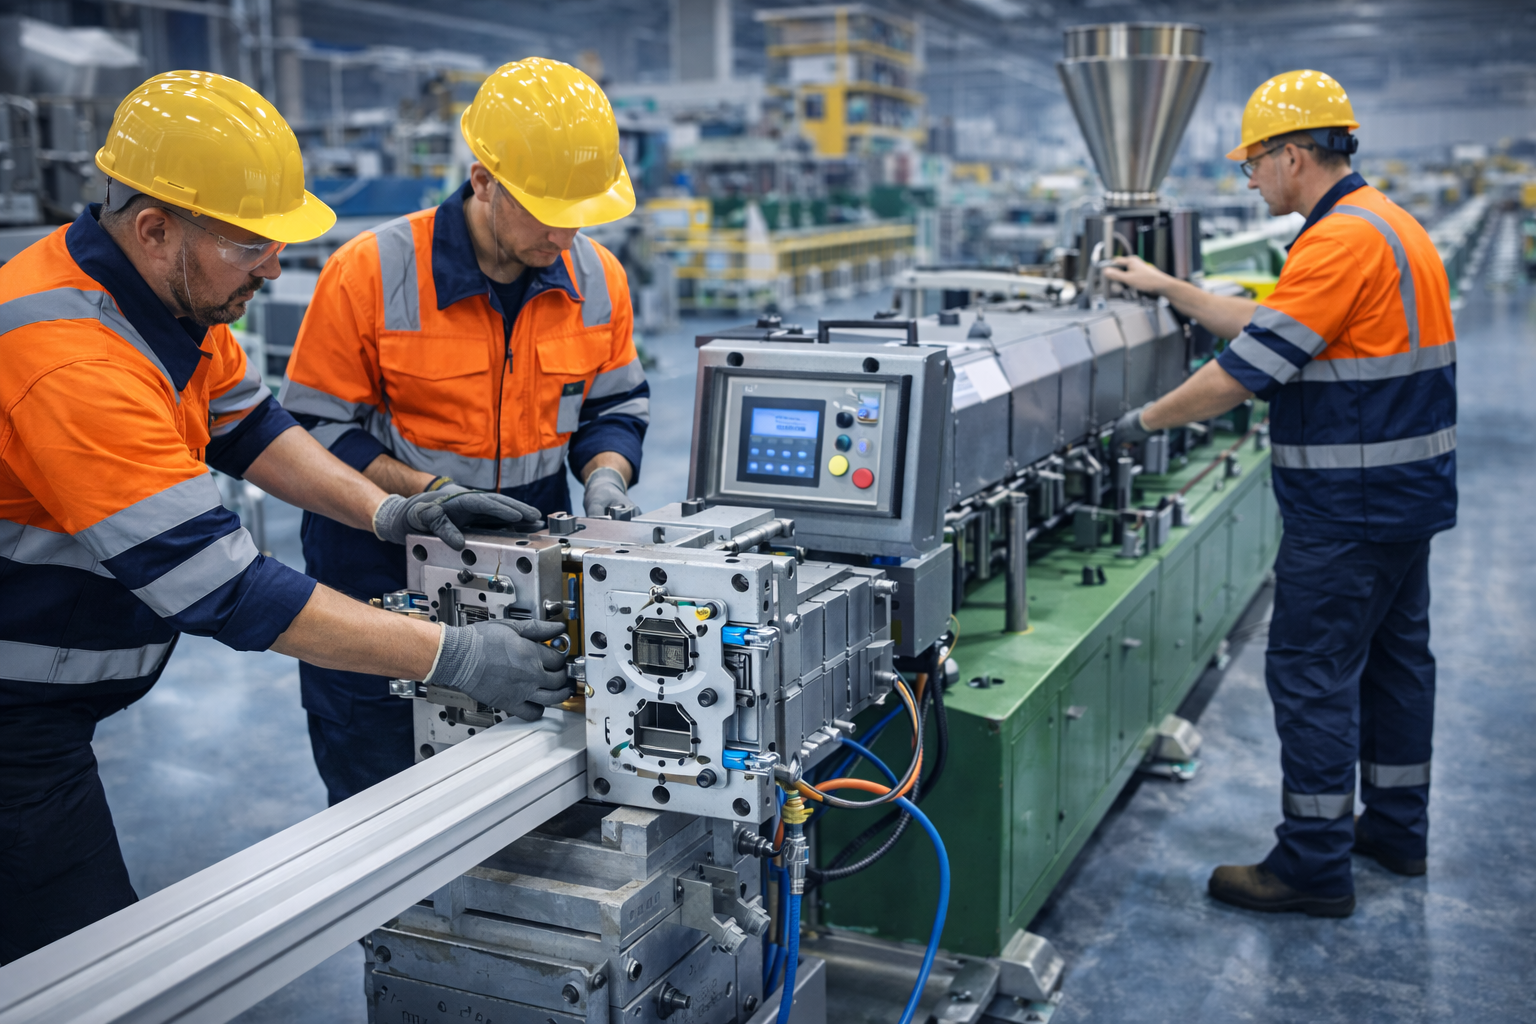
Manufacturing employs CNC turning, milling, and grinding centers capable of maintaining flight land widths, root diameters, and lead angles to tight tolerances. Barrel bores are honed to ±0.01 mm. After heat treatment, final grinding restores the original geometry or implements an improved profile (for example, a deeper feed section or a more efficient barrier flight). Quality control includes hardness mapping, surface-roughness measurement, dimensional reports, and, where required, ultrasonic or magnetic-particle inspection.
For customers seeking maximum uptime, EXTRUTEX also offers complete rebuilding services: worn flights are rebuilt by plasma or laser cladding, barrels are re-lined or re-nitrided, and the restored assemblies are returned with a renewed service-life expectation at a fraction of the cost of a new set.
5. Technical Specifications Snapshot
| Parameter |
Typical Specification / Range |
Notes |
| Screw diameter range |
20 mm – 300 mm |
Larger diameters on request |
| L/D ratio |
20:1 – 48:1 (custom) |
Optimized per application |
| Base materials (screws) |
38CrMoAlA, 40Cr, tool steels, PM steels, stainless |
Selected by wear/corrosion demand |
| Base materials (barrels) |
38CrMoAlA, Böhler V820, bi-metallic liners |
Ni-based or WC liners available |
| Surface hardness |
≥ HV 900 (nitrided) |
Case depth 0.5–0.8 mm |
| Flight coating options |
Plasma Mo, hard chrome, special alloys |
Thickness 0.02–0.20 mm |
| Bore tolerance |
±0.01 mm |
After final honing |
| Typical applications |
PE, PP, PVC, PET, PS, ABS, PA, PC, filled compounds, recycling |
All common thermoplastics |
| Compatible configurations |
Single, conical twin, parallel co-/counter-rotating |
Segmented elements for major platforms |
| Delivery options |
New complete sets, modular elements, rebuilds |
Stock for popular sizes |
6. Application-Specific Benefits
Polyolefin pipe and profile: High-output barrier or HELIFEED-style geometries combined with grooved feed sections deliver stable throughput at lower melt temperatures, improving dimensional control and reducing energy consumption.
Rigid PVC: Conical twin-screw pairs with carefully balanced compression and low-shear mixing zones minimize degradation while maximizing output of pipe, window profiles, and sheets.
Compounding and masterbatch: Segmented co-rotating elements with optimized kneading blocks provide excellent dispersive and distributive mixing for glass-fiber, mineral-filled, and color concentrates.
Recycling: Wear-resistant materials and effective venting geometries handle contaminated post-consumer flake, reducing the frequency of screw changes and improving melt filtration efficiency downstream.
Engineering plastics and specialty resins: Corrosion-resistant alloys and gentle melting profiles protect sensitive materials such as PET, PA, and halogenated compounds.
7. Economic and Operational Advantages
Replacing a worn screw-and-barrel set with an EXTRUTEX solution typically restores original output rates, lowers specific energy consumption, reduces scrap rates caused by gels or incomplete melting, and extends the interval between subsequent maintenance events. Because the components are manufactured to the same or tighter tolerances as the OEM originals—and often incorporate design improvements—the return on investment is realized within months through higher productivity and lower energy and scrap costs.
Global logistics support, including coordination of shipping and customs documentation, further reduces total downtime. Technical consultation is available before order placement to confirm material selection and geometry for the customer’s exact resin and process conditions.
Summary of value: Austrian design intelligence + German metallurgical quality + flexible manufacturing footprint = high-performance, cost-effective screws and barrels for any plastic extruder brand operating anywhere in the world.
8. Conclusion
The longevity and efficiency of every plastic extrusion line ultimately depend on the condition of its screws and barrels. When these critical components reach the end of their useful life, operators face a choice: accept declining performance and rising costs, or invest in precision replacements engineered for the task. EXTRUTEX exists to make the second choice straightforward, technically sound, and economically attractive.
By covering the full spectrum of single-screw, conical-twin, and parallel-twin platforms from KraussMaffei, Coperion, Leistritz, Battenfeld-Cincinnati, Davis-Standard, Milacron, Reifenhäuser, Shibaura, JSW, Bausano, AMUT, Bandera, and dozens of other manufacturers worldwide, EXTRUTEX removes the traditional barrier of OEM exclusivity. Customers gain access to modern materials, optimized geometries, and reliable delivery without being locked into a single supplier’s pricing or lead times.
Whether the requirement is a standard replacement set, a performance-upgraded geometry, modular twin-screw elements, or a complete rebuild of existing hardware, EXTRUTEX provides a single-source solution backed by engineering expertise and rigorous quality control. The result is restored productivity, improved product quality, and a lower total cost of ownership for extrusion operations of every scale.



-
(0 customer reviews)