No products in the cart.
All rights of this website are reserved for EXTRUTEX Austria and its partner companies, © 2026

Multiple Payment Methods

Discount for advance payments over 50%

Free Shipping Coordination Services
Payment methods:

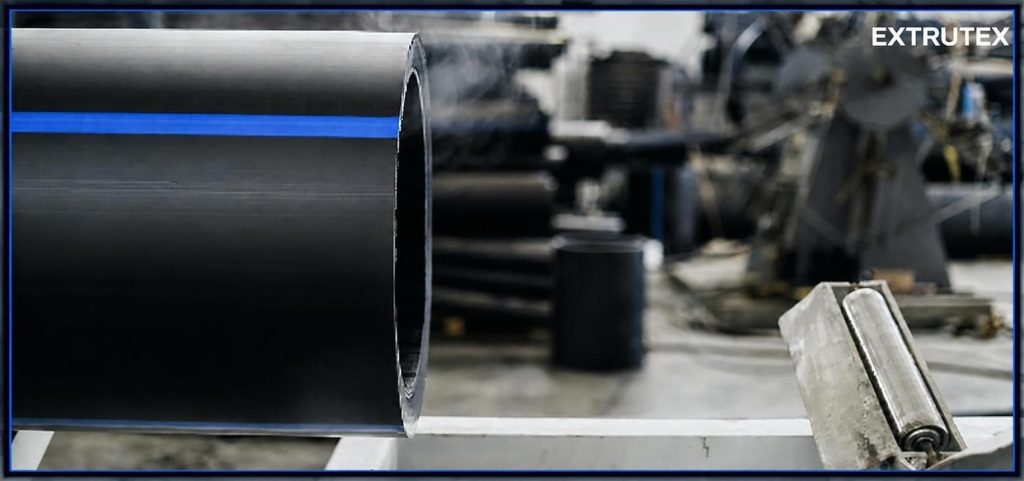
EXTRUTEX designs and supplies complete polyethylene (PE) pipe extrusion lines for manufacturing high-quality plastic pipes for water supply, drainage, irrigation, gas distribution, industrial fluid transportation, infrastructure and other demanding applications. With pipe production solutions ranging from small-diameter pipes of 12 mm to customized large-diameter systems of up to 3500 mm, EXTRUTEX provides flexible extrusion technology for different production capacities, pipe specifications and factory requirements.
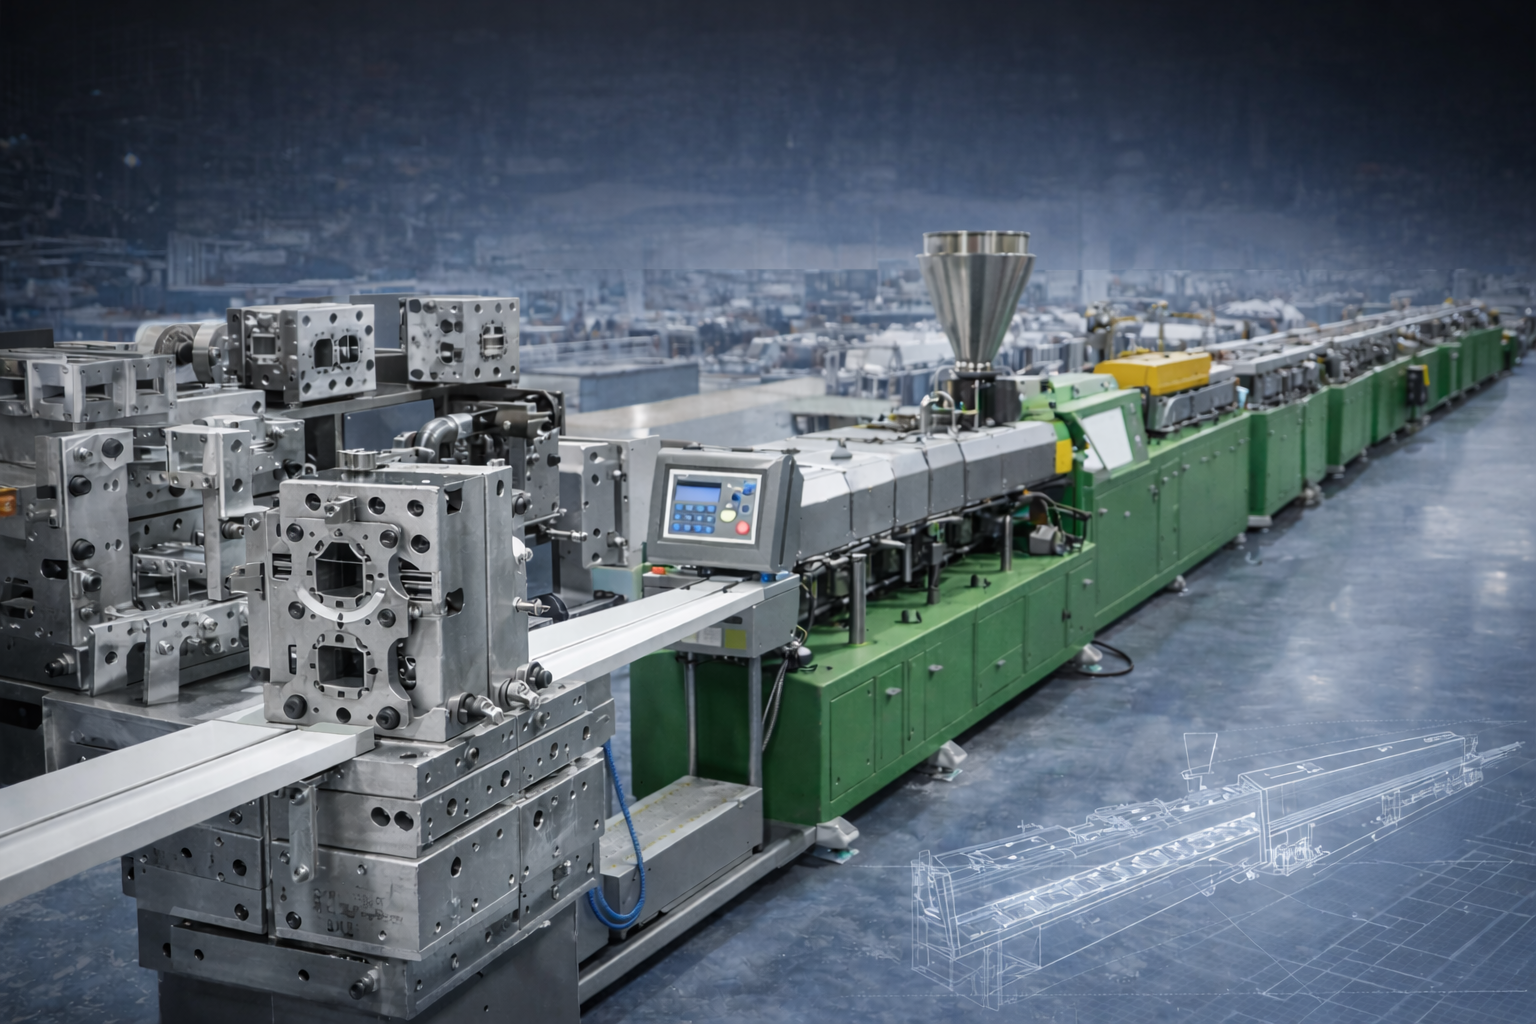
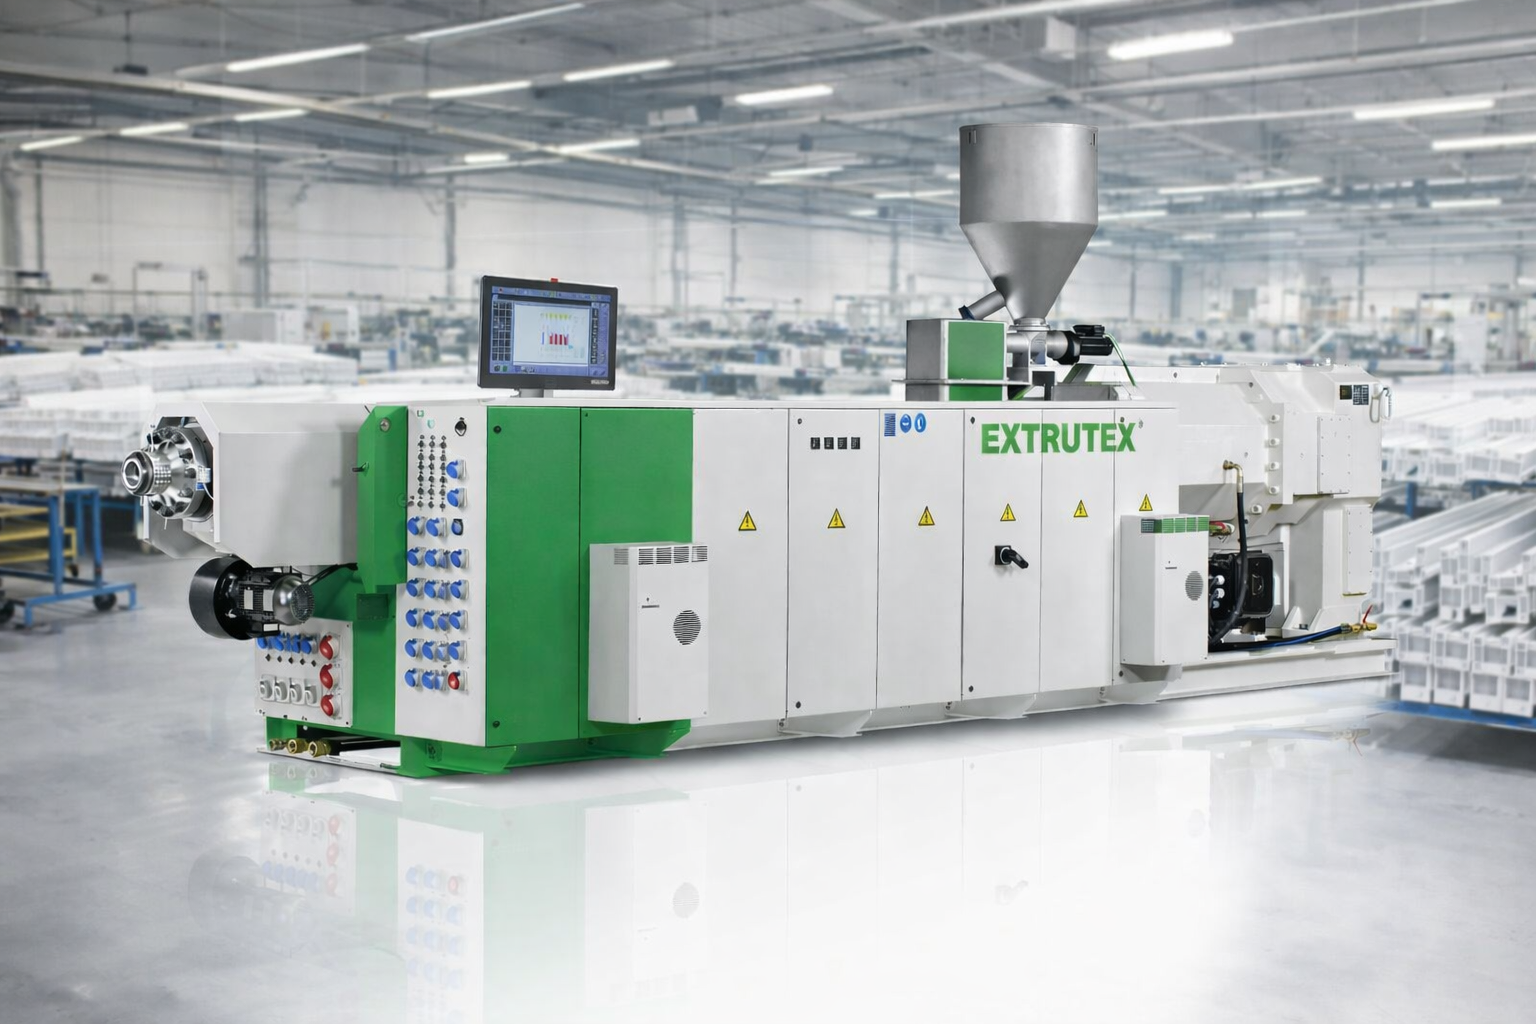
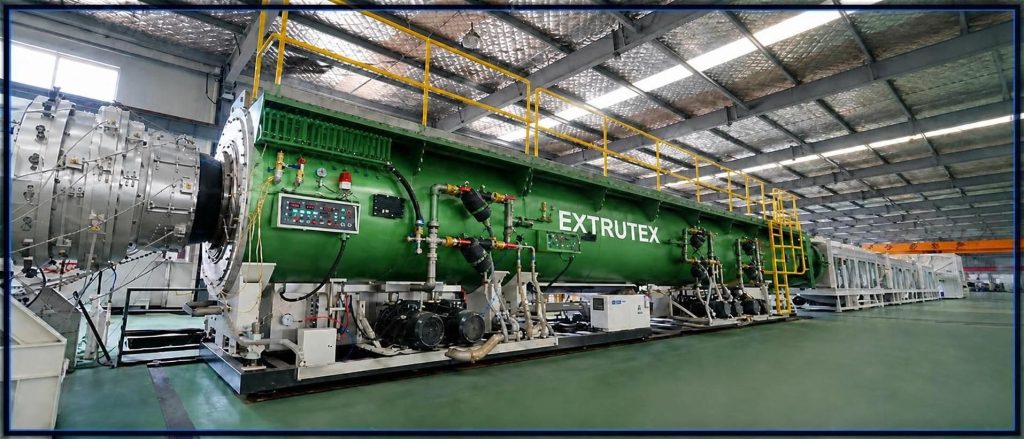
Our PE pipe production lines integrate single-screw extruders, pipe extrusion dies, vacuum calibration tanks, spray cooling tanks, haul-off units, cutting saws and tilt tables. Depending on the required pipe diameter, wall thickness, material grade, output and production environment, the complete line can be configured with appropriate extrusion and downstream equipment.
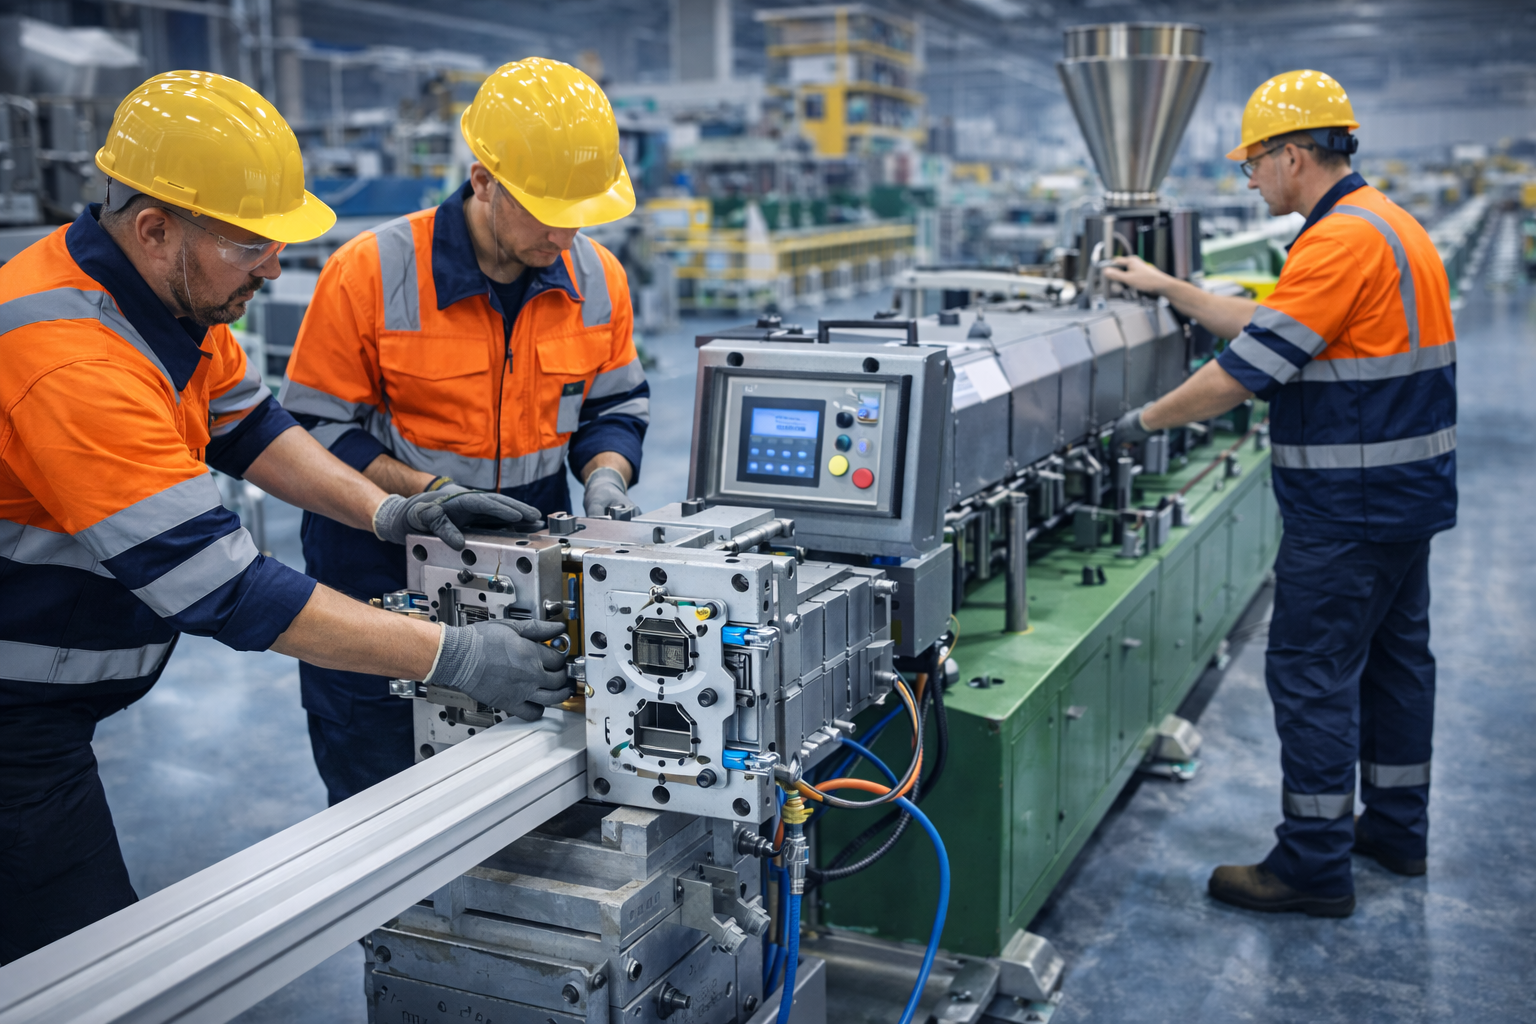
EXTRUTEX combines Austrian design, laboratory and R&D capabilities with manufacturing in China to provide practical extrusion solutions for pipe manufacturers worldwide. Each production line can be configured according to the customer's technical requirements, factory layout, applicable standards and intended pipe applications.
A PE pipe extrusion line is a coordinated production system in which polyethylene material is melted, homogenized, extruded through a specially designed die, calibrated, cooled, pulled at a controlled speed, cut to length and transferred for collection. Stable operation depends on the coordination of every component, from screw design and melt pressure to vacuum calibration, cooling capacity and haul-off speed.
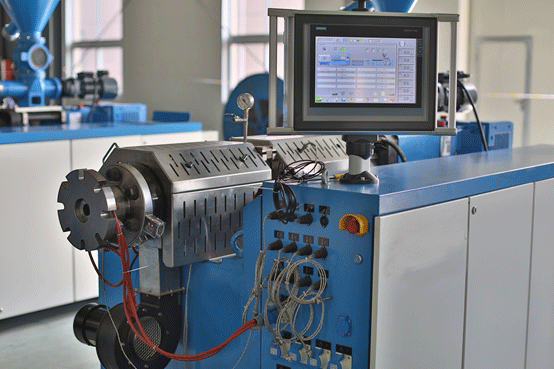
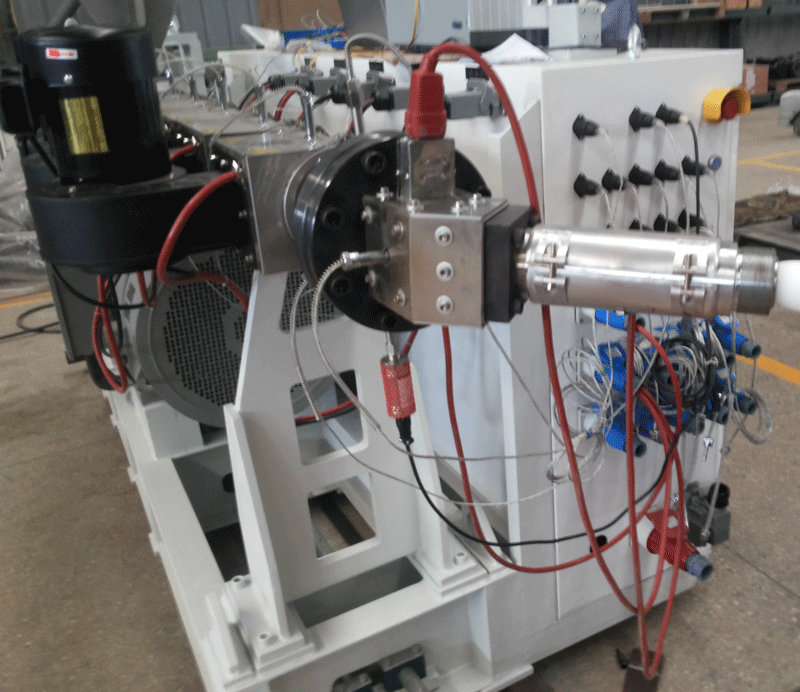
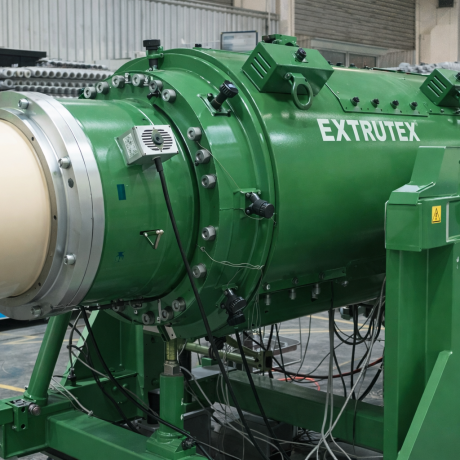
The single-screw extruder is the central processing unit of the production line. It conveys, melts, homogenizes and pressurizes polyethylene materials before delivering a stable melt flow to the pipe die. EXTRUTEX PE pipe extrusion lines use HELIFEED single-screw extruder configurations selected according to the pipe diameter range, material characteristics, wall thickness, required output and production speed.
Our previously established HELIFEED pipe extruder series includes 45/40, 60/40, 75/40, 90/40, 105/40, 125/40 and 150/40 configurations. The appropriate model is selected for each project rather than applying one extruder to every pipe size.
Depending on the application, the extruder can be equipped with a suitable screw and barrel design, controlled heating and cooling zones, a variable-speed drive, melt pressure and temperature monitoring, and a production control system. Screw geometry, compression characteristics and processing conditions are selected to suit the intended PE grade and production requirements.
For small-diameter pipes, the focus is on stable melt delivery, precise dimensional control and efficient high-speed production. For large-diameter pipes, the extrusion system must provide sufficient melt throughput, stable pressure, appropriate thermal control and uniform material distribution across the pipe wall.
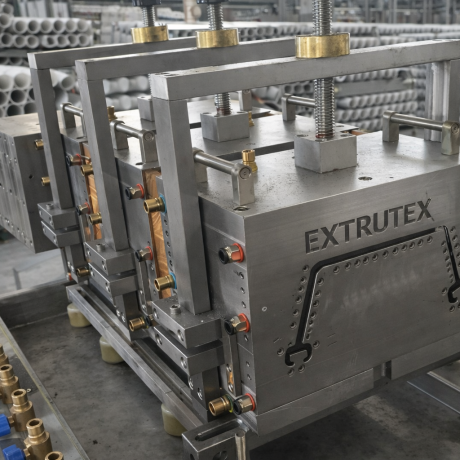
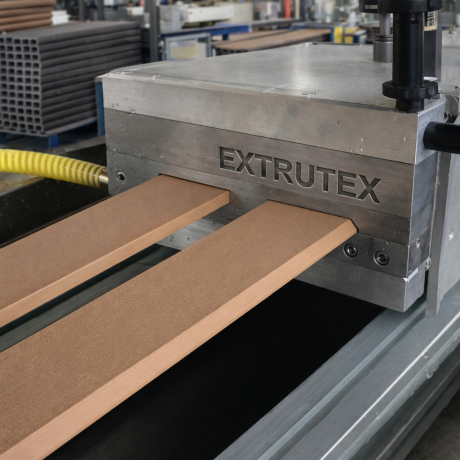
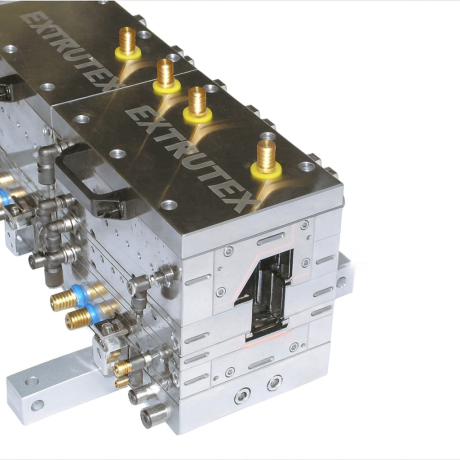
The pipe die head distributes molten polyethylene around the circumference of the pipe to produce a consistent wall structure. Die design must account for the pipe's outside diameter, SDR or wall thickness, material grade, output rate and operating conditions.
EXTRUTEX can configure pipe dies for different PE pipe dimensions and production requirements. Interchangeable tooling, suitable flow channels and carefully selected die components help manufacturers change between product specifications efficiently. For large-diameter pipes, the die head and extrusion system must be engineered together to maintain stable melt distribution and dimensional consistency.
Die design, mandrel dimensions and processing conditions are finalized according to the customer's pipe specification. Specialized configurations, including multilayer structures, require additional extruders, co-extrusion components and appropriate control systems.
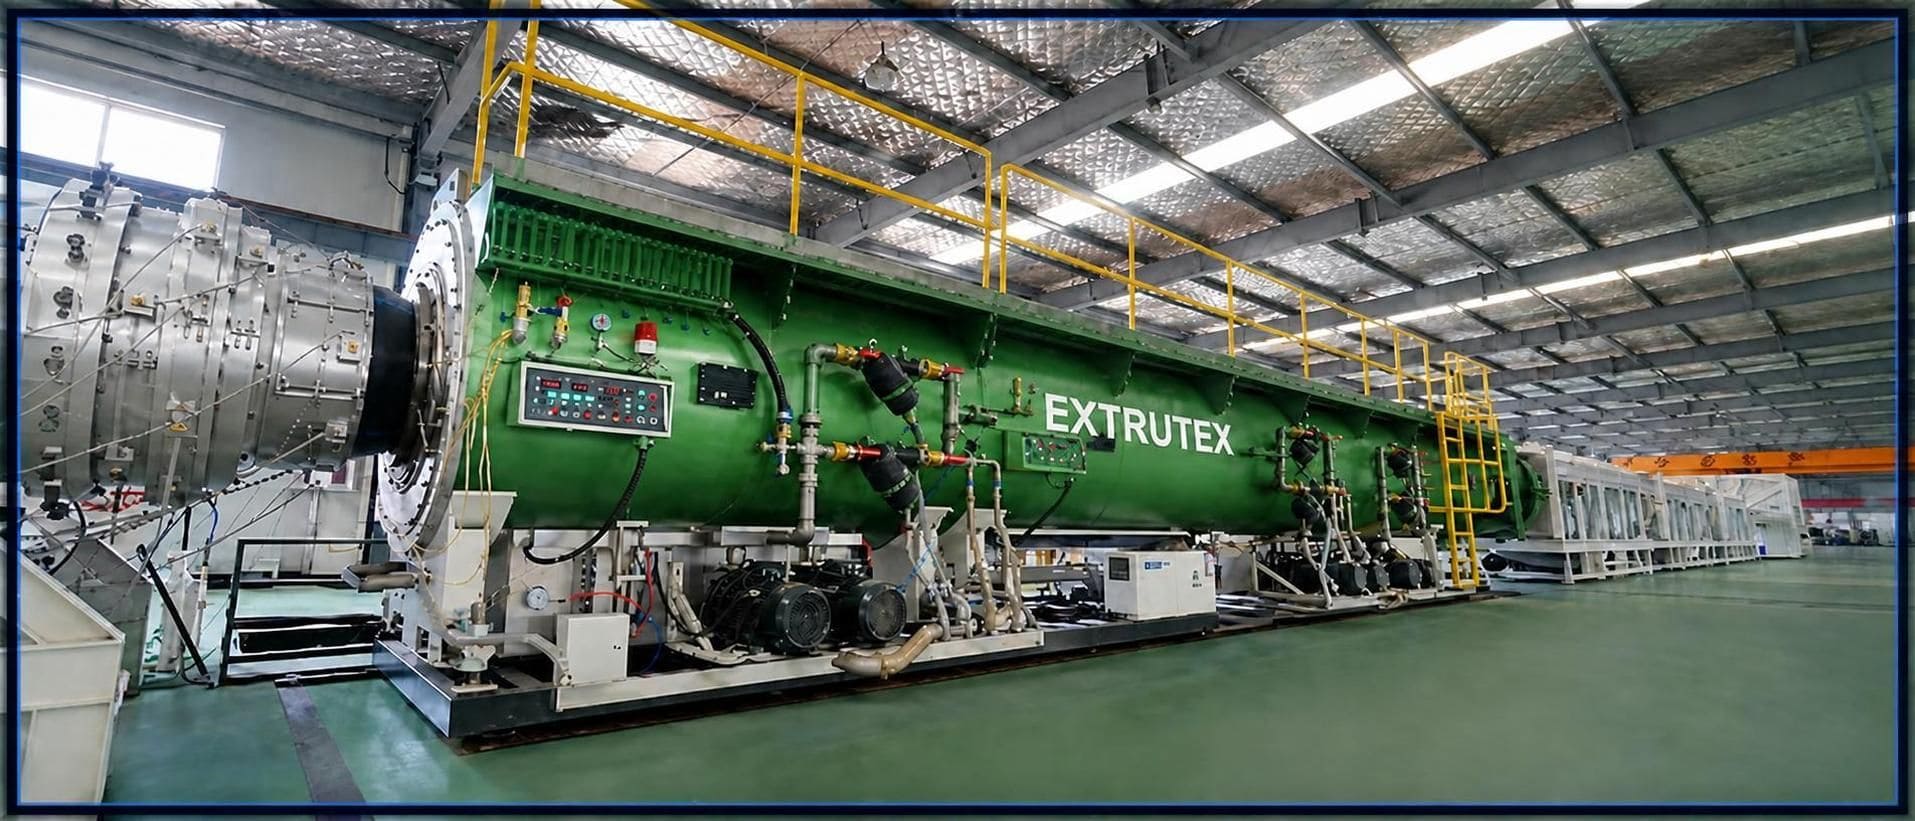
The vacuum calibration tank establishes the initial pipe dimensions after the molten PE leaves the die. Controlled vacuum draws the pipe against the calibration sleeve or sizing system, helping maintain the specified outside diameter and circularity while the material begins to cool.
The vacuum calibration section is particularly important for dimensional accuracy, surface quality and consistent pipe geometry. Its configuration depends on pipe diameter, wall thickness, line speed and the selected calibration method.
EXTRUTEX provides vacuum calibration systems configured for the intended pipe size. Small-diameter lines prioritize compact construction and precise sizing, while larger systems require appropriately engineered tanks, calibration components, vacuum capacity, water circulation and mechanical support.
After initial calibration, the pipe passes through a spray cooling tank where circulating water removes heat from the pipe wall. Proper cooling allows the PE pipe to develop sufficient dimensional stability before entering the haul-off and cutting sections.
The length, number of cooling sections, spray arrangement, water flow and circulation capacity are selected according to the pipe dimensions, material thickness and required production speed. Larger pipes and thicker wall sections generally require greater cooling capacity and a carefully controlled cooling arrangement.
Depending on the production specification, EXTRUTEX can configure multiple cooling tanks, adjustable spray nozzles, water circulation systems, filtration arrangements and temperature monitoring. Cooling must be balanced to avoid unnecessary production bottlenecks and maintain stable pipe dimensions.
The haul-off unit pulls the pipe through the downstream equipment at a controlled speed. Its pulling force and speed must be matched to the extruder output, pipe dimensions and cooling conditions.
Depending on the pipe diameter, EXTRUTEX can configure suitable caterpillar haul-off equipment with an appropriate number of tracks, contact surfaces, clamping arrangements and drive capacity. Small-diameter pipes require accurate speed control, while large-diameter pipes require sufficient traction, mechanical strength and stable pipe handling.
Synchronized control between the extruder and haul-off helps maintain consistent wall thickness and production speed. The final configuration is selected according to the maximum pipe size, operating load and expected production conditions.
The cutting saw cuts the extruded pipe into specified lengths. The cutting solution depends on the pipe diameter, wall thickness, material behavior and required cutting quality.
For smaller pipes, a high-speed cutting system may be appropriate. Medium- and large-diameter lines may require a planetary cutting saw or another engineered cutting arrangement suitable for the pipe dimensions. Cutting control can be synchronized with line speed to achieve repeatable lengths and clean pipe ends.
EXTRUTEX selects the cutting equipment according to the actual application. Cutting method, blade specification, clamping system, chip extraction and safety provisions are finalized for the ordered line.
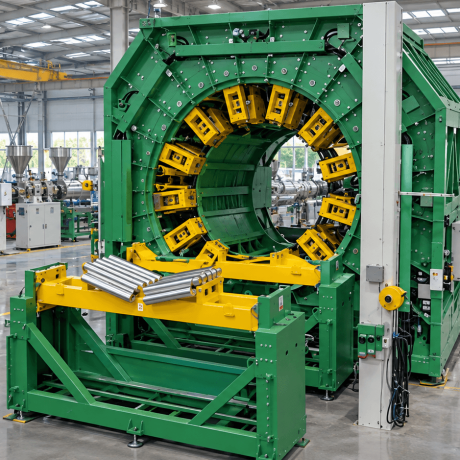
The tilt table receives finished pipes after cutting and supports controlled unloading and collection. Its dimensions, load capacity, working length and discharge mechanism are selected according to pipe diameter, cut length and pipe weight.
For smaller pipes, a compact collection table may be sufficient. For large-diameter pipes, the table must accommodate substantial pipe weight and dimensions while providing stable support and safe handling. Additional rollers, pipe supports or material transfer equipment can be incorporated where required.
The following tables provide indicative EXTRUTEX line configurations. Extruder selection and downstream equipment are determined by the intended pipe diameter, wall thickness, PE grade, output target, line speed and factory conditions. The stated diameter ranges are planning ranges, not a guarantee that every pipe dimension can be produced with one unchanged tooling set.
This compact line is intended for small-diameter PE pipes used in irrigation, water distribution, agricultural systems, micro-irrigation and general fluid transportation. Production priorities include dimensional consistency, stable high-speed extrusion and efficient changeover between pipe sizes.
| Item | Technical configuration |
|---|---|
| Pipe diameter | 12–32 mm |
| Main extruder | HELIFEED 45/40 single-screw extruder; final selection depends on output requirements |
| Pipe die | PE pipe die head configured for the required diameters |
| Calibration | Vacuum calibration tank with suitable sizing sleeve |
| Cooling | Spray cooling water tank |
| Haul-off | High-speed caterpillar haul-off selected for small-diameter pipe |
| Cutting | Automatic cutting saw or application-specific cutting system |
| Collection | Tilt table or suitable pipe collection equipment |
| Production focus | Stable extrusion, precise sizing and efficient small-pipe production |
This configuration serves water supply, agricultural irrigation, general-purpose pressure pipes and utility applications. The extruder, die and downstream equipment are selected to provide stable production over the required diameter range.
| Item | Technical configuration |
|---|---|
| Pipe diameter | 32–63 mm |
| Main extruder | HELIFEED 45/40 or 60/40, selected according to required output |
| Pipe die | Interchangeable PE pipe die configuration |
| Calibration | Vacuum sizing tank |
| Cooling | Spray cooling tank sized for the required line speed |
| Haul-off | Caterpillar haul-off with synchronized speed control |
| Cutting | Automatic saw selected for the pipe dimensions |
| Collection | Tilt table or customized collection system |
| Production focus | Flexible production of small- and medium-diameter PE pipes |
This versatile production line covers a broad range of medium-diameter pipes for water distribution, irrigation networks, infrastructure and industrial applications. The line configuration can be adjusted to accommodate the intended pipe wall thickness and production output.
| Item | Technical configuration |
|---|---|
| Pipe diameter | 50–160 mm |
| Main extruder | HELIFEED 75/40 single-screw extruder |
| Extruder output reference | Approximately 400–580 kg/h for the established 75/40 configuration; actual line output depends on material and operating conditions |
| Pipe die | PE die head and tooling matched to each pipe specification |
| Calibration | Vacuum calibration tank |
| Cooling | Spray cooling tank or coordinated cooling sections |
| Haul-off | Multi-track caterpillar haul-off as required |
| Cutting | Automatic cutting saw |
| Collection | Powered or gravity-assisted tilt table, as specified |
| Production focus | Flexible medium-diameter pipe production and stable dimensional control |
This line is designed for medium- to large-diameter PE pipes used in municipal water supply, industrial transportation, infrastructure and other demanding applications. Extruder throughput, die dimensions and cooling capacity must be coordinated to support the selected pipe wall thickness and production speed.
| Item | Technical configuration |
|---|---|
| Pipe diameter | 110–250 mm |
| Main extruder | HELIFEED 90/40 single-screw extruder |
| Extruder output reference | Approximately 540–770 kg/h for the established 90/40 configuration; actual output is application-dependent |
| Pipe die | Large-bore PE pipe die head |
| Calibration | Vacuum calibration tank with appropriately sized sleeve |
| Cooling | Extended spray cooling tank configuration as required |
| Haul-off | Heavy-duty caterpillar haul-off selected for pipe weight and diameter |
| Cutting | Automatic cutting saw suitable for the selected pipe range |
| Collection | Reinforced tilt table or engineered discharge system |
| Production focus | Stable medium- and large-diameter pipe production |
This configuration is intended for infrastructure projects, municipal water networks, industrial pipelines and other applications requiring large-diameter polyethylene pipes. Greater attention is given to melt throughput, die distribution, vacuum sizing, cooling performance and downstream mechanical capacity.
| Item | Technical configuration |
|---|---|
| Pipe diameter | 250–630 mm |
| Main extruder | HELIFEED 105/40 or 125/40, selected according to the required output |
| 125/40 output reference | Approximately 770–1,100 kg/h for the established 125/40 configuration |
| Pipe die | Large-diameter PE die head |
| Calibration | Vacuum calibration system engineered for the selected diameter |
| Cooling | Long spray cooling tank or multiple cooling sections |
| Haul-off | Heavy-duty multi-track caterpillar haul-off |
| Cutting | Large-diameter automatic or planetary cutting saw, as appropriate |
| Collection | Heavy-duty tilt table and pipe support system |
| Production focus | Large-diameter pipes with coordinated extrusion and cooling |
This large-diameter line is designed for major water transmission projects, drainage systems, industrial infrastructure and specialized pipe applications. Its configuration is determined by pipe wall thickness, maximum required diameter, PE material grade and the customer's target production rate.
| Item | Technical configuration |
|---|---|
| Pipe diameter | 630–1500 mm |
| Main extruder | HELIFEED 125/40 or 150/40, selected according to the production specification |
| 150/40 output reference | Approximately 940–1,300 kg/h for the established 150/40 configuration |
| Pipe die | Large-diameter die head engineered for the required pipe dimensions |
| Calibration | Heavy-duty vacuum calibration system |
| Cooling | Extended spray cooling sections with project-specific water circulation |
| Haul-off | High-capacity caterpillar haul-off with suitable contact and traction systems |
| Cutting | Heavy-duty cutting system selected for pipe diameter and wall thickness |
| Collection | Engineered support and tilt table system for large pipe sections |
| Production focus | Large-scale infrastructure pipe manufacturing |
EXTRUTEX can develop customized large-diameter PE pipe production systems for infrastructure and industrial projects requiring pipes between 1100 mm and 2500 mm. At these dimensions, equipment selection requires detailed engineering rather than simply scaling up a smaller standard line.
| Item | Technical configuration |
|---|---|
| Pipe diameter | 1100–2500 mm |
| Main extruder | HELIFEED 150/40 or a project-engineered high-output extrusion configuration |
| Extrusion capacity | Calculated according to pipe wall thickness, material grade and target output |
| Pipe die | Custom large-diameter PE die head |
| Calibration | Project-specific vacuum calibration and pipe sizing system |
| Cooling | Extended cooling system engineered for pipe mass and production speed |
| Haul-off | Heavy-duty pulling equipment designed for large-diameter pipe |
| Cutting | Customized large-diameter cutting system |
| Collection | Heavy-load support, pipe handling and tilt table arrangement |
| Production focus | Customized large-scale pipe manufacturing systems |
For projects requiring extra-large polyethylene pipes, EXTRUTEX offers customized engineering for production diameters up to 3500 mm. Such systems are designed around the actual product specification, plant layout, material handling requirements and production objectives.
| Item | Technical configuration |
|---|---|
| Pipe diameter | Customized configurations up to 3500 mm |
| Main extruder | Engineered high-output single-screw system; additional extrusion units where required by the product design |
| Pipe die | Custom-engineered large-diameter die and melt distribution system |
| Calibration | Project-specific sizing and vacuum arrangements |
| Cooling | Customized cooling tanks, spray systems and water circulation |
| Haul-off | Specially engineered heavy-duty pulling or pipe handling equipment |
| Cutting | Customized cutting and positioning system |
| Collection | Heavy-duty support, tilt table and pipe transfer solutions |
| Production capacity | Established through detailed project engineering |
| Production focus | Extra-large pipes for major infrastructure and specialized industrial projects |
Important engineering note: The HELIFEED output figures above are extruder reference capacities, not guaranteed finished-pipe output for every diameter. Actual production depends on wall thickness, SDR, material grade, pipe weight per meter, die design, cooling capacity, haul-off speed and the required product standard. The largest diameter configurations require project-specific validation of the complete line.
EXTRUTEX PE pipe extrusion lines can be configured for suitable polyethylene grades, including PE80 and PE100, subject to the material specification and application. The selected resin, additives and processing conditions must be compatible with the intended pipe performance requirements.
Gas distribution pipes require suitable approved materials, traceability, quality assurance and compliance with the applicable local standards. The production line alone does not certify the finished pipe for a particular application.
A modern PE pipe extrusion line requires coordinated control of the extruder, die, vacuum calibration tank, cooling system, haul-off and cutting equipment. EXTRUTEX can configure the control architecture according to the project requirements, including centralized operation, temperature regulation, variable-speed drives and synchronized downstream control.
Automation options are selected according to the required production accuracy, operating procedures and budget. Additional measuring instruments, data logging, remote monitoring and factory integration can be specified for suitable projects.
Consistent PE pipe quality depends on more than the extruder itself. The complete process must be balanced to maintain the specified outside diameter, wall thickness, roundness, surface appearance and mechanical performance.
The pipe die determines melt distribution, while vacuum calibration establishes the initial outside diameter. Cooling controls the pipe's thermal history, and the haul-off influences line speed and dimensional stability. Cutting and collection equipment must then handle the finished product without causing damage or deformation.
EXTRUTEX configures these systems as an integrated production line. Customers should define the required pipe standard, diameter tolerance, wall thickness, SDR range, resin grade, output target and inspection procedure during the technical specification stage.
EXTRUTEX does not treat every pipe factory as having identical production requirements. A compact line for irrigation pipes has different priorities from a high-output system for municipal water transmission or an extra-large pipe line for infrastructure construction.
Our engineering approach considers the entire production process, from material feeding and screw-and-barrel selection to die design, calibration, cooling, pulling, cutting and pipe collection. This helps ensure that the equipment configuration reflects the intended products and the practical limitations of the factory.
Available customization may include:
For multilayer PE pipes or specialized product structures, the line can be evaluated for additional extruders, co-extrusion dies and related equipment. Such configurations require a separate technical design and are not included automatically in a standard single-screw line.
EXTRUTEX can develop customized PE pipe extrusion systems for pipe diameters up to 3500 mm. The final configuration depends on the product design, pipe wall thickness, production capacity, factory layout and downstream handling requirements.
The established HELIFEED single-screw series includes 45/40, 60/40, 75/40, 90/40, 105/40, 125/40 and 150/40 configurations. The appropriate model is selected according to the pipe diameter, material, wall thickness and required output.
Yes. The standard equipment concept includes a vacuum calibration tank and spray cooling water tank, with their dimensions and capacities selected according to the production requirements.
Yes. Haul-off configuration, pulling capacity, cutting method and tilt table dimensions can be specified according to pipe size, finished length, weight and handling requirements.
Not necessarily with one unchanged tooling set. Production across a diameter range may require interchangeable dies, calibration sleeves, downstream adjustments and, for some applications, different equipment configurations. The final range must be confirmed during engineering.
Capacity is calculated using the extruder's usable output together with pipe diameter, wall thickness, resin density, line speed, cooling performance and downstream limitations. A confirmed production target should be established for each required pipe specification.
The line can be configured for suitable PE100 materials. Final suitability depends on the selected resin, tooling, process conditions, finished-pipe testing and applicable product standards.
Whether you are planning a compact 12–32 mm irrigation pipe line, a medium-diameter water pipe production system, a 630–1500 mm infrastructure line or a customized solution up to 3500 mm, EXTRUTEX can help define the appropriate extrusion and downstream configuration.
To prepare a suitable technical proposal, please provide the required pipe diameter range, PE material grade, wall thickness or SDR, target output in kg/h, finished pipe lengths, applicable standards and available factory space. These details allow the extruder, pipe die, vacuum calibration tank, spray cooling tanks, haul-off, cutting saw and tilt table to be selected as a coordinated production system.
EXTRUTEX – PE Pipe Extrusion Lines from 12 mm to 3500 mm. Customized extrusion technology for efficient, stable and application-focused polyethylene pipe manufacturing.
There are no reviews yet.
By submitting your email, you agree to our company’s terms and conditions.
We are not looking to sell; we are here to provide you with the best support and service.
Contact available 24/7
Please do not contact us for advertising or sales inquiries
All rights of this website are reserved for EXTRUTEX Austria and its partner companies, © 2026
-
(0 customer reviews)