No products in the cart.
All rights of this website are reserved for EXTRUTEX Austria and its partner companies, © 2026

Multiple Payment Methods

Discount for advance payments over 50%

Free Shipping Coordination Services
Payment methods:
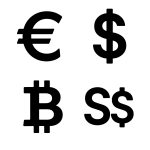

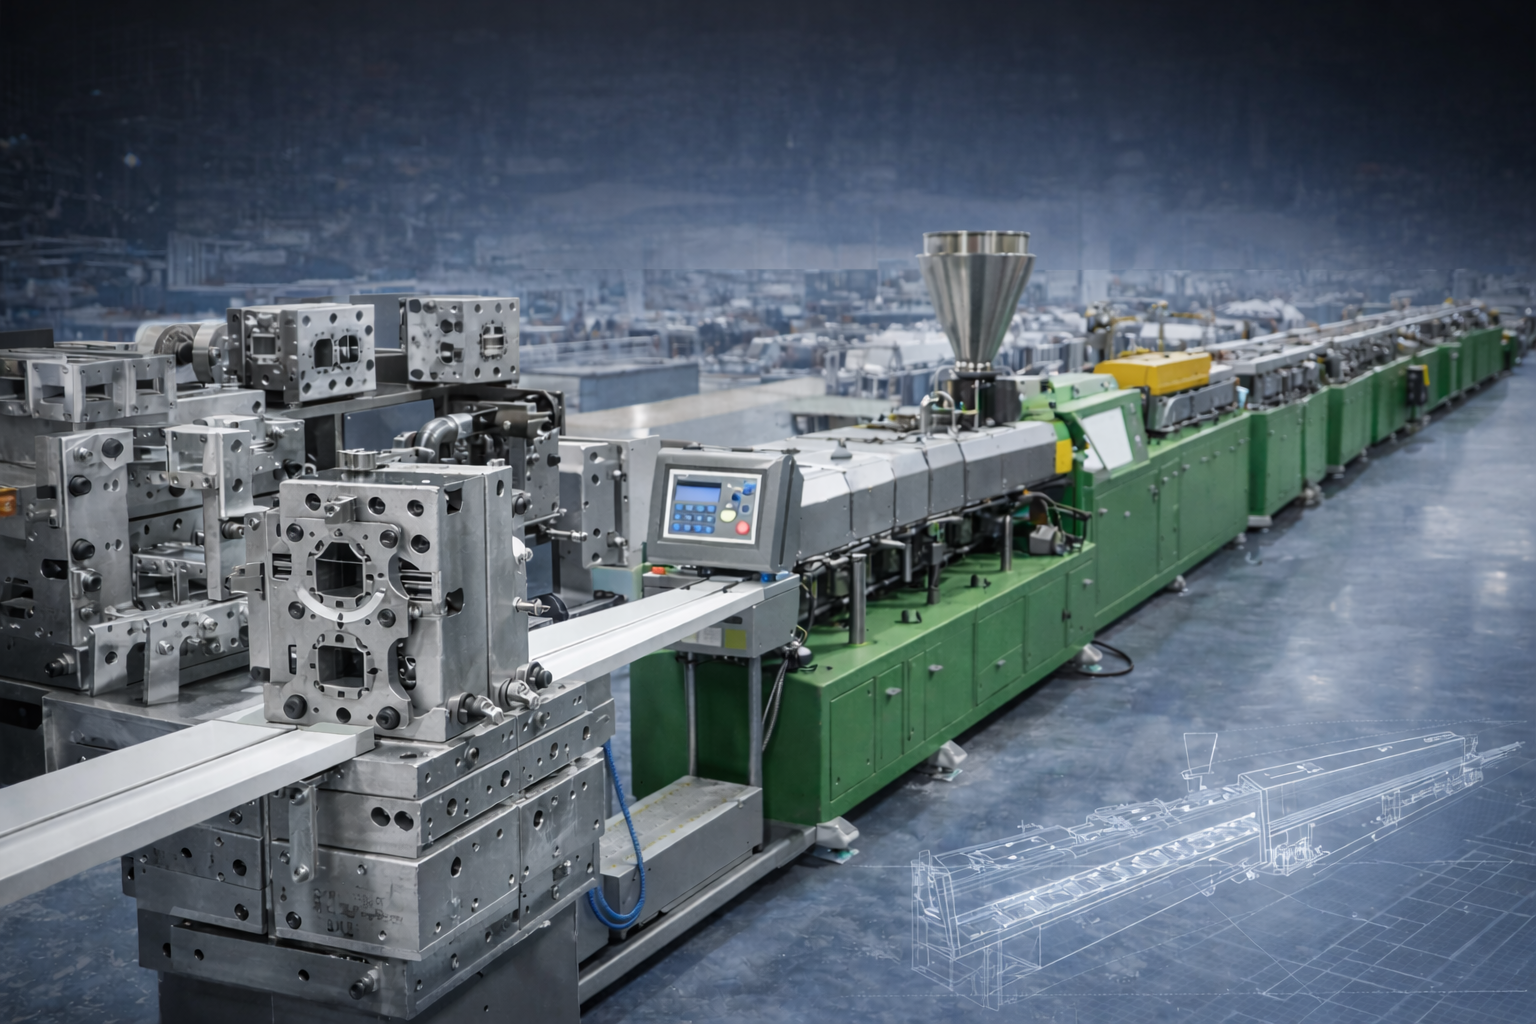
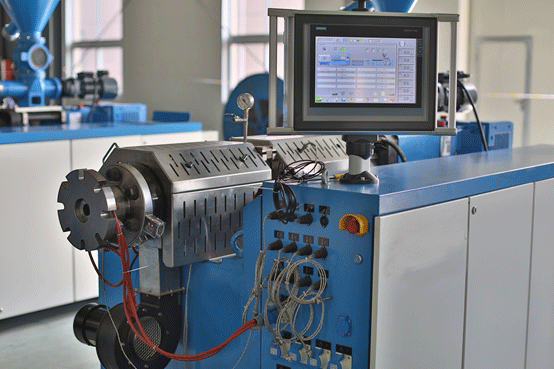
The EX65J drinking straw extrusion line is designed for continuous production of PP and PLA drinking straws. It integrates extrusion, cooling, hauling, cutting and collection into one coordinated production system, providing an efficient solution for standard drinking straw manufacturing.
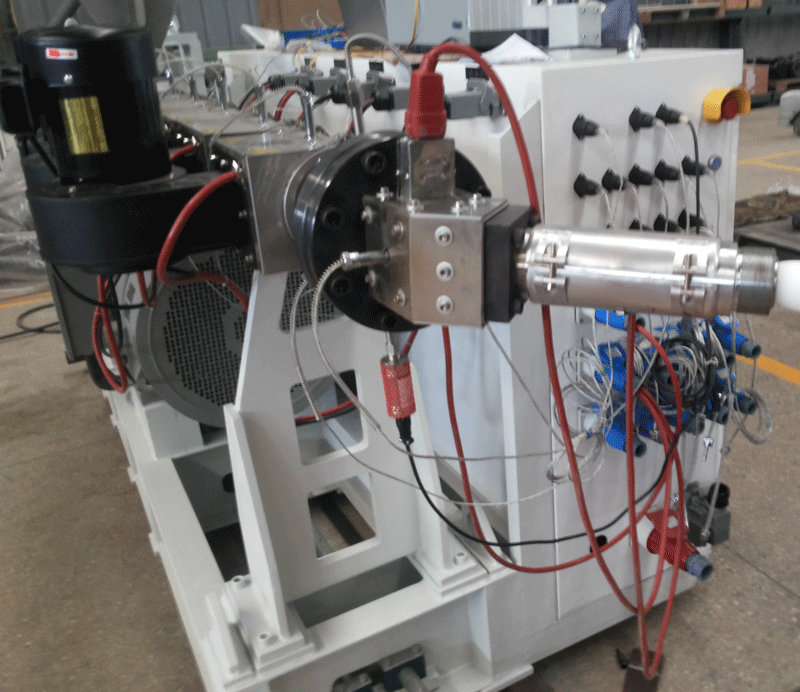
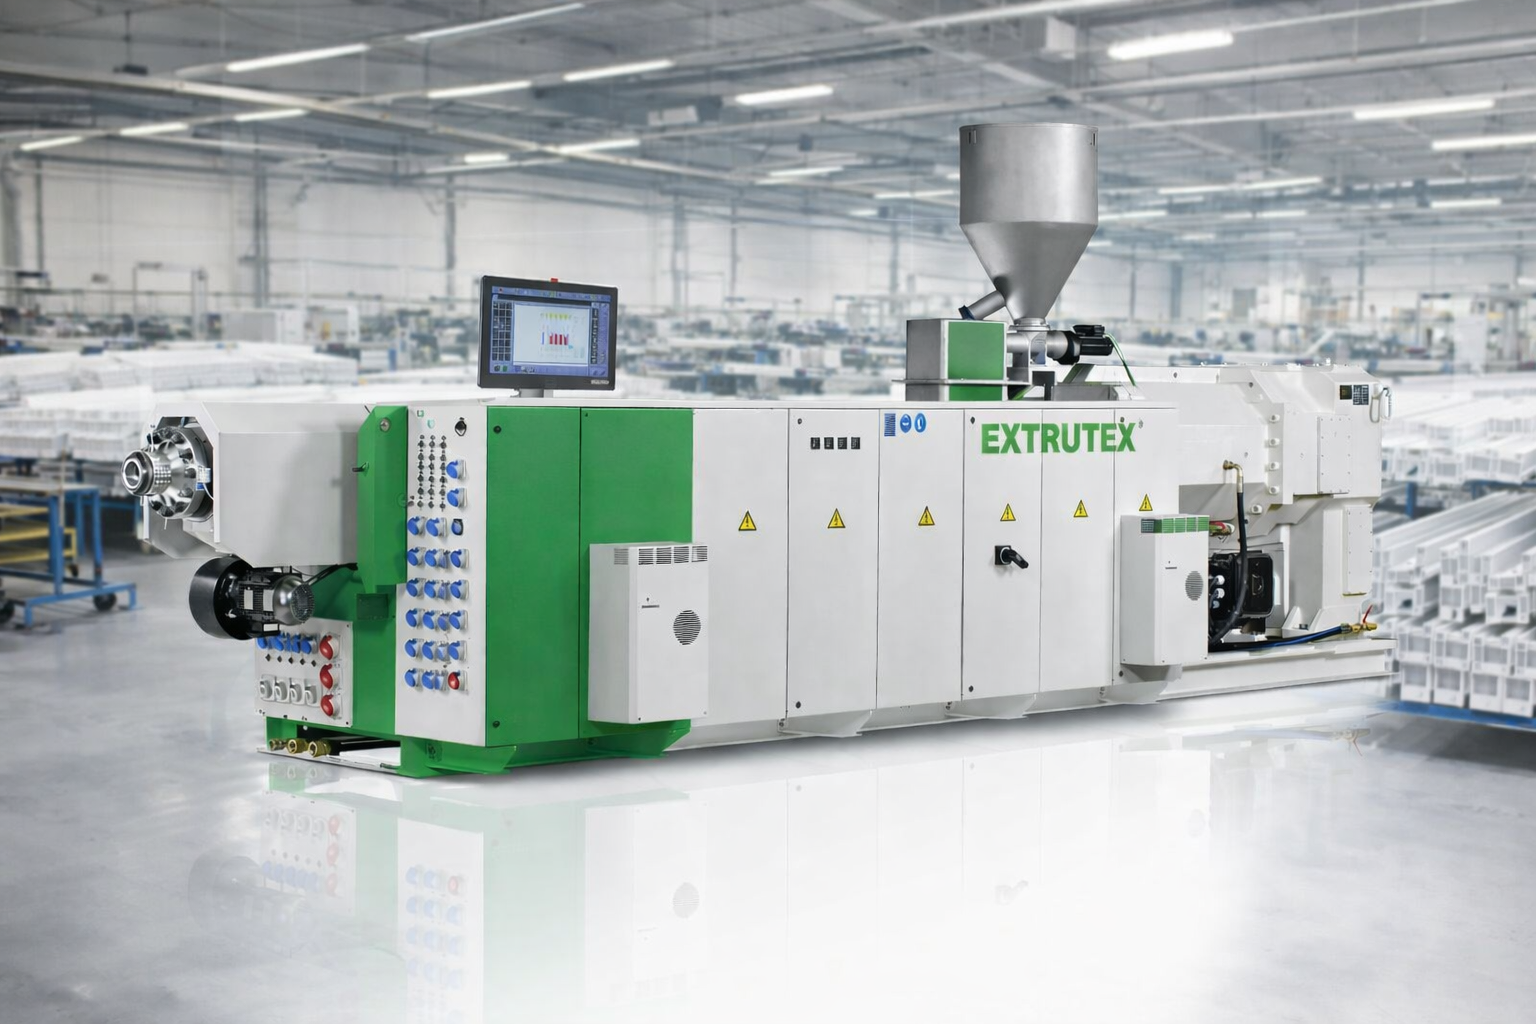
EXTRUTEX EX65J is a professional drinking straw extrusion line developed for manufacturers requiring stable and continuous production of standard PP and PLA drinking straws. The complete system combines a 65 mm extrusion unit with a cooling tank, haul-off system, cutting device, collection system and electrical control system.
The machine is designed around the requirements of small-diameter plastic tube extrusion. During production, the polymer is plasticized in the extruder and continuously formed through the extrusion tooling. The newly formed straw then enters the cooling and sizing section, where its dimensions are stabilized before being transported to the cutting unit. The finished straws are cut to the required length and transferred to the collection system.
Depending on straw diameter, wall thickness, length, polymer characteristics and production settings, the EX65J can reach production speeds from 400 to 1800 pieces per minute. The extrusion throughput is approximately 60–65 kg/h, while the actual piece output depends on the weight and dimensions of the finished straw.
The EX65J follows a straightforward continuous extrusion process. Each stage is coordinated to maintain stable dimensions and reliable cutting performance.
EXTRUTEX configures the EX65J as an integrated production line rather than as an isolated extruder. This approach allows the extrusion, cooling, traction and cutting stages to work together as a continuous production process.
The main extrusion system uses a 65 mm screw with a 33:1 L/D configuration. The 30 kW main motor is frequency controlled, allowing production speed and extrusion conditions to be adjusted according to material and straw size.
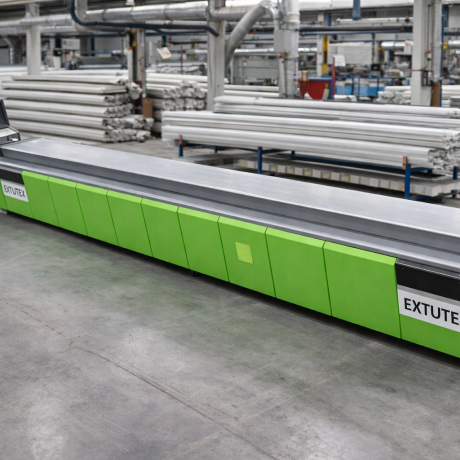
The cooling section stabilizes the freshly extruded straw after forming. The standard cooling tank is approximately 3.5 m long and can be customized according to the customer's production requirements.
The traction system continuously pulls the formed straw through the cooling section. Controlled hauling is important for maintaining consistent straw dimensions and production stability.
The cutting system separates the continuously extruded tube into individual drinking straws. Cutting performance is matched to the selected straw length and production speed.
After cutting, finished straws are transferred to a collection area for inspection, counting, packaging or further handling.
The electrical control system coordinates the main extrusion drive, traction and cutting functions. Frequency-controlled operation provides flexible adjustment for different PP and PLA production conditions.
The following specifications describe the standard EX65J configuration. Final machine configuration can be adapted according to straw diameter, material, production speed, voltage and other customer requirements.
| Item | Specification | Details |
|---|---|---|
| Main Extruder Motor | 30 kW | Frequency controlled |
| Extruder | 65 mm | Main extrusion unit |
| Screw L/D | 33:1 | 65/33 extrusion configuration |
| Extrusion Output | 60–65 kg/h | Depending on material and operating conditions |
| Production Speed | 400–1800 pcs/min | Depends on straw specification |
| Materials | PLA, PP | Standard configuration |
| Straw Diameter | Φ2–Φ13 mm | Production range |
| Straw Length | Customer specified | Determined by cutting configuration |
| Length Difference | 0.1–1 mm | According to production conditions |
| Traction Cutting Device | 0.75 kW × 2 | Traction and cutting drive configuration |
| Vacuum Sizing System | Not included | Optional/custom configuration |
| Cooling Tank | 3.5 m | Customizable |
| Control Mode | Frequency controlled | Adjustable operating speed |
| Application | Drinking Straws | PP and PLA production |
At the heart of the EX65J is a 65 mm extrusion system with a 33:1 screw length-to- diameter ratio. This configuration provides sufficient residence time and plasticizing capacity for continuous production of small-diameter drinking straws.
The 30 kW main motor uses frequency-controlled operation. This allows the operator to adjust extrusion speed according to polymer characteristics and finished straw requirements. For production environments where different straw sizes are manufactured on the same machine, variable-speed operation provides useful flexibility.
The extrusion process must maintain stable melt temperature and pressure. This is particularly important for PLA, where processing conditions need to be controlled carefully to achieve consistent plasticization and avoid unnecessary thermal degradation.
PLA is increasingly used for drinking straw production where manufacturers require alternatives to conventional petroleum-based plastics. The EX65J can be configured for PLA extrusion with process conditions adapted to the characteristics of the selected PLA grade.
PLA generally requires more controlled material handling than conventional PP. Moisture management is particularly important because excessive moisture can negatively affect melt processing and finished product quality. Depending on the PLA material supplied by the customer, a suitable drying system can be integrated before extrusion.
The cooling section is also important for PLA straw production. After the tube exits the forming die, controlled cooling helps stabilize the diameter and shape before the material reaches the haul-off and cutting stages.
Polypropylene remains a widely used material for standard drinking straws because of its processing characteristics, lightweight structure and suitability for high- speed extrusion. The EX65J provides frequency-controlled extrusion and continuous downstream processing for PP straw production.
Production conditions can be adjusted according to the selected PP grade, straw diameter, wall thickness and required finished length. The combination of extrusion, cooling, traction and cutting enables manufacturers to operate the complete line as one continuous production system.
Cooling is a critical stage in small-diameter straw extrusion. Immediately after the polymer leaves the extrusion tooling, the material is still hot and relatively flexible. The cooling tank removes heat and allows the extruded tube to stabilize before traction and cutting.
The standard EX65J cooling tank is approximately 3.5 metres long. The tank length can be customized depending on the production material, straw diameter, extrusion speed and available factory space.
A vacuum sizing system is not included in the standard configuration shown here. Where the production process requires additional sizing control, EXTRUTEX can evaluate and configure the appropriate vacuum sizing solution.
After cooling, the straw is continuously transported by the traction system toward the cutting section. The synchronization between hauling and cutting is essential when producing large quantities of short finished straws.
The EX65J can achieve production speeds from 400 to 1800 pieces per minute, depending on the product specification. Shorter and smaller straws can generally achieve higher piece counts, while larger diameters, thicker walls or longer products change the production rate.
The specified length difference is approximately 0.1–1 mm, with the final result depending on material behavior, machine adjustment, cutting conditions and product specifications.
Before ordering a drinking straw extrusion line, manufacturers should define the final product specification rather than selecting the machine only by motor power or nominal output. EXTRUTEX engineers can evaluate the complete process based on the required product dimensions and material.
EXTRUTEX offers different straw extrusion configurations according to the required level of process control. The EX65J is a practical solution for standard PP and PLA drinking straw production with frequency-controlled operation.
| Feature | EX65J | EX-65QS Full Servo |
|---|---|---|
| Main Drive | Frequency controlled | Full servo system |
| Standard Materials | PP, PLA | PP, PLA, PBS, PHA and other compatible materials |
| Extruder | 65 mm | 65 mm |
| Control Requirement | Standard production | Higher synchronization and control precision |
| Typical Application | Standard drinking straws | Advanced and higher-control straw production |
The EXTRUTEX PLA straw production concept focuses on stable plasticization, controlled processing temperature and efficient continuous operation. Proper temperature management helps maintain consistent melt quality while avoiding unnecessary heating and cooling losses.
The production line developed around PLA material characteristics is intended to provide accurate temperature control and efficient material plasticization. By coordinating the extrusion and downstream sections, manufacturers can maintain a stable production process while optimizing operating conditions for the selected PLA grade.
Extrusion, cooling, hauling and cutting are integrated into one continuous production process.
The system is designed for straw diameters from approximately Φ2 to Φ13 mm, subject to tooling and process configuration.
Production speed can reach up to 1800 pieces per minute for suitable straw specifications and operating conditions.
The standard machine is designed for PP and PLA drinking straw production, with process configuration matched to the material.
The standard 3.5 m cooling tank can be customized according to line layout and production requirements.
Frequency-controlled operation allows production speed to be adjusted for different materials and straw specifications.
Before installation, the customer should confirm factory space, electrical supply, compressed air requirements where applicable, cooling-water conditions and material handling arrangements. The complete line layout should provide sufficient space for operation, maintenance and finished-product collection.
Material preparation is particularly important when processing PLA. If the selected PLA grade requires drying, a suitable dryer and material-loading system should be included in the production configuration.
EXTRUTEX can configure the extrusion line according to local electrical standards, production requirements and the customer's preferred downstream arrangement.
EXTRUTEX develops and supplies plastic extrusion machinery based on European engineering principles and practical industrial manufacturing requirements. The EX65J drinking straw extrusion line is produced under the EXTRUTEX engineering concept with manufacturing capabilities in China.
EXTRUTEX combines Austrian design and engineering standards with manufacturing resources in Nanjing and Shanghai, China. This structure allows the company to provide technically customized extrusion solutions while maintaining competitive manufacturing efficiency.
For drinking straw manufacturers, EXTRUTEX can support the selection of the extrusion configuration, tooling, cooling section, haul-off, cutting system and auxiliary equipment according to the required product.
Rather than selecting equipment only according to nominal machine size, EXTRUTEX considers the complete production process, including material characteristics, diameter, wall thickness, length, output, cooling requirements and cutting speed. This approach helps ensure that the extrusion line is matched to the actual finished product.
| Parameter | EX65J |
|---|---|
| Machine Type | Drinking Straw Extrusion Line |
| Manufacturer | EXTRUTEX |
| Design | Austrian Design |
| Manufacturing | China — Nanjing and Shanghai |
| Materials | PP, PLA |
| Main Extruder | 65 mm, L/D 33:1 |
| Main Motor | 30 kW, Frequency Controlled |
| Extrusion Output | 60–65 kg/h |
| Production Speed | 400–1800 pcs/min |
| Straw Diameter | Φ2–Φ13 mm |
| Cooling Tank | 3.5 m, customizable |
| Vacuum Sizing | Not included in standard configuration |
| Production Process | Extrusion → Cooling → Hauling → Cutting → Collection |
The EXTRUTEX EX65J drinking straw extrusion line is a practical solution for continuous production of PP and PLA drinking straws. With a 65 mm, 33:1 extrusion system, 30 kW frequency-controlled main motor, integrated cooling, hauling and cutting, the line provides a complete production platform for standard straw manufacturing.
Its production range of approximately 400–1800 pieces per minute and extrusion throughput of 60–65 kg/h provide flexibility for different straw specifications. The 3.5 m cooling tank can also be customized according to material, product size and factory layout.
For standard PP and PLA production, the EX65J provides a cost-effective and straightforward configuration. For manufacturers requiring full servo control, enhanced synchronization or broader biodegradable-material compatibility, EXTRUTEX can provide the EX-65QS full servo straw extrusion solution.
With Austrian design and manufacturing in Nanjing and Shanghai, China, EXTRUTEX provides complete extrusion solutions for plastic and polymer processing applications, from individual machines to customized production lines.
There are no reviews yet.
By submitting your email, you agree to our company’s terms and conditions.
We are not looking to sell; we are here to provide you with the best support and service.
Contact available 24/7
Please do not contact us for advertising or sales inquiries
All rights of this website are reserved for EXTRUTEX Austria and its partner companies, © 2026
-
(0 customer reviews)