EXTRUTEX ERC-63 – U-PVC Profile Extrusion Machine
High-Performance Conical Twin Screw Extruder for U-PVC Profile Production
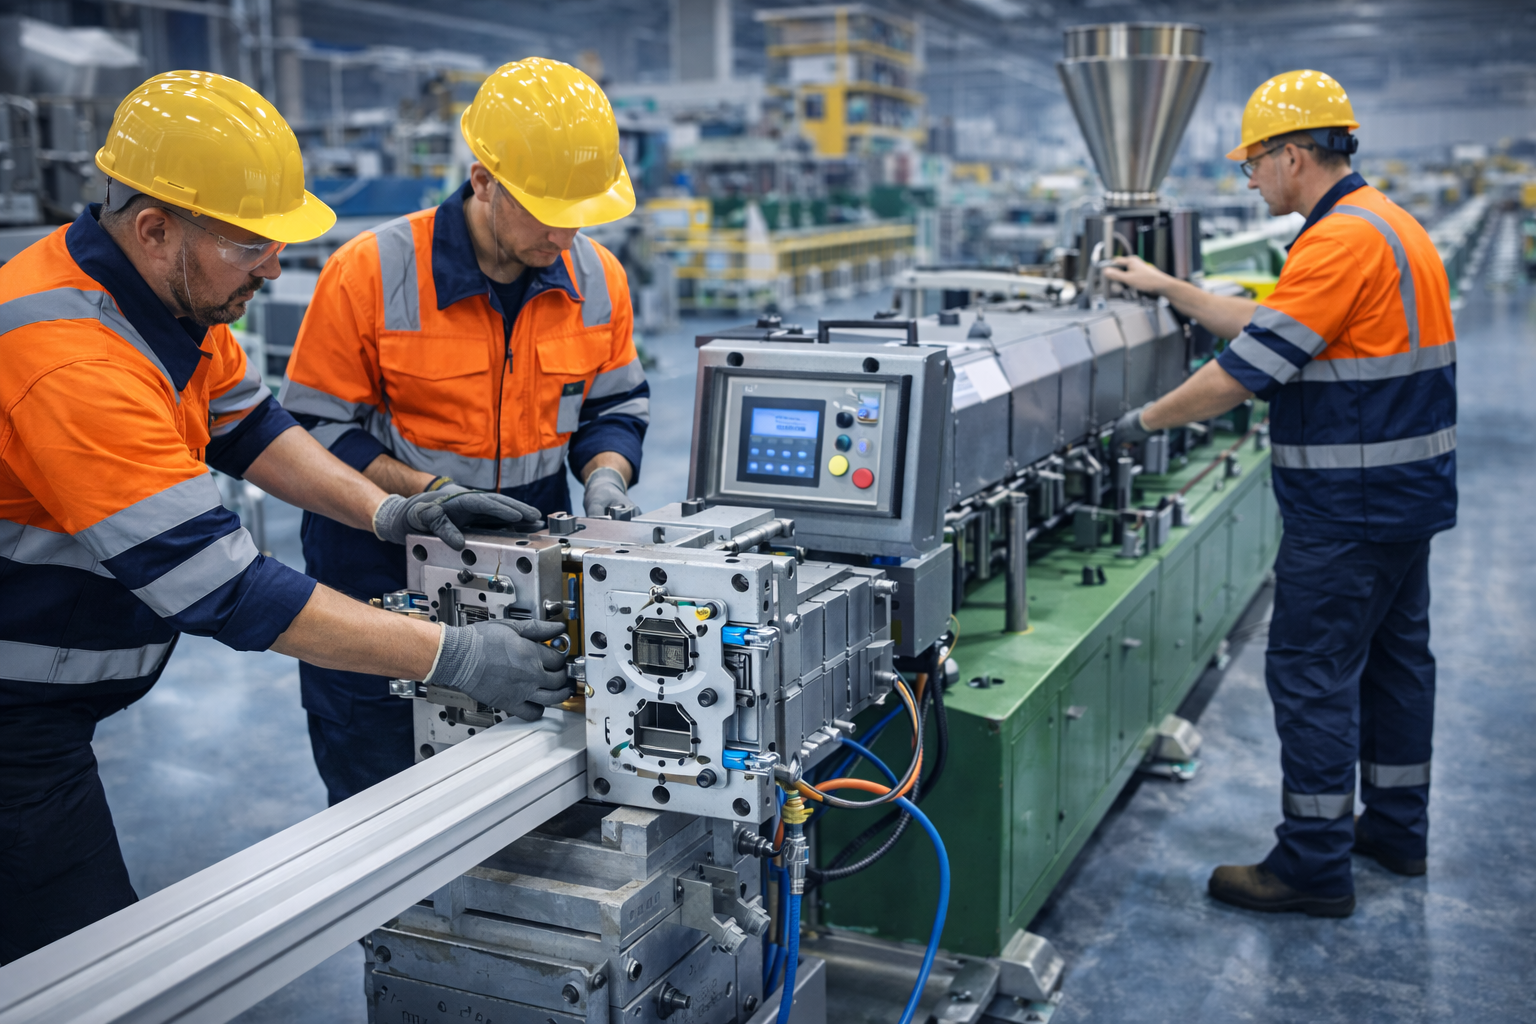
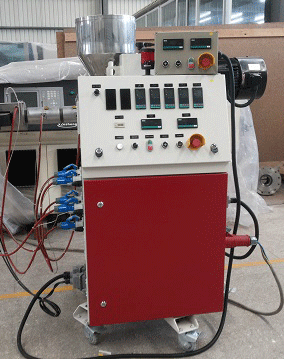
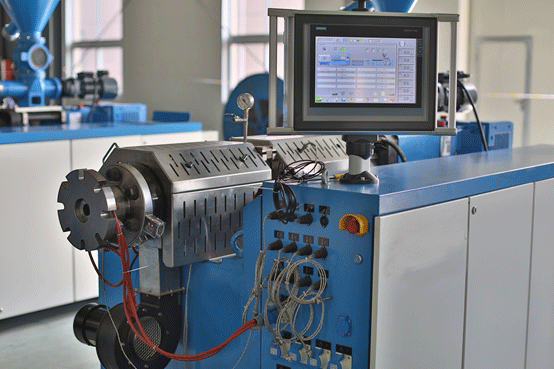
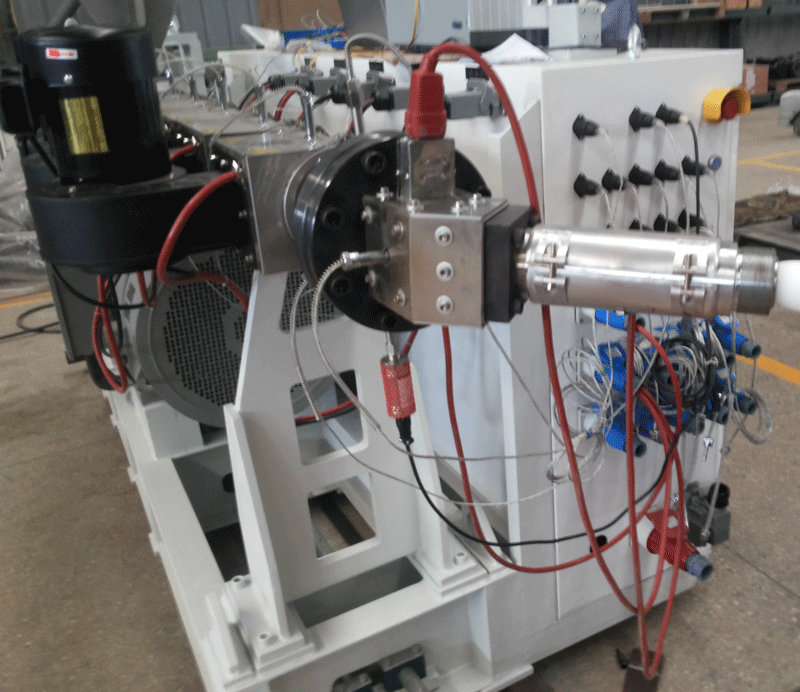
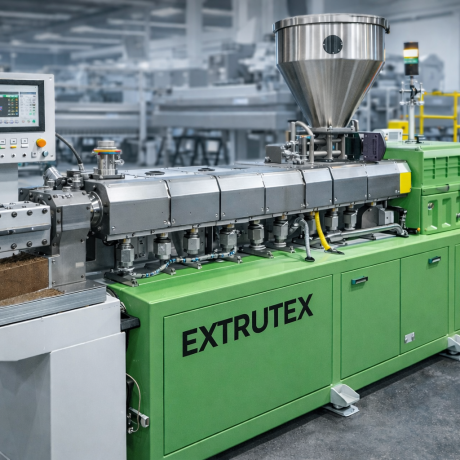
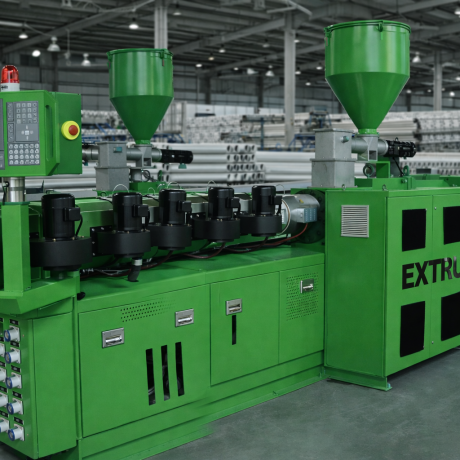
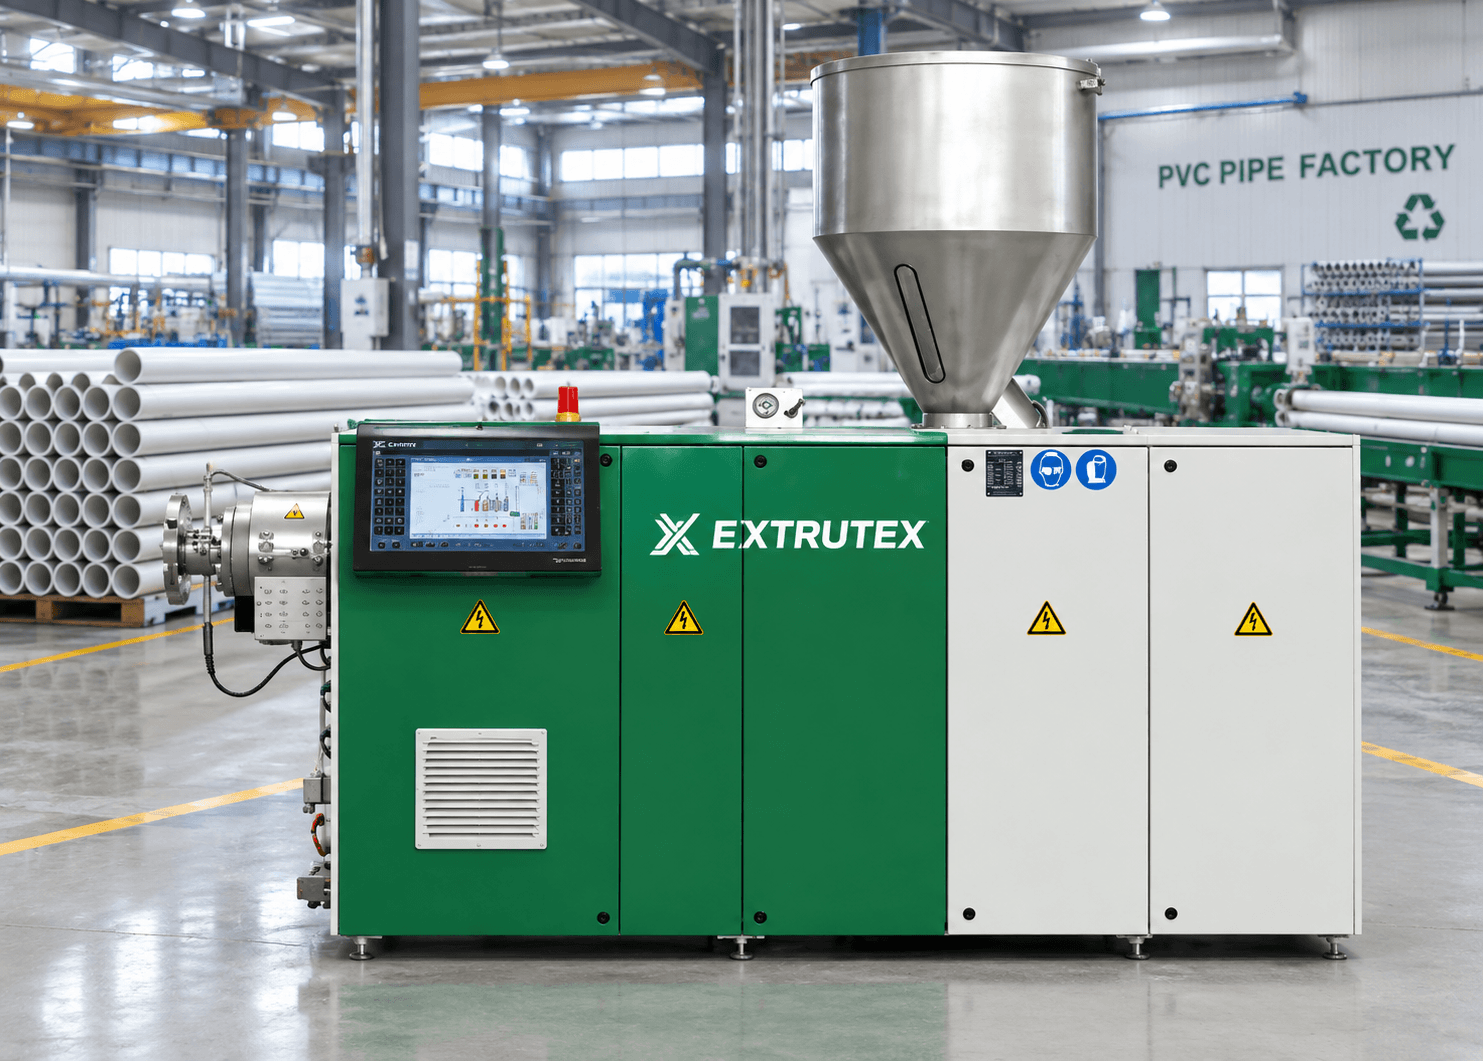
The EXTRUTEX ERC-63 is a high-performance conical twin screw extruder specially designed for the production of U-PVC profiles. With a production capacity of approximately 70–220 kg/h and a 37 kW main motor, the ERC-63 provides a flexible and reliable extrusion platform for manufacturers producing window profiles, door profiles, construction profiles, decorative profiles, technical profiles and other rigid PVC extrusion products.
Designed for continuous industrial production, the ERC-63 combines efficient PVC plasticization, stable melt pressure, accurate temperature control and consistent material conveying. Its conical twin screw configuration is particularly suitable for processing U-PVC dry blends and calcium-zinc stabilized PVC formulations used in modern profile extrusion.
Technical Specifications
| Model |
Application |
Output |
Main Motor |
| ERC-63 |
U-PVC Profile Extrusion |
70–220 kg/h |
37 kW |
Designed for U-PVC Profile Extrusion
The EXTRUTEX ERC-63 is engineered specifically for rigid PVC profile production. Its extrusion system provides controlled conveying, mixing and plasticization of U-PVC materials before the melt enters the profile die.
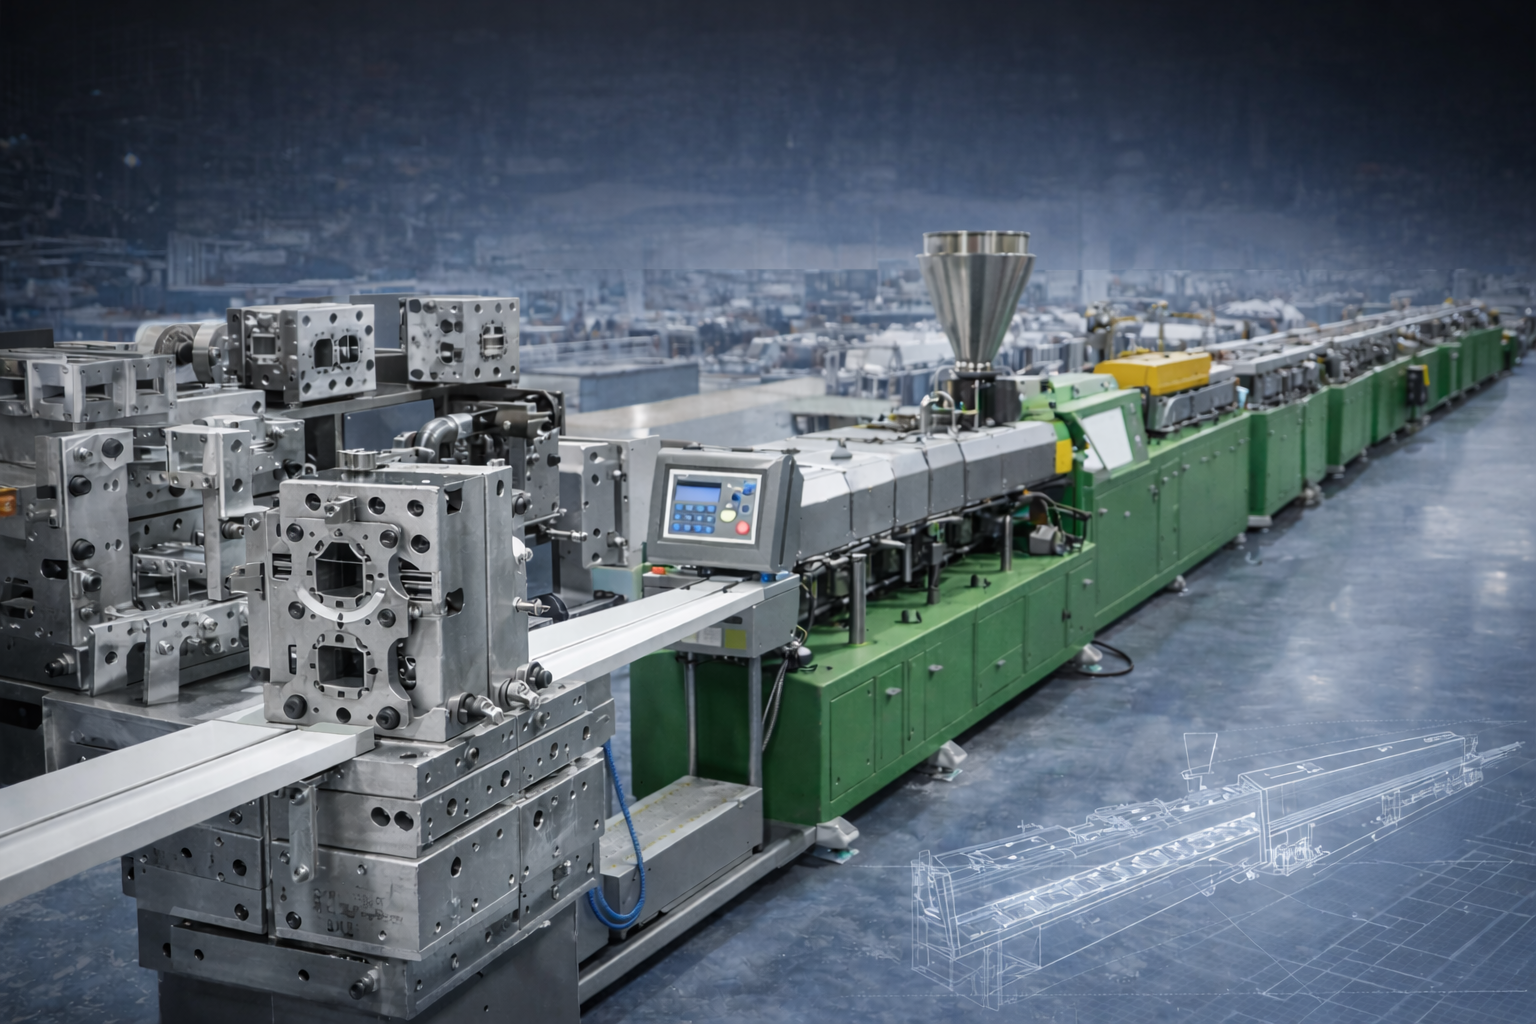
The machine can be integrated with complete downstream equipment including a profile die, vacuum calibration table, cooling system, haul-off, cutting unit and automatic stacking table. This allows the ERC-63 to operate as the main extrusion unit of a complete U-PVC profile production line.
Applications of EXTRUTEX ERC-63
- U-PVC window profiles
- U-PVC door profiles
- PVC window frames
- PVC door frames
- Sliding window profiles
- Glazing profiles
- Beading profiles
- Frame profiles
- Sash profiles
- Corner profiles
- Partition profiles
- Construction profiles
- Decorative PVC profiles
- Technical PVC profiles
- Furniture and interior profiles
- Special customized PVC profiles
Conical Twin Screw Extrusion Technology
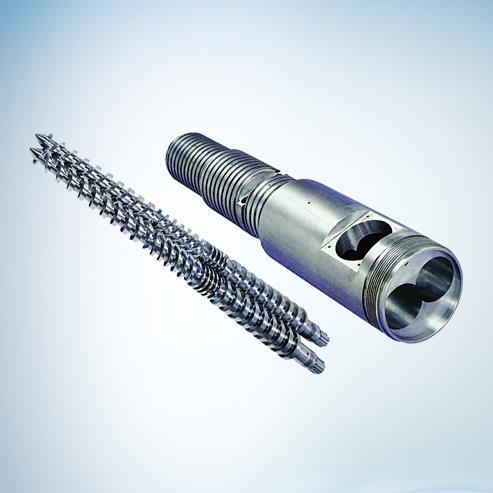
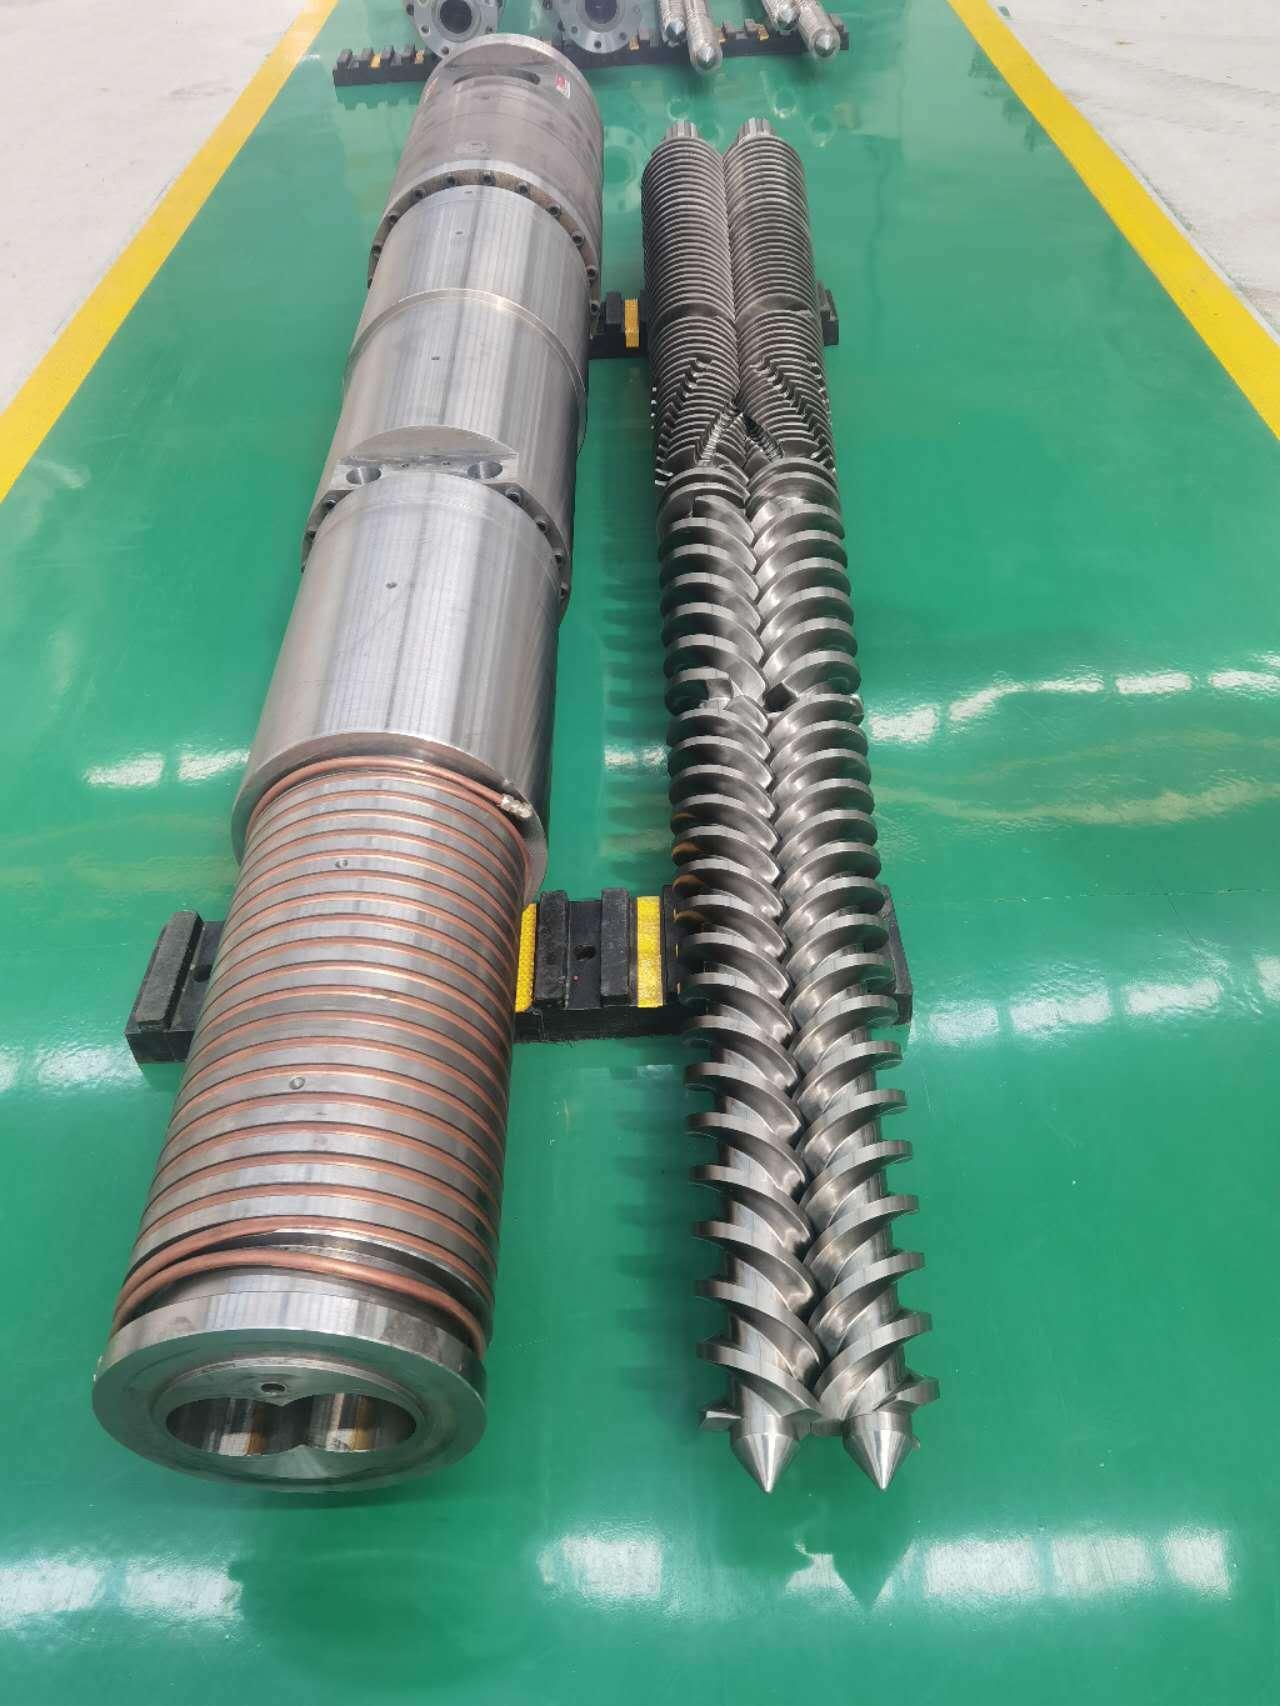
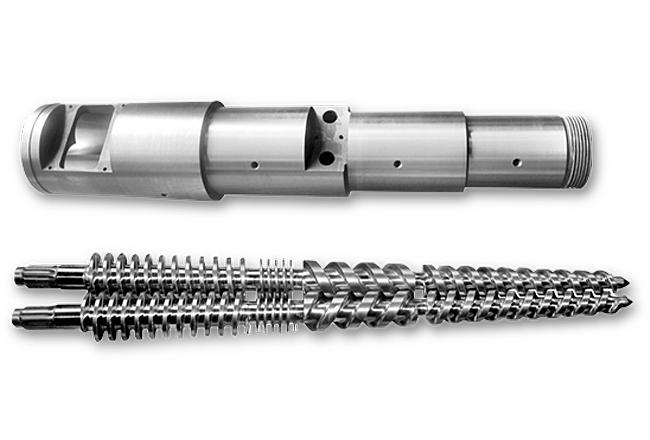
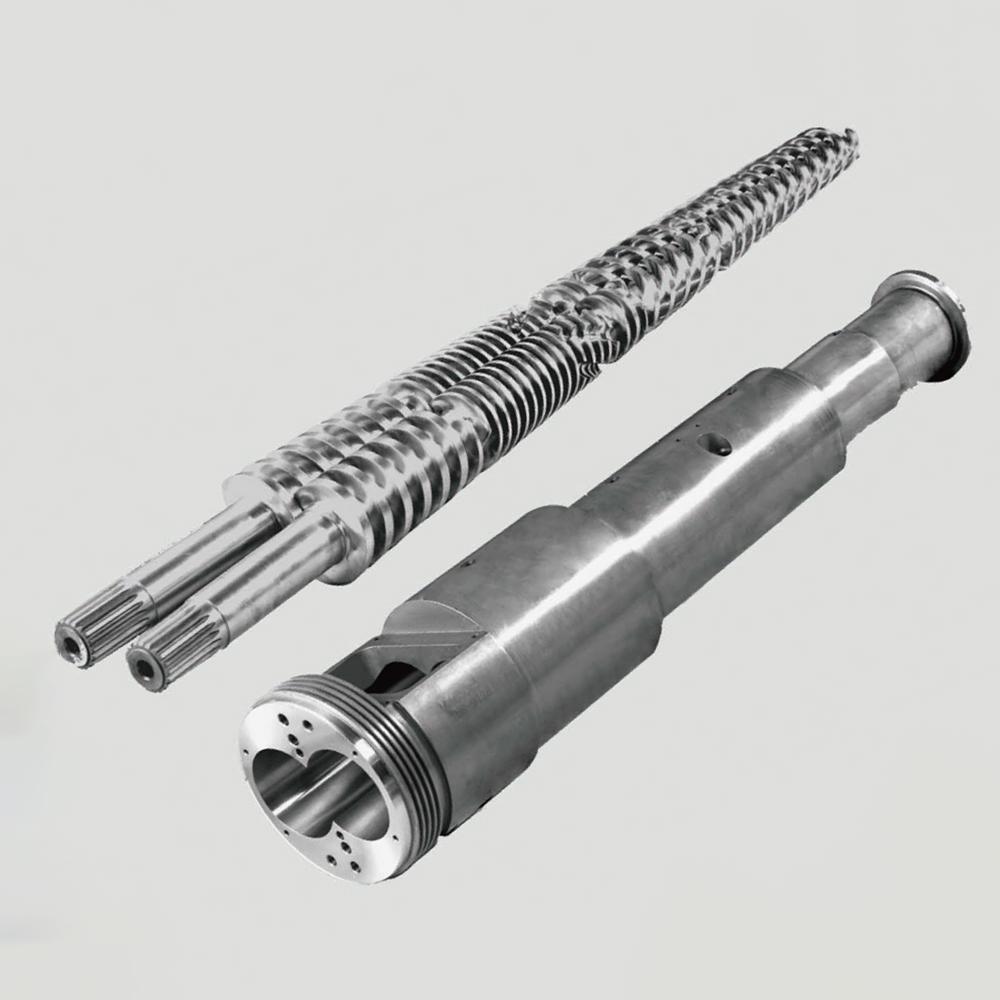
The ERC-63 uses a conical twin screw extrusion system designed for efficient processing of rigid PVC compounds. The twin screw arrangement provides effective conveying, mixing and plasticization while maintaining stable processing conditions.
Conical twin screw technology is widely used for U-PVC profile extrusion because it provides the torque and processing characteristics required for PVC dry blends. The screw geometry can be optimized according to the PVC formulation, profile design and required production conditions.
The ERC-63 offers a practical combination of production capacity, extrusion stability and compact machine configuration for medium-scale and industrial U-PVC profile manufacturing.
37 kW Main Drive System
The 37 kW main motor provides the required drive power for stable continuous extrusion within the 70–220 kg/h production range. The drive system is designed to provide controlled screw operation and consistent material conveying during production.
Stable screw speed is important for maintaining uniform output, melt pressure and profile dimensions. The ERC-63 drive system therefore works together with the feeding, heating and temperature-control systems to maintain consistent extrusion conditions.
Stable PVC Plasticization
U-PVC requires carefully controlled processing to achieve stable quality. The ERC-63 is designed to provide controlled melting and homogenization of PVC compounds before the material enters the profile die.
The extrusion process can be adjusted according to the PVC formulation, stabilizer system, profile geometry and required production speed. This makes the ERC-63 suitable for a wide range of rigid PVC profile applications.
Temperature Control System
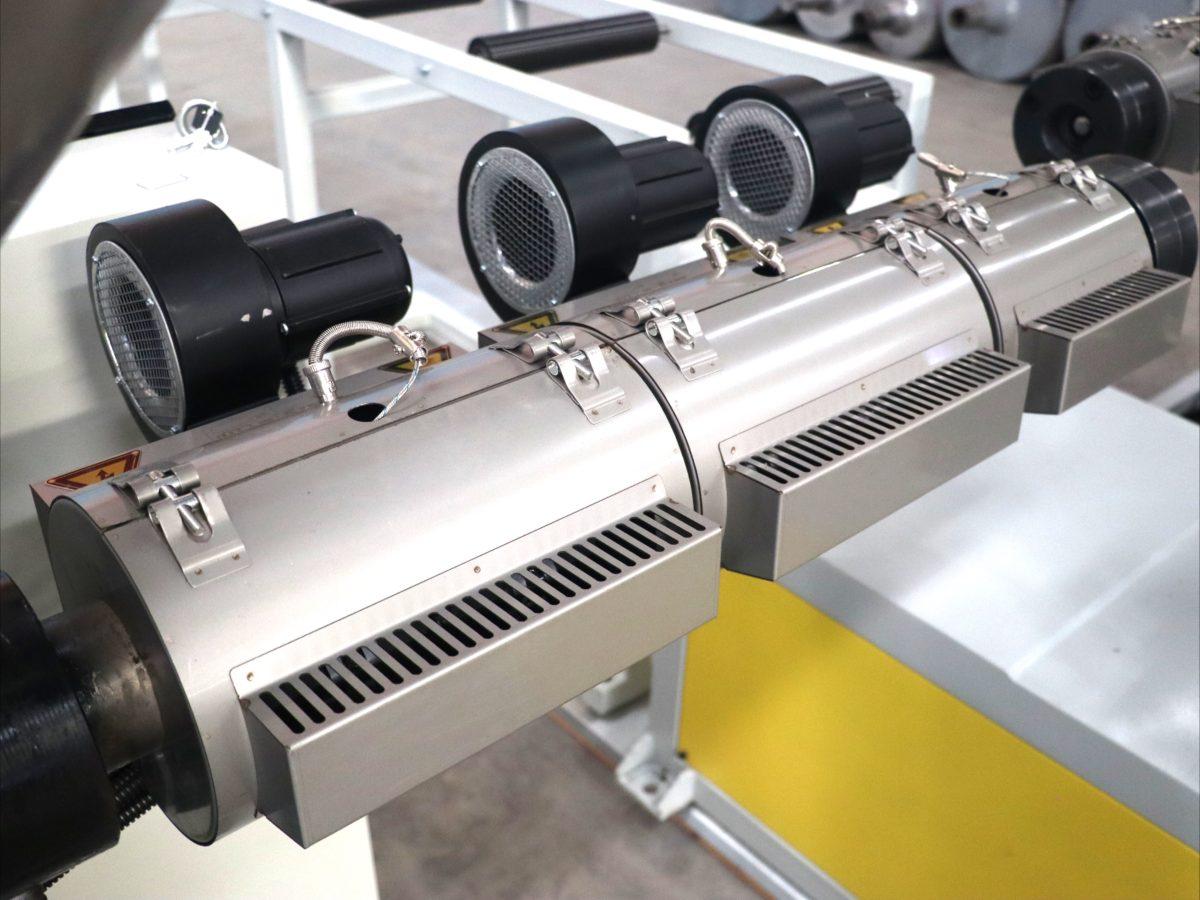
Accurate temperature control is essential for high-quality PVC profile production. The ERC-63 is equipped with controlled heating and cooling zones to help maintain stable processing temperatures throughout the extrusion barrel.
Processing zones can be monitored and adjusted according to the characteristics of the PVC formulation. Stable temperature conditions help improve melt consistency, profile surface quality and long-term production stability.
U-PVC Dry Blend Compatibility
The EXTRUTEX ERC-63 can be configured for common U-PVC dry blend formulations used in profile extrusion. Depending on the application, formulations may include PVC resin, calcium carbonate, processing modifiers, impact modifiers, pigments, lubricants and calcium-zinc stabilizer systems.
The machine can also be adapted to different formulations according to the required profile performance, color, surface finish and production conditions.
Profile Tooling and Die Systems
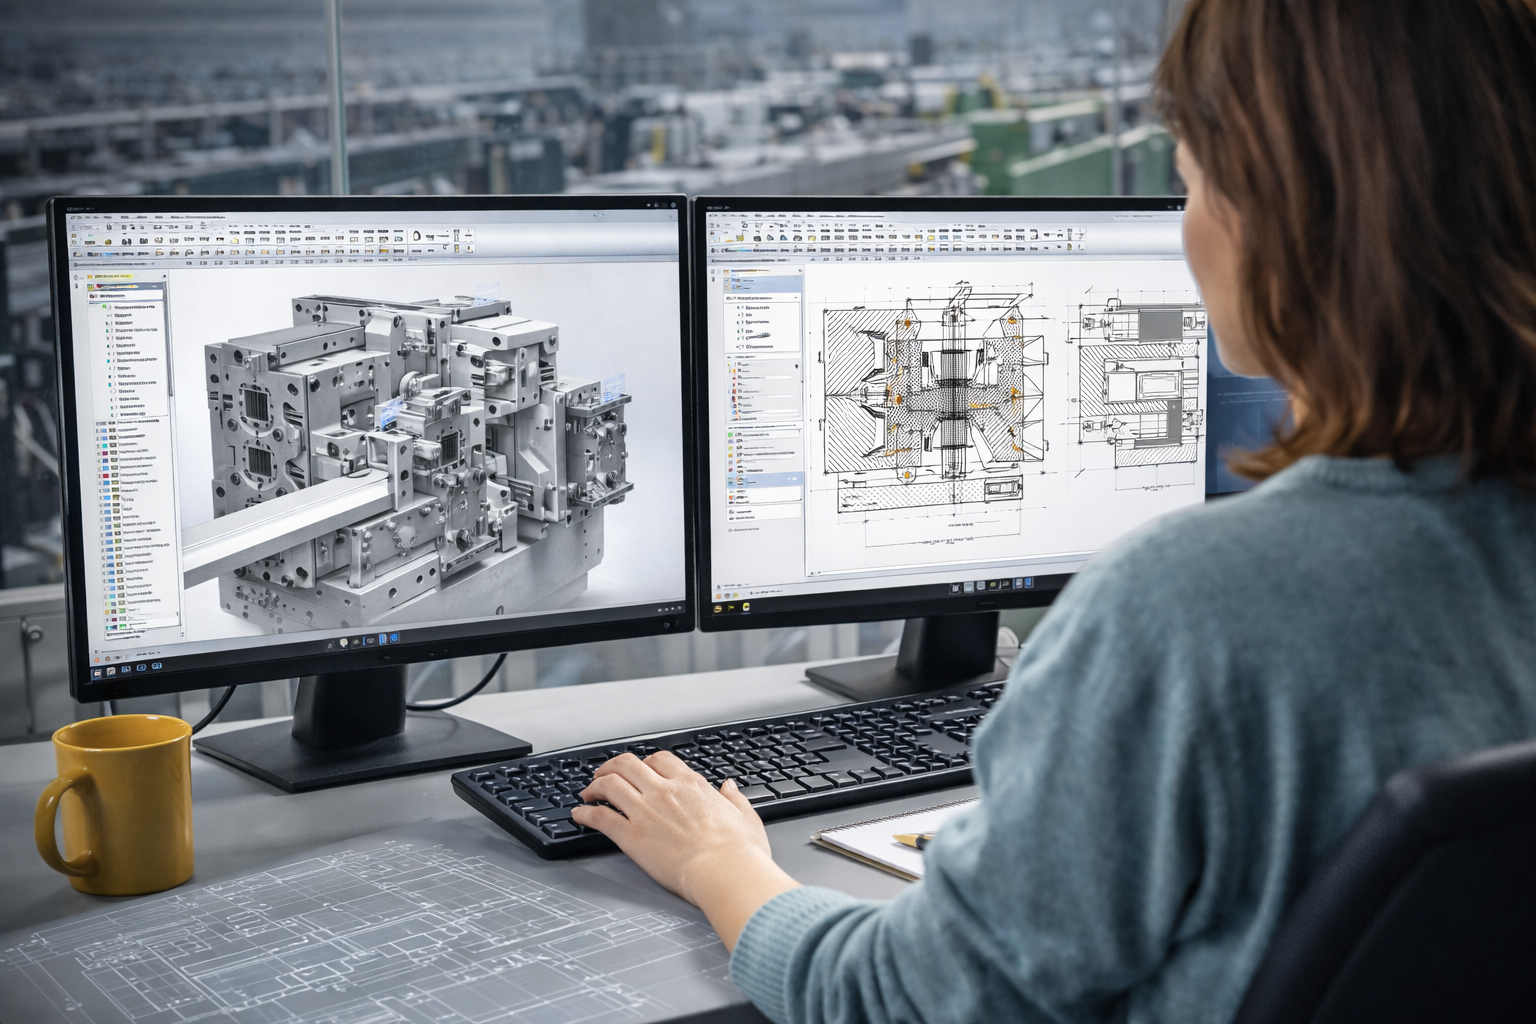
For complete production solutions, EXTRUTEX can supply the appropriate U-PVC profile tooling and extrusion dies for the ERC-63. The die design is an important part of the extrusion process because it determines the initial profile geometry and material distribution.
EXTRUTEX can develop customized profile tooling according to customer drawings, profile dimensions, cavity design, wall thickness and production requirements.
Complete Downstream Equipment
The ERC-63 can be integrated with a complete U-PVC profile extrusion downstream system, including:
- U-PVC profile extrusion die
- Vacuum calibration table
- Cooling and calibration system
- Profile haul-off
- Automatic cutting machine
- Length measurement system
- Automatic stacking table
- Profile handling equipment
The downstream equipment can be configured according to profile size, profile geometry, production speed and required automation level.
Vacuum Calibration and Cooling
After leaving the extrusion die, the hot U-PVC profile enters the calibration and cooling section. Accurate vacuum calibration helps establish the final dimensions of the profile while controlled cooling maintains dimensional stability.
The calibration system can be designed according to the profile geometry and production requirements. Different vacuum calibration configurations can be supplied for window, door, construction and technical profiles.
Profile Haul-Off System
A stable haul-off system is essential for maintaining consistent profile dimensions and surface quality. The EXTRUTEX downstream system provides controlled traction after the calibration and cooling section.
The haul-off speed can be synchronized with the extruder output and profile dimensions. This allows manufacturers to maintain stable production conditions during continuous production.
Cutting and Automatic Stacking
After the profile reaches the required cooling condition, the cutting system can produce accurately measured lengths for packaging or further processing. Automatic stacking equipment can then collect and organize the finished profiles.
The cutting and stacking configuration can be customized according to the profile type, length, production speed and factory layout.
Surface Quality and Dimensional Stability
For window and door profile manufacturers, appearance and dimensional accuracy are critical. The ERC-63 extrusion system is designed to provide stable melt conditions that support consistent profile geometry and good surface quality.
Correct screw configuration, temperature settings, die design, calibration and haul-off synchronization are all important factors in achieving a high-quality finished profile.
Window and Door Profile Production
The ERC-63 is suitable for the production of a wide range of U-PVC window and door system components. EXTRUTEX can support manufacturers with extrusion equipment, profile tooling and complete downstream equipment.
Profiles can be developed according to local construction requirements, architectural designs and customer-specific window and door systems.
Customized Profile Extrusion Solutions
Every PVC profile production project can have different requirements. Profile dimensions, number of cavities, wall thickness, formulation, output, surface finish and cutting length can all influence the extrusion line configuration.
EXTRUTEX can configure the ERC-63 according to the customer's specific profile requirements and production targets. Customized solutions can include the extruder, tooling, calibration system, haul-off, cutting, stacking and auxiliary equipment.
70–220 kg/h Production Capacity
With a production range of approximately 70–220 kg/h, the ERC-63 is suitable for manufacturers requiring a flexible U-PVC profile extrusion platform. The machine can be used for standard profile production as well as customized profile projects.
Actual production capacity depends on factors including the PVC formulation, profile geometry, wall thickness, die design, screw configuration, temperature settings and operating conditions. EXTRUTEX engineers can select and configure the extrusion system according to the required application.
Automation and Process Control
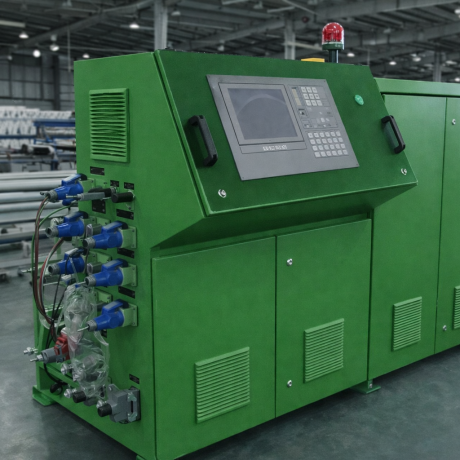
The ERC-63 can be supplied with modern control and monitoring systems for extrusion temperature, screw speed, feeding, motor operation and production conditions. Automation can also be extended to the downstream equipment to create a synchronized profile extrusion line.
A centralized control system helps operators monitor the complete production process and adjust operating parameters efficiently.
Low Maintenance Design
The ERC-63 is designed for industrial operation with attention to accessibility and maintenance. Important components can be inspected and serviced as part of a planned maintenance program.
Regular inspection of the screws, barrel, gearbox, heaters, cooling system, feeding system and downstream equipment helps maintain stable production and extend machine service life.
Screw & Barrel System
The screw and barrel configuration is selected according to the requirements of U-PVC profile extrusion. Proper screw geometry is important for controlled conveying, mixing, plasticization and pressure generation.
EXTRUTEX can provide screw & barrel configurations according to the PVC formulation, profile application and desired production range.
Gearbox and Drive Engineering
The extrusion drive system is matched with the conical twin screw configuration to provide stable torque transmission during continuous PVC processing. Gearbox selection and mechanical design are important for achieving reliable operation under demanding production conditions.
EXTRUTEX can also provide specialized extruder gearbox solutions and supporting drive components according to the machine configuration and customer requirements.
Austrian Engineering Experience
EXTRUTEX combines modern manufacturing capabilities with European engineering know-how. Our engineering team works with extensive experience in plastic extrusion, PVC profile systems, extrusion tooling and complete production lines.
This engineering approach allows EXTRUTEX to provide solutions covering the complete process, from raw material processing and extrusion through tooling, calibration, cooling, haul-off, cutting and final profile handling.
OEM Manufacturing and Global Support
The EXTRUTEX ERC-63 can be supplied as an OEM extrusion solution for PVC profile manufacturers, distributors and complete-line integrators. Machine configurations can be adapted according to production requirements, factory conditions and local market applications.
EXTRUTEX provides technical support for installation, commissioning, operator training, process optimization and spare parts. Long-term after-sales support is available to help customers maintain reliable production throughout the machine's service life.
Why Choose EXTRUTEX ERC-63?
- Designed specifically for U-PVC profile extrusion
- Conical twin screw extrusion technology
- 70–220 kg/h production capacity
- 37 kW main motor
- Suitable for window and door profiles
- Suitable for construction and technical profiles
- Compatible with U-PVC dry blend formulations
- Stable plasticization and melt processing
- Professional PVC profile tooling options
- Complete downstream equipment integration
- Customized extrusion line configurations
- Industrial automation and process control options
- OEM manufacturing solutions
- European engineering support
- Long-term technical and after-sales support
EXTRUTEX ERC-63 – Complete U-PVC Profile Extrusion Solution
The EXTRUTEX ERC-63 provides a flexible extrusion platform for manufacturers of U-PVC window profiles, door profiles, construction profiles, decorative profiles and technical PVC products. With a 37 kW main drive and a production range of approximately 70–220 kg/h, the machine is designed for stable and efficient rigid PVC processing.
Combined with professional profile tooling, vacuum calibration, cooling, haul-off, cutting and stacking equipment, the ERC-63 can form the core of a complete U-PVC profile production line. EXTRUTEX can configure the complete system according to the customer's profile design, production capacity and factory requirements.



-
(0 customer reviews)