No products in the cart.
All rights of this website are reserved for EXTRUTEX Austria and its partner companies, © 2026
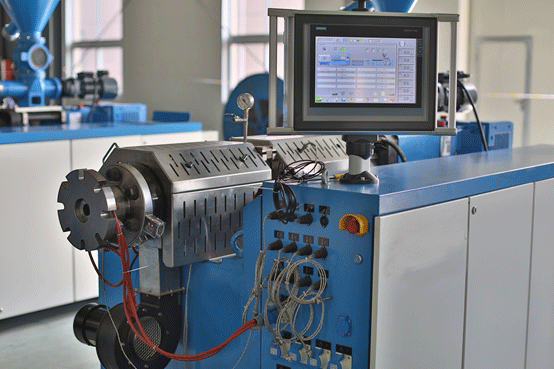
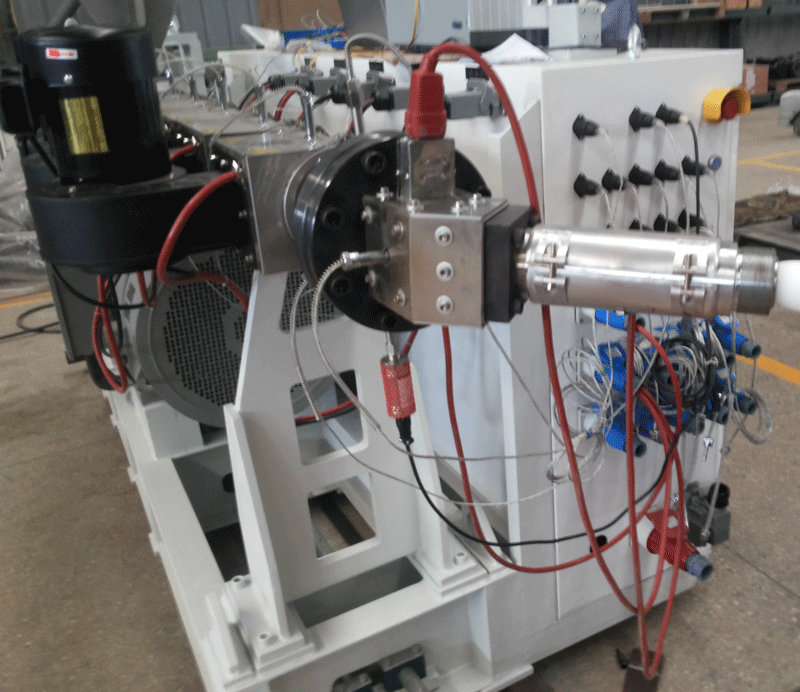
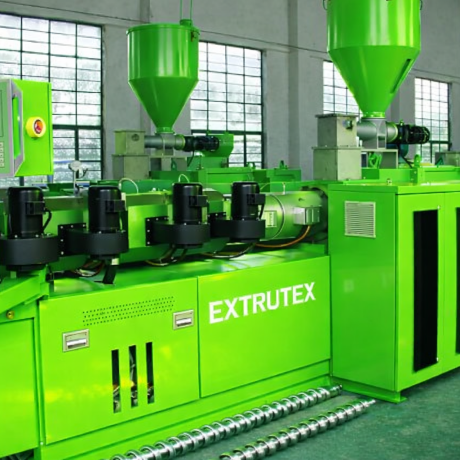
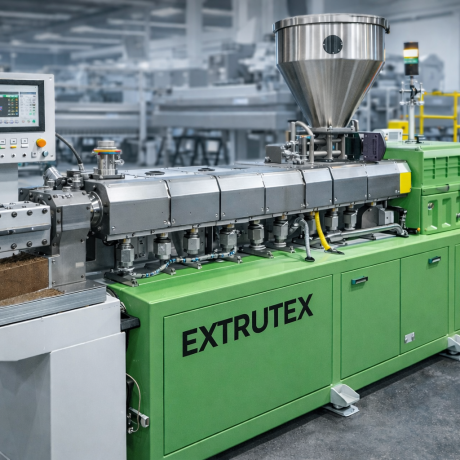
EXTRUTEX EXCT-50 Co-Rotating Twin-Screw Extruder

Multiple Payment Methods

Discount for advance payments over 50%

Free Shipping Coordination Services
Payment methods:
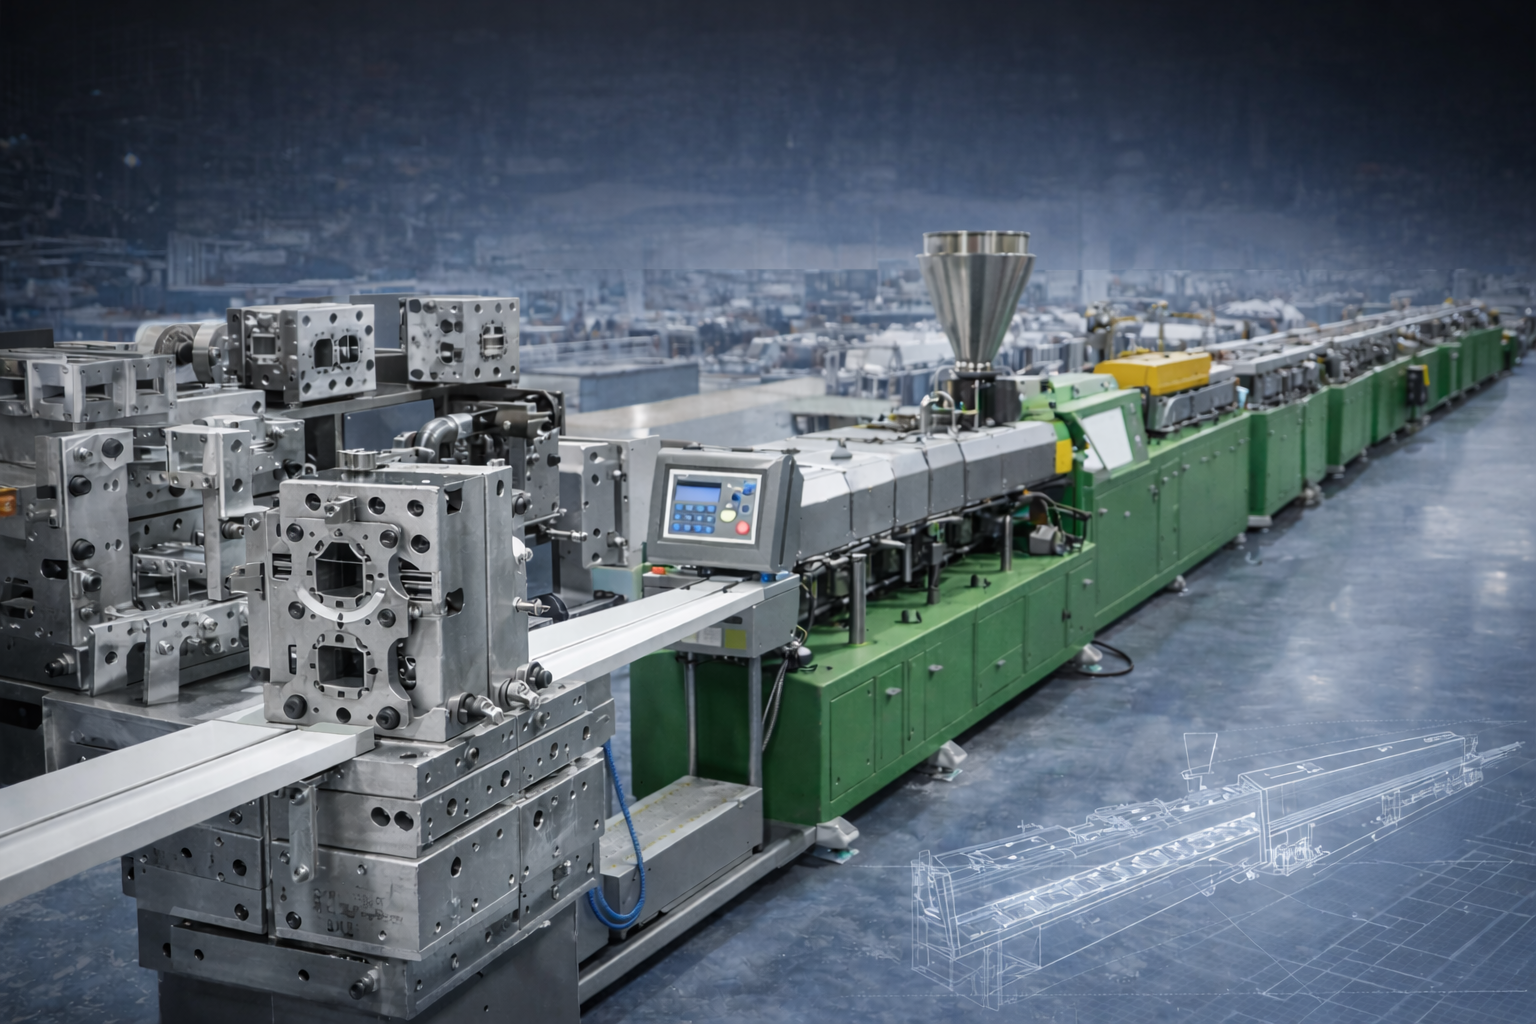
The EXTRUTEX EXCT-50 is a modular co-rotating twin-screw extruder designed for continuous polymer compounding, mixing, dispersion, homogenization, masterbatch production, recycling and other demanding thermoplastic processing applications.
With a 50 mm screw diameter, the EXCT-50 provides a higher processing capacity than the smaller EXCT series models while maintaining the flexibility of the modular twin-screw platform. The machine is designed for manufacturers requiring a versatile compounding system capable of processing different polymers, fillers, additives and formulations.
The EXCT-50 combines a co-rotating twin-screw system, modular screw and barrel construction, independently controlled processing zones and a practical clamshell barrel design.
The clamshell system provides rapid access to the screws and internal processing area, simplifying cleaning, maintenance, inspection, screw-element replacement and product changeover.
With an output range of approximately 60–150 kg/h, depending on material and process conditions, the EXCT-50 is suitable for pilot production, medium-scale manufacturing and specialized continuous compounding applications.
| Specification | EXCT-50 |
|---|---|
| Model | EXCT-50 |
| Screw Diameter | 50 mm |
| L/D Ratio | 28–48 |
| Screw Speed | 300–500 rpm |
| Main Motor Power | 37 / 45 kW |
| Production Capacity | 60–150 kg/h |
| Screw Type | Co-Rotating Twin Screw |
| Barrel Design | Modular Clamshell |
| Processing Mode | Continuous |
| Application | Compounding, Mixing, Dispersion, Masterbatch, Recycling & R&D |
Actual production capacity depends on polymer type, formulation, screw configuration, feeding rate, screw speed, temperature profile and other process conditions.
The 50 mm screw diameter gives the EXCT-50 a substantial processing platform for applications requiring greater throughput while retaining the flexibility of modular twin-screw technology.
The co-rotating twin-screw configuration provides simultaneous conveying, melting and mixing capabilities.
The two screws rotate in the same direction and can be equipped with different conveying, kneading and mixing elements. This allows the internal processing profile to be configured according to the material and desired result.
The EXCT-50 can therefore be configured for applications ranging from relatively gentle polymer blending to intensive filler dispersion and compounding.
The EXCT-50 is designed for an approximate production range of 60–150 kg/h.
This capacity makes the machine suitable for a wide variety of pilot and production applications.
Actual output is influenced by several factors, including:
Polymer type
Bulk density
Melt viscosity
Formulation
Filler concentration
Additive loading
Screw configuration
Screw speed
Feeding system
Processing temperature
Residence time
Required mixing intensity
Downstream pressure
For this reason, EXTRUTEX recommends selecting the final configuration according to the actual material and required production conditions rather than capacity alone.
The EXCT-50 provides a screw-speed range of approximately 300–500 rpm.
The operating speed can be selected according to the formulation and required processing intensity.
Different materials require different combinations of mechanical energy, residence time and mixing intensity. The modular screw system allows the EXCT-50 to be configured accordingly.
Higher screw speeds can provide increased mixing intensity and mechanical energy for suitable applications, while lower speeds can be selected when a gentler processing condition or longer residence time is preferred.
The relationship between screw speed, throughput, temperature and screw configuration should be optimized for each formulation.
The EXCT-50 can be configured with an L/D ratio from 28 to 48.
This provides flexibility in determining the effective processing length and number of functional zones.
A shorter configuration can be used for applications requiring fewer processing stages, while longer configurations provide additional space for more complex processes.
A longer processing arrangement may incorporate sequential zones such as:
Feeding → Conveying → Melting → Mixing → Dispersion → Degassing → Homogenization → Pressure Building → Discharge
The selected L/D ratio can therefore be matched to the required processing sequence.
The clamshell barrel is one of the practical features of the EXCT-50.
The barrel can be opened to provide direct access to the twin screws and processing chamber.
This simplifies important operational tasks such as:
Cleaning
Product changeover
Screw inspection
Screw-element replacement
Removal of residual material
Maintenance
Troubleshooting
Process development
For manufacturers processing several formulations, rapid access to the processing chamber can help reduce intervention time between products.
It is also particularly useful when developing new compounds where screw configurations may need to be changed and evaluated regularly.
The EXCT-50 uses a modular barrel concept in which different barrel sections can be arranged according to the requirements of the process.
Each processing section can have a specific function.
Possible zones include:
Feeding
Conveying
Preheating
Melting
Kneading
Mixing
Dispersion
Homogenization
Side feeding
Degassing
Vacuum devolatilization
Pressure building
Discharge
The modular barrel architecture allows the processing line to be configured around the formulation.
Each barrel section can be controlled independently to create an appropriate temperature profile along the extrusion process.
This is particularly important because different stages of compounding may require different thermal conditions.
The feeding zone may require controlled temperatures to prevent premature melting or bridging. The melting section may require higher thermal conditions, while mixing and downstream sections may require carefully controlled temperatures to maintain suitable melt viscosity.
The EXCT-50 can incorporate electrical heating and controlled cooling for the individual barrel zones.
This allows engineers to manage:
Melting temperature
Melt viscosity
Mixing conditions
Residence time
Thermal history
Devolatilization
Final melt temperature
The screw system of the EXCT-50 can be configured using different screw and kneading elements.
This allows the machine to perform several processing functions within one continuous barrel.
Conveying elements transport material through the barrel while controlling the filling level and residence time.
Dedicated screw sections promote controlled polymer melting and plasticization.
Kneading elements provide additional mechanical energy and mixing intensity where required.
Intensive mixing sections can be used to disperse fillers, pigments and additives into the polymer matrix.
The screw arrangement can promote uniform distribution of different formulation components.
Downstream elements can stabilize and homogenize the melt before discharge.
Dedicated sections can be incorporated for removal of moisture, air and volatile components.
The final screw sections can be configured to generate the pressure required for filtration and downstream equipment.
The EXCT-50 can be configured to perform a complete sequence of compounding operations.
Raw materials can be introduced through controlled feeding systems.
Depending on the formulation, the system can handle polymer pellets, powders, fillers, additives, pigments and other components.
Accurate feeding is essential for maintaining the desired formulation ratio and stable production.
The initial screw elements transport the materials through the extruder.
The conveying system can be configured according to the required throughput, filling level and residence time.
As the polymer moves through the processing zones, thermal and mechanical energy progressively convert the solid material into a homogeneous melt.
The screw geometry and barrel temperature profile can be adjusted according to the polymer.
After melting, the material passes through mixing and kneading sections.
These zones can provide both distributive and dispersive mixing.
The process can be configured for:
Polymer blends
Filled compounds
Masterbatch
Additive concentrates
Reinforced thermoplastics
Recycled compounds
When moisture or volatile components need to be removed, a dedicated degassing section can be incorporated.
Vacuum-assisted devolatilization can be used where appropriate to reduce unwanted volatile content in the melt.
Following intensive mixing and degassing, the melt can be stabilized through a downstream homogenization section.
The objective is to provide a consistent melt before filtration, pelletizing or forming.
The EXCT-50 can be combined with an appropriate melt-screening system.
Filtration can remove unwanted solid particles and contaminants before the melt reaches the downstream equipment.
This is particularly relevant to recycled materials and formulations containing impurities.
The final melt can be supplied to a suitable pelletizing or forming system.
Depending on the application, the EXCT-50 can be integrated with:
Strand pelletizing
Water-ring pelletizing
Melt filtration
Sheet dies
Profile dies
Customized downstream systems
The EXTRUTEX EXCT-50 can be used in a wide range of polymer-processing applications.
Typical applications include:
Polymer compounding
Masterbatch production
Color masterbatch
Filler masterbatch
Calcium carbonate compounds
Mineral-filled compounds
Polymer blending
Additive dispersion
Reinforced plastics
Engineering thermoplastics
Recycled polymer compounds
Recycling and re-compounding
Specialty compounds
R&D
Pilot production
Medium-scale continuous production
The final screw and barrel configuration should be selected according to the formulation and required processing conditions.
The EXCT-50 provides a useful intermediate platform between small development equipment and large industrial compounding systems.
Its 60–150 kg/h capacity range allows manufacturers to conduct meaningful production trials while maintaining a manageable machine size.
The modular architecture also makes it possible to test different screw configurations.
Engineers can evaluate:
Mixing intensity
Screw speed
Residence time
Feeding rate
Barrel temperature
Degassing conditions
Pressure
Throughput
Screw-element arrangement
This makes the EXCT-50 suitable for both product development and commercial production of specialized formulations.
The internal components of the EXCT-50 can be selected according to the material being processed.
Standard configurations can use suitable nitrided steel components, while more demanding applications can be equipped with enhanced wear- or corrosion-resistant materials and surface treatments.
This is especially important when processing abrasive formulations containing:
Calcium carbonate
Glass fiber
Mineral fillers
Wood fiber
Ceramic materials
High filler concentrations
Recycled polymers
Material selection can be adapted according to the actual formulation and operating conditions.
Provides a larger processing platform for higher-throughput compounding.
Suitable for pilot, specialized and medium-scale continuous production applications.
Provides flexible processing conditions for different formulations.
Allows the processing length to be matched to the required number of processing stages.
Motor configuration can be selected according to processing requirements.
Provides convenient and rapid access to the screws for maintenance, cleaning and product changeover.
Conveying, melting, kneading, mixing, dispersion, degassing and pressure-building zones can be configured as required.
Each processing section can be thermally controlled according to the material requirements.
Suitable for polymer compounding, masterbatch, recycling, filled compounds, polymer blending and R&D.
The EXTRUTEX EXCT-50 combines a 50 mm co-rotating twin-screw system, modular processing technology and a practical clamshell barrel into a flexible compounding platform.
With 300–500 rpm screw speed, 28–48 L/D configurations, 37/45 kW motor options and a production capacity of approximately 60–150 kg/h, the EXCT-50 is designed for manufacturers requiring greater throughput while retaining the process flexibility of a modular twin-screw extruder.
Its configurable screw and barrel architecture allows different processing stages to be integrated into one continuous system, including feeding, conveying, melting, kneading, mixing, dispersion, homogenization, degassing, pressure building and discharge.
The clamshell barrel provides convenient access to the processing chamber, helping simplify cleaning, maintenance, screw changes and product changeover.
EXTRUTEX EXCT-50 — Modular co-rotating twin-screw technology for flexible, efficient and controlled polymer compounding.
When production needs exceed the ordinary, the EXTRUTEX ATP 114-32S steps in — a masterclass in single-screw extrusion engineering.
Built with Austrian precision and forged for endurance, this machine transforms PVC and UPVC granules into flawless, smooth, dimensionally stable sheets at a rate few can match.
The ATP 114-32S represents the next generation of sheet extrusion — optimized for wide sheets, thick sections, and continuous high-capacity output.
It’s designed for manufacturers who demand more than performance — they demand perfection.
The EXTRUTEX ATP 114-32S integrates a special geometric screw design that optimizes material melting, mixing, and degassing.
This unique geometry ensures exceptional melt homogeneity, superior plasticization, and reduced thermal stress, even at high throughputs.
A bimetallic barrel paired with molybdenum-coated screws delivers outstanding wear resistance and a long operational life, while the 32 L/D ratio ensures excellent output consistency for rigid and semi-rigid PVC sheets.
Its AC vector drive motor and high-torque gearbox provide smooth, vibration-free power delivery, allowing precise control of melt pressure and sheet uniformity.
The multi-zone temperature control system, governed by a PLC-based control panel, maintains the thermal balance critical for quality surface finish and dimensional accuracy.
The ATP 114-32S is engineered for large-scale PVC sheet production — foamed or rigid — and can be configured with automatic feeders, melt pressure sensors, and integrated flat die systems for complete process control from hopper to haul-off.
| Parameter | Specification |
|---|---|
| Model | EXTRUTEX ATP 114-32S |
| Application | UPVC / PVC Rigid Sheet Extrusion |
| Screw Diameter | 114 mm |
| L/D Ratio | 32:1 |
| Output Range | 270 – 450 kg/h |
| Installed Power | 107 kW |
| Drive Type | AC Vector Drive Motor |
| Screw Design | Special Geometric Design for PVC Melting and Mixing |
| Barrel Material | Nitrided / Bimetallic with Molybdenum Coating |
| Gearbox Type | High Torque, Low Noise Design |
| Heating Zones | Multi-Zone (6 to 8 Zones Adjustable) |
| Cooling System | Air / Water Integrated Cooling System |
| Control System | PLC with Touch Screen Operation |
| Degassing System | Optional Single / Double Vented Design |
| Feeding System | Automatic Volumetric / Gravimetric Feeder |
| Melt Temperature Range | 170 – 195 °C (adjustable) |
| Applications | PVC Foam Board, Rigid PVC Sheet, Advertising Panels, UPVC Flat Panels |
| Output Stability | ±1.5% Consistency |
| Country of Origin | Austria (Designed by EXTRUTEX) |
The ATP 114-32S excels where productivity meets precision.
Its robust torque, thermal uniformity, and melt stability guarantee consistent sheet thickness and perfect surface clarity — even under continuous, 24-hour production cycles.
With 107 kW of engineered efficiency, it delivers the ideal balance between power consumption and throughput, resulting in reduced operating costs and maximized profitability.
Every component — from gearbox to barrel — is built to EXTRUTEX’s uncompromising European standards, making this extruder not just a machine, but a long-term production partner.

There are no reviews yet.
The EXTRUTEX EXCT-50 is a modular co-rotating twin-screw extruder designed for continuous polymer compounding, mixing, dispersion, homogenization, masterbatch production, recycling and other demanding thermoplastic processing applications.
With a 50 mm screw diameter, the EXCT-50 provides a higher processing capacity than the smaller EXCT series models while maintaining the flexibility of the modular twin-screw platform. The machine is designed for manufacturers requiring a versatile compounding system capable of processing different polymers, fillers, additives and formulations.
The EXCT-50 combines a co-rotating twin-screw system, modular screw and barrel construction, independently controlled processing zones and a practical clamshell barrel design.
The clamshell system provides rapid access to the screws and internal processing area, simplifying cleaning, maintenance, inspection, screw-element replacement and product changeover.
With an output range of approximately 60–150 kg/h, depending on material and process conditions, the EXCT-50 is suitable for pilot production, medium-scale manufacturing and specialized continuous compounding applications.
| Specification | EXCT-50 |
|---|---|
| Model | EXCT-50 |
| Screw Diameter | 50 mm |
| L/D Ratio | 28–48 |
| Screw Speed | 300–500 rpm |
| Main Motor Power | 37 / 45 kW |
| Production Capacity | 60–150 kg/h |
| Screw Type | Co-Rotating Twin Screw |
| Barrel Design | Modular Clamshell |
| Processing Mode | Continuous |
| Application | Compounding, Mixing, Dispersion, Masterbatch, Recycling & R&D |
Actual production capacity depends on polymer type, formulation, screw configuration, feeding rate, screw speed, temperature profile and other process conditions.
The 50 mm screw diameter gives the EXCT-50 a substantial processing platform for applications requiring greater throughput while retaining the flexibility of modular twin-screw technology.
The co-rotating twin-screw configuration provides simultaneous conveying, melting and mixing capabilities.
The two screws rotate in the same direction and can be equipped with different conveying, kneading and mixing elements. This allows the internal processing profile to be configured according to the material and desired result.
The EXCT-50 can therefore be configured for applications ranging from relatively gentle polymer blending to intensive filler dispersion and compounding.
The EXCT-50 is designed for an approximate production range of 60–150 kg/h.
This capacity makes the machine suitable for a wide variety of pilot and production applications.
Actual output is influenced by several factors, including:
Polymer type
Bulk density
Melt viscosity
Formulation
Filler concentration
Additive loading
Screw configuration
Screw speed
Feeding system
Processing temperature
Residence time
Required mixing intensity
Downstream pressure
For this reason, EXTRUTEX recommends selecting the final configuration according to the actual material and required production conditions rather than capacity alone.
The EXCT-50 provides a screw-speed range of approximately 300–500 rpm.
The operating speed can be selected according to the formulation and required processing intensity.
Different materials require different combinations of mechanical energy, residence time and mixing intensity. The modular screw system allows the EXCT-50 to be configured accordingly.
Higher screw speeds can provide increased mixing intensity and mechanical energy for suitable applications, while lower speeds can be selected when a gentler processing condition or longer residence time is preferred.
The relationship between screw speed, throughput, temperature and screw configuration should be optimized for each formulation.
The EXCT-50 can be configured with an L/D ratio from 28 to 48.
This provides flexibility in determining the effective processing length and number of functional zones.
A shorter configuration can be used for applications requiring fewer processing stages, while longer configurations provide additional space for more complex processes.
A longer processing arrangement may incorporate sequential zones such as:
Feeding → Conveying → Melting → Mixing → Dispersion → Degassing → Homogenization → Pressure Building → Discharge
The selected L/D ratio can therefore be matched to the required processing sequence.
The clamshell barrel is one of the practical features of the EXCT-50.
The barrel can be opened to provide direct access to the twin screws and processing chamber.
This simplifies important operational tasks such as:
Cleaning
Product changeover
Screw inspection
Screw-element replacement
Removal of residual material
Maintenance
Troubleshooting
Process development
For manufacturers processing several formulations, rapid access to the processing chamber can help reduce intervention time between products.
It is also particularly useful when developing new compounds where screw configurations may need to be changed and evaluated regularly.
The EXCT-50 uses a modular barrel concept in which different barrel sections can be arranged according to the requirements of the process.
Each processing section can have a specific function.
Possible zones include:
Feeding
Conveying
Preheating
Melting
Kneading
Mixing
Dispersion
Homogenization
Side feeding
Degassing
Vacuum devolatilization
Pressure building
Discharge
The modular barrel architecture allows the processing line to be configured around the formulation.
Each barrel section can be controlled independently to create an appropriate temperature profile along the extrusion process.
This is particularly important because different stages of compounding may require different thermal conditions.
The feeding zone may require controlled temperatures to prevent premature melting or bridging. The melting section may require higher thermal conditions, while mixing and downstream sections may require carefully controlled temperatures to maintain suitable melt viscosity.
The EXCT-50 can incorporate electrical heating and controlled cooling for the individual barrel zones.
This allows engineers to manage:
Melting temperature
Melt viscosity
Mixing conditions
Residence time
Thermal history
Devolatilization
Final melt temperature
The screw system of the EXCT-50 can be configured using different screw and kneading elements.
This allows the machine to perform several processing functions within one continuous barrel.
Conveying elements transport material through the barrel while controlling the filling level and residence time.
Dedicated screw sections promote controlled polymer melting and plasticization.
Kneading elements provide additional mechanical energy and mixing intensity where required.
Intensive mixing sections can be used to disperse fillers, pigments and additives into the polymer matrix.
The screw arrangement can promote uniform distribution of different formulation components.
Downstream elements can stabilize and homogenize the melt before discharge.
Dedicated sections can be incorporated for removal of moisture, air and volatile components.
The final screw sections can be configured to generate the pressure required for filtration and downstream equipment.
The EXCT-50 can be configured to perform a complete sequence of compounding operations.
Raw materials can be introduced through controlled feeding systems.
Depending on the formulation, the system can handle polymer pellets, powders, fillers, additives, pigments and other components.
Accurate feeding is essential for maintaining the desired formulation ratio and stable production.
The initial screw elements transport the materials through the extruder.
The conveying system can be configured according to the required throughput, filling level and residence time.
As the polymer moves through the processing zones, thermal and mechanical energy progressively convert the solid material into a homogeneous melt.
The screw geometry and barrel temperature profile can be adjusted according to the polymer.
After melting, the material passes through mixing and kneading sections.
These zones can provide both distributive and dispersive mixing.
The process can be configured for:
Polymer blends
Filled compounds
Masterbatch
Additive concentrates
Reinforced thermoplastics
Recycled compounds
When moisture or volatile components need to be removed, a dedicated degassing section can be incorporated.
Vacuum-assisted devolatilization can be used where appropriate to reduce unwanted volatile content in the melt.
Following intensive mixing and degassing, the melt can be stabilized through a downstream homogenization section.
The objective is to provide a consistent melt before filtration, pelletizing or forming.
The EXCT-50 can be combined with an appropriate melt-screening system.
Filtration can remove unwanted solid particles and contaminants before the melt reaches the downstream equipment.
This is particularly relevant to recycled materials and formulations containing impurities.
The final melt can be supplied to a suitable pelletizing or forming system.
Depending on the application, the EXCT-50 can be integrated with:
Strand pelletizing
Water-ring pelletizing
Melt filtration
Sheet dies
Profile dies
Customized downstream systems
The EXTRUTEX EXCT-50 can be used in a wide range of polymer-processing applications.
Typical applications include:
Polymer compounding
Masterbatch production
Color masterbatch
Filler masterbatch
Calcium carbonate compounds
Mineral-filled compounds
Polymer blending
Additive dispersion
Reinforced plastics
Engineering thermoplastics
Recycled polymer compounds
Recycling and re-compounding
Specialty compounds
R&D
Pilot production
Medium-scale continuous production
The final screw and barrel configuration should be selected according to the formulation and required processing conditions.
The EXCT-50 provides a useful intermediate platform between small development equipment and large industrial compounding systems.
Its 60–150 kg/h capacity range allows manufacturers to conduct meaningful production trials while maintaining a manageable machine size.
The modular architecture also makes it possible to test different screw configurations.
Engineers can evaluate:
Mixing intensity
Screw speed
Residence time
Feeding rate
Barrel temperature
Degassing conditions
Pressure
Throughput
Screw-element arrangement
This makes the EXCT-50 suitable for both product development and commercial production of specialized formulations.
The internal components of the EXCT-50 can be selected according to the material being processed.
Standard configurations can use suitable nitrided steel components, while more demanding applications can be equipped with enhanced wear- or corrosion-resistant materials and surface treatments.
This is especially important when processing abrasive formulations containing:
Calcium carbonate
Glass fiber
Mineral fillers
Wood fiber
Ceramic materials
High filler concentrations
Recycled polymers
Material selection can be adapted according to the actual formulation and operating conditions.
Provides a larger processing platform for higher-throughput compounding.
Suitable for pilot, specialized and medium-scale continuous production applications.
Provides flexible processing conditions for different formulations.
Allows the processing length to be matched to the required number of processing stages.
Motor configuration can be selected according to processing requirements.
Provides convenient and rapid access to the screws for maintenance, cleaning and product changeover.
Conveying, melting, kneading, mixing, dispersion, degassing and pressure-building zones can be configured as required.
Each processing section can be thermally controlled according to the material requirements.
Suitable for polymer compounding, masterbatch, recycling, filled compounds, polymer blending and R&D.
The EXTRUTEX EXCT-50 combines a 50 mm co-rotating twin-screw system, modular processing technology and a practical clamshell barrel into a flexible compounding platform.
With 300–500 rpm screw speed, 28–48 L/D configurations, 37/45 kW motor options and a production capacity of approximately 60–150 kg/h, the EXCT-50 is designed for manufacturers requiring greater throughput while retaining the process flexibility of a modular twin-screw extruder.
Its configurable screw and barrel architecture allows different processing stages to be integrated into one continuous system, including feeding, conveying, melting, kneading, mixing, dispersion, homogenization, degassing, pressure building and discharge.
The clamshell barrel provides convenient access to the processing chamber, helping simplify cleaning, maintenance, screw changes and product changeover.
EXTRUTEX EXCT-50 — Modular co-rotating twin-screw technology for flexible, efficient and controlled polymer compounding.
When production needs exceed the ordinary, the EXTRUTEX ATP 114-32S steps in — a masterclass in single-screw extrusion engineering.
Built with Austrian precision and forged for endurance, this machine transforms PVC and UPVC granules into flawless, smooth, dimensionally stable sheets at a rate few can match.
The ATP 114-32S represents the next generation of sheet extrusion — optimized for wide sheets, thick sections, and continuous high-capacity output.
It’s designed for manufacturers who demand more than performance — they demand perfection.
The EXTRUTEX ATP 114-32S integrates a special geometric screw design that optimizes material melting, mixing, and degassing.
This unique geometry ensures exceptional melt homogeneity, superior plasticization, and reduced thermal stress, even at high throughputs.
A bimetallic barrel paired with molybdenum-coated screws delivers outstanding wear resistance and a long operational life, while the 32 L/D ratio ensures excellent output consistency for rigid and semi-rigid PVC sheets.
Its AC vector drive motor and high-torque gearbox provide smooth, vibration-free power delivery, allowing precise control of melt pressure and sheet uniformity.
The multi-zone temperature control system, governed by a PLC-based control panel, maintains the thermal balance critical for quality surface finish and dimensional accuracy.
The ATP 114-32S is engineered for large-scale PVC sheet production — foamed or rigid — and can be configured with automatic feeders, melt pressure sensors, and integrated flat die systems for complete process control from hopper to haul-off.
| Parameter | Specification |
|---|---|
| Model | EXTRUTEX ATP 114-32S |
| Application | UPVC / PVC Rigid Sheet Extrusion |
| Screw Diameter | 114 mm |
| L/D Ratio | 32:1 |
| Output Range | 270 – 450 kg/h |
| Installed Power | 107 kW |
| Drive Type | AC Vector Drive Motor |
| Screw Design | Special Geometric Design for PVC Melting and Mixing |
| Barrel Material | Nitrided / Bimetallic with Molybdenum Coating |
| Gearbox Type | High Torque, Low Noise Design |
| Heating Zones | Multi-Zone (6 to 8 Zones Adjustable) |
| Cooling System | Air / Water Integrated Cooling System |
| Control System | PLC with Touch Screen Operation |
| Degassing System | Optional Single / Double Vented Design |
| Feeding System | Automatic Volumetric / Gravimetric Feeder |
| Melt Temperature Range | 170 – 195 °C (adjustable) |
| Applications | PVC Foam Board, Rigid PVC Sheet, Advertising Panels, UPVC Flat Panels |
| Output Stability | ±1.5% Consistency |
| Country of Origin | Austria (Designed by EXTRUTEX) |
The ATP 114-32S excels where productivity meets precision.
Its robust torque, thermal uniformity, and melt stability guarantee consistent sheet thickness and perfect surface clarity — even under continuous, 24-hour production cycles.
With 107 kW of engineered efficiency, it delivers the ideal balance between power consumption and throughput, resulting in reduced operating costs and maximized profitability.
Every component — from gearbox to barrel — is built to EXTRUTEX’s uncompromising European standards, making this extruder not just a machine, but a long-term production partner.
By submitting your email, you agree to our company’s terms and conditions.
We are not looking to sell; we are here to provide you with the best support and service.
Contact available 24/7
Please do not contact us for advertising or sales inquiries
All rights of this website are reserved for EXTRUTEX Austria and its partner companies, © 2026
-
(0 customer reviews)